Engineering Whitepaper & Strategic Sourcing Guide

China Armature Generator Suppliers & Factories: Industrial Engineering & Global Supply Chain Resilience

Technical evaluation, metallurgy roadmap, lifecycle longevity benchmarks, and factory audit criteria for high-precision commutators and electromagnetic armatures in automotive EFI, power generation, and precision micromotors.

Certified Component Catalog

High-Torque Armature & Commutator Assembly Matrix

Explore our Tier-1 benchmarked product series engineered for corrosive fuel mixtures, high-altitude excitation stability, and extended continuous-duty cycles.

Core Product Carbon graphite commutator for EFI fuel pump armature

Carbon Commutator

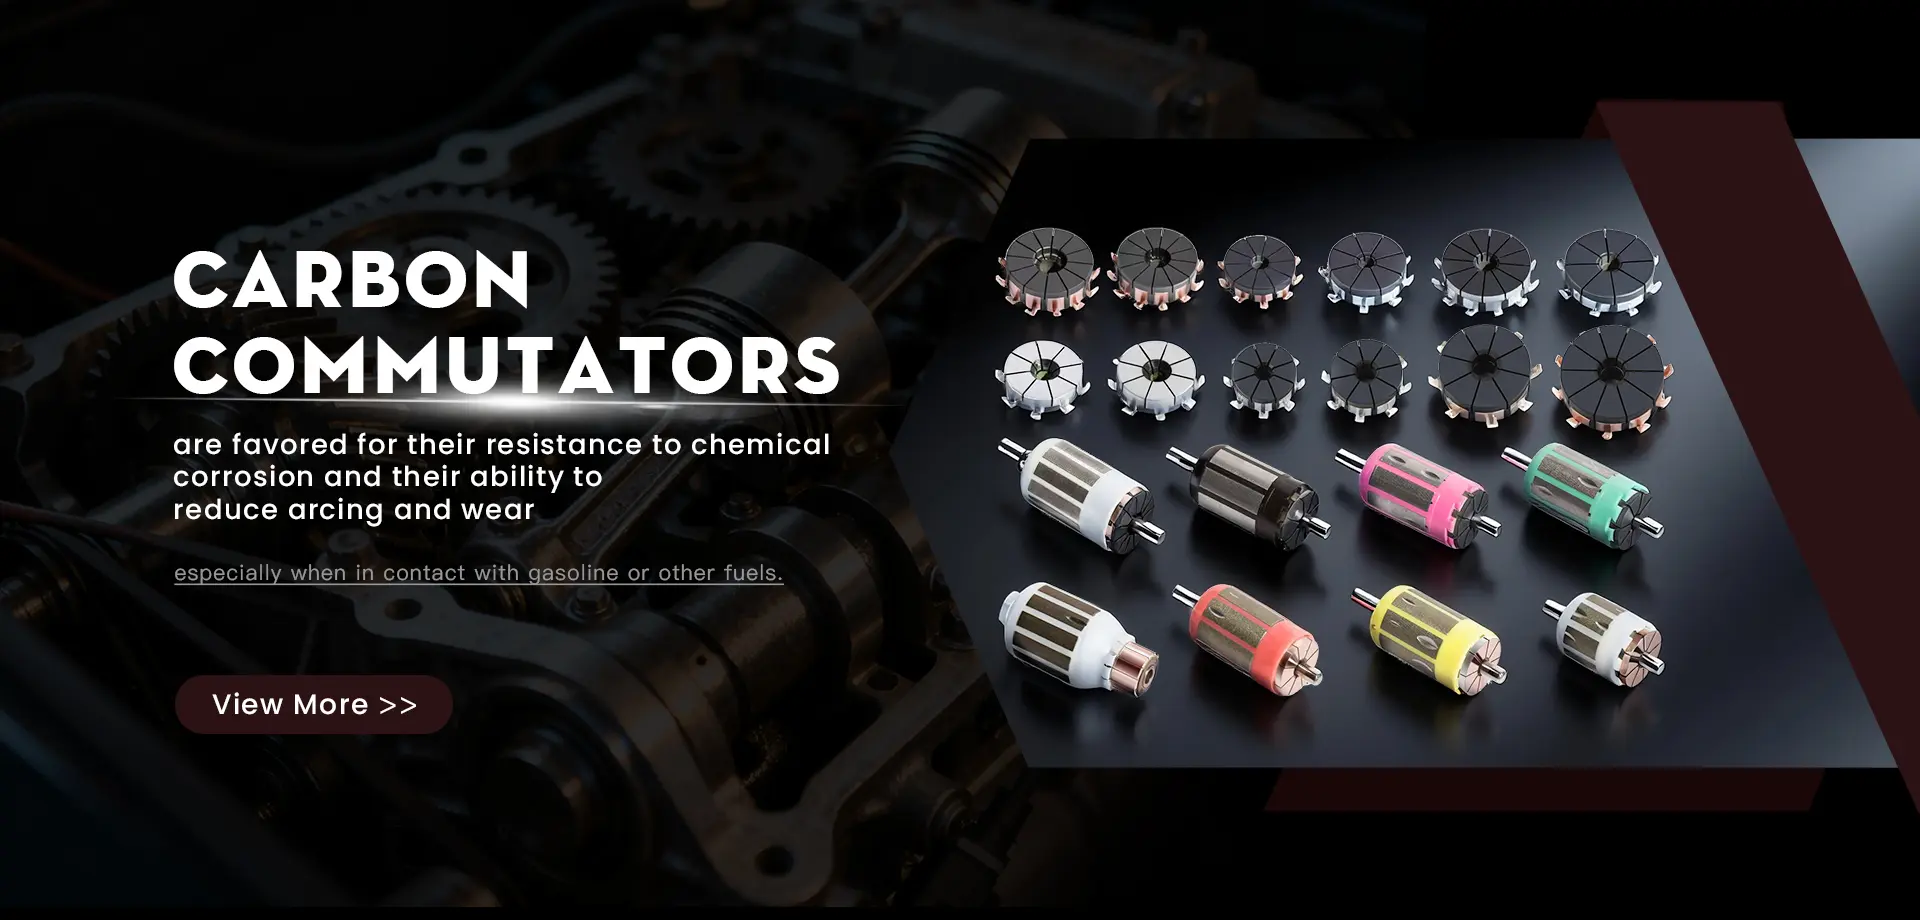
Carbon-graphite disc architecture engineered for automotive and small-engine rotating armatures facing intense alcohol erosion.

  • Segment MaterialGraphite-Ag Composite
  • Dielectric Strength> 2500 V/50Hz
View Technical Spec
Armature Core Hualeao electric fuel pump and fuel pump armature components

Balanced Rotor Armatures

Precision dynamic-balanced armature assemblies built with cold-rolled silicon steel laminations to minimize eddy-current losses.

  • Dynamic Balance≤ 2.5 mg·mm
  • Shaft HardnessHRC 58-62
View Technical Spec
Power Generation Electric fuel pump for automotive electronic fuel injection

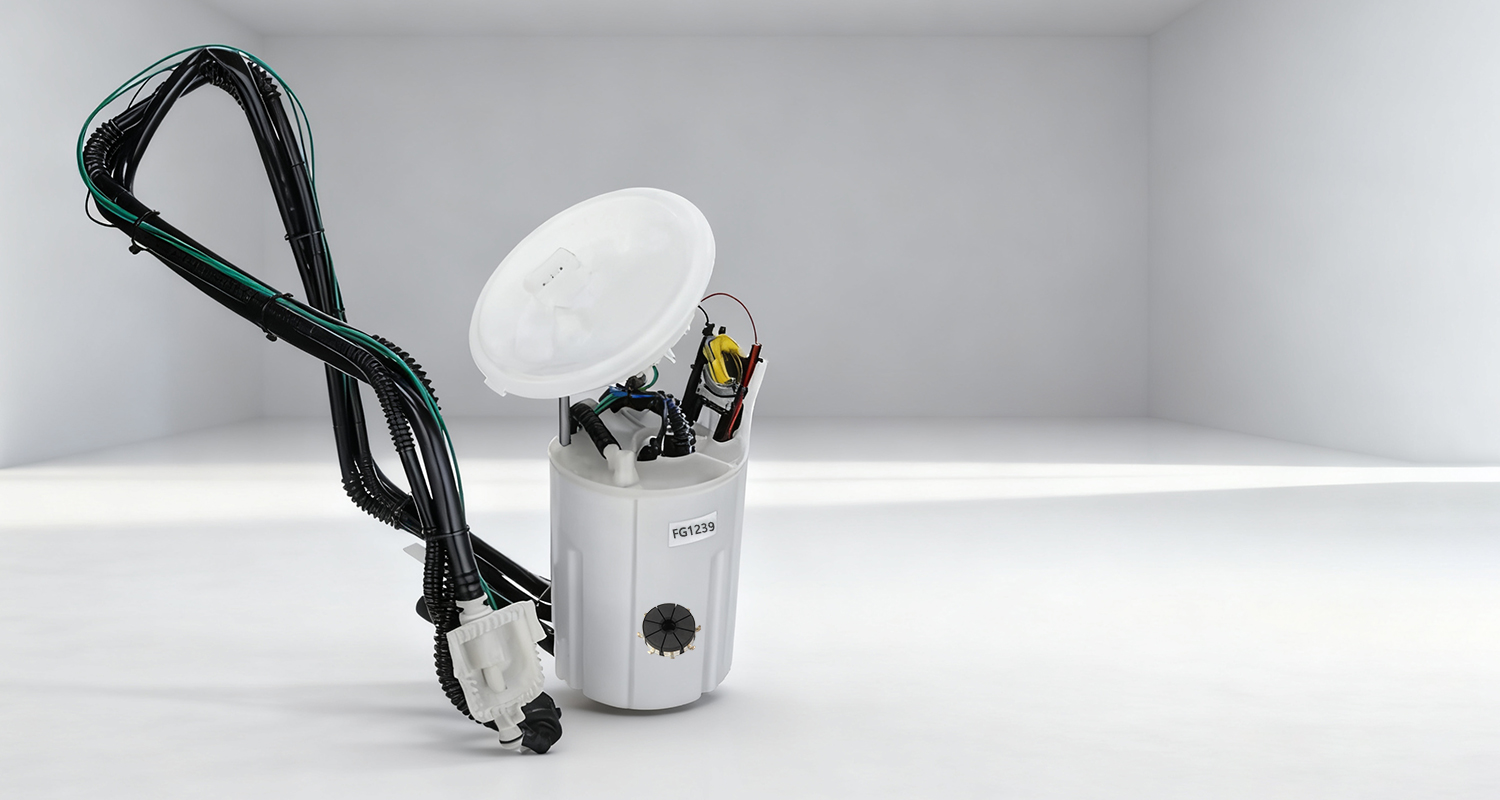
Electric Fuel Pump

Integrated high-pressure micro-motor pump featuring high mechanical efficiency, stable pressure delivery, and whisper-quiet operation.

  • Working Pressure3.0 - 5.5 Bar
  • Operational Flow> 110 L/Hour
View Technical Spec
Combustion Control Automotive oxygen sensor 89465-0E040 lambda sensor

Oxygen Sensor

High-sensitivity planar ceramic sensing element, providing real-time feedback loops to ECU processors for optimal stoichiometric combustion.

  • Response Speed≤ 100 ms
  • Sensor Reference89465-0E040 OE
View Technical Spec
Best-Seller HC-QZQE-049C carbon commutator best-selling fuel pump part

HC-QZQE-049C Commutator

Flagship alcohol-proof commutator variant configured with high-purity reinforced copper alloy base hooks and carbon contact segments.

  • Hook Tensile Force> 180 N
  • Alcohol ToleranceE85 / M100 Proof
View Technical Spec
Extreme Environments Ethanol- and methanol-resistant carbon commutators for fuel pump motors

Methanol Resistant Rotors

Surface-passivated commutator discs built to stop galvanic electrolysis in high-methanol and flex-fuel powertrain applications.

  • Insulation ResinThermoset Phenolic
  • Salt Mist Durability96h ASTM B117
View Technical Spec
High RPM Unit Function of a commutator in a DC motor

High-Speed Commutator Core

Engineered for high rotational speeds exceeding 12,000 RPM, preventing segment lifting and minimizing brush arcing damage.

  • Centrifugal Test18,000 RPM Burst
  • Surface SmoothnessRa ≤ 0.2 μm
View Technical Spec
Full System Automotive engine fuel system using carbon commutator fuel pumps

EFI Submersible Assembly

Turnkey pump motor assembly containing armatures, precision winding, built-in carbon commutators, and electromagnetic filters.

  • Voltage Rating12V / 24V DC
  • EMC SuppressionCISPR 25 Class 3
View Technical Spec
Executive Sourcing Insights

Evaluating China Armature Generator Suppliers & Factories

A comprehensive engineering breakdown for supply chain directors, procurement leads, and automotive electro-mechanical engineers assessing Chinese manufacturing clusters.

Electromagnetic Efficiency & Copper Fill Ratios

The core quality of generator and micro-motor armatures depends entirely on the slot design, the magnetic saturation point of laminated silicon steel (usually 50WW600 or 50WW470 grades), and high-density automatic needle winding. Leading Chinese factories deploy automated multi-axis precision winders ensuring uniform slot fills exceeding 85%, which dramatically suppresses harmonic losses and operating thermal escalation.

Commutation Metallurgy & Carbon Tribology

Standard copper commutators rapidly develop copper oxide build-up, segment pitting, and excessive brush dust under high vibration or when submerged in oxygenated biofuels (such as E20, E85, or M15). China's leading tier-1 innovators utilize sintered carbon-graphite blocks bonded to precision copper terminals, delivering superior self-lubricating tribology, near-zero spark erosion, and extended operating lifecycles exceeding 6,000 hours.

Total Dimensional Repeatability (Cpk ≥ 1.67)

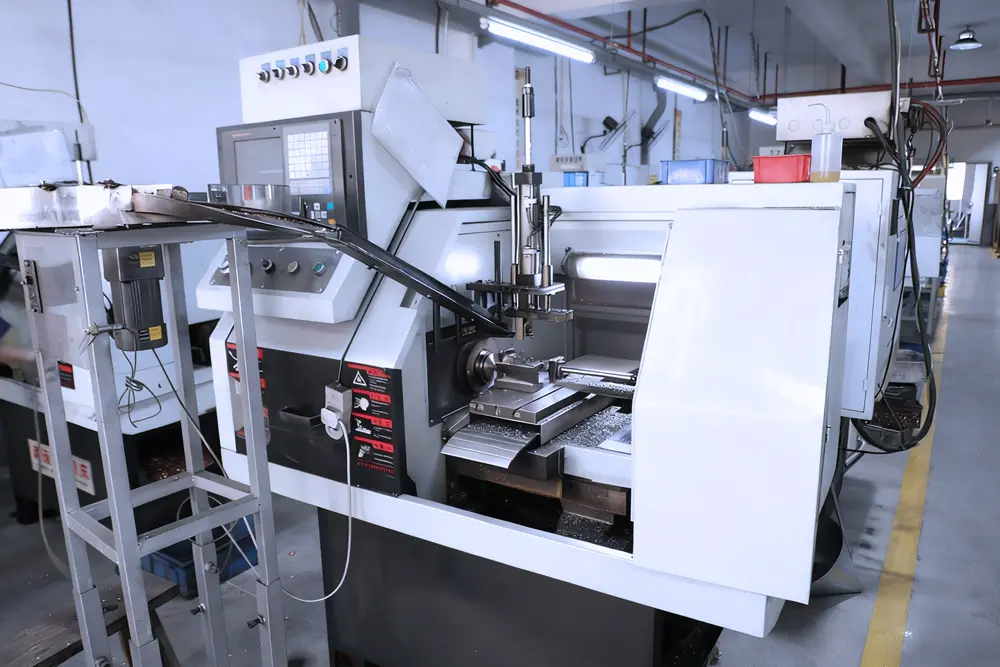
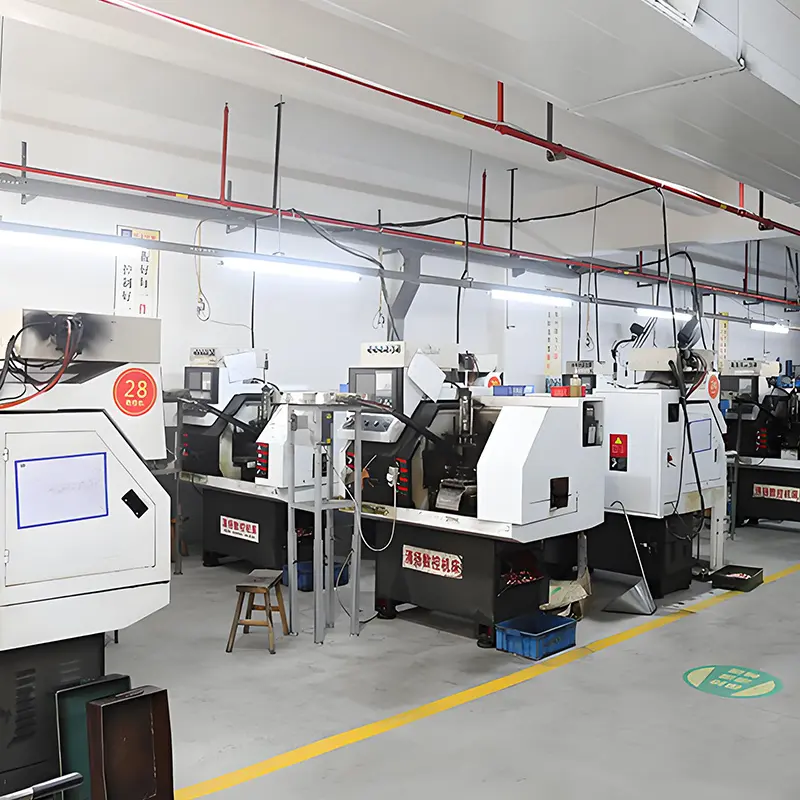
Armature generator components require sub-micron precision on shaft runout, commutator outer-diameter concentricity, and inter-segment insulation spacing. Wenzhou Hualeao maintains an automated optical measurement closed-loop across its CNC turning and slotting lines, securing critical Cpk values ≥ 1.67 across serial aftermarket and OEM production runs.

Industrial Ecosystem

China Factory Cluster Resilience: The Wenzhou Manufacturing Engine

How hyper-concentrated regional supply chains allow Chinese generator armature manufacturers to offer unmatched prototyping speed, price stability, and batch-to-batch consistency.

Raw Material Proximity

Our Ruian, Wenzhou base provides immediate access to ISO-certified cold-heading copper providers, high-purity synthetic graphite producers, and specialized thermosetting phenolic molding compounds within a 40-kilometer radius.

Rapid Tooling Iteration

Integrated tooling workshops reduce complex die modification timelines from traditional 6-week Western turnarounds down to 10 working days, significantly compressing our clients' Time-to-Market (TTM).

Cost Scalability & Lean Margins

Automated stamping, multi-cavity injection tooling, and computerized winding lines allow steady output scaling while keeping piece-rate prices 25% to 40% below European and North American manufacturing equivalents.

Supply Stability Assurances

Buffer inventories of critical electrolytic copper, custom formulated bonding glues, and graphite blanks ensure uninterrupted assembly schedules even during seasonal shipping fluctuations or global commodity spikes.

6,200 m²
Modern Clean Production Facility
50+
Precision Engineers & Technicians
10+
Patented Tooling & Quality Certs
3,000+
Worldwide Commercial Partners
Engineering Deployments

Armature & Commutator Field Deployment Environments

From extreme tropical humidity to high-vibration off-highway power stations, our commutators and armatures are tailored to hostile real-world operational stressors.

Automotive EFI Fuel Systems

Modern passenger cars and light commercial vehicles require fuel pumps to operate submerged in harsh gasoline-ethanol blends. Our carbon commutators resist ethanol chemical breakdown and mechanical abrasion, maintaining continuous fuel delivery without sparking or pressure decay.

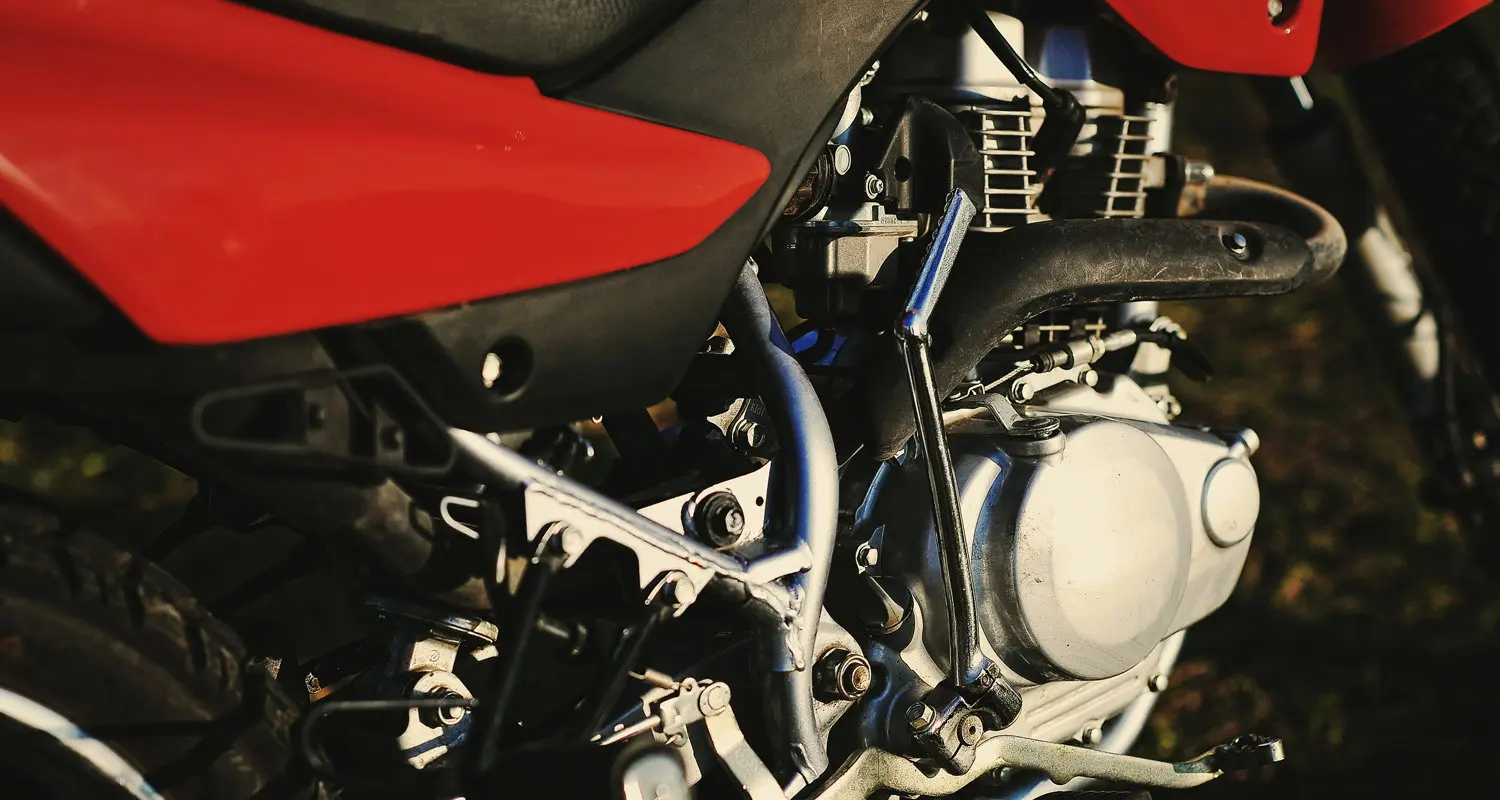
High-Revving Motorcycles

Two-wheelers and scooters place heavy electrical and physical strain on compact fuel pumps due to high engine vibration and space constraints. Our miniaturized commutators maintain high-frequency electrical contact stability under revs exceeding 10,000 RPM.

Heavy Machinery & Mining

Excavators, hydraulic earthmovers, and mining trucks run long continuous duty cycles in high heat and dust. Our armature assemblies feature class-H thermal insulation and reinforced windings that withstand continuous 180°C core temperatures.

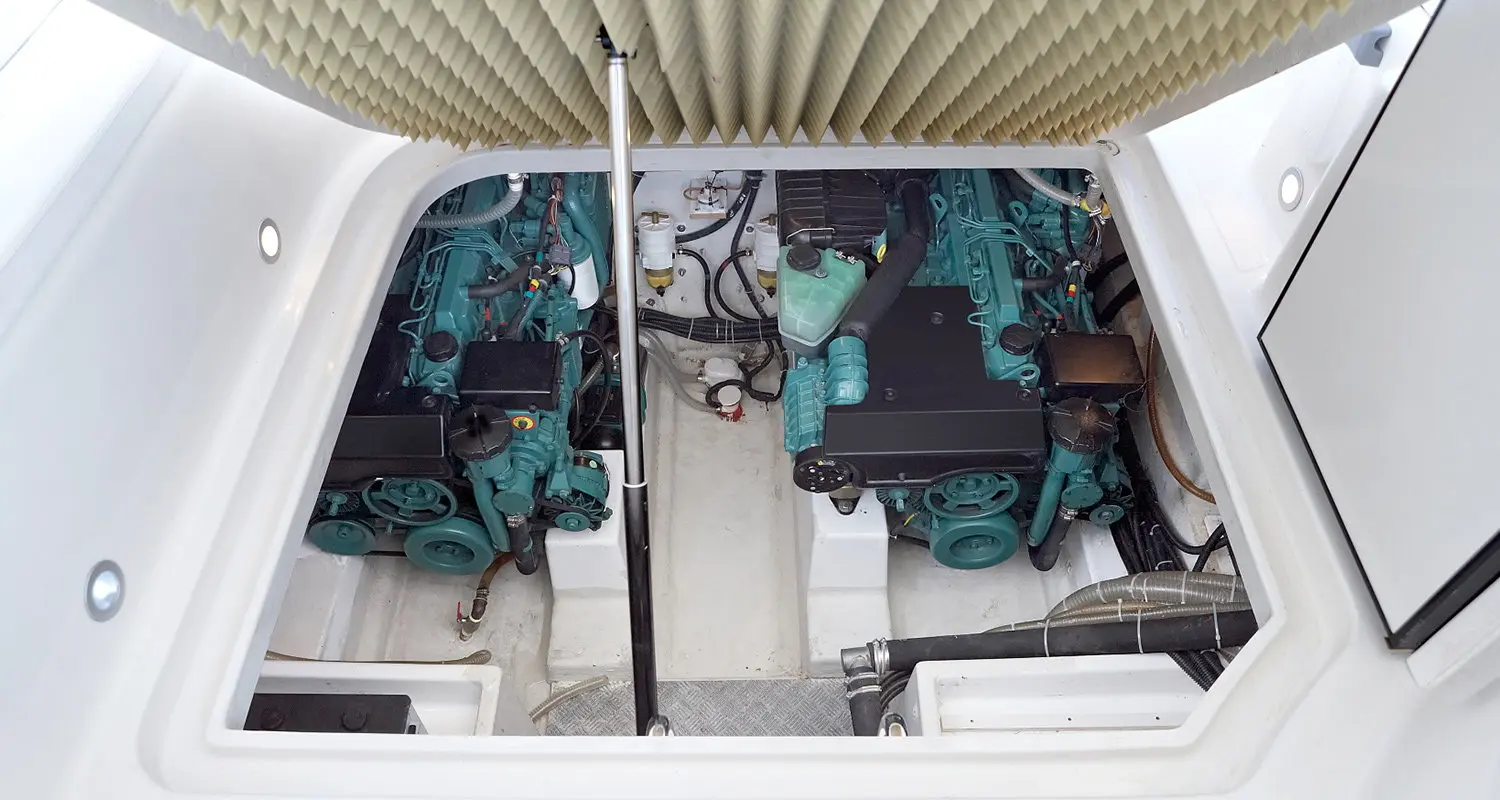
Marine & Coastal Generators

Salt spray and constant high humidity degrade standard metal commutators through rapid galvanic corrosion. We apply specialized surface passivations, anti-corrosive synthetic graphite, and epoxy encapsulation to prevent electrical failure in marine outboards and marine gensets.

Materials Metallurgy Review

Direct Engineering Comparison: Copper vs. Carbon Commutator Assemblies

Understanding the electrical, mechanical, and electrochemical differences determining fuel pump and armature life in modernized powertrain systems.

Performance Criteria Standard Copper Commutators Hualeao Graphite / Carbon Composite Procurement Impact
Corrosion Resistance in E10-E85 Ethanol Poor. Rapid acid pitting, oxide formation, and heavy surface cavitation. Immune. Chemically inert graphite face eliminates galvanic electrolysis. Critical for emerging flex-fuel market warranties (Brazil, EU, USA).
Friction Coefficient (μ) & Brush Wear 0.28 – 0.35 μ. Rapid brush degradation generating conductive copper dust. 0.12 – 0.18 μ. Self-lubricating graphite reduces brush degradation by 65%. Triples pump MTBF (Mean Time Between Failures) to >5,000 hours.
Operating Noise & EMI Signature Moderate to high. Spark discharge creates significant electrical interference. Ultra-low. Smooth arc transitions satisfy strict automotive EMC limits. Passes stringent CISPR 25 Class 3/4 radiated noise requirements.
Segment Thermal Expansion Stability High expansion rate risking segment lift under localized high-temperature spikes. Ultra-low CTE (Coefficient of Thermal Expansion) closely matches core resins. Prevents commutator segment lifting during run-dry thermal shock.
Initial Unit Cost Ratio Baseline benchmark (1.0x). 1.10x – 1.25x (higher raw material sintering expense). Offset by a 300% lifespan jump, lowering global warranty claims.
Quality Assurance Protocols

IATF 16949-Aligned Armature & Commutator Manufacturing

From metallurgical validation of incoming synthetic graphite to optical runout verification, our 4-stage inspection system guarantees field reliability.

Stage 1: Spectrometric Material Verification

Every batch of oxygen-free copper, carbon block blends, and specialized phenolic molding resin undergoes spectroscopic chemistry validation, grain-structure density checks, and glass transition temperature (Tg) testing prior to pressing.

Stage 2: Compression & Direct Sintering

Tooling dies utilize high-tonnage multi-stage hot pressing to bond the carbon-graphite contact face to the copper structural hooks without micro-voids, delivering shear bond strengths exceeding international OEM targets.

Stage 3: Diamond CNC Turning & Undercutting

Commutator ODs and segment isolation grooves are finished with natural monocrystalline diamond cutting tools, achieving optical surface finishes (Ra ≤ 0.2 μm) while ensuring inter-segment air clearances remain burr-free.

Stage 4: Dielectric Breakdown & Spin Testing

Every serial unit faces 100% dielectric isolation testing (2,500V breakdown test) alongside 15,000 RPM centrifugal overspeed screening to verify segment structural anchoring against hot centrifugal deformation.

R&D Strategy

Technology Roadmap: Next-Gen Armature & Hybrid Solutions

How Chinese factories are innovating beyond legacy brushed architectures to support hydrogen, hybrid, and ultra-high-efficiency electric auxiliary platforms.

Hydrogen & Methanol Fuel Cell Auxiliaries

As green hydrogen, e-methanol, and synthetic fuels enter heavy logistics, traditional electrical accessories require chemically unreactive contact materials. Our advanced carbon-graphite matrices are formulated to prevent hydrogen embrittlement in auxiliary circulation pumps and fuel cell humidifiers.

Nanocomposite Graphene Impregnation

By blending nanoscale graphene platelets into the standard sintered synthetic graphite matrix, our advanced R&D line has boosted mechanical flexural strength by 40% while dropping contact electrical resistance by 18%, reducing heat build-up under rapid duty-cycle starts.

Brushless DC (BLDC) Integrated Rotors

In step with the electrification shift toward BLDC motor systems, Hualeao produces precision-skewed laminated armatures equipped with bonded rare-earth Neodymium (NdFeB) ring magnets, delivering frictionless efficiency for Tier-1 smart powertrain pumps.

Regulatory Adherence

Global Market Compliance & Import Risk Mitigation

Ensuring complete documentation, hazardous substance elimination, and supply transparency for procurement teams across North America, the European Union, and the Asia-Pacific.

RoHS & REACH SVHC Free

All copper hook matrices, brazing solders, synthetic graphite blocks, and insulating phenolic compounds are completely free of hazardous substances. We maintain third-party testing via SGS/TUV to guarantee lead (Pb), cadmium (Cd), and mercury (Hg) content remain well within EU thresholds.

IMDS Material Data Sheet Filings

For Tier-1 automotive fuel system assemblers requiring traceability, Hualeao provides full International Material Data System (IMDS) declarations, expediting OEM vehicle audit approvals and PPAP Level 3 documentation submittals.

Supply Chain Transparency & Dual Sourcing

To shield clients from unexpected tariff shocks or geopolitical shipping disruptions, we provide clear origin manifests, export compliance paperwork, and flexible logistics through Ningbo and Shanghai deep-water container terminals.

Extended Catalog Matrix

Explore Additional Armature & Generator Components

Access high-precision commutators, complete pump armatures, lambda sensors, and sub-assemblies built to strict OE drawings and physical sample matches.

Armature Rotor Hualeao R&D and innovation for carbon commutators

Precision Generator Armature

High-efficiency wound armatures built for continuous industrial generator excitation circuits and micro DC powertrains.

  • Lamination TypeSilicon Steel 0.5mm
  • Temperature ClassClass H (180°C)
View Technical Spec
Commutator Raw material selection for graphite commutators

Planar Carbon Commutator

Flat disc configuration for ultra-compact fuel pumps, significantly reducing axial motor length in high-density engines.

  • Face Flatness≤ 0.003 mm
  • Bonding Strength> 25 MPa
View Technical Spec
Sub-Assembly Customized commutator production and engineering support

EFI Fuel Pump Rotor Core

Pre-balanced pump core sub-assembly ready for immediate motor housing insertion, minimizing Tier-1 assembly bottlenecks.

  • Winding Resistance0.8 – 1.4 Ω
  • Shaft Concentricity≤ 0.005 mm
View Technical Spec
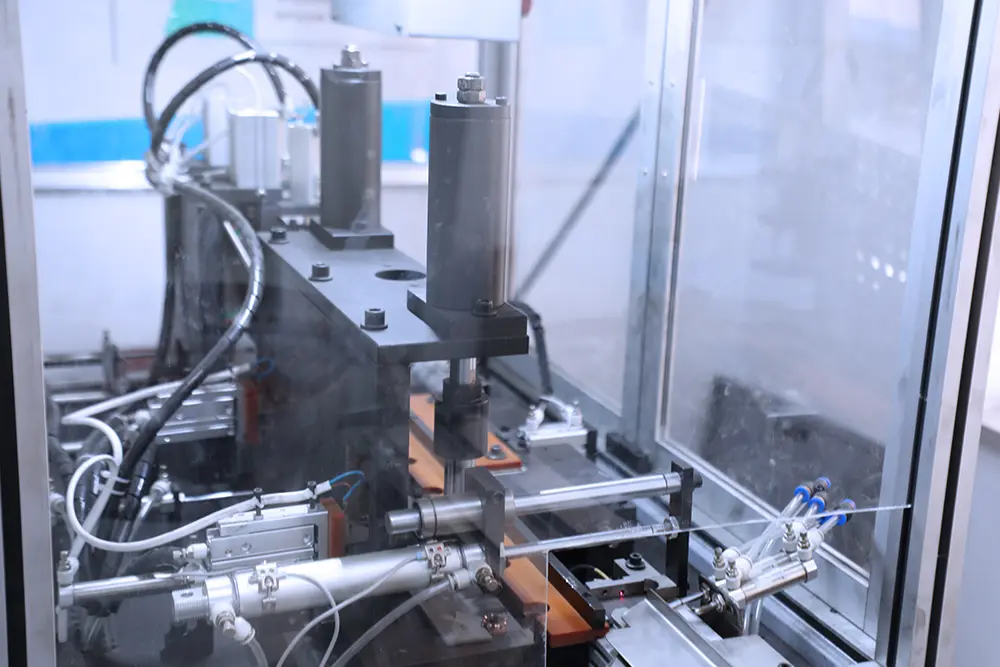
Sensor Tech Quality assurance and inspection of carbon commutators

Planar Exhaust O2 Sensor

Zirconia ceramic feedback sensor for accurate internal combustion air-fuel stoichiometric control and catalyst protection.

  • Heater ElementBuilt-in Ceramic
  • Working Temp350°C – 850°C
View Technical Spec
Heavy Duty Engineering vehicle and construction machinery engine fuel system

Commercial Vehicle Pump

Reinforced high-volume diesel & gasoline lift pump designed for heavy construction vehicles and continuous-duty gensets.

  • Nominal Voltage24V Heavy Duty
  • Continuous Life> 6,000 Hours
View Technical Spec
Marine Grade Marine boat engine fuel system with corrosion-resistant commutator

Marine Generator Commutator

Corrosion-passivated commutator units engineered specifically to pass salt-fog durability tests in coastal power installations.

  • Surface CoatingAnti-Oxidant Passivation
  • Salt Spray TestASTM B117 120h
View Technical Spec
Compact Rotor Motorcycle engine fuel system with miniaturized carbon commutator

Miniature Motorcycle Rotor

High-revving, low-inertia rotor assemblies engineered for sport motorcycles requiring instantaneous throttle response.

  • Max Angular Speed14,000 RPM
  • Inertia Moment≤ 1.2 g·cm²
View Technical Spec
Top Replacement Hualeao commutator production workshop

OE Direct Aftermarket Core

Standardized replacement core assemblies directly matching major European and Japanese fuel pump cross-references.

  • OE Tolerance FitDrop-in Replacement
  • Quality StandardIATF 16949 Verified
View Technical Spec
Sourcing & Engineering FAQ

Frequently Asked Questions: Armature & Commutator Manufacturing

Direct technical and operational answers to the most common queries raised by international purchasing directors and electro-mechanical project leads.

What role does an armature and commutator assembly play in electric generators and fuel pumps?

In electric motors and generators, the armature serves as the primary power-producing component containing insulated wire coils that rotate through a stator magnetic field. The commutator functions as an automatic mechanical rotary switch, continuously reversing current polarity between the rotating windings and stationary brushes. This maintains unidirectional magnetic torque in pump motors or allows continuous direct current extraction in DC generators. Its surface contact flatness, bar-to-bar insulation, and resistance to erosion dictate motor efficiency, current draw, and service longevity.

Why is sintered carbon-graphite superior to copper in modern automotive fuel pump commutators?

Modern commercial fuels commonly incorporate ethanol or methanol blends (E10 up to E85). When conventional copper commutators run fully submerged in these fuels, electric arcing generates accelerated electrolytic corrosion and surface pitting. Additionally, copper against carbon brushes exhibits high friction (μ ≈ 0.30), forming conductive debris that clogs pump bushings. Sintered carbon-graphite commutators are completely chemically inert to alcohol fuels, provide self-lubricating dry sliding (μ ≤ 0.15), eliminate abrasive metal buildup, and triple overall operational lifespan.

Can Hualeao develop customized armatures and commutators directly from 2D/3D customer drawings or OE samples?

Yes. Approximately 45% of our manufacturing volume consists of custom-engineered OEM and aftermarket production runs. Sourcing engineers can submit 2D technical drawings (AutoCAD/PDF with GD&T), 3D STEP/IGES CAD files, or physical worn samples. Our engineering team conducts full reverse engineering, FEA magnetic analysis, and resin-to-metal mold simulation, providing validated DFM (Design for Manufacturability) feedback and prototypes within 10 to 15 working days.

What quality control procedures guarantee zero-defect shipments across large volume orders?

Our Ruian manufacturing facility enforces strict IATF 16949-aligned quality control gates. Every production lot undergoes incoming raw material spectroscopic validation, automated laser dimension verification during diamond cutting, 100% dielectric isolation testing (2,500V bar-to-bar breakdown checks), and 15,000 RPM centrifugal overspeed destruction sampling. Serial Cpk values on critical shaft diameters and commutator runout are maintained ≥ 1.67, with full PPAP Level 3 documentation available upon request.

What are standard production lead times and Minimum Order Quantity (MOQ) thresholds?

For catalog standard parts and high-running aftermarket models, MOQs start from 500 to 1,000 units with standard batch delivery within 20 to 25 calendar days. For fully custom tooling projects, initial sample lots require 15 to 20 days for mold fabrication, followed by PPAP sample signoff and full container dispatch in 30 days. We provide sea freight consolidations via Ningbo/Shanghai ports or expedited air-cargo dispatches for prototype validation.

Direct Factory Collaboration

Consult with Our Precision Armature Engineers

Whether you require replacement carbon commutators for high-alcohol EFI systems or custom-wound generator armatures for industrial equipment, our technical team provides rapid quotes, CAD reviews, and PPAP validation data.

Email Engineering Drawings Download Technical Catalog