High-wear graphite assemblies, dynamic-balanced armatures, and oxygen sensing electronics engineered to meet ISO/TS and IATF 16949 standards.

Formulated with high-density synthetic graphite and deoxidized high-conductivity copper segments to eliminate fuel galvanic corrosion.

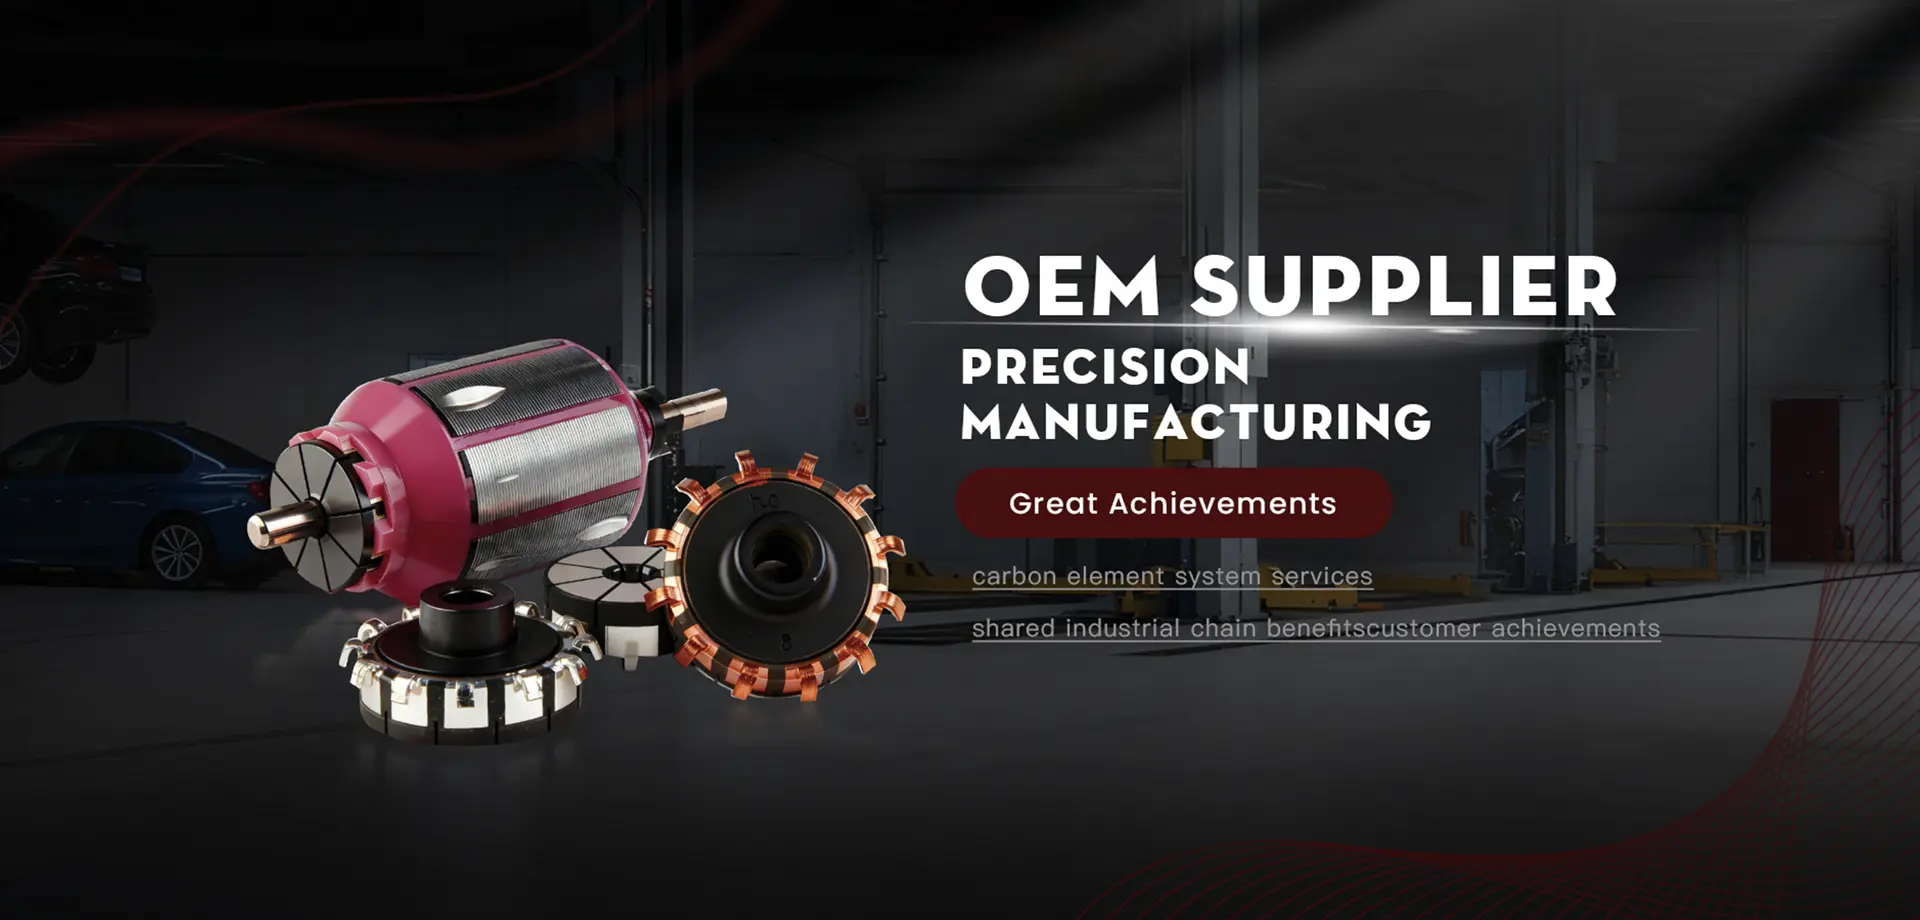
Complete motor armatures featuring automated multi-axis precision winding, class-H resin impregnation, and dynamically balanced shafts.

Zirconia electrolyte sensing element with planar heating technology for ultra-fast light-off and real-time stoichiometric feedback.

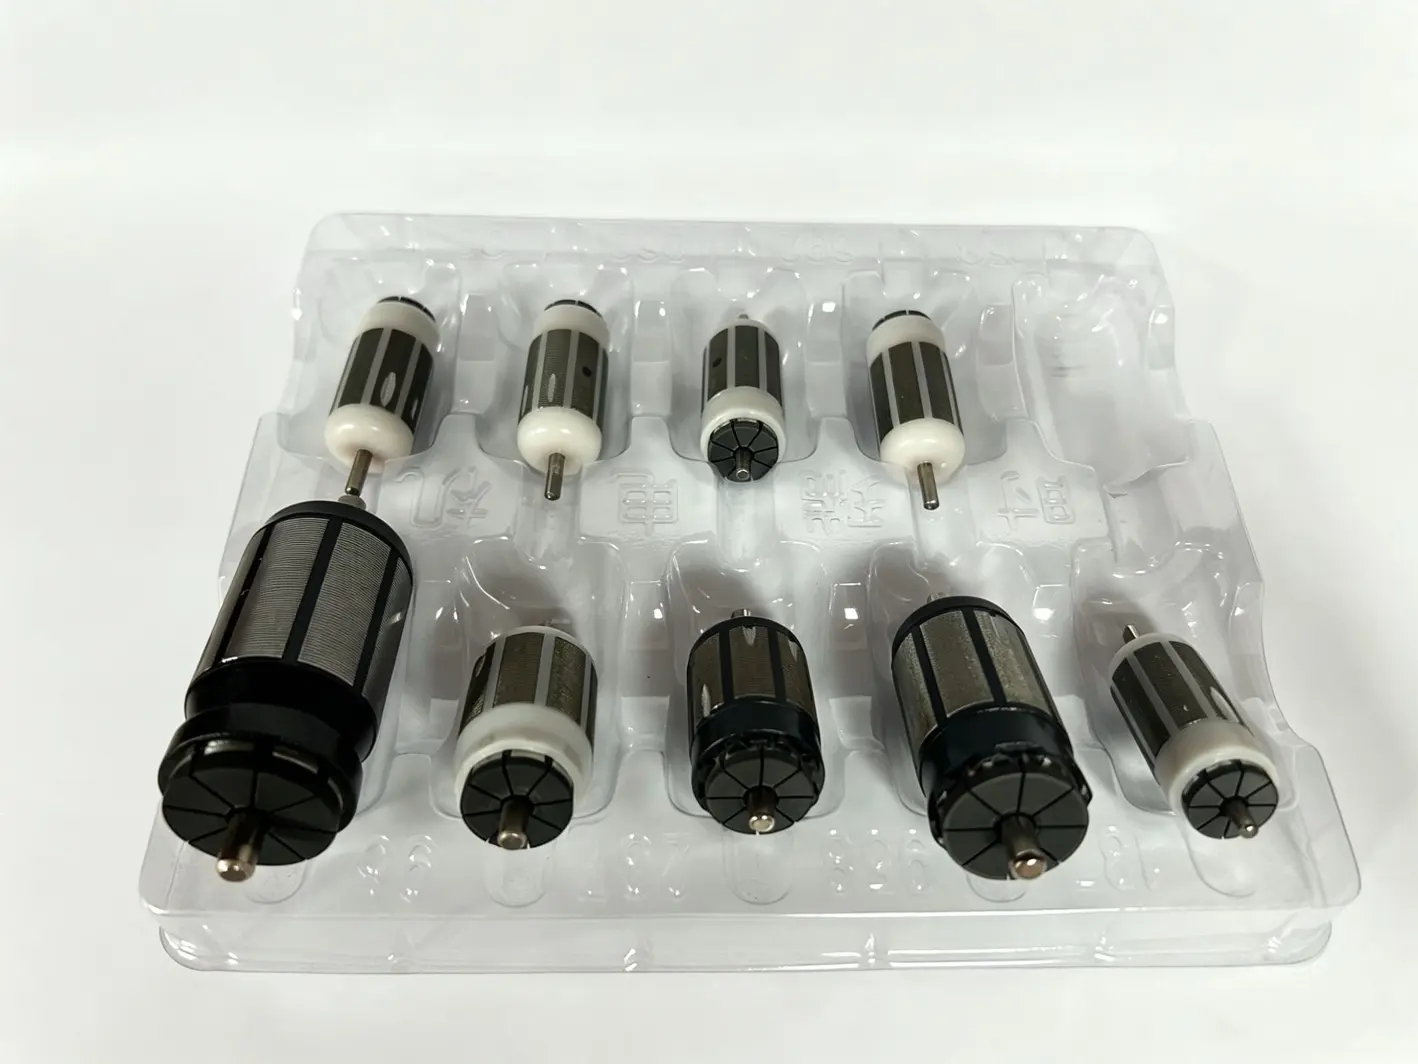
Flagship disc-type commutator engineered for high-pressure multi-port fuel injection (MPI) and direct injection low-pressure feed modules.
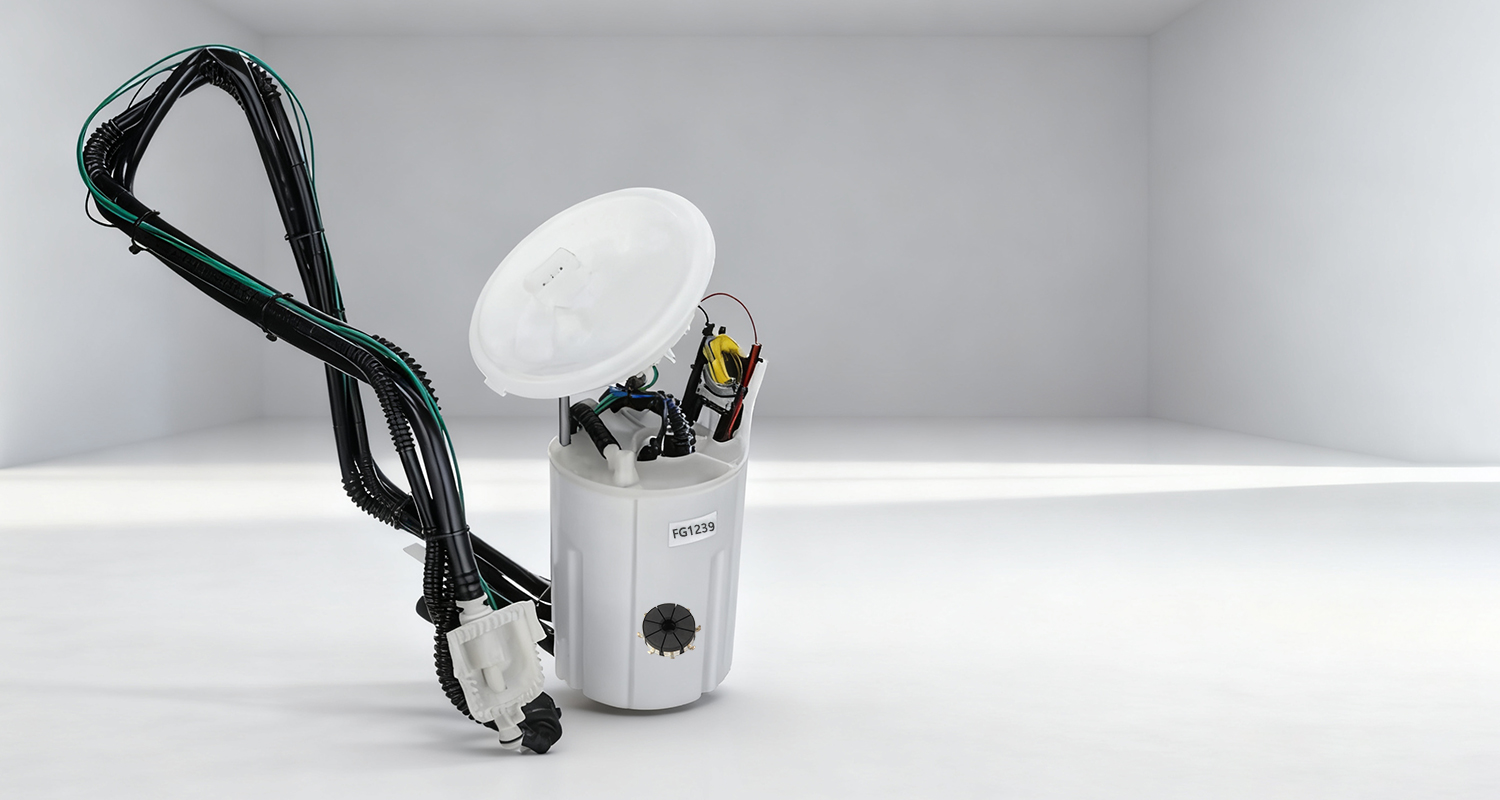
Turbine and roller-cell internal pumping chambers combined with graphite commutation for zero spark erosion in volatile fuel atmospheres.
Molded phenolic glass fiber core matrix offering reinforced dielectric stability and structural rigidity under high-RPM centrifugation.
Vibration-dampened rotor cores featuring oversized copper alloy segments and high-viscosity epoxy encapsulation against continuous shock loads.
Direct build-to-print manufacturing from 2D/3D CAD drawing packages with full metallurgical analysis, custom shaft tooling, and PPAP level 3.
Why conventional metallic commutators fail in alcohol-rich bio-fuels and how China's precision manufacturing clusters are establishing global reliability benchmarks.
Global decarbonization mandates have expanded the adoption of oxygenated fuel mixtures including E10, E85, and neat E100 ethanol, as well as M15/M85 methanol blends. In traditional fuel pump rotors, copper-faced commutators operate directly submerged in these fluids. The combination of electrical micro-arcing and hygroscopic water uptake initiates rapid electrochemical corrosion, leading to pitting, severe spark erosion, brush degradation, and sudden pump failure.
Wenzhou Hualeao integrates specialized carbon-graphite contacts onto the copper commutator substrate. Synthetic graphite exhibits near-infinite chemical inertness toward organic acids, alcoholates, and sulfur contaminants found in low-grade fuels. The self-lubricating microcrystalline carbon film stabilizes interfacial electrical conductivity, mitigating friction-induced thermal spikes and lowering brush-face wear by over 78% compared to bare copper alloys.
Submersible fuel pump rotors operate at rotational velocities exceeding 8,000 to 12,000 RPM inside confined modular baffles. Mechanical vibration caused by dynamic rotor unbalance accelerates commutator segment eccentricity, leading to brush chattering and hydraulic cavitational collapse. Our multi-plane micro-dynamic balancing achieves residual unbalance ratings below 2.0 mg·mm, securing ultra-low acoustic signatures (<38 dB) and over 150,000 operational miles.
| Evaluation Parameter | Legacy Copper Commutator Rotor | Standard Aftermarket Generic | Hualeao Carbon-Graphite Rotor System |
|---|---|---|---|
| Fuel Compatibility | Unleaded gasoline only (E0-E5) | Partial E10 compatibility | Universal E0 - E100, M15 - M85, Biodiesel & Marine fuels |
| Electrochemical Wear Rate | High (severe galvanic pitting in ethanol) | Moderate (copper migration under arc) | Near Zero (graphite passivation layer formation) |
| Segment Radial Runout | ± 0.012 mm | ± 0.008 mm | ≤ 0.003 mm (high-precision diamond turned) |
| Dynamic Residual Balance | ≤ 10 mg·mm | ≤ 6.0 mg·mm | ≤ 2.0 mg·mm (dual-plane active laser balancing) |
| Mean Service Life (Hours) | 1,200 – 1,800 Hours | 2,000 – 2,500 Hours | > 5,000 Hours continuous duty |
| National Energy-Saving Status | Not Listed | Not Listed | Official China 11th Five-Year Energy Conservation Project |
Located in Ruian, Wenzhou—China's capital of automotive electronics—Hualeao combines vertically integrated raw material control with automated production lines.
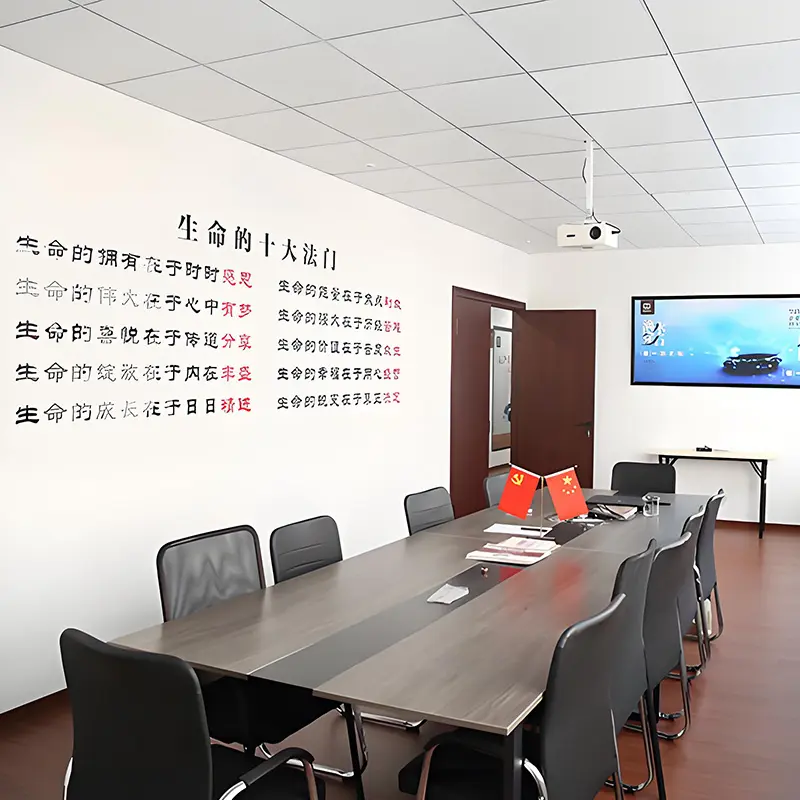
Operating within a modern 6,200 m² production complex, Wenzhou Hualeao leverages the complete Tier-1 supply chain ecosystems of Zhejiang province. From refined CW004A electrolytic copper and ultra-fine synthetic graphite powder to aerospace-grade modified phenolic resins, raw materials are sourced from qualified partners under strict PPAP Level 3 controls.
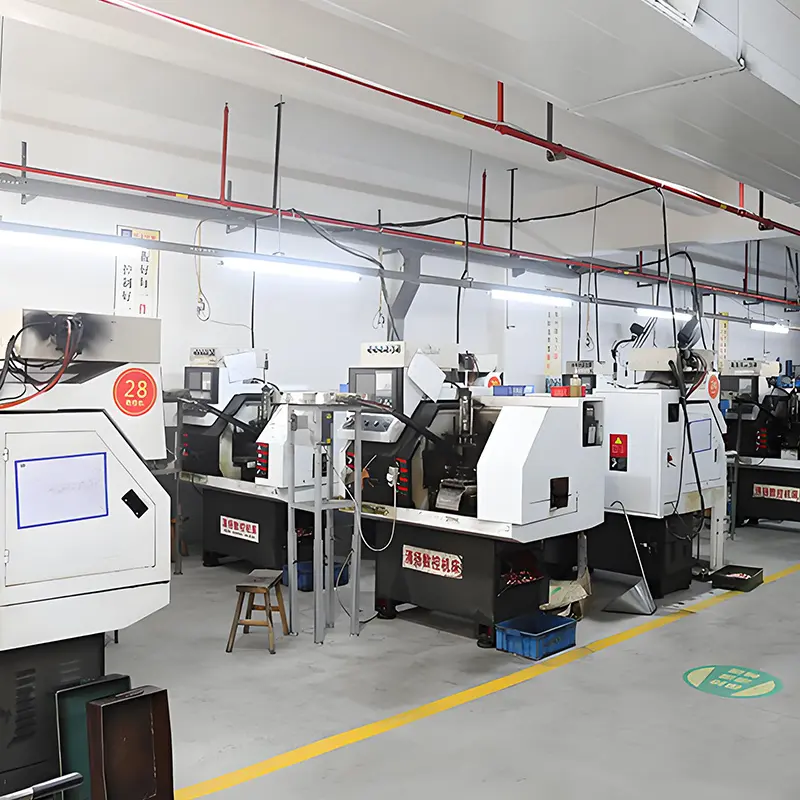
Our plant deploys computerized multi-station cold heading presses, automated carbon disc sintering kilns, high-speed flyer winding machinery, and diamond-tooled CNC segment finishing stations that deliver repeatability across production batches reaching millions of units per annum.
Through joint technical research initiatives with automotive material institutes, Hualeao has aligned commutator chemical, electrical, and mechanical criteria with European and Japanese OEM specifications.

We serve as designated tier suppliers to global fuel pump manufacturers and electronic injection brands across Europe, North America, and South America, delivering drop-in armatures and custom segment patterns.

Continuous academic cooperation with leading engineering institutes allows continuous optimization of the graphite-to-copper intermetallic bonding interface, eliminating delamination under thermal shock.

Automated spectral analysis and continuous SPC lot monitoring ensure consistent density (>1.78 g/cm³), electrical resistivity, and shear strength across 100,000-unit continuous runs.

Our fuel pump carbon commutators were honored under the National Energy Conservation and Emission Reduction framework, proving sustained contribution to micro-motor fuel economy.
From ultra-compact motorcycle fuel modules to high-vibration off-highway mining rigs, our armatures deliver uncompromised pumping flow rates.
Modern internal combustion and PHEV range-extenders require fast fuel rail pressurization during start-stop cycling. Hualeao carbon commutators eliminate start-stop arcing wear, guaranteeing rapid pressure buildup across direct and multi-port injection architectures.
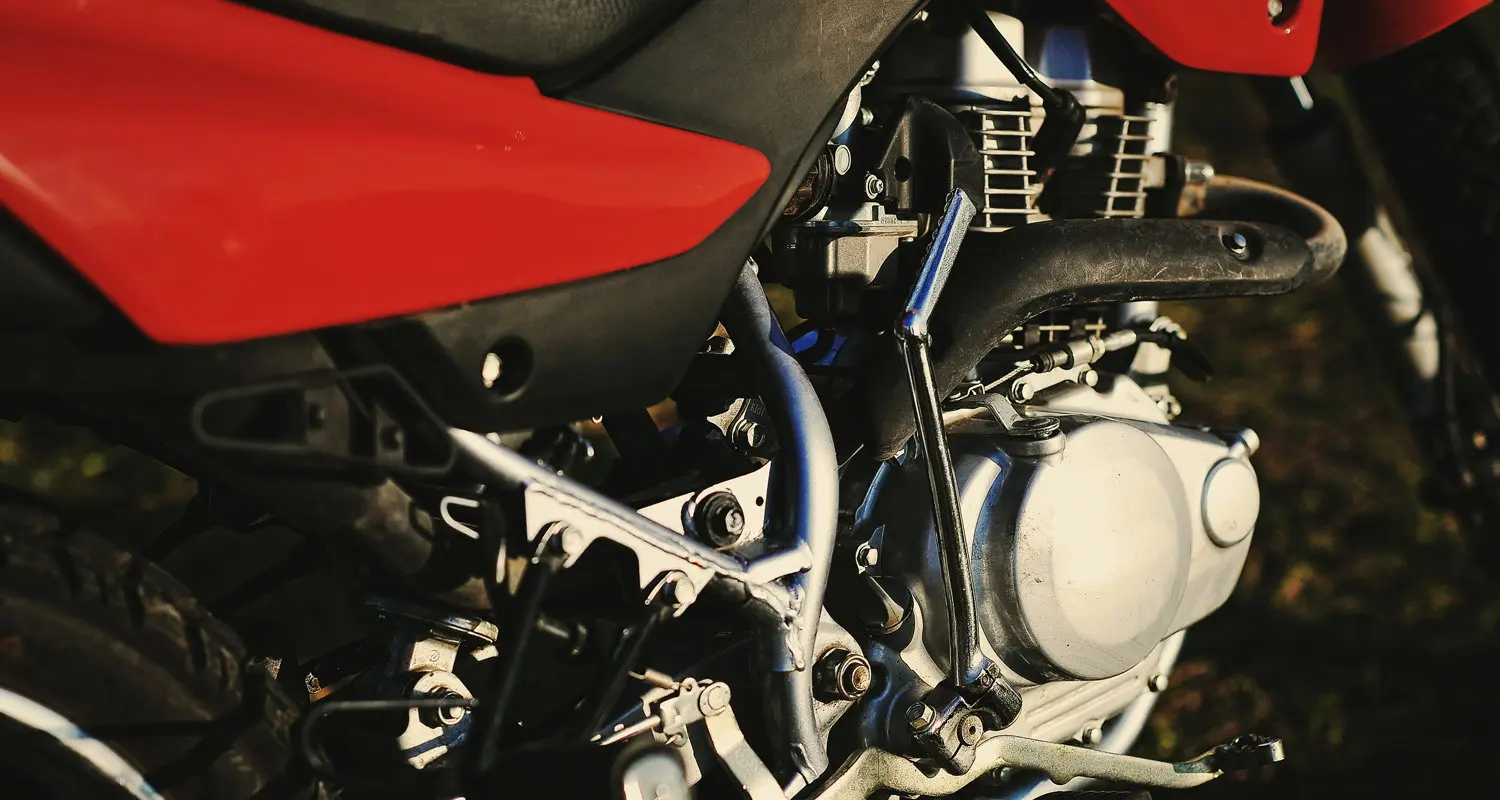
Space-constrained motorcycle fuel tanks expose fuel pump assemblies to elevated ambient fuel temperatures and continuous high-rev centrifugal force. Our miniaturized planar commutators resist high-RPM brush bounce while fitting 30mm pump diameters.
Excavators, wheel loaders, and agricultural tractors operate in severe duty profiles characterized by diesel contamination, high particulates, and non-stop structural vibration. Reinforced resin-molded rotor slots ensure unbroken insulation resistance.
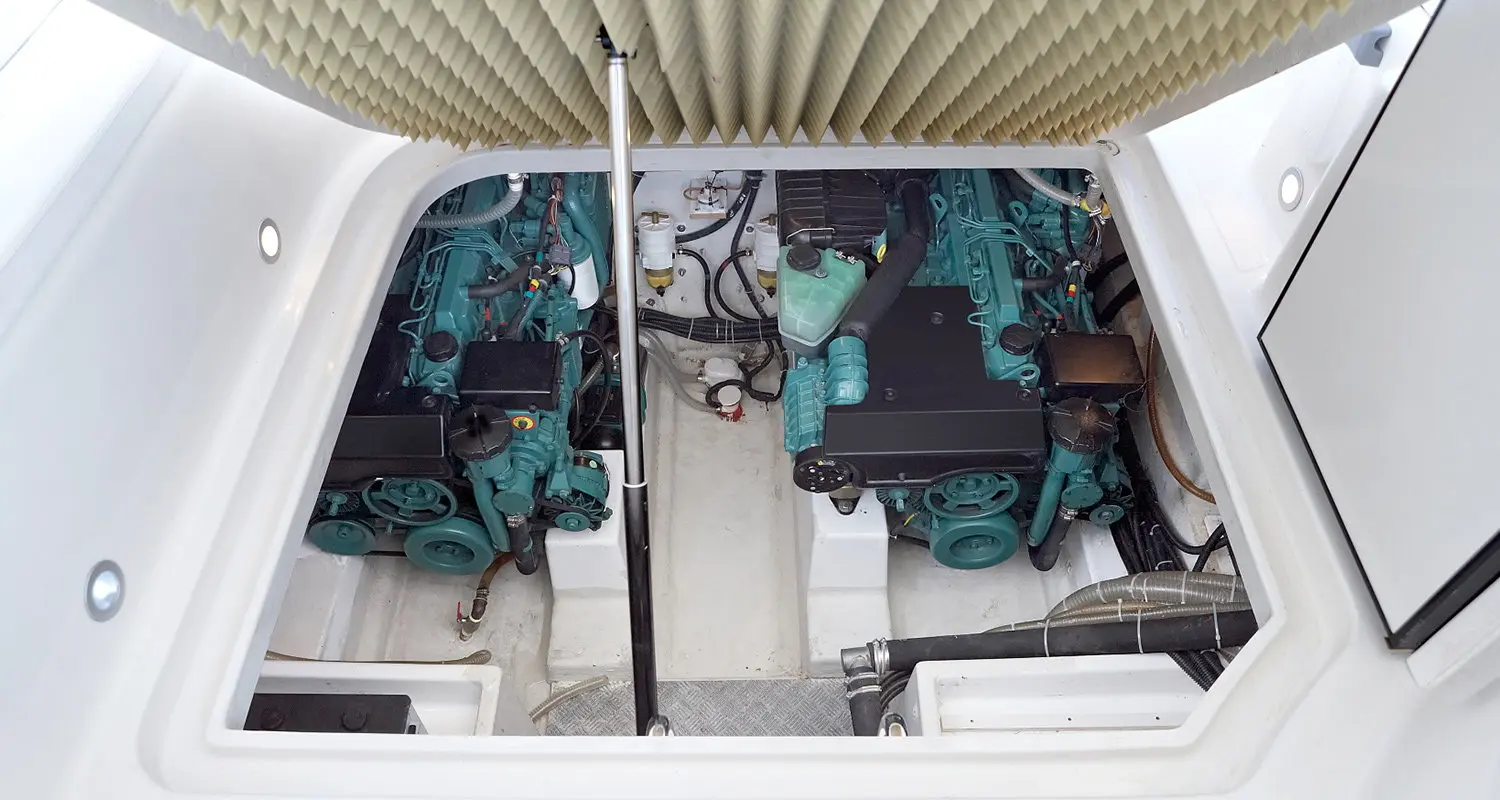
High moisture and airborne marine salt spray accelerate electrochemical decomposition of copper commutators. Hualeao’s salt-spray treated armature shafts and carbon-graphite barriers prevent galvanic coupling inside boat engine fuel tanks.
Every fuel pump rotor and carbon commutator undergoes four distinct stages of strict statistical verification before warehouse release.
Chemical composition verification of incoming copper billets (Cu ≥ 99.95%), graphite density profiling, grain structure analysis, and thermoset resin moisture content checks.
High-speed automated punching, multi-cavity injection encapsulation, diamond turning of contact planes, and tight segment undercut grooving to prevent graphite bridging.
Dual-plane laser balancing removes asymmetric masses on the armature core, achieving micro-gram accuracy to eliminate low-frequency harmonic vibration inside the pump body.
Automated optical sorting monitors runout (≤3μm), inter-bar insulation resistance (>100MΩ at 500V DC), high-voltage surge surge testing, and ethanol immersion endurance tests.
Technical considerations for automotive procurement specialists, pump tier suppliers, and replacement system brand managers when evaluating China rotor suppliers.
Procurement teams must verify that the graphite compound is specifically formulated for immersion in alcohol fuels. Insist on carbon density (>1.75 g/cm³) and resin curing glass transition temperature (Tg > 180°C) to prevent thermal softening during dry-tank startup incidents.
Commutator segments must withstand high electrical impulse without dielectric breakdown. RFQs should mandate 500V to 1500V surge impulse tests across adjacent segments to prevent micro-short circuits caused by copper dust accumulation.
Tier-1 automotive programs require full Production Part Approval Process (PPAP) deliverables: Design FMEA, Process Flow Charts, Control Plans, Gage R&R studies, and full dimensional ballooned prints measured on calibrated Zeiss CMM systems.
Always request 5,000-hour accelerated fuel immersion test data in aggressive test fluids (e.g., FAM-B or ASTM Fuel C mixed with 15% to 85% ethanol). Commutators must exhibit zero segment lifting, zero delamination, and minimal carbon brush wear.
Practical engineering references covering electrical commutation dynamics, exhaust gas lambda sensor feedback, and micro-motor architectures.
An oxygen (lambda) sensor resides in the exhaust manifold, analyzing post-combustion residual oxygen and transmitting closed-loop voltage data to the engine control unit (ECU) to maintain the exact 14.7:1 stoichiometric ratio, protecting the catalytic converter from thermal overload.
Submerged in modern ethanol-rich fuel, traditional copper commutators suffer severe spark wear and chemical oxidation. Graphite commutators transfer electrical current with lower friction coefficients, self-healing transfer films, and robust resistance to galvanic alcoholate attacks.
Acting as an electromechanical rotary switch, the commutator dynamically reverses coil polarity within the armature as it spins through stator magnetic poles. This continuous current switching sustains unidirectional torque, guaranteeing stable pump output pressure.
Clear technical answers addressing fuel chemistry, dimensional tolerances, custom tooling, and supply chain logistics for international buyers.
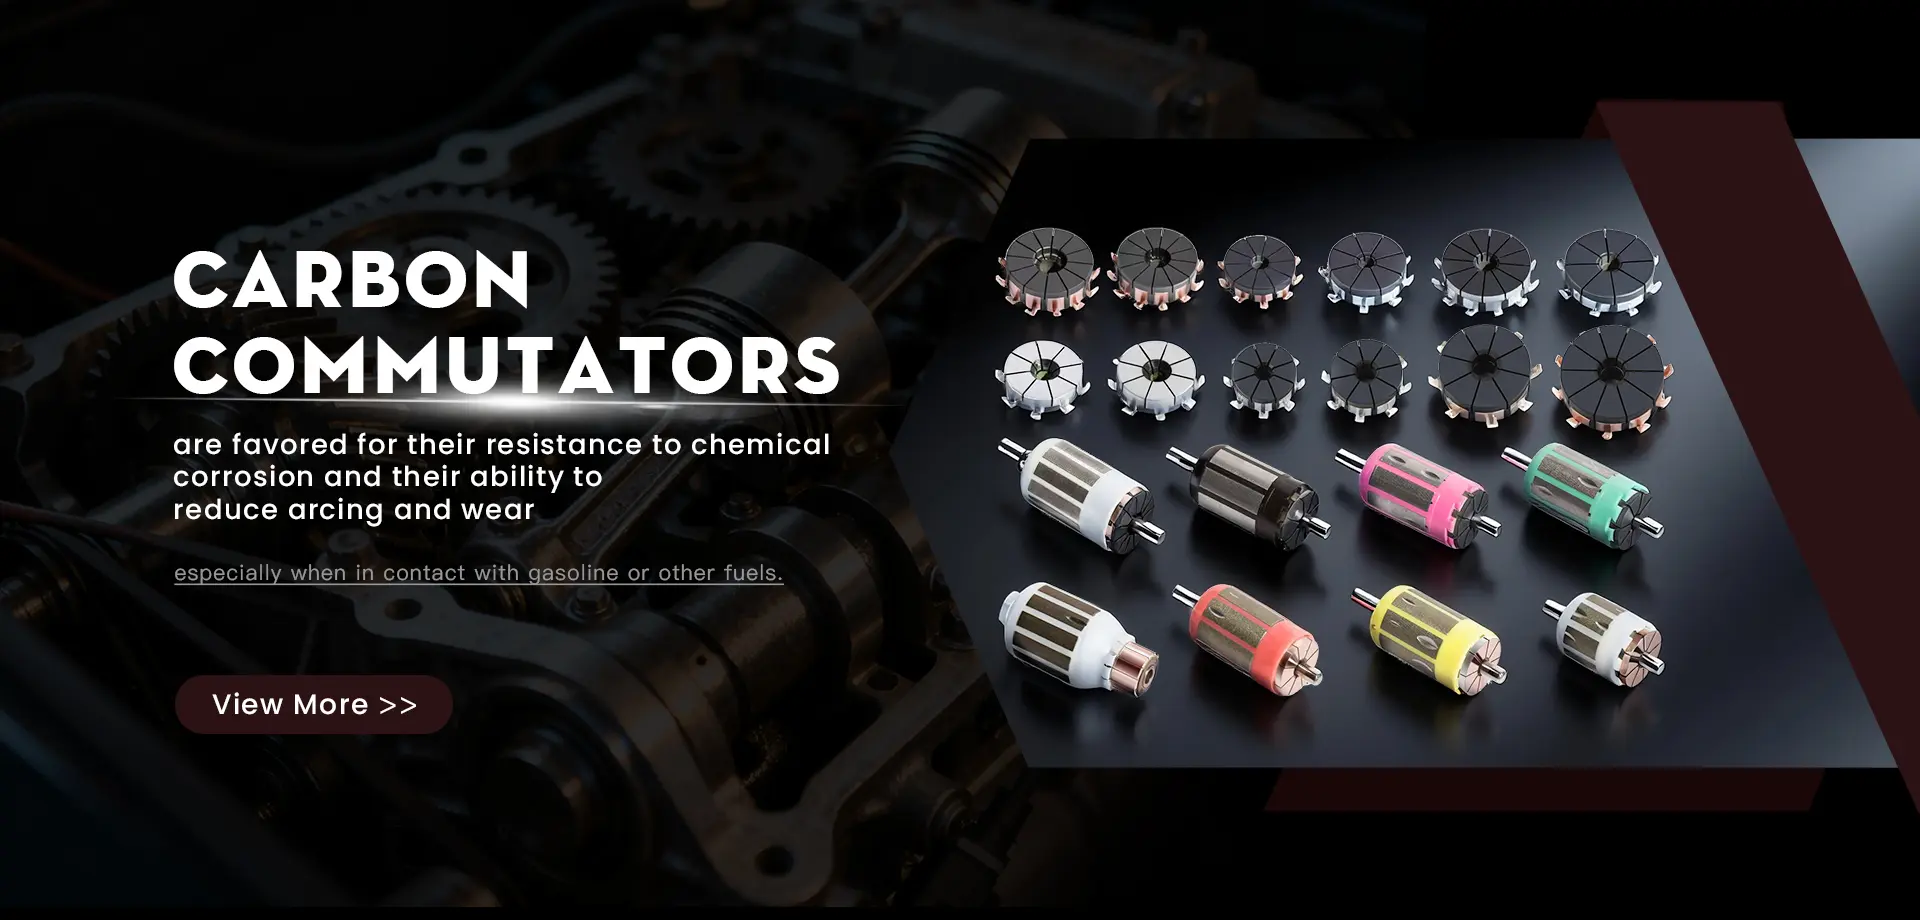
The carbon commutator conducts DC electrical current from stationary brushes to rotating copper wire coils on the motor armature while continuously reversing current flow direction. Because electric fuel pumps are submerged directly inside the fuel tank, the commutator must deliver stable commutation without creating explosive spark levels, corrosive oxidation, or rapid surface degradation.
Submerged fuel pump motors run in fuels containing ethanol, methanol, moisture, and chemical additives. In these environments, copper commutators suffer from rapid electrochemical corrosion, anodic pitting, and catastrophic brush erosion. Carbon (graphite) commutators are chemically inert, resist alcohol fuel degradation, form a self-lubricating interfacial film, and extend pump lifespan to over 5,000 continuous hours.
Yes. Over 65% of our production is customized to client requirements. Send your 2D engineering drawings (PDF/DWG), 3D solid models (STEP/IGES), physical OE sample parts, or reference numbers. Our engineering department handles mold design, copper alloy stamping, carbon sintering tooling, and PPAP validation in 15 to 25 business days.
Our precision components are deployed in automotive passenger cars (gasoline, flex-fuel, hybrid), motorcycle EFI systems, off-highway construction and mining equipment (excavators, loaders), commercial heavy-duty trucks, marine inboard and outboard engines, as well as agricultural tractors worldwide.
We maintain a closed-loop quality system certified to ISO standards. We utilize proprietary thermosetting high-Tg bonding matrices between the graphite face and the copper substrate. Every batch is subjected to high-temperature shear strength testing, thermal shock cycles (-40°C to +140°C), and automated optical CMM dimensional verification to guarantee zero delamination.
Standard catalog items maintain safety stock for prompt dispatch. Custom production runs require an MOQ of 2,000 to 5,000 pieces depending on tooling complexity. Mass production runs are typically completed within 20 to 30 days, with complete export packaging from Ningbo or Shanghai seaports or via air express.
Hualeao has reverse-engineered and benchmarked the technical, metallurgical, and durability standards of leading European and Japanese manufacturers. Our components match foreign OE benchmarks in radial runout (≤0.003mm), dynamic balancing, and chemical stability in E85/M85, while offering the competitive cost structures and agile responsiveness of China’s premier automotive electronics hub.
You can request technical specifications, 2D outline drawings, and cross-reference catalogs directly by visiting our Request a Catalog page or emailing [email protected]. Our engineering team responds within 24 business hours with comprehensive PDF spec sheets and compatible CAD files.
Select individual component categories below for technical documentation, engineering cross-references, and direct factory procurement.
Designed for multi-fuel compatibility, high transmission accuracy, and low electrical noise in high-RPM submersible pumps.
Complete fuel pumps and modular pump cores engineered with dynamic balancing for low acoustic emissions.
Direct-fit zirconia lambda sensors designed to optimize combustion stoichiometry and reduce hydrocarbon tailpipe emissions.
Our most in-demand rotor cores and commutators, benchmarked to match standard OEM references across Asian and European platforms.
Wound armatures featuring copper segment terminations, precision-slotted laminations, and rust-inhibiting shaft coatings.
Axial contact face commutators optimized for compact fuel modules requiring minimum motor length and low brush friction.
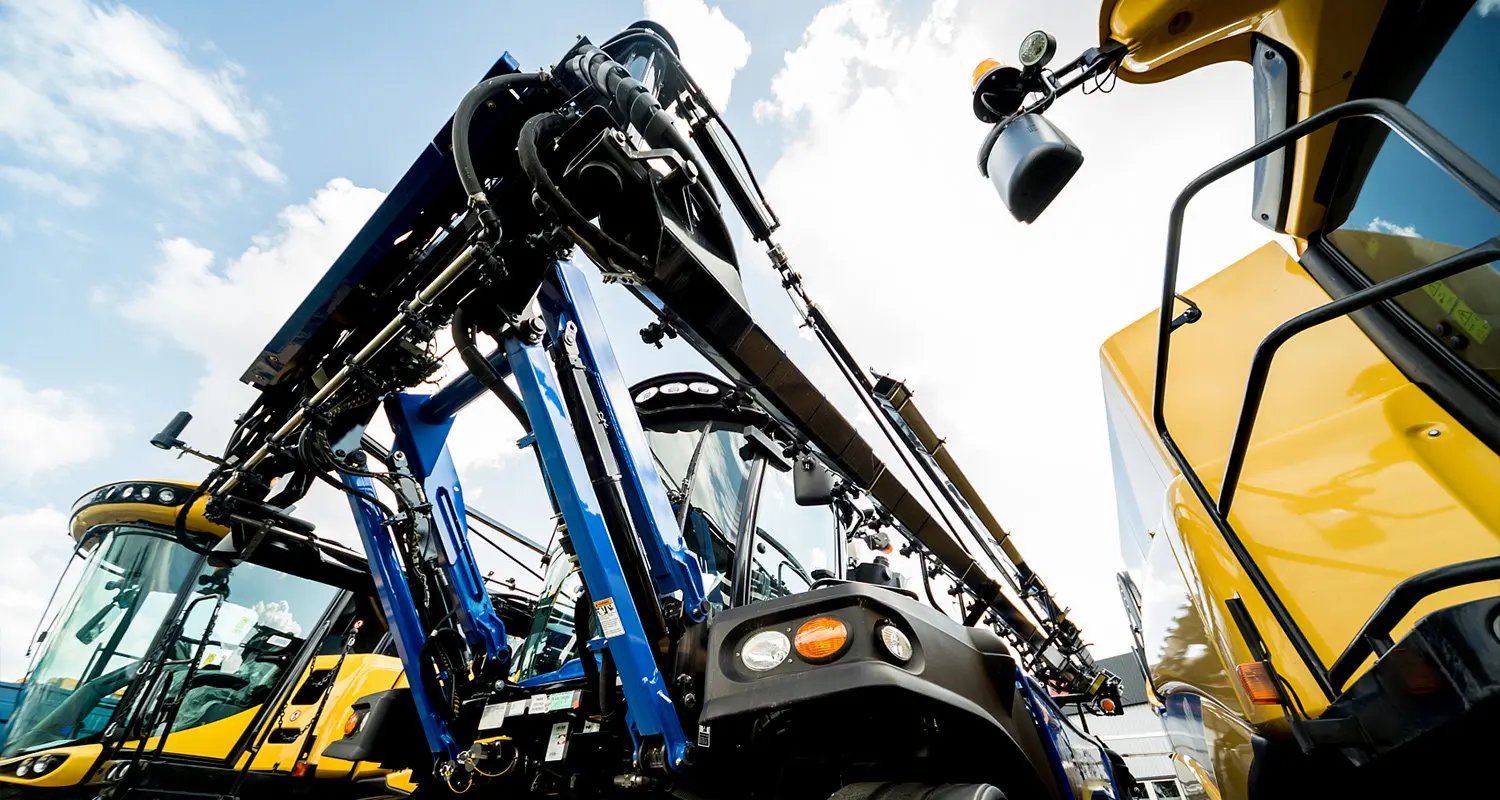
Heavy-duty armatures and graphite discs engineered to withstand diesel particulate contaminants, high heat, and shock vibrations.
Accelerate your new fuel pump development program with dedicated prototyping, material testing, and rapid mold fabrication.
Whether you require CAD drawings, sample validation units, custom segment mold creation, or factory audit schedules in Wenzhou, our team delivers complete technical proposals within 24 hours.