Explore our core engineering catalog engineered for tier-1 automotive EFI assemblies, flex-fuel systems (FFVs), and corrosive alcohol-blend duty cycles.

Engineered carbon-graphite contact surfaces designed to eliminate electrochemical erosion under E85 and high-methanol environments.
Explore Commutator Details →
High-reliability submerged DC pump units featuring dynamically balanced armatures and fuel-resistant composite housings.
View Electric Pump Models →
High-accuracy stoichiometric sensing ensuring closed-loop ECU fuel mapping optimization for gasoline-ethanol flexible combustion.
Examine Sensor Specs →
Industry-standard high-volume OEM replacement commutator verified under rigorous continuous alcohol immersion endurance standards.
Source Model HC-QZQE-049C →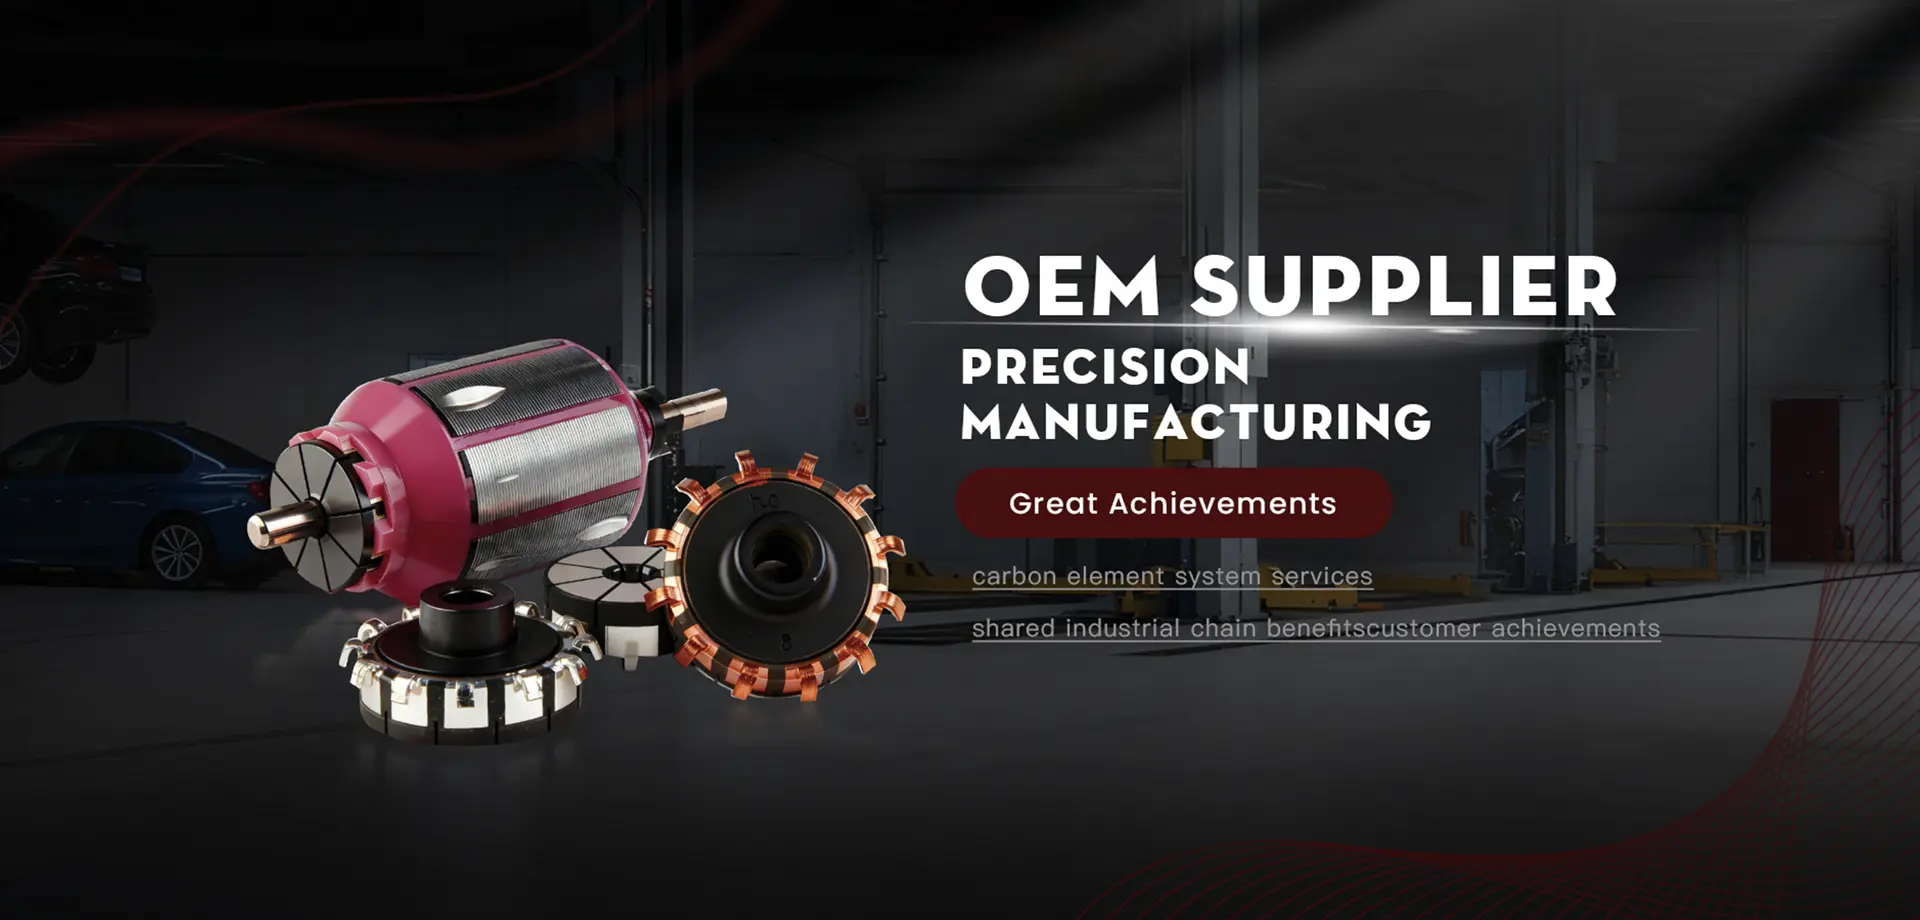
Balanced micro-motor rotor assemblies equipped with pre-soldered carbon commutators for high-pressure multi-port injection.
Armature Technical Data →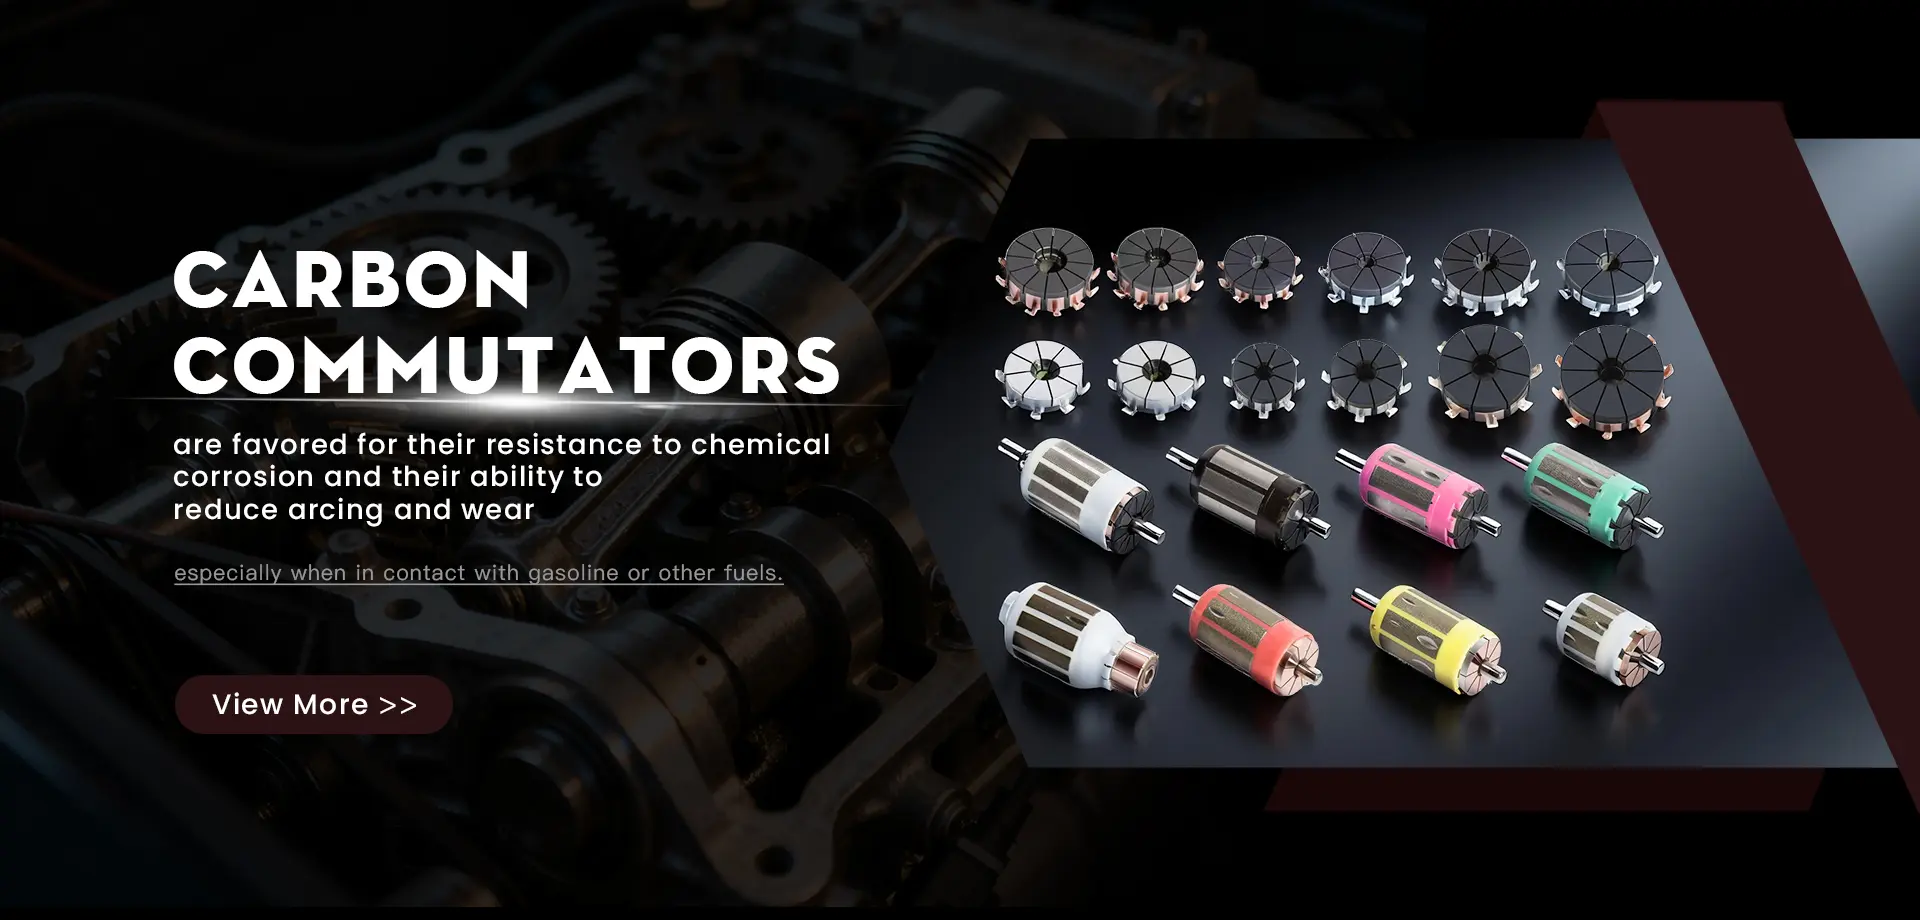
Ultra-compact axial disc commutators engineered for space-constrained fuel pump modules with flat commutator faces.
Request Disc CAD Drawings →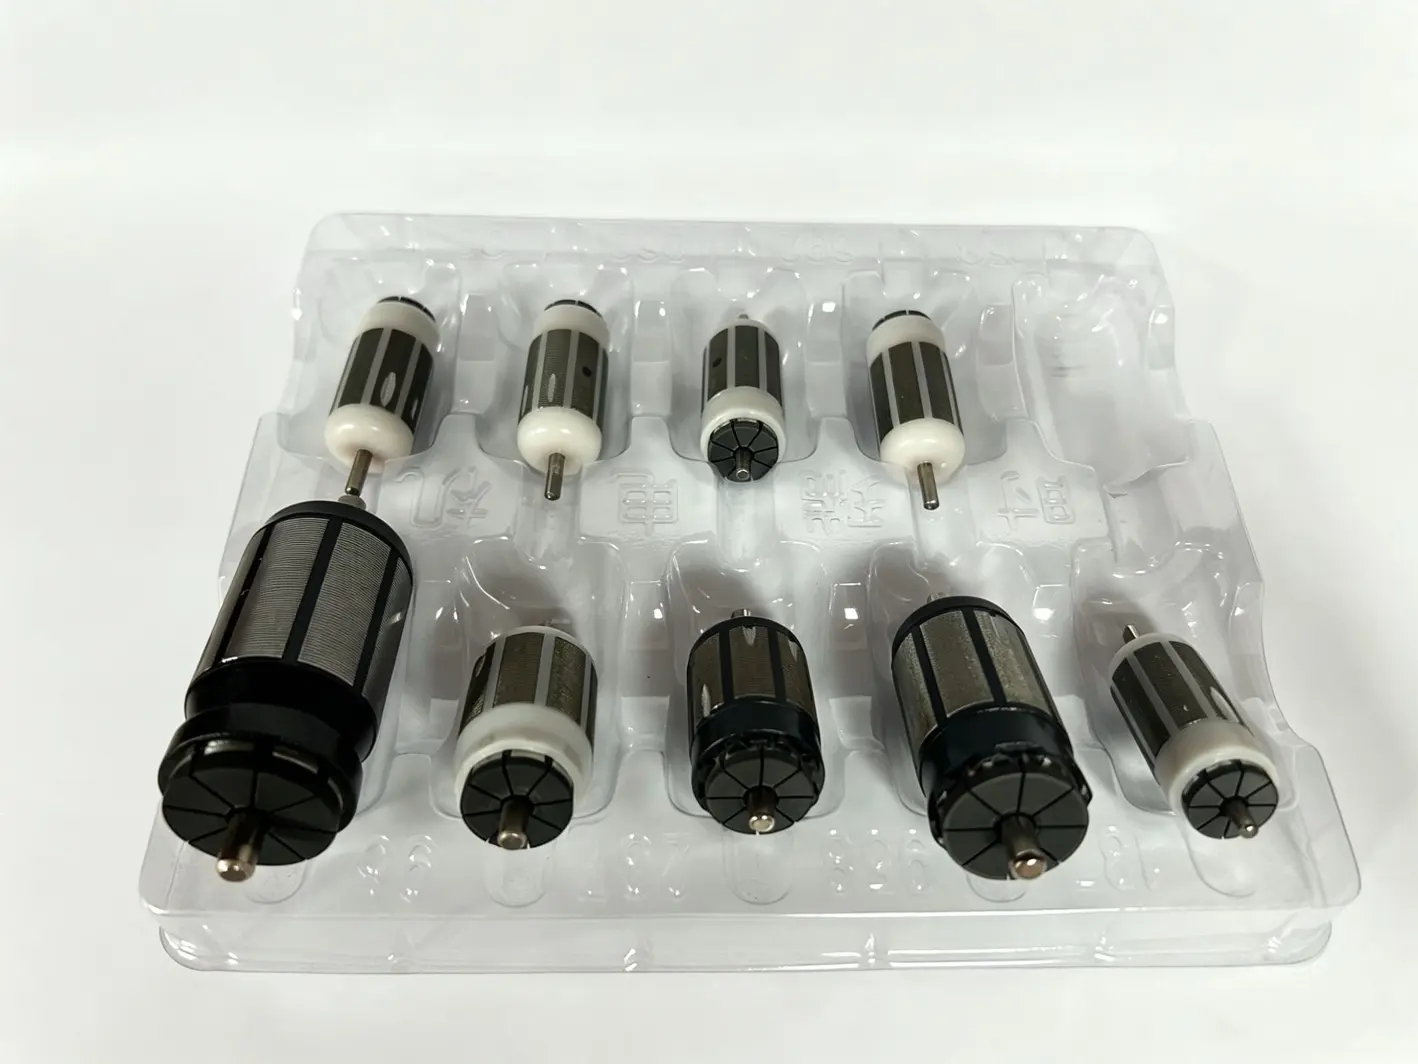
Specially formulated carbon-copper interface delivering micro-arc resistance and zero delamination during dry-run fuel starvation.
Review Metallurgical Data →
Dedicated co-development program matching custom segment numbers, copper tang styles, and OD/ID specifications to your blueprint.
Submit OEM Engineering Blueprint →Analyzing the electrochemical tribology, material migration, and market drivers shifting international fuel delivery architectures from conventional copper to specialized carbon-graphite.
With environmental directives such as the European Union RED II/III, the United States Renewable Fuel Standard (RFS), and aggressive E20 blending rollouts in India and E27–E100 flex-fuel adoption across South America, global automotive powertrains are processing increasingly aggressive alcohol fractions. Submerged DC electric fuel pumps that operated trouble-free on non-polar hydrocarbon gasoline face immediate operational challenges when exposed to polar bioethanol, biomethanol, and renewable bio-diesels.
Standard DC brushed fuel pumps submerge the entire motor—including armature, brushes, and commutator—directly inside the pressurized fuel reservoir to ensure continuous thermal cooling. However, alcohols exhibit higher dielectric constants, elevated ionic conductivity, and the propensity to harbor acetic acid and water condensates. In traditional copper commutators, this triggers intense anodic dissolution, galvanic corrosion across copper segments, rapid spark pitting, and premature motor lockup.
By migrating from bare copper segments to advanced carbon-graphite composite running surfaces mechanically interlocked with copper substrates, the chemical vulnerability is eliminated. Carbon exhibits electrochemical passivity in alcohol media, preventing ionic migration and galvanic pitting. Furthermore, graphitic carbon provides natural self-lubricating boundary films, counteracting the inherently poor tribological lubricity of pure ethanol and methanol.
| Performance Metric / Test Parameter | Standard Copper Commutators | Hualeao Carbon-Graphite Biofuel Commutator | Engineering Impact & Strategic Value |
|---|---|---|---|
| Ethanol / Methanol Compatibility | Prone to severe galvanic oxidation (E10 max limit) | Complete resistance across E10–E100 & M15–M85 | Eliminates warranty risks and fuel-related field pump failures. |
| Operating Life in Biofuel Immersion | Approx. 300 to 600 hours before critical segment erosion | Exceeds 3,000 to 5,000+ continuous hours | Meets and surpasses Tier-1 automotive 150,000-mile lifecycle targets. |
| Electrical Spark / Arcing Energy | High arc energy leading to rapid segment pitting | Suppressed contact sparking via graphitic transition layer | Lower high-frequency EMI noise; prevents vapor ignition risks. |
| Dimensional Swelling under Alcohol Exposure | Copper stable, but plastic base prone to delamination | Hydrolytically stabilized phenolic resin (<0.05% expansion) | Maintains segment planarity and high rotational dynamic balance. |
| Cost vs. Performance Index | Low initial cost; unacceptable failure rate in FFVs | Import-grade durability at competitive Chinese manufacturing parity | Direct drop-in replacement for high-cost Western & Japanese brands. |
Purchasing managers, fuel system lead architects, and aftermarket distributors face tightening regulatory constraints and supplier consolidation.
Global fleet data consistently demonstrates that introducing low-cost aftermarket fuel pumps into E20 or flex-fuel territories results in catastrophic warranty spikes within 6 to 12 months. Commutator segment erosion directly leads to brush shorting and complete armature seizure, damaging brand equity for tier-1 suppliers and replacement distributors.
Wenzhou Hualeao Automotive Parts Co., Ltd. addresses this directly through accelerated immersion testing protocols in accordance with SAE J1681 standards. Our commutators undergo long-term soaking and continuous dynamic testing in surrogate alcohol formulations containing aggressive corrosive species, ensuring that batch integrity is guaranteed before dispatch.
Relying on single-source multinational commutator providers often brings extended lead times, restrictive MOQs, and inflated pricing structures. Operating from our dedicated 6,200 m² advanced facility in Ruian, Wenzhou, Hualeao offers scalable manufacturing capacity that provides tier-1 pump assemblers with supply resilience, custom tooling agility, and stable unit economics.
A closed-loop technical framework combining high-temperature solid-state diffusion, phenolic molding stabilization, and micro-precision surface finishing.
The primary point of failure in composite commutators is the mechanical and electrical interface between the outer carbon ring and the internal copper lead segments. Hualeao utilizes a proprietary dovetail interlocking geometry combined with high-pressure hot isostatic sintering. This eliminates micro-voids, prevents fuel ingress at the bond line, and maintains shear resistance under centrifugal forces exceeding 25,000 RPM.
Commutator insulating cores operate continuously submerged in high-temperature fuel baths (up to 70°C). Ordinary thermosetting resins absorb alcohol molecules, leading to volumetric swelling, core softening, and commutator segment shorting. Our engineering process incorporates glass-fiber reinforced, alcoholysis-resistant phenolic resins that exhibit virtually zero volumetric deformation and retain dielectric isolation over decades.
Segment isolation requires micrometer-level precision. Our automated production line utilizes CNC diamond fly-cutting and micro-slitting techniques to achieve ultra-narrow commutator bar spacing without carbon residue bridging. The running surface is polished to a mirror finish (Ra ≤ 0.2 μm), minimizing initial brush wear and promoting immediate formation of a stable, low-friction transfer film.
Automotive ECUs and digital dashboard clusters are vulnerable to high-frequency brush-commutator RF noise. The high electrical resistivity of carbon segments compared to pure copper dampens inductive current spikes during commutation polarity switching. This natural spark quenching capability significantly lowers brush operating temperature and reduces EMI emissions to easily clear CISPR 25 Class 5 automotive thresholds.
Combining independent intellectual property, university research alliances, and automated manufacturing from China's premier automotive components corridor.
Our EFI carbon commutator was recognized as a designated new-vehicle energy conservation and emission reduction project under China's 11th Five-Year Plan, solidifying our engineering leadership in powertrain efficiency.
Production processes, material densities, bonding matrices, and electrical contact resistance parameters have been systematically benchmarked to meet or exceed imported German and Japanese tier-1 brand standards.
Continuous strategic collaboration with leading scientific research institutes and university engineering departments drives ongoing innovation in carbon matrix formulations and advanced alcoholysis barrier resins.
Every commutator batch undergoes strict four-stage qualification: raw material spectrometry, in-line vision inspection, automated dimensional laser gauging, and post-assembly electrical dielectric breakdown verification.
Providing specialized mechanical commutation solutions across passenger cars, commercial transport, off-highway machinery, and marine vessels.
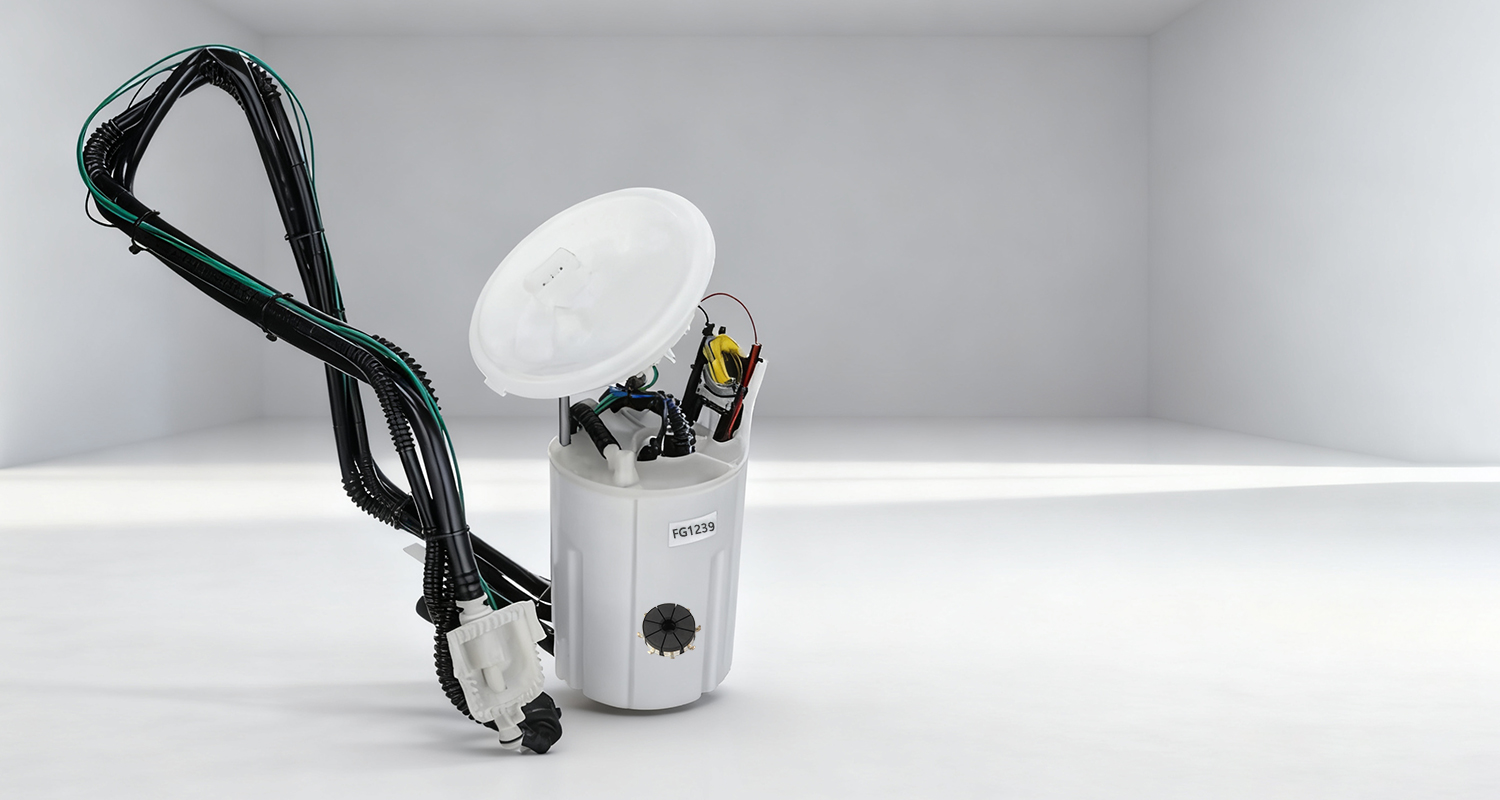
Submerged fuel pump armatures running continuously in flex-fuel tanks with ethanol concentrations fluctuating dynamically from E10 to pure E100 hydrous ethanol.
Miniaturized, low-inertia carbon commutators capable of handling extreme vibration, rapid RPM spikes (up to 14,000 RPM pump speed), and limited thermal packaging.
Severe-duty fuel delivery units handling low-grade biodiesel blends, heavy dust, continuous full-throttle vibrations, and high ambient temperature profiles.
Specially sealed and surface-passivated commutators engineered to withstand humid salt-spray atmospheres and water-entrained maritime alternative fuel tanks.
How Hualeao aligns with global compliance directives and engineers future-ready commutator architectures for the next generation of alternative fuels.
Our production protocols are aligned with IATF 16949 quality standards, ensuring stringent lot traceabilities. Commutator raw materials strictly comply with EU RoHS and REACH regulations (SVHC-free), eliminating heavy metal hazards while meeting clean emission standards worldwide.
While brushless (BLDC) motors dominate external drives, brushed DC motors with carbon commutators remain the dominant, safest, and most cost-effective choice inside volatile biofuel tanks. They eliminate complex in-tank drive electronics and micro-arc ignition risks, delivering bulletproof reliability at significantly lower total system cost.
Our forward R&D is developing graphene-doped carbon formulations for ultra-low resistance and self-healing boundary layers in synthetic e-fuels, biomethanol, and SAF transfer systems. We are also expanding planar disc commutators for next-generation brushless hybrid staging pumps.
In-depth engineering answers to the most common questions raised by procurement managers, automotive electrical architects, and pump rebuilders.
Explore our additional production lines for direct OEM integration, high-performance aftermarket rebuilds, and custom armature engineering programs.
Multi-hook copper terminal structure with sintered graphite contact surface for universal automotive fuel pump rewinding and OEM armatures.
Get Segment Specifications →
Automated manufacturing offering superior repeatability, tightly controlled runout (≤0.003 mm), and rapid dispatch for tier-1 supply chains.
Request Production Quote →
Engineered for high-flow turbo and direct injection secondary systems, resistant to high ethanol swelling and vapor lock issues.
View Flow Rate Curves →
Zirconia ceramic sensing element engineered to resist fuel additive contamination and alcohol combustion exhaust byproducts.
Explore Sensor Catalog →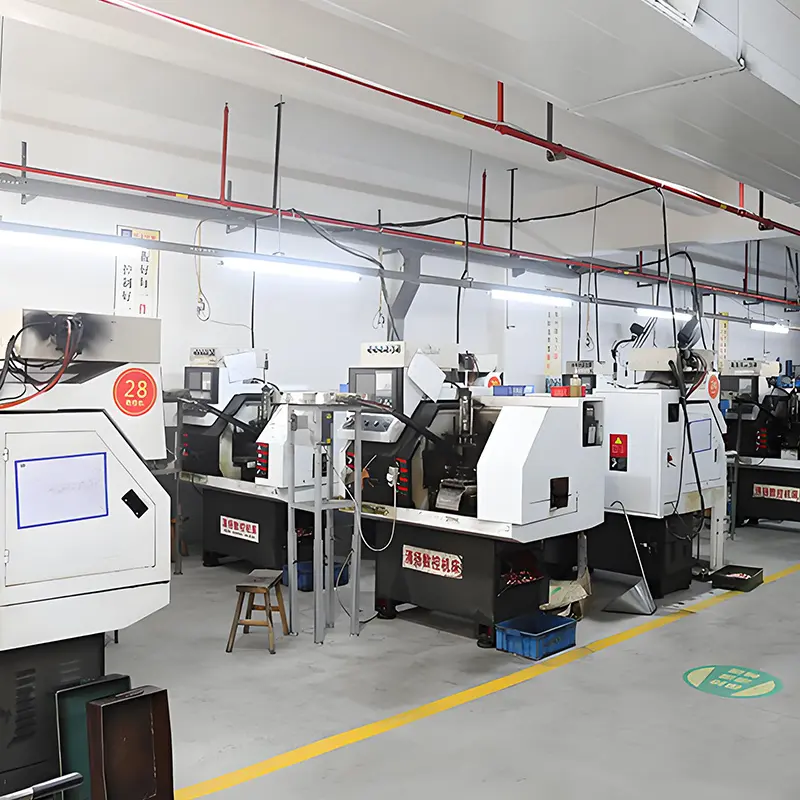
Custom mold design service delivering tight concentricity tolerances on commutator copper shells, hooks, and carbon segment assemblies.
Consult Tooling Engineers →
100% computerized optical measurement and micro-resistance sorting for safety-critical automotive powertrain electric pumps.
Read Inspection Whitepapers →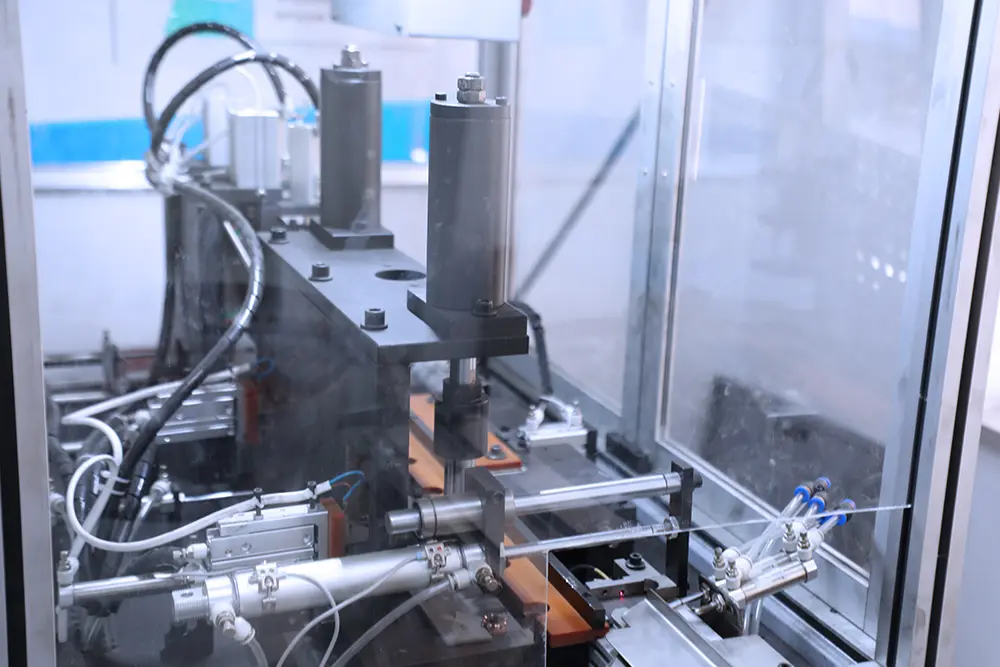
Fine-grain graphite material featuring controlled porosity and optimized electrical resistivity tailored for alcohol-submerged motors.
Search Commutator Grades →
Integrated rotor assemblies including carbon commutator, precision-wound copper armature, and dynamic balancing for direct housing assembly.
Download Assembly Blueprint →
Equipped with a 6,200 m² modern manufacturing infrastructure in Ruian, Wenzhou, and staffed by over 50 skilled professionals and engineers, Hualeao is dedicated to solving electrochemical corrosion challenges in alternative fuel motor systems. We supply trusted tier-1 automotive suppliers, EFI pump manufacturers, and worldwide aftermarket distributors.