IATF 16949 Engineering Standard · Industrial Whitepaper

China Electric Brake Pump Suppliers & Manufacturers

Authoritative OEM & Tier-1 whitepaper analyzing electric vacuum brake boosters, electro-hydraulic brake (EHB) systems, high-durability carbon commutators, and electronic fuel delivery solutions engineered in Ruian, Wenzhou, China.

Precision Engineering Catalog

High-Performance Electric Pumps & Subsystem Assemblies

Explore our premier portfolio of automotive electric brake pump components, alcohol-resistant graphite commutators, electronic fuel injection (EFI) fuel pumps, and lambda sensors engineered for global aftermarket distributors and Tier-1 integrators.

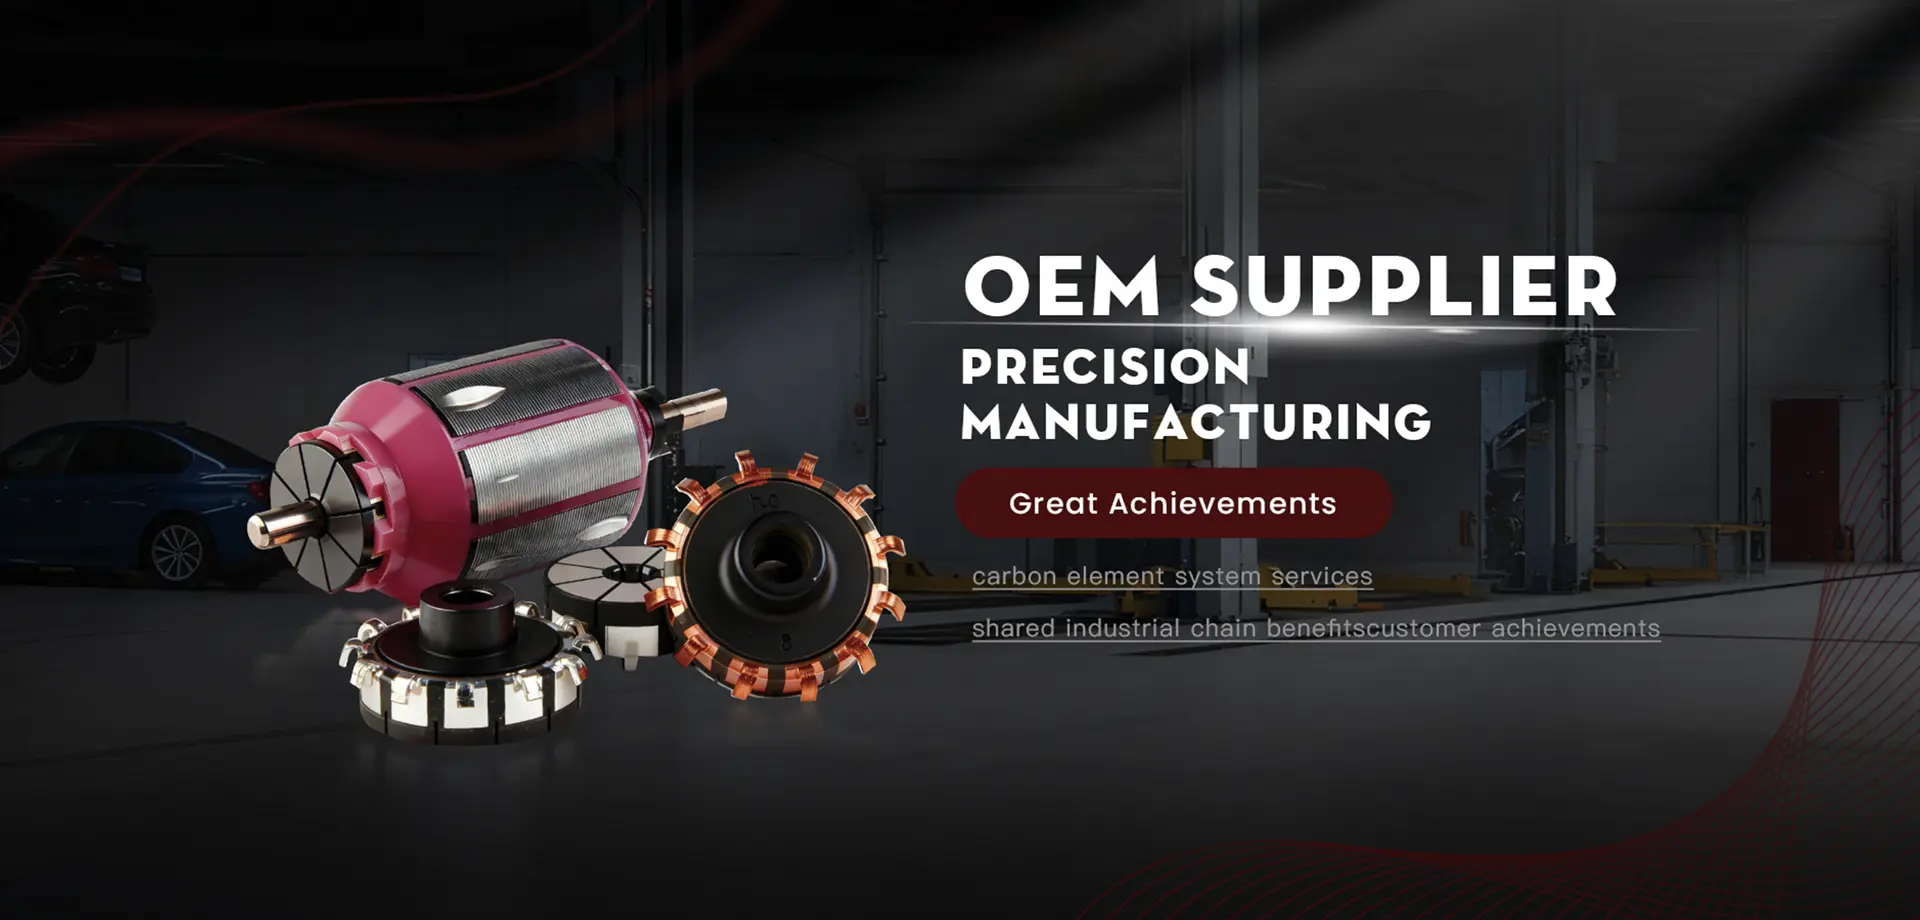
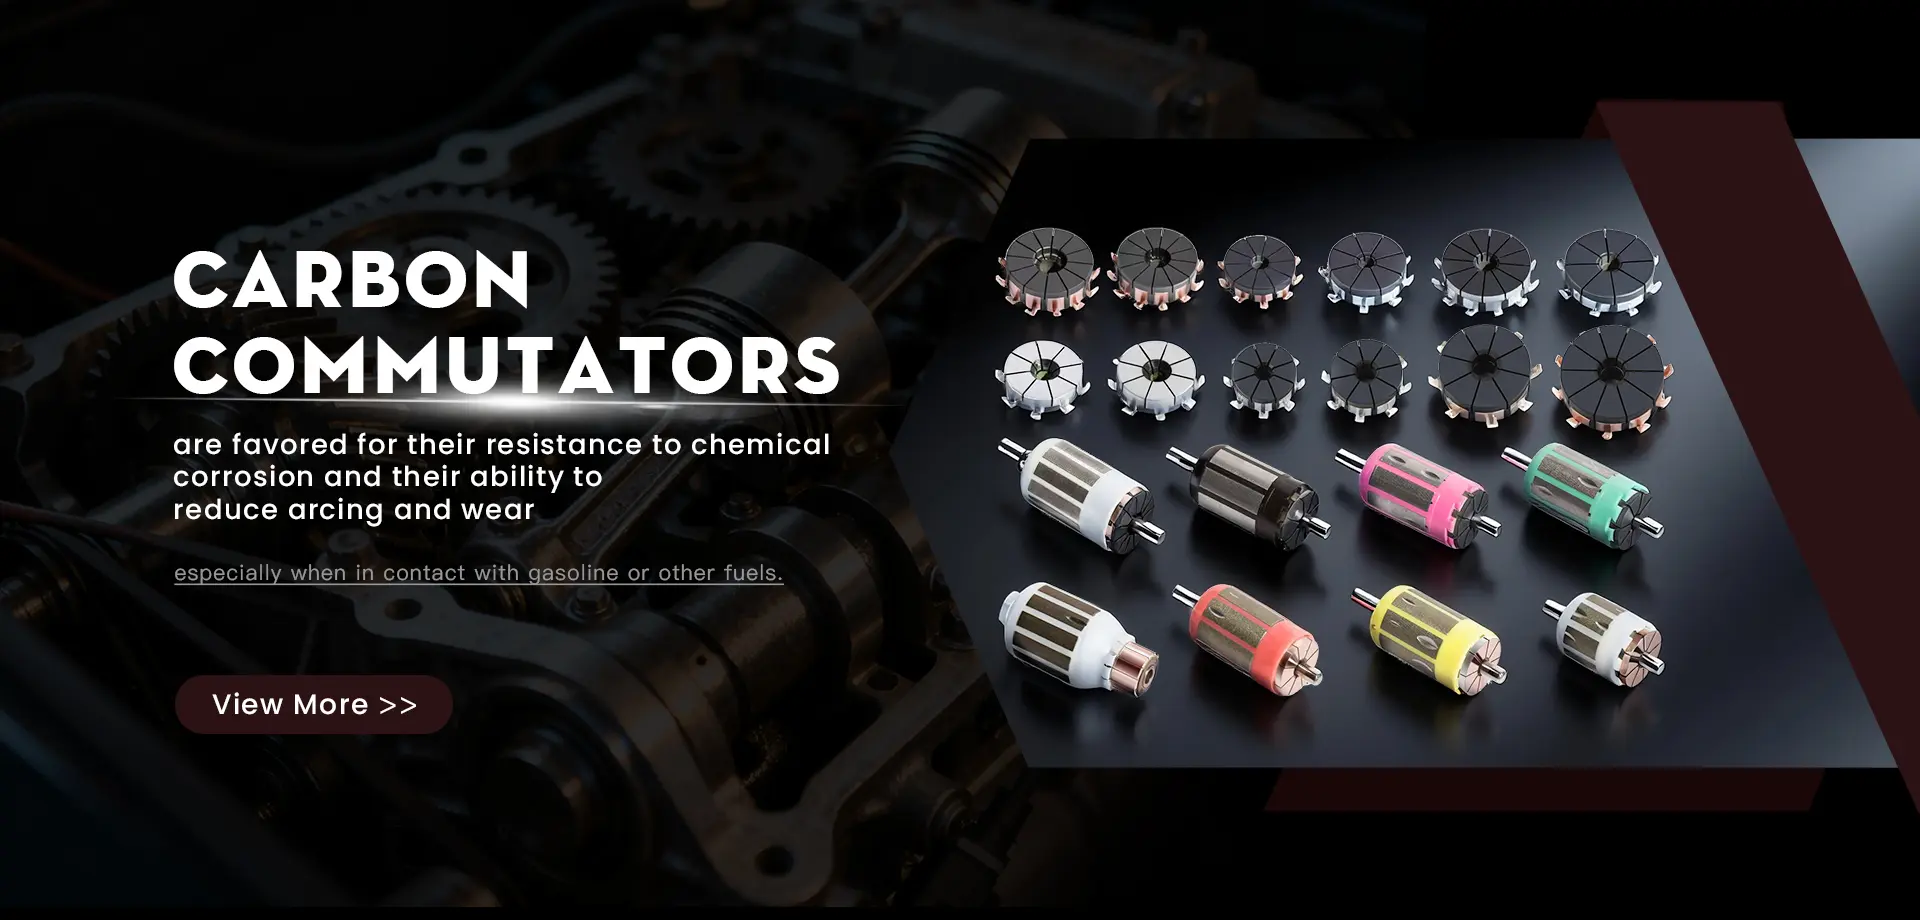
Core Component Carbon graphite commutator for automotive pump armatures

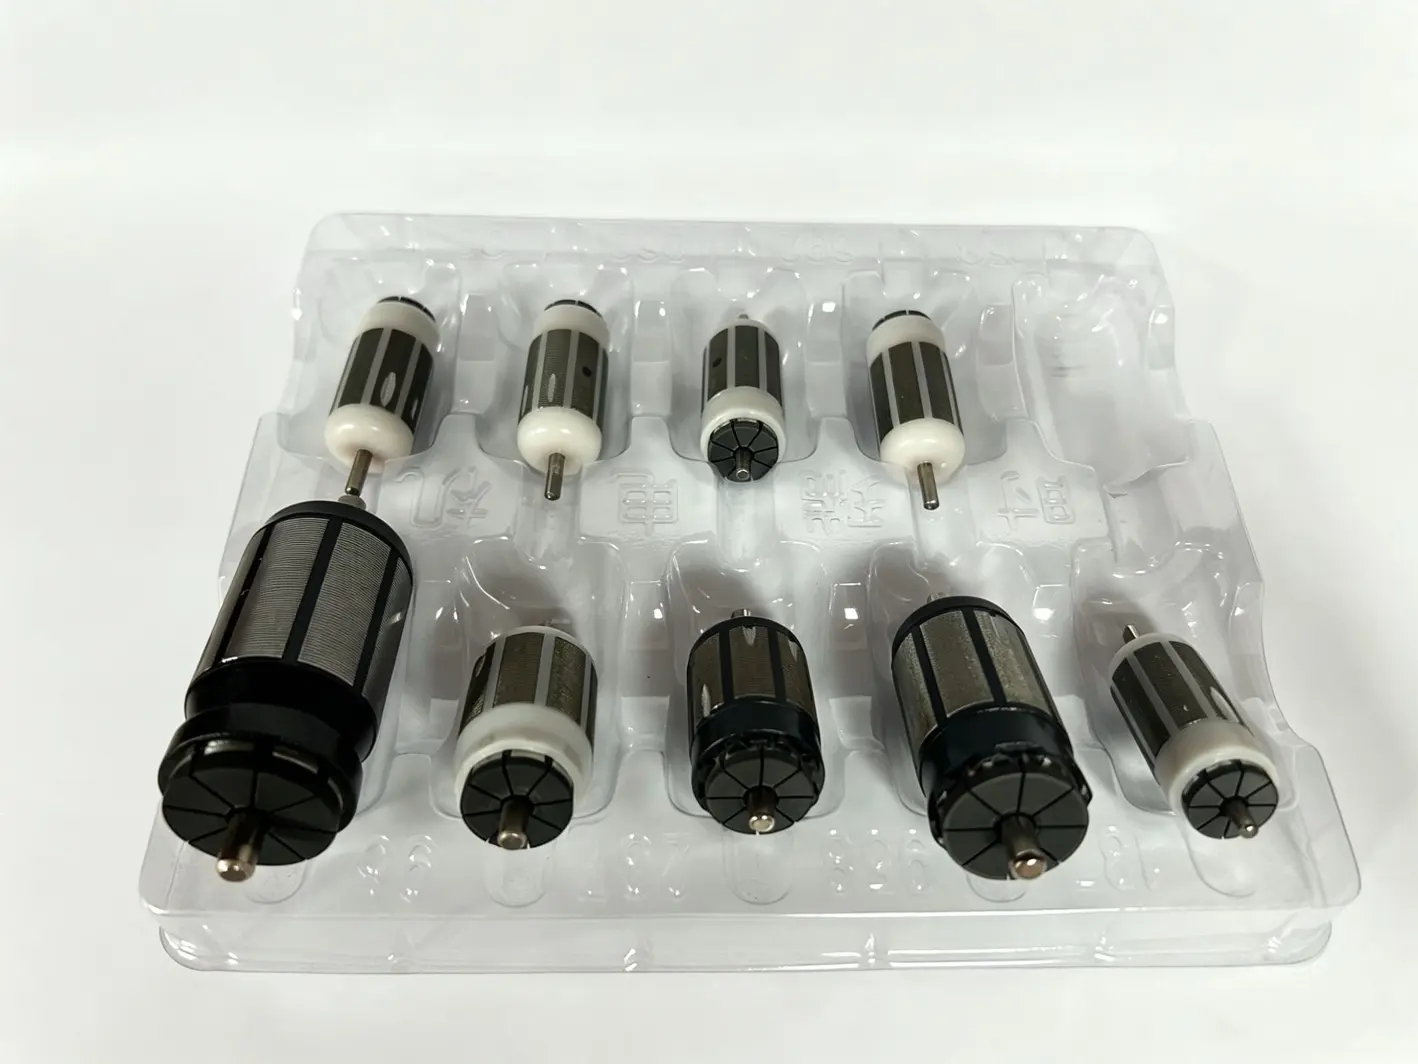
Carbon Commutator Assembly

High-precision carbon-graphite commutators engineered for DC pump motors operating in corrosive fuel or intense brake pump environments.

  • MaterialCarbon-Graphite + Cu
  • ApplicationEFI & Micro Pump Motors
  • ResistanceEthanol / Methanol Proof
Complete Pump Electric fuel pump assembly for automotive EFI systems

Electric EFI Pump Unit

Dynamic-balanced core pump units engineered for continuous high-pressure delivery, low noise output, and extended working life cycles.

  • OperationSubmerged / In-line
  • Key TechDynamic Balancing Core
  • StandardsOEM / OES Replacement
ECU Feedback Automotive oxygen sensor 89465-0E040 lambda sensor

Precision Oxygen Sensor

High-precision upstream/downstream exhaust lambda sensors providing real-time air-fuel ratio closed-loop feedback to ECU management.

  • OE Reference89465-0E040 Series
  • ElementZirconia Ceramic
  • ProtectionDual Protective Tube
OEM Best Seller HC-QZQE-049C carbon commutator best seller

HC-QZQE-049C Commutator

Flagship OEM replacement commutator designed for heavy-duty fuel delivery and automotive micro-motor armatures with minimal spark generation.

  • ModelHC-QZQE-049C
  • CustomizationDrawing & OE Matching
  • Durability> 3,500 Operating Hours
Armature Assembly Automotive fuel and vacuum pump motor armatures

Precision Motor Armature

Balanced copper-wound motor armatures with integrated graphite commutators, optimized for high torque, zero cogging, and thermal resilience.

  • WindingHigh-Purity Copper Wire
  • Balancing< 2mg Dynamic Tolerance
  • ApplicationBrake Booster & EFI Motor
Graphite Disc Disc type planar carbon commutator for fuel and auxiliary pumps

Planar Disc Commutator

Face-type planar commutators delivering uniform contact pressure, ultra-low acoustic signature, and exceptional resistance to fuel cavitation.

  • StructurePlanar / Face-type Disc
  • Noise Level< 42 dB(A) Smooth Run
  • CompatibilityGasoline, E85, Methanol
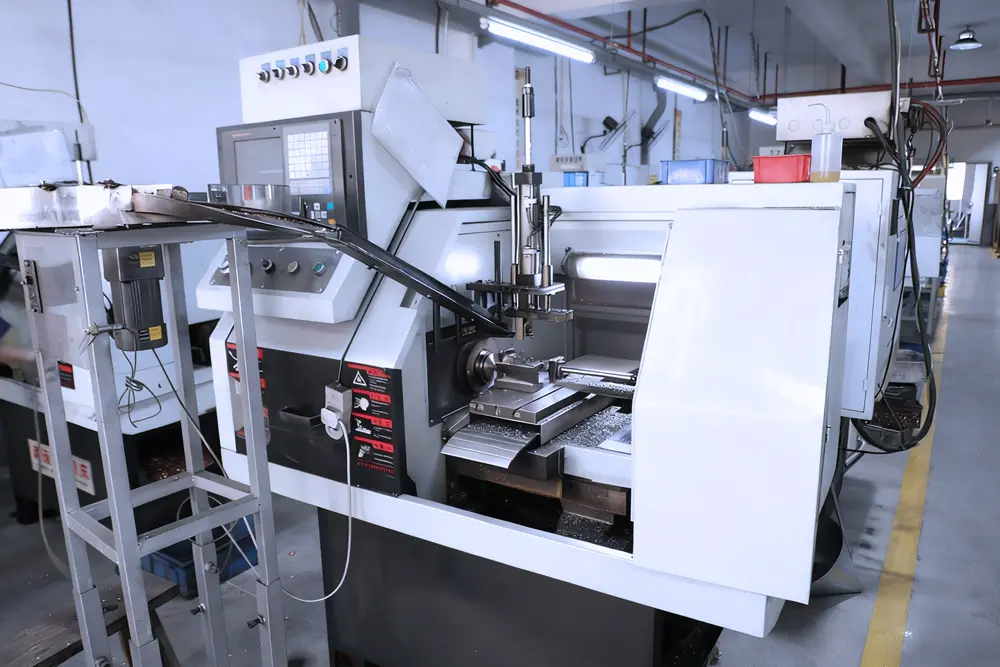
Factory Tour Precision manufacturing workshop for electric pump parts

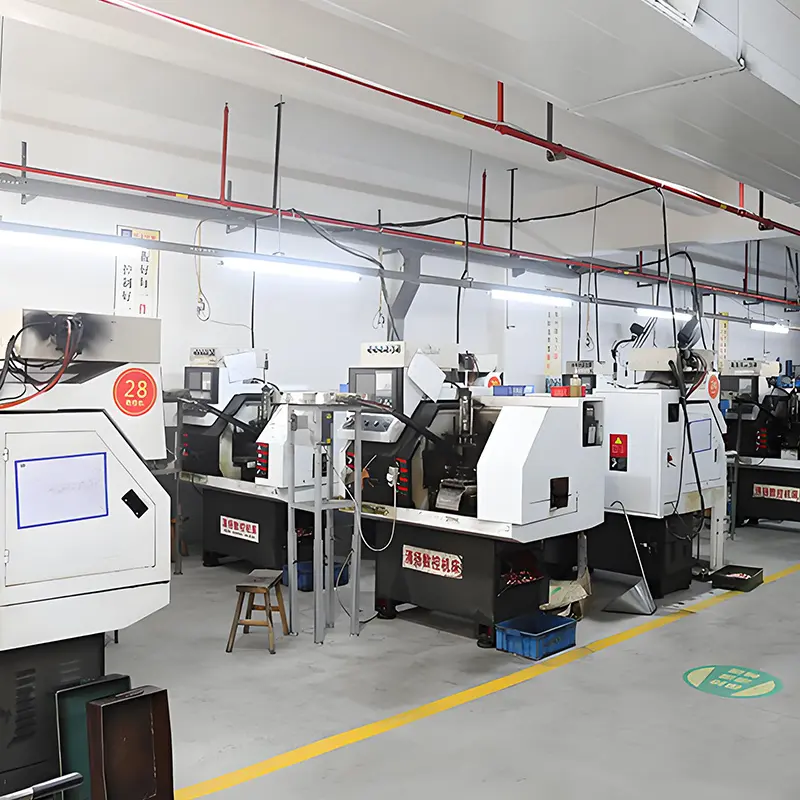
Automated Workshop Units

Custom contract manufacturing for micro-motor assemblies and pump internals leveraging robotic segment placement and optical inspection.

  • Capacity100,000+ Units / Month
  • Inspection100% Automated Optical/AOI
  • FacilityRuian, Wenzhou Base
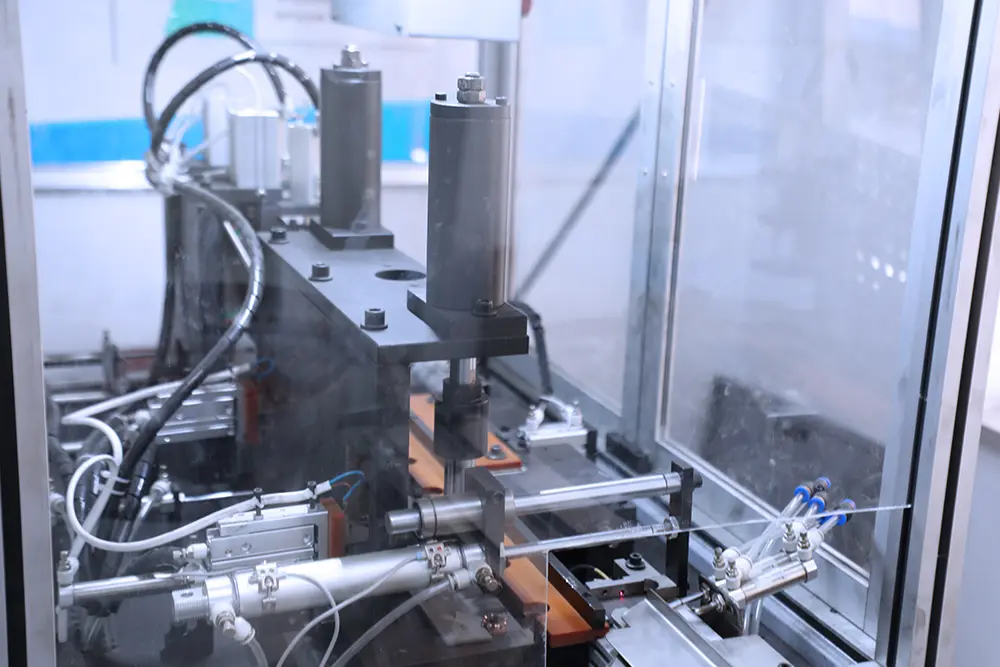
Custom Solution Inspection and testing line for automotive electric pump modules

Subsystem Modular Solutions

Integrated micro-motor and pump housing engineering tailored to customer CAD schematics, OE fitment benchmarks, and environmental test specs.

  • EngineeringCAD / 3D SolidWorks Design
  • TestingSalt-Spray & Thermal Shock
  • TraceabilityLaser QR Code Serialization
Global Market Analysis

Commercial & Industrial Landscape of Electric Brake Pumps

The global automotive brake subsystem landscape is experiencing a generational shift. The transition from internal combustion engines (ICE) to hybrid electric vehicles (HEV) and battery electric vehicles (BEV) has fundamentally eliminated the continuous manifold vacuum traditionally used to power pneumatic brake boosters.

Pneumatic Vacuum Deprivation

Downsized turbocharged direct-injection gasoline engines and electrified powertrains generate insufficient or zero intake manifold vacuum. Global automakers rely heavily on standalone auxiliary Electric Vacuum Pumps (EVP) and integrated electro-hydraulic brake systems to guarantee instant deceleration pressure.

Stringent Response Time Metrics

Advanced Driver Assistance Systems (ADAS) and Autonomous Emergency Braking (AEB) mandate hydraulic pressure rise times under 120 to 150 milliseconds to achieve zero-collision standards. Electric brake booster pumps provide near-instantaneous pressure spikes compared to sluggish mechanical belts.

Micro-Motor Duty Cycle Demands

Brake boost pumps experience irregular intermittent duty cycles, extreme vibration profiles (up to 15G), and aggressive thermal cycling (-40°C to +125°C). Motor brush-commutator pairs must withstand rapid stall currents without dielectric degradation or mechanical fracturing.

System Architecture Vacuum / Pressure Source Response Latency Energy Parasitic Drag Application Domain
Traditional Mechanical Vacuum Engine Intake Manifold / Camshaft Pump 350 – 500 ms Continuous engine load (~0.8 kW drag) Legacy naturally-aspirated ICE
Auxiliary Electric Vacuum Pump (EVP) Independent On-Demand 12V DC Vane/Diaphragm 180 – 250 ms On-demand activation only (< 0.1 kWh/100km) Turbo GDI, Mild Hybrids, PHEV
Electro-Hydraulic Braking (EHB / One-Box) Integrated High-Speed Brushless/Brushed Motor 90 – 130 ms Intelligent regenerative coordination Modern BEVs, Autonomous Driving Level 2+ / Level 3
Electro-Mechanical Brake (EMB / Caliper Actuated) Direct Caliper Motor Gear Drive (Brake-by-Wire) < 80 ms Zero hydraulic drag, purest electric actuation Next-Gen Steer-by-Wire & EMB Platforms
Industrial Cluster Dynamics

The Wenzhou & Ruian Manufacturing Advantage

Located in Ruian, Wenzhou — widely recognized as the automotive components manufacturing capital of China — Wenzhou Hualeao Automotive Parts Co., Ltd. capitalizes on unparalleled supply chain concentration, vertical production density, and relentless manufacturing velocity.

  • 15-Kilometer Vertical Sourcing Radius

    From metallurgical graphite synthesis and copper stamping to automated injection molding and dynamic balancing, our entire component ecosystem resides within minutes of our assembly floor.

  • 6,200 m² Precision Production Ecosystem

    Advanced tooling, multi-station compression presses, and high-speed multi-axis CNC commutating lathes guarantee micron-level concentricity and surface finish standards.

  • National Energy-Saving Project Recognition

    Our EFI carbon commutator was recognized as a designated national energy conservation and emission reduction project under China’s 11th Five-Year Plan, underscoring deep domestic R&D validity.

Hualeao factory research and development facility in Wenzhou China
6,200m²
Integrated Factory Area · Ruian, Wenzhou
50+
Expert Tooling Engineers & Technicians
10+
Accredited Industry Quality Certifications
3,000+
Active Global OEM & Aftermarket Buyers
Operational Realities

Mission-Critical Application Scenarios

Electric brake and fluid pumps do not operate in laboratory cleanrooms. They must function under harsh environmental shocks, volatile fuel chemistries, high temperatures, and salt-laden atmospheres.

Electric & Hybrid Passenger Cars

BEVs and PHEVs require active electronic brake vacuum boost during regenerative deceleration. Commutators and motors maintain silent operation (<42 dB) inside passenger cabin zones while executing frequent micro-starts.

Biofuel, Ethanol & Methanol Environments

Standard copper commutators react with organic acids present in E85, E100, and M15 fuels, resulting in rapid pitting and catastrophic open circuits. Our high-density carbon-graphite elements resist chemical dissolution completely.

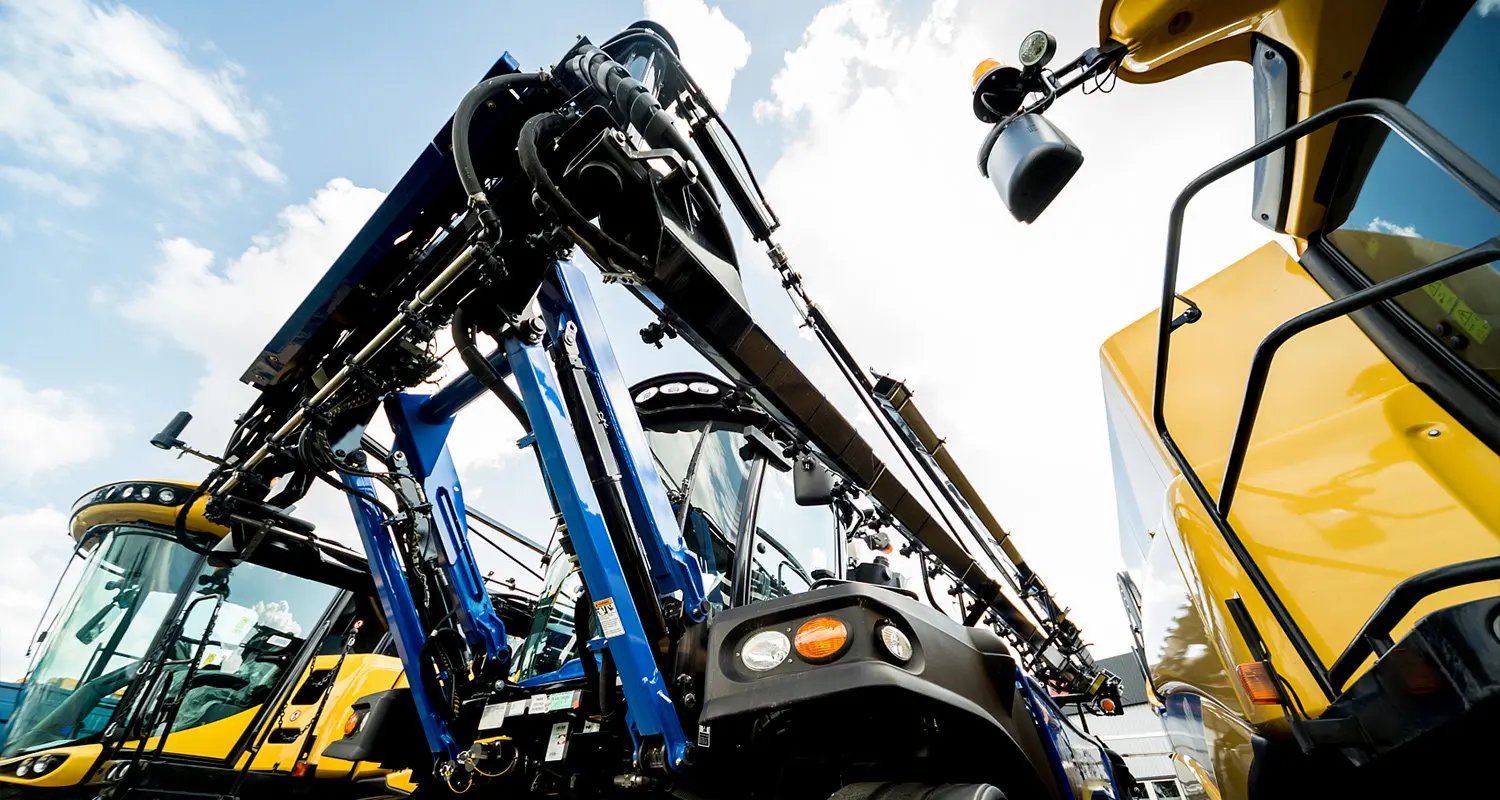
Heavy Commercial & Construction Fleet

Excavators, mobile cranes, and mining haulers undergo intense continuous vibration and ambient heat up to 110°C. Reinforced segment clamping rings prevent centrifugal graphite displacement under sudden hydraulic stall loads.

Marine Inboard & Coastal Systems

Continuous exposure to high-humidity saline fog destroys ordinary automotive brush assemblies. Specialized surface passivation and stainless terminal reinforcements protect pump cores from electrolytic galvanic oxidation.

Forward Engineering Roadmap

Key Industry Trends Transforming Electric Brake Pumps

The convergence of software-defined vehicles, functional safety standards (ISO 26262 ASIL D), and electrification is revolutionizing automotive pumping dynamics.

1. Convergence on One-Box EHB Systems

The automotive market is transitioning rapidly from Two-Box (separate EVP + vacuum booster) to integrated One-Box electro-hydraulic brake systems. In a One-Box configuration, the electronic pedal simulator, motor pump, and ABS/ESC valve block are consolidated into a single lightweight unit. This requires pump motors capable of delivering up to 18 MPa of pressure in under 100 ms.

2. Nano-Composite Carbon Commutator Chemistry

While brushless DC (BLDC) motors gain market share in primary high-duty actuators, brushed DC motors remain the dominant, cost-efficient choice for auxiliary booster pumps, secondary fail-safe circuits, and aftermarket replacements. The development of phenolic resin-bonded nano-graphite eliminates brush arc erosion and lowers radio-frequency electrical noise (EMC compliance).

3. Fail-Safe Dual Circuit Redundancy

Autonomous driving architectures (SAE Level 3 to Level 5) require mechanical and electrical redundancy. China suppliers are advancing dual-stator micro-pumps and twin-circuit motor windings so that a singular brush, coil, or power failure will not compromise hydraulic emergency stops.

Sourcing & Compliance Standards

What Global Tier-1 Buyers Demand from China Suppliers

Procurement directors and quality engineers from Europe, North America, and Southeast Asia look beyond raw unit price. International automotive partnerships demand strict adherence to rigorous engineering protocols.

IATF 16949 & PPAP Level 3

Full Production Part Approval Process (PPAP) documentation, including Process FMEA, Control Plans, Gauge R&R, and dimensional layout inspections to ensure zero defect slippage during series ramp-up.

Material Purity & Spectroscopy

Direct verification of copper oxygen content (<10 ppm) and graphite density (>1.78 g/cm³) via optical emission spectrometry and helium pycnometry to prevent mechanical delamination.

Automated In-Line AOI Inspection

100% automated optical inspection for segment undercut depth, mica undercut clearance, bar-to-bar pitch consistency, and bar-to-ground dielectric breakdown resistance up to 1,500V.

Supply Chain Continuity & ESG

Robust multi-tier supplier audit networks, closed-loop scrap recycling, RoHS / REACH compliance, and guaranteed buffer inventory safety reserves for global shipping security.

Engineering Knowledge Base

Frequently Asked Questions for Sourcing Directors

Find authoritative answers to critical engineering, material validation, and production questions regarding electric brake pumps, fuel pumps, and carbon commutators.

What are the key technical failure modes of electric brake booster pumps?

The dominant failure modes in electric vacuum brake pumps include: (1) Vane/diaphragm wear caused by fine particulate contamination, (2) Motor commutator burn-out due to inductive arcing during high-frequency stop-start cycles, and (3) Moisture condensation ingress leading to bearing seizure in freezing environments. Hualeao combats motor failure by deploying precision-ground carbon commutators with synthetic resin binders that maintain stable film lubrication even under heavy electrical sparking.

Why is carbon (graphite) preferred over pure copper in pump commutators?

In submerged fuel pumps and high-duty auxiliary motors, fuel or ambient humidity functions as an electrolyte. Under DC potential, copper segments suffer electrochemical corrosion, aggressive oxidation, and accelerated mechanical gouging. Carbon-graphite commutators form an inert tribological transfer film that resists chemical attack from alcohol additives (ethanol/methanol) and exhibits self-lubricating properties, reducing brush friction and extending operational lifespan past 3,000+ continuous hours.

How does Wenzhou Hualeao validate parts against imported OE benchmarks?

Our development process aligns directly with international OE material and performance criteria. We employ coordinate measuring machines (CMM) for sub-micron geometrical verification, digital profilometers to evaluate surface roughness (Ra < 0.2 μm), automated voltage drop testing, and continuous endurance dyno test benches simulating 100,000 brake actuation cycles in temperature-controlled environmental chambers (-40°C to 120°C).

Can Hualeao manufacture customized motor armatures and commutators from drawings?

Yes. Our engineering division works directly with 2D drawings (DWG, PDF) and 3D CAD files (STEP, IGES, SolidWorks). We determine the appropriate segment geometry, mold design, copper hook layout, carbon formulation, and dynamic balance limits. Prototype samples are typically completed within 15 to 25 business days, backed by comprehensive pre-production dimensional inspection reports.

What quality assurances accompany large-volume OEM export shipments?

All production runs are governed by rigorous in-process statistical process control (SPC). Every outgoing lot is accompanied by a Certificate of Analysis (COA), material melt certificates, dimensional reports, and dielectric breakdown testing records. We offer standard OEM warranty coverage ranging from 12 to 24 months, with full batch traceability enabled via laser-etched QR codes and serial numbering.

What lead times and minimum order quantities (MOQ) apply for international orders?

For standard catalog commutators and fuel pump models, our typical MOQ starts at 500 to 1,000 units, with repeat orders dispatching within 15 to 20 days. For custom-tooled prototypes or dedicated private-label assemblies, initial tooling lead time is approximately 3 to 4 weeks. Sea freight departs through Ningbo or Shanghai ports, while air expedited shipments leave via Wenzhou Longwan or Shanghai Pudong.

Featured Sourcing Catalog

Explore Our Full Range of Subsystem Solutions

Connect directly with our engineering division to request complete technical data sheets, CAD blueprints, and volume wholesale quotations for immediate procurement.

Heavy Machinery Construction machinery engine fuel system components

Heavy Duty Fuel System Core

High-displacement pump components built to withstand heavy dust, mechanical vibration, and continuous industrial duty cycles.

  • EnvironmentHigh Dust / Heavy Shock
  • TargetLoaders, Cranes, Excavators
  • LifespanExtended Service Interval
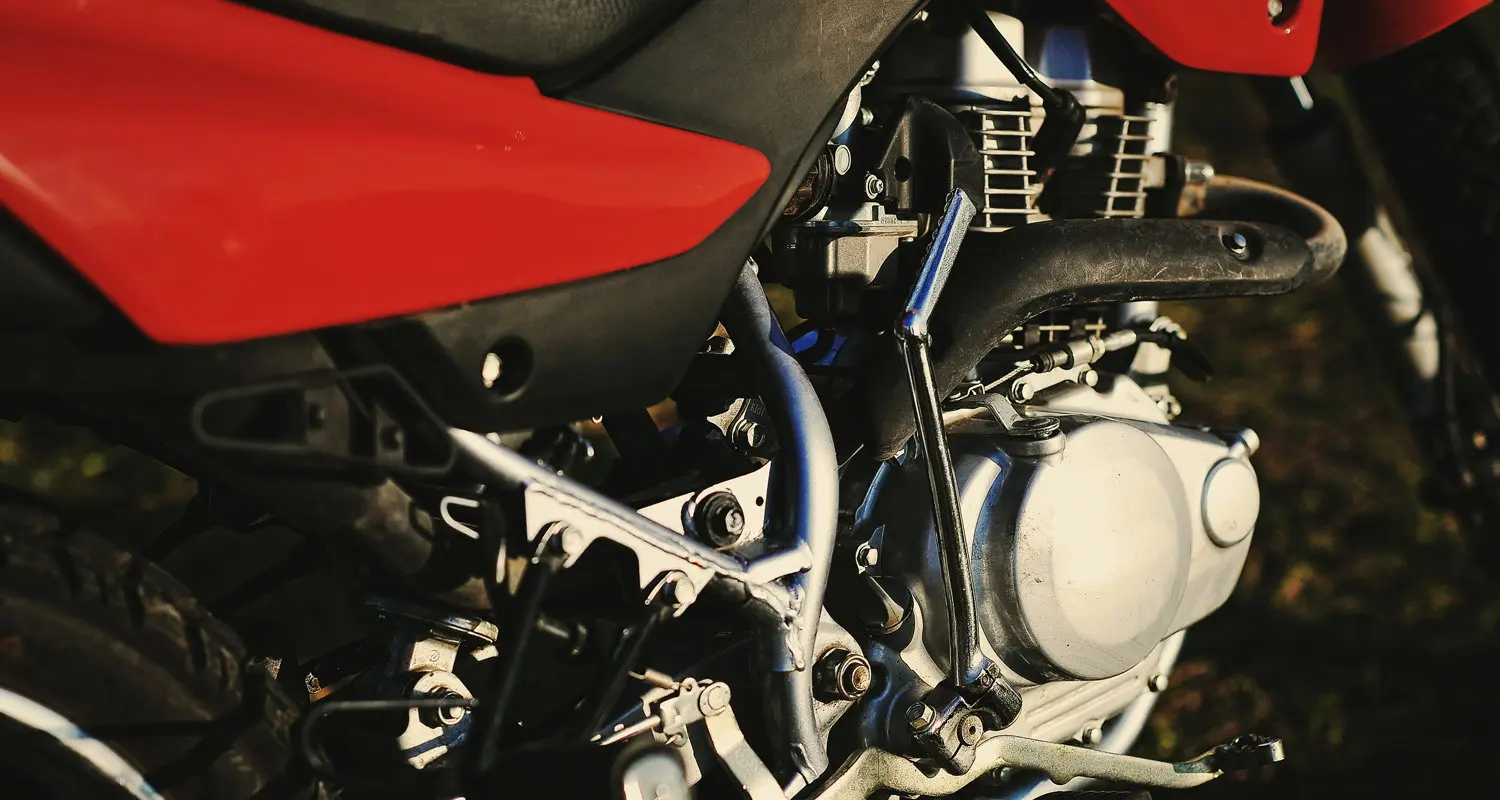
High RPM Unit Motorcycle engine EFI pump micro commutator

High-Rev Motorcycle Commutator

Ultra-compact, low-inertia carbon commutators engineered for high-revving motorcycle engines with instant throttle response.

  • InertiaUltra-Low Rotor Weight
  • SpeedsUp to 12,000 RPM Stable
  • DesignSpace-Saving Envelope
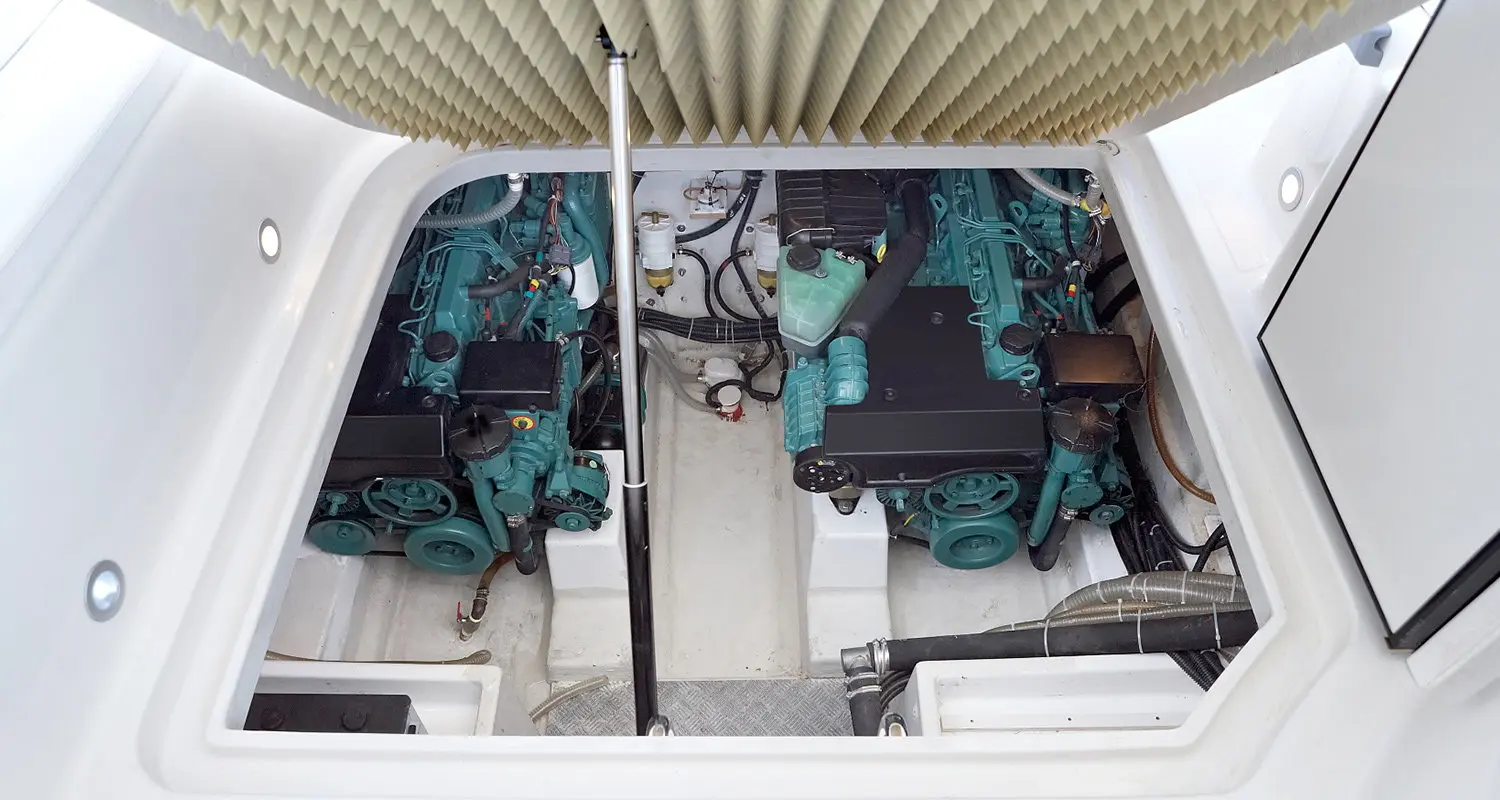
Marine Spec Marine engine fuel system corrosion proof components

Marine Salt-Spray Protected Unit

Passivated brass terminals and anti-corrosive carbon alloys tailored for coastal vessels and inboard marine engine setups.

  • Test StandardASTM B117 Salt Fog 500h
  • ProtectionAnti-Electrolytic Barrier
  • MediaMarine Grade Distillates
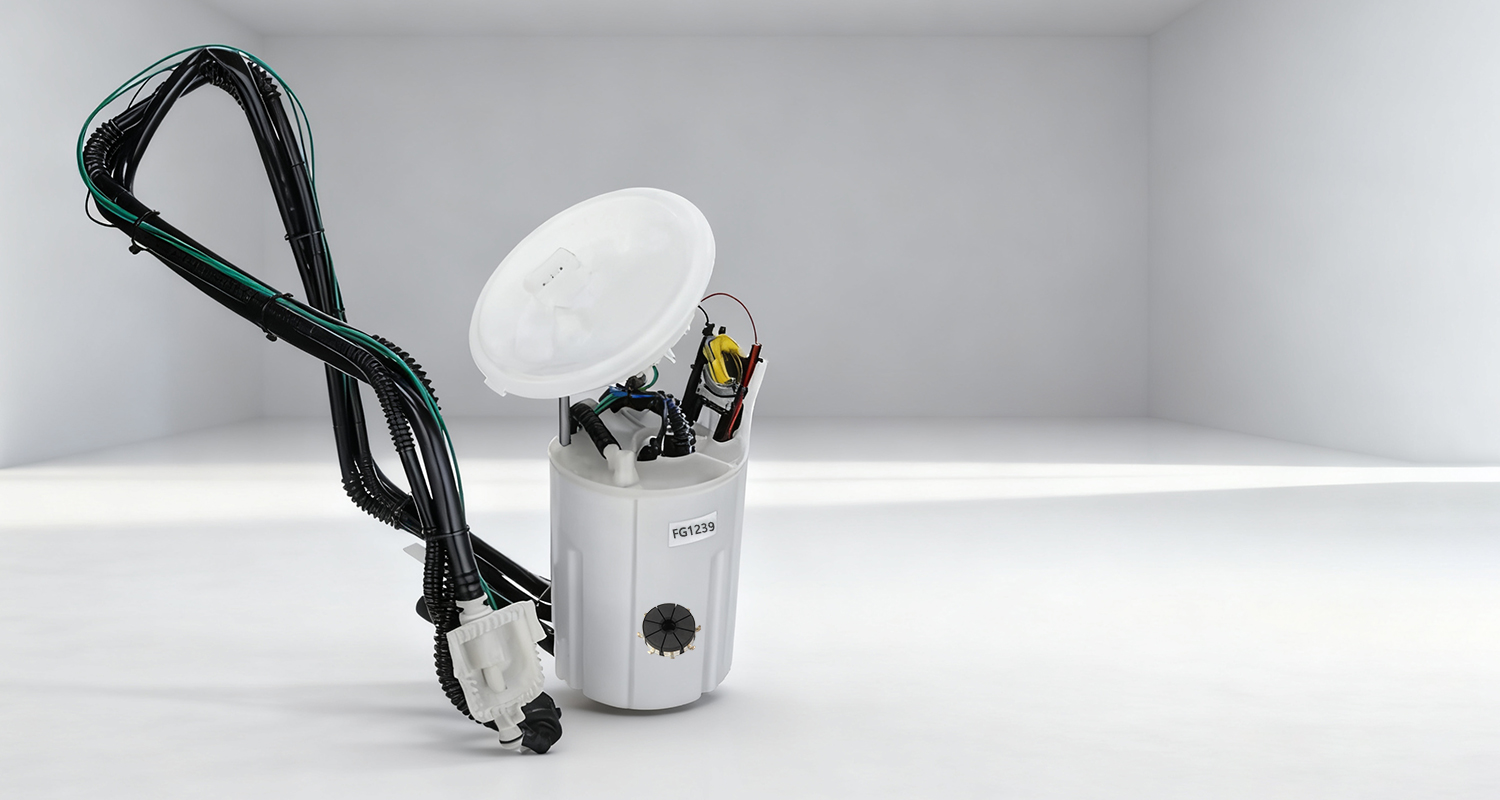
Automotive Powertrain Automotive engine fuel pump and electronic delivery system

Automotive Fuel Delivery System

Comprehensive fuel pump modules providing stable rail pressure, low vapor lock tendency, and seamless ECU integration.

  • Flow RateCalibrated to OEM Curve
  • Noise SignatureAcoustic Damping Design
  • FitmentDirect Bolt-on OE Specs
Inspection Line Quality assurance and electrical testing of commutators

Quality Assurance Test Station

Multi-point automated electrical integrity testing station verifying bar resistance, dielectric strength, and bar weld integrity.

  • Testing100% In-Line High-Pot Test
  • ToleranceMicron Precision Gauging
  • CertificationFull Lot Traceability
Material Lab Raw material selection for graphite and copper pump commutators

Raw Material Formulation Lab

Strict verification of synthetic graphite grain sizes and binder resins ensuring zero porosity and uniform volumetric electrical conductivity.

  • Graphite GradeIsostatically Molded
  • Copper Purity> 99.95% Electrolytic Cu
  • Thermal Range-40°C to +150°C Stable
Precision Tooling Custom commutator production and tool design

Custom Mold & Tooling Services

In-house tooling department fabricating stamping dies, multi-cavity injection molds, and automated assembly fixtures for custom pump motors.

  • Tooling CycleFast 20-Day Prototyping
  • EquipmentSlow-Wire EDM & CNC Milling
  • FlexibilityLow to High Volume Runs
Exhaust Control DC motor and sensor integration for modern automotive applications

Exhaust & Motor Management

Integrated engine management hardware solutions aligning fuel injection velocity, micro-motor response, and exhaust emissions compliance.

  • FeedbackMicrosecond ECU Sampling
  • EmissionsEuro 6 / China 6 Compatible
  • IntegrationDirect Harness Connectors
Direct Factory Engineering Desk

Have a Drawing, OE Reference, or RFP?

Connect directly with our senior application engineers in Ruian, Wenzhou. We evaluate your pump volume requirements, motor armature constraints, and fuel media properties to provide rapid quotations and CAD feasibility reports.

Verified Manufacturing Contact Data

Company: Wenzhou Hualeao Automotive Parts Co., Ltd.

Plant Address: Building 5, Lianjiang Industrial Park, Pantai Street, Ruian City, Wenzhou, Zhejiang Province, China

Telephone Desk: +86-577-66811811

Mobile / Direct: +86-150-6776-3878

Official Inquiries: [email protected]