Supplying Tier-1 fuel system assemblers and precision DC motor manufacturers with high-concentricity carbon commutators, balanced armatures, high-pressure EFI modules, and lambda sensors.

Formulated for aggressive fuel environments, high rotational speeds, and reduced electrical sparking in submerged pump armatures.

Submerged electronic fuel injection pump built with dynamically balanced armatures, low vibration harmonics, and stable flow curves.

Zirconia ceramic sensing element delivering high response rates and accurate closed-loop stoichiometric air-fuel feedback.

High-demand planar disc-type carbon commutator for compact EFI armatures, offering superior axial space conservation.
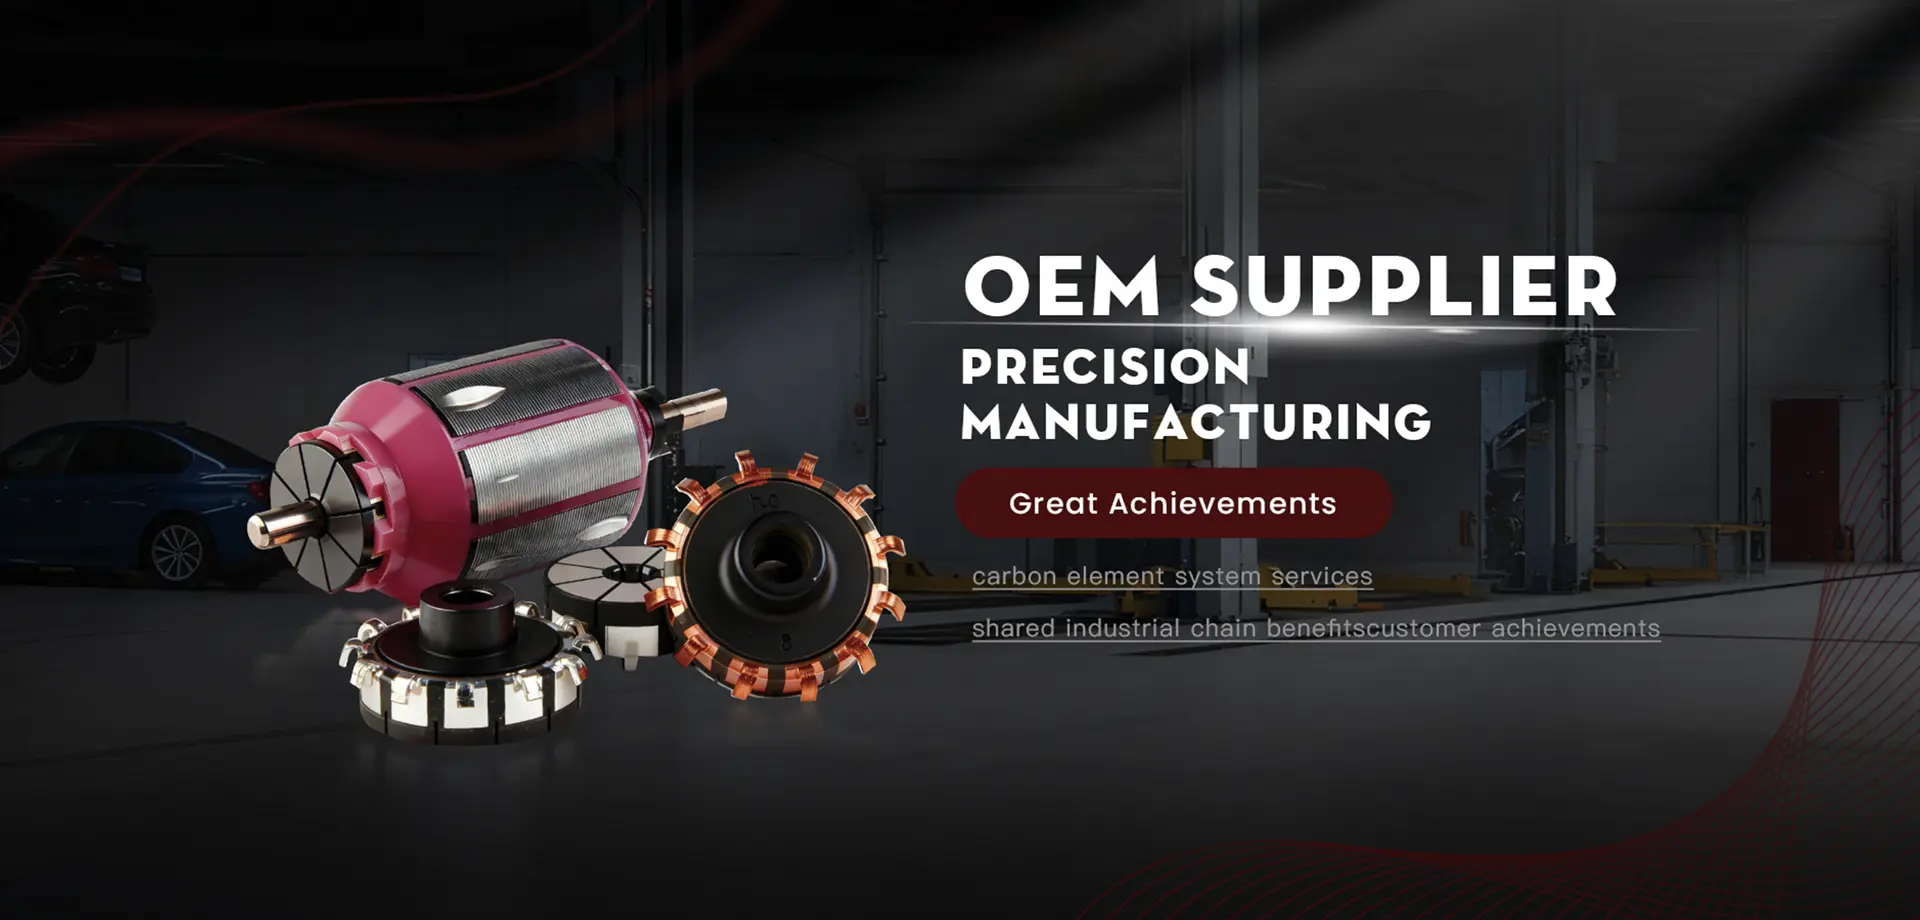
Precision-wound copper magnet wire armature with molded commutator segments engineered for continuous 12V/24V service life.
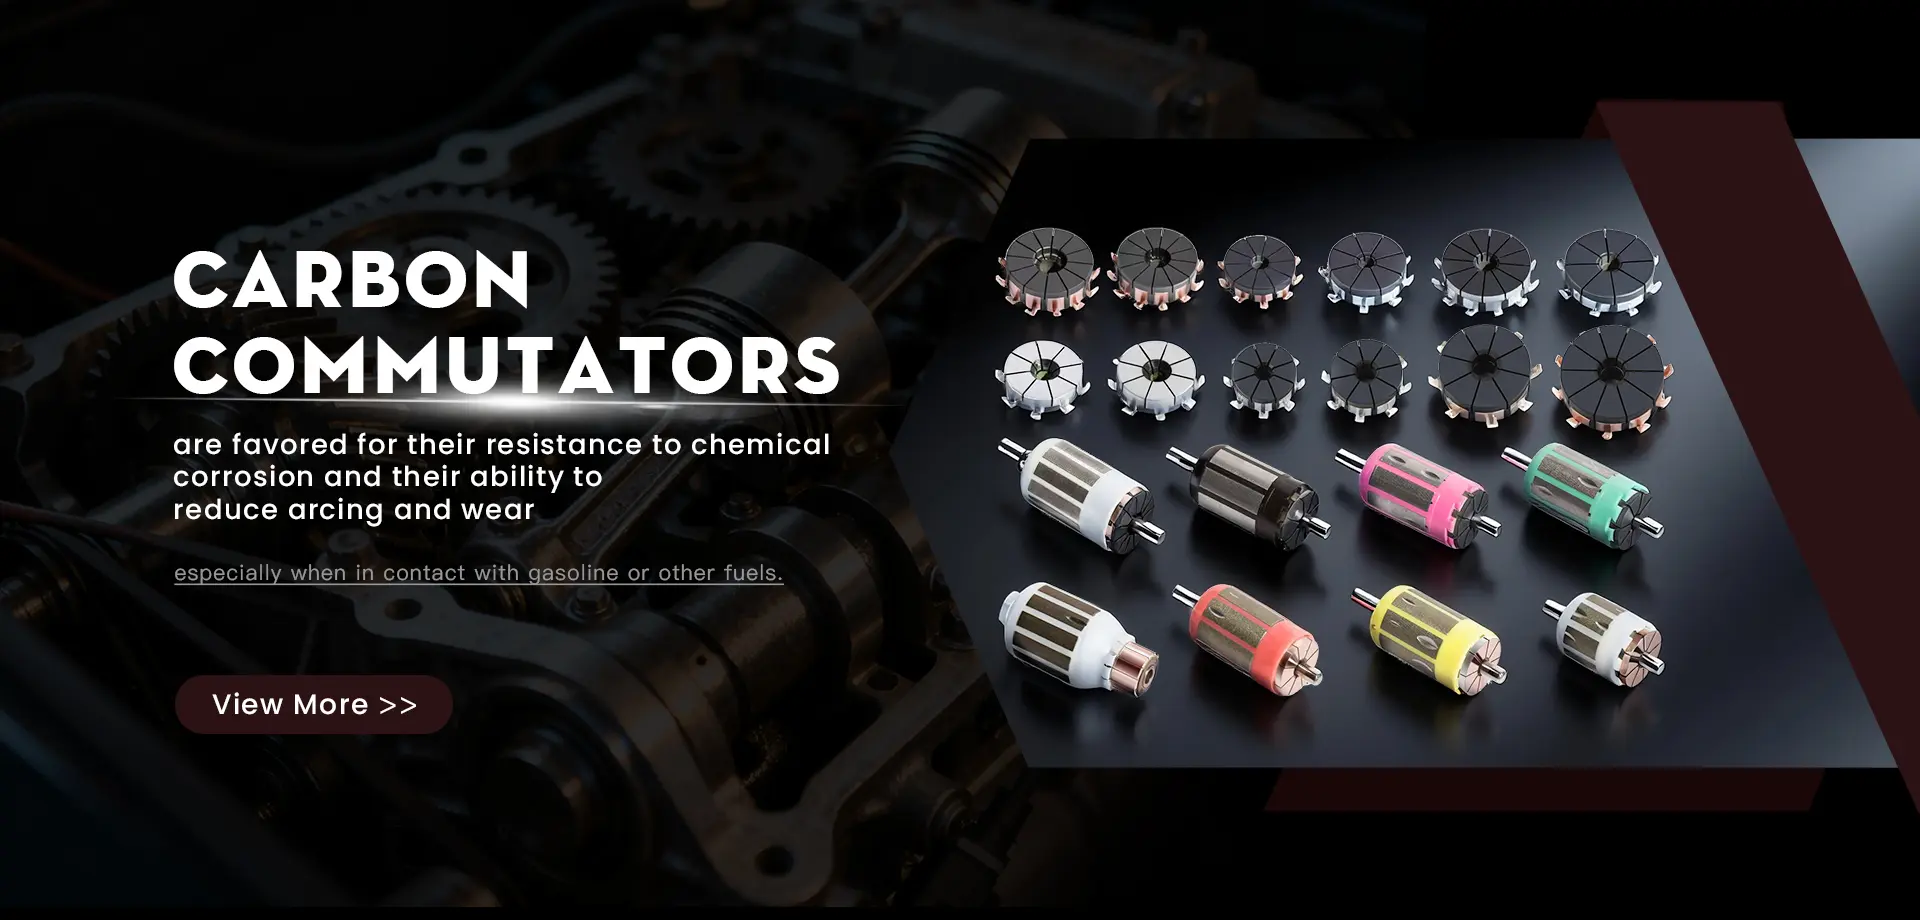
Engineered synthetic carbon barrier preventing electrochemical copper delamination in severe flex-fuel environments.
Reinforced mechanical anchoring designed to withstand high hydraulic pressure spikes, severe dust ingress, and shock loading.
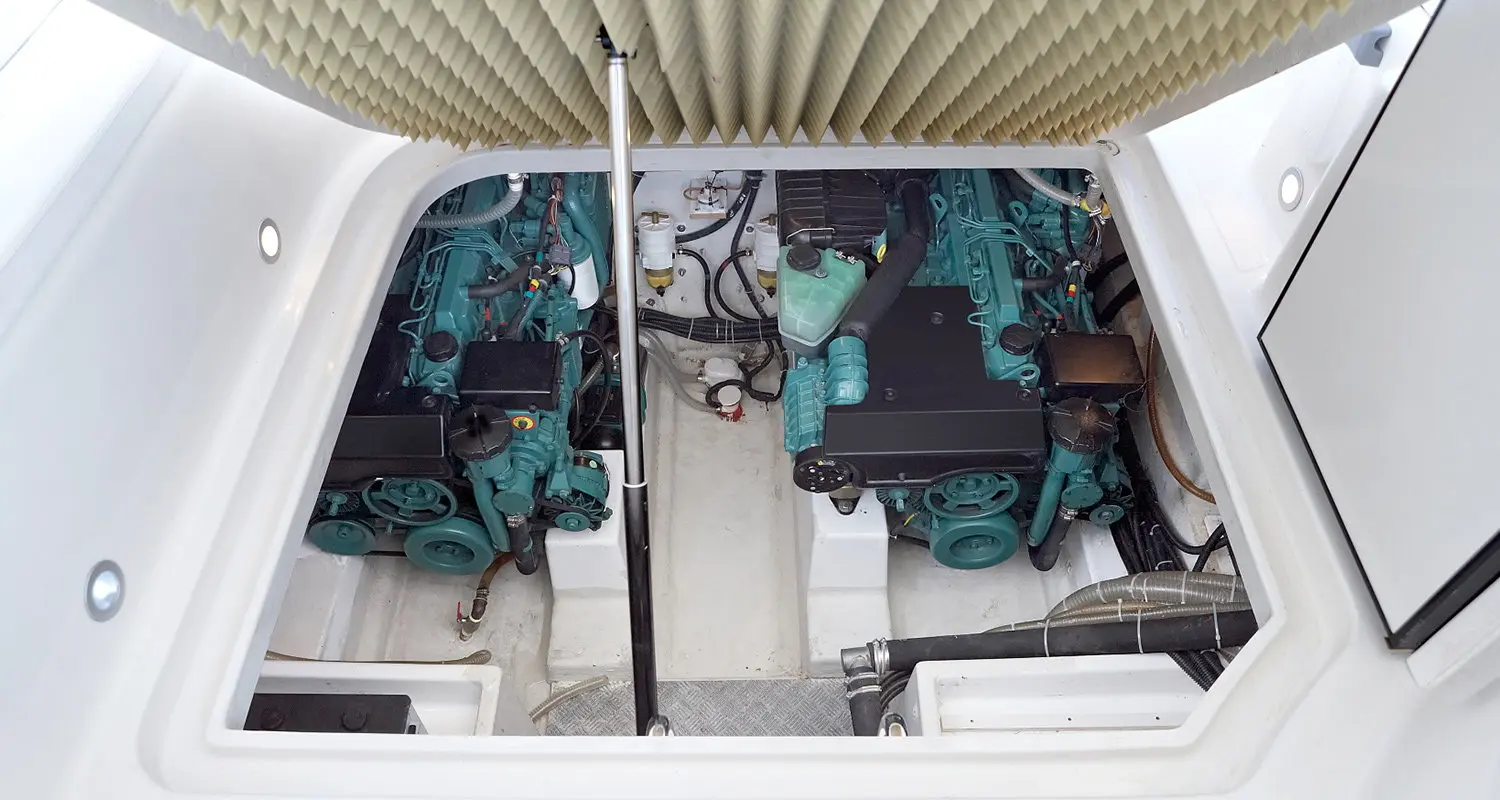
Special anti-corrosion chemical passivation preventing electrolytic galvanic pitting in marine coastal salt-fog conditions.
Navigating the dual evolution of global vehicle electrification, micro-motor multiplication, and flex-fuel resilience across the international Tier-1 procurement ecosystem.
Global regulatory mandates pushing for E10, E27 (Brazil), E85 (North America), and synthetic methanol blends (Asia & Europe) have created a catastrophic failure point for legacy copper-segment commutators. In high-polarity alcohol fuels, standard copper undergoes rapid electrolytic corrosion and micro-arcing wear. Carbon (graphite) commutators provide an chemically inert tribological contact interface that preserves contact stability over 150,000+ vehicle miles.
While high-voltage traction inverters dominate EV news, modern passenger cars and commercial fleets utilize between 80 and 150 auxiliary micro-motors. Submerged in-tank fuel pumps, selective catalytic reduction (SCR) urea injection dosing pumps, auxiliary transfer units, and hybrid powertrain secondary circuits continue to demand ultra-compact brushed DC motors where commutator precision determines unit efficiency, acoustic signature, and EMI compliance.
Next-generation powertrain auxiliary components require an aggressive reduction in axial length and weight without sacrificing torque or operational duty cycle. Planar disc-type commutators and precision diamond-faced commutators allow motor engineers to shorten overall armature stack dimensions by up to 25%, enabling smaller pump envelopes with lower rotational inertia, faster spool-up response, and optimized fuel metering efficiency.
Procuring critical commutation and armature components is no longer purely about piece price. World-class automotive and industrial purchasing groups apply rigorous qualification frameworks.
International OEMs require complete Production Part Approval Processes (PPAP), including Process Failure Mode and Effects Analysis (PFMEA), control plans, and Gage R&R studies to guarantee zero ppm delivery metrics.
Commutator segments undergo heavy tangential centrifugal forces at 18,000–25,000 RPM. Buyers scrutinize the proprietary bonding layer joining the graphite contact facet with the copper carrier substrate.
Total Indicated Runout (TIR) on the commutator diameter must consistently test below 0.003mm. Excessive bar-to-bar step height produces brush bounce, audible motor whine, and electromagnetic radiation.
High-purity carbon-graphite grain size distribution and copper alloy purity (electrolytic tough pitch copper) must be validated with full mill test certificates per production lot to avoid in-field batch degradation.
Based in Ruian, Wenzhou — China's premier automotive components capital — Wenzhou Hualeao Automotive Parts Co., Ltd. marries deep cluster synergy with automated precision manufacturing.
Wenzhou Hualeao Automotive Parts Co., Ltd. researches, engineers, and manufactures carbon (graphite) commutators, fuel pump armatures, and oxygen sensors designed directly against leading foreign brand benchmarks. As part of China’s 11th Five-Year Plan energy-saving initiative, our components deliver import-equivalent endurance at local industrial scale.
Our 6,200 m² modern production complex in Lianjiang Industrial Park integrates automatic compression molding, CNC micro-finishing, automated copper hook forming, and 100% optical AOI segment inspection.
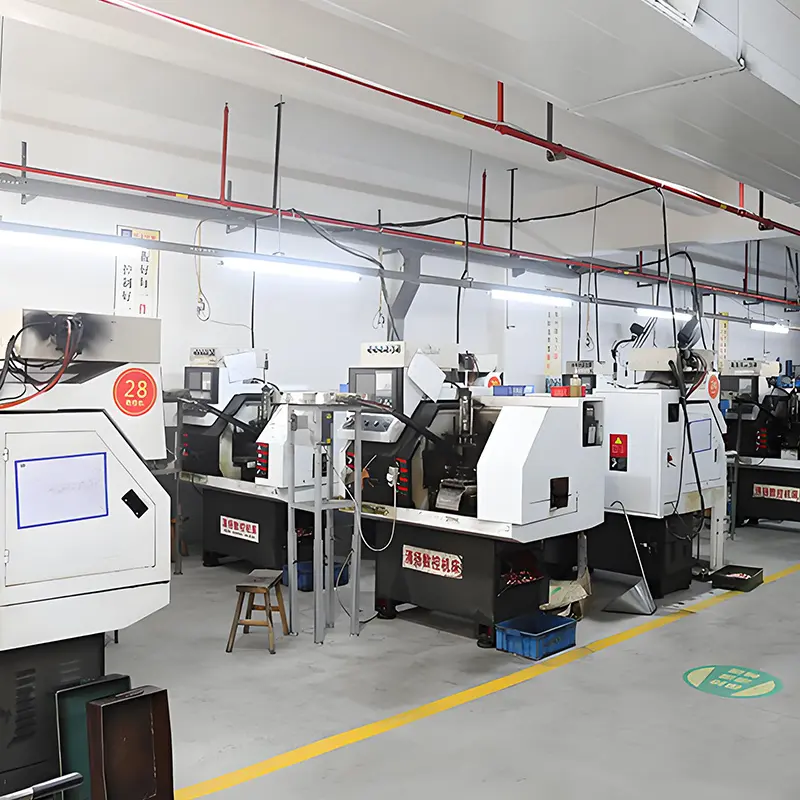

Trusted supplier to established automotive electronics, fuel system assemblers, and global aftermarket distribution networks needing stable, ultra-reliable components.

Ongoing collaboration with top-tier scientific research institutes and universities continually advances our tribological material matrices and high-speed electrical test benches.

Our upstream ecosystem in Zhejiang ensures rapid tooling turnaround (under 20 days for custom tooling), continuous capacity buffers, and zero-defect batch repeatability.

Our commutators and dynamic-balanced pump modules have successfully localized critical EFI components across multiple clean-energy and flex-fuel automotive platforms.
Every commutator and electric fuel pump armature passes through 4 non-negotiable verification gates to eliminate field risk for global procurement teams.
Finite element analysis (FEA) of thermal dissipation, rotational stress under 25,000 RPM, and contact spark distribution modeling before cutting prototype tooling.
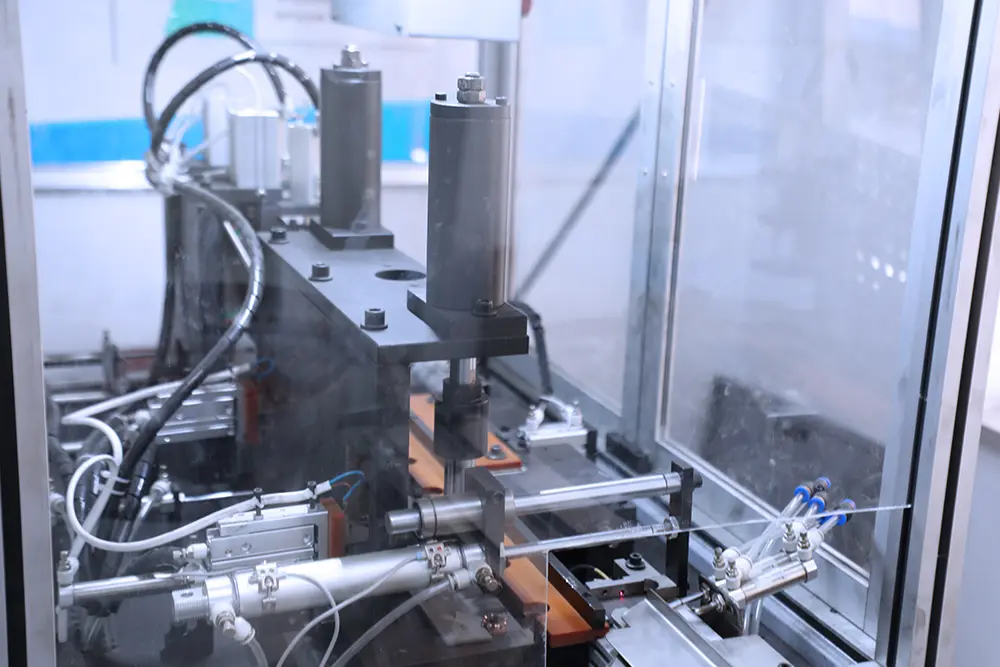
Spectrographic verification of incoming copper grades and carbon block density, ensuring micro-porosity ratings that prevent fuel absorption swelling.
Closed-loop hot-press molding using high-grade thermosetting phenolic resins to secure absolute segment lock and withstand high operating temperatures.
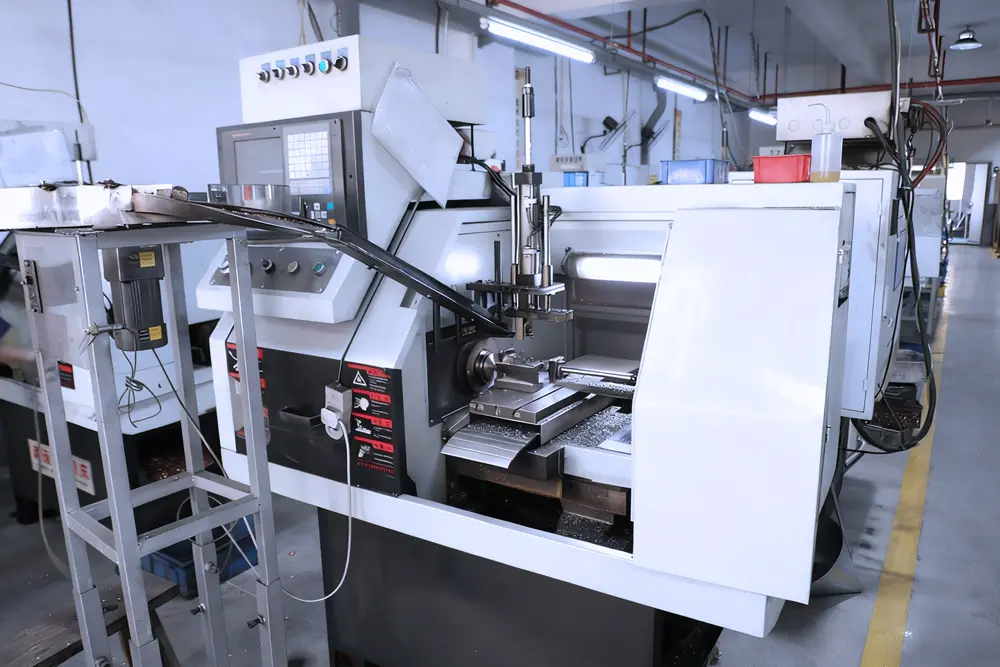
Automated machine vision verification of bar slotting, inter-bar short circuit insulation tests at 1500V AC, and dynamic laser runout profiling.
From high-speed consumer motorcycles to demanding construction hydraulics, our commutators and motor cores maintain steady fluid delivery.
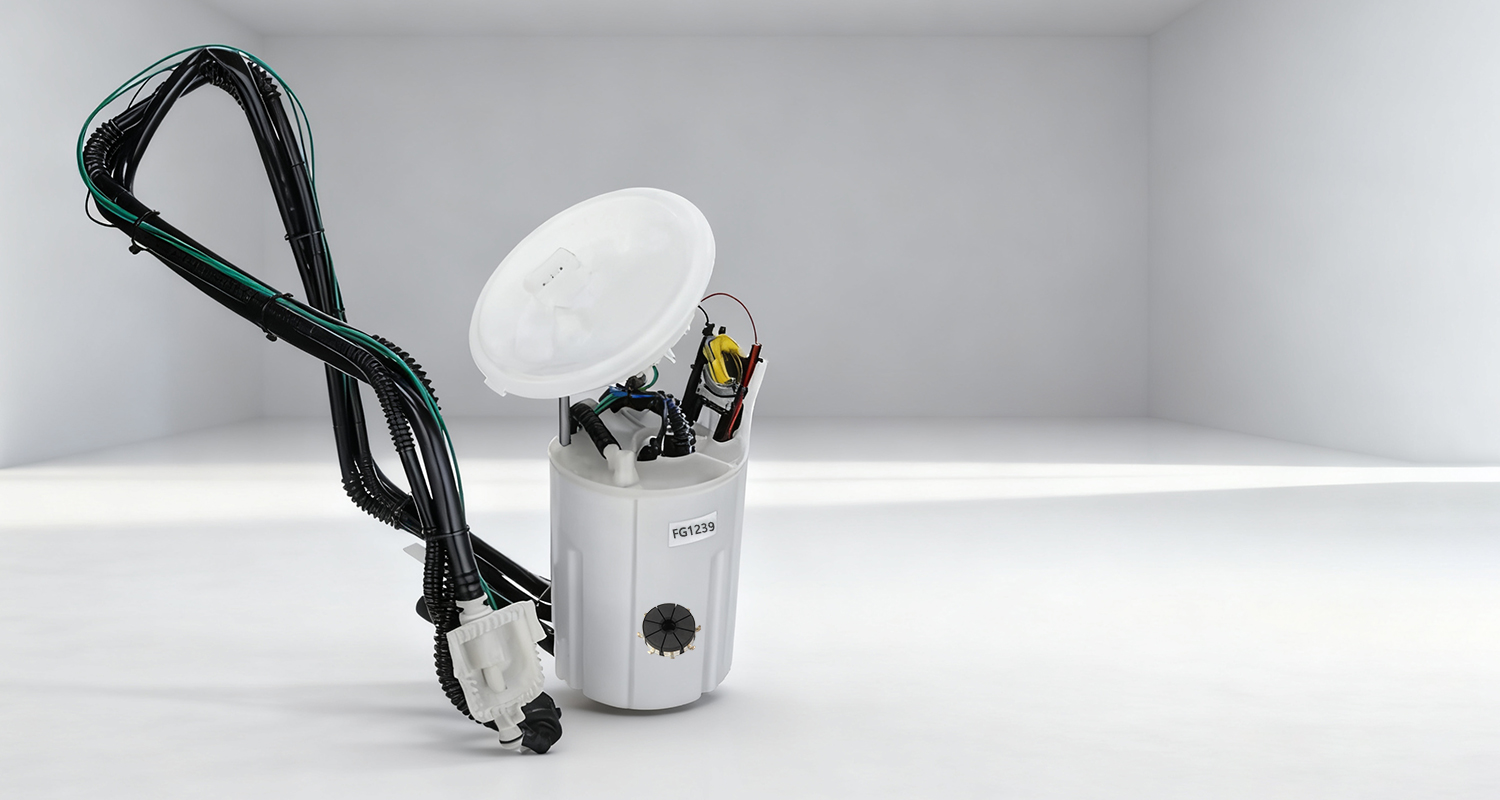
Operating continuously submerged in high-temperature fuel tanks. Our carbon commutators resist ethanol blends, maintaining quiet actuation and low electrical noise across 150,000 km.
Explore Automotive »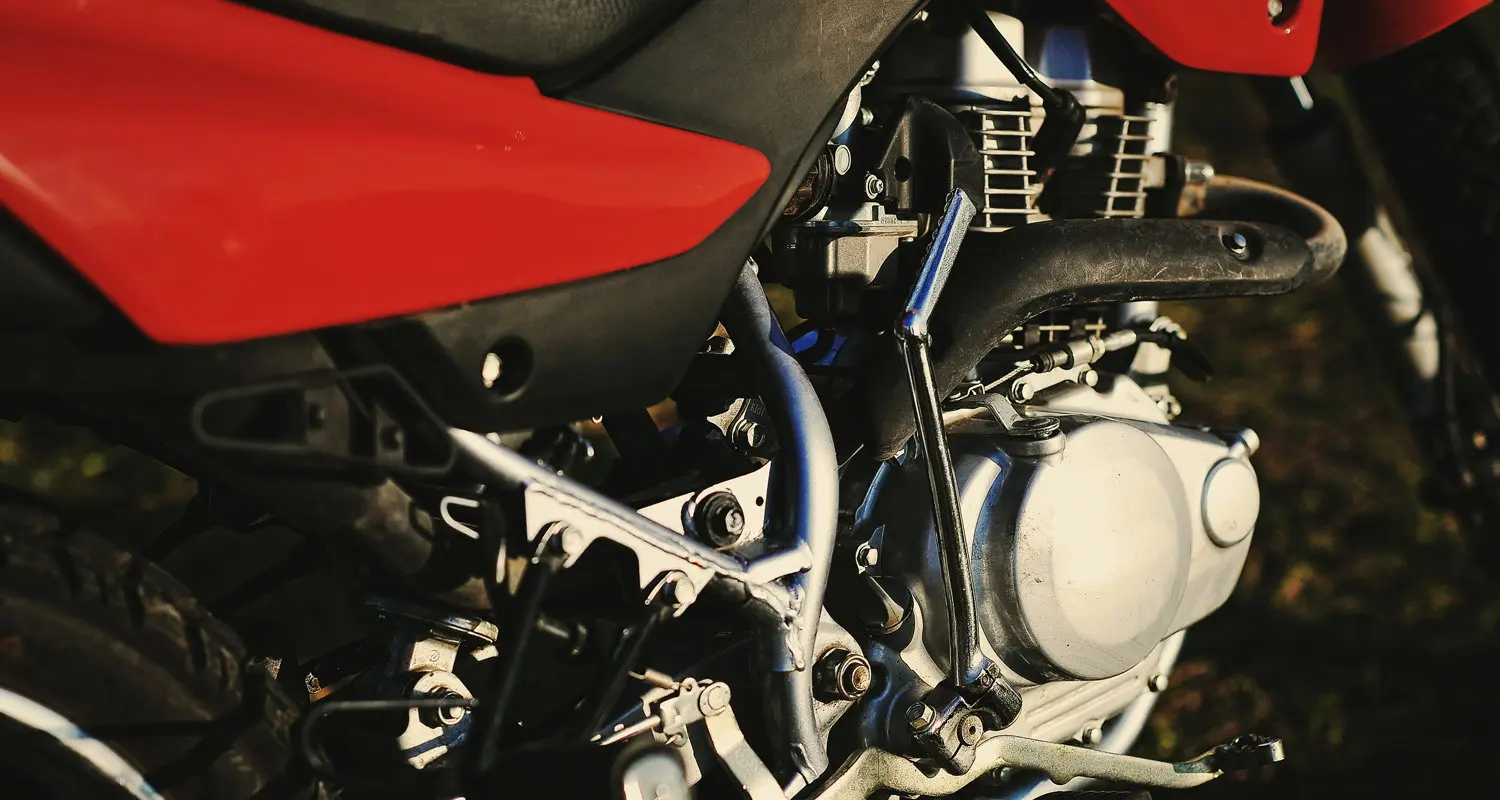
Compact fuel systems require rapid pressure ramp-up within cramped spaces. Miniaturized disc and cylindrical carbon commutators sustain 14,000+ motor RPM without segment shedding.
Explore Motorcycle »
Excavators, wheel loaders, and agricultural tractors operate in severe heat, continuous vibration, and contaminated environments, demanding heavy-duty 24V armatures.
Explore Heavy Duty »
Outboard and inboard motors face salt-air oxidation and fuel condensation. Our corrosion-resistant commutators pass extended salt-spray and condensation cyclic tests without galvanic failure.
Explore Marine »In-depth engineering documentation provided by Hualeao’s research group to support motor designers and fuel system integration specialists.
An oxygen (O2) sensor monitors unburnt oxygen in the exhaust manifold, generating a voltage differential transmitted to the engine ECU. In high-efficiency combustion engines, this sensor maintains closed-loop feedback at the stoichiometric point (λ = 1.00), preventing catalytic converter burnout and reducing hydrocarbon emissions.
Technical Guide »
Submerged fuel pump motors depend entirely on fuel liquid for motor cooling and lubrication. Traditional copper segments dissolve under the acidic action of degraded ethanol blends. Carbon commutators provide a graphite barrier layer that eliminates electrochemical migration, quenches commutator micro-sparks, and maintains stable rotor current without catastrophic brush degradation.
Technical Guide »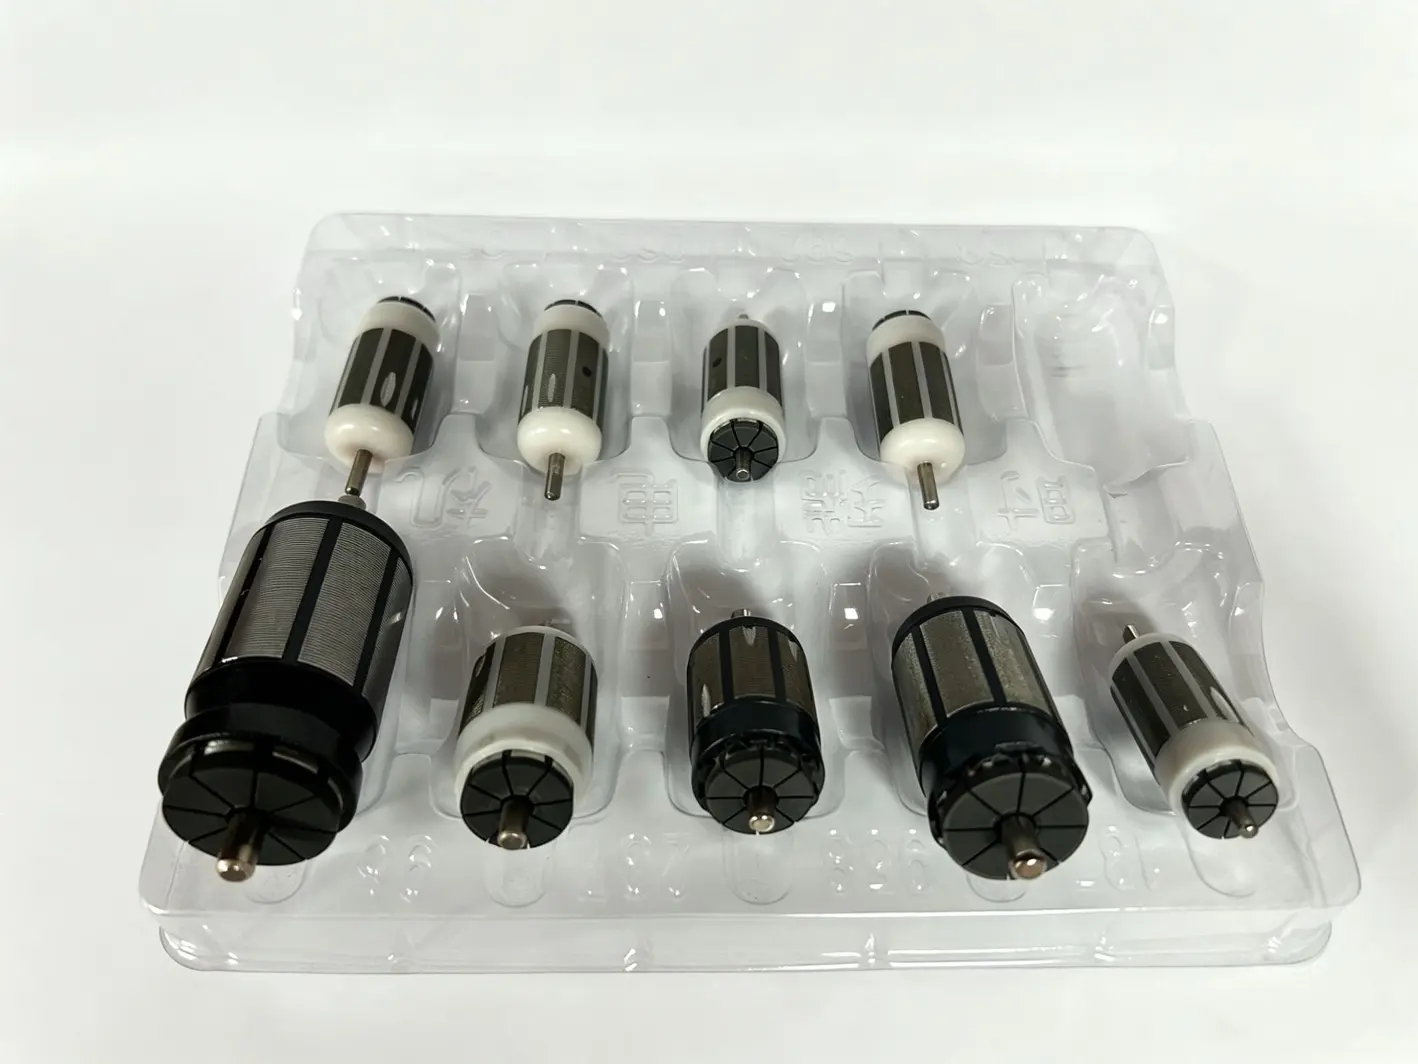
The commutator acts as a mechanical rotary inverter switch. As the armature turns within the permanent magnetic field, the commutator continually reverses winding current at the exact moment of neutral magnetic plane transit. Without high dimensional accuracy and high-temperature dielectric insulation, torque ripple and severe arcing cause premature motor burnout.
Technical Guide »Common technical and commercial questions addressed by our engineering department for global purchasing managers and system engineers.
The carbon commutator acts as the dynamic electrical rotary switch between the stationary carbon brushes and the rotating armature windings. In submerged pumps, the entire motor cavity is filled with pressurized gasoline or alcohol fuel. The carbon commutator transfers DC current while maintaining low mechanical friction and preventing brush contact sparking that could otherwise degrade fuel and wear down segments.
Ethanol and methanol attract moisture and produce organic acids under electrical breakdown. Copper commutator segments subjected to DC voltages in wet alcohol experience severe electrolytic migration, de-alloying, and pitting. Graphite is chemically inert to alcohol and biofuels, forming a resilient transfer film that prevents copper corrosion and extends motor service life beyond 3,000 continuous hours.
Yes. Over 65% of our production consists of customized OEM components. Global clients provide 2D/3D CAD models (STEP, IGES, DWG) or physical OE samples. Our engineering team confirms segment layout, bar-to-hook dimensions, copper substrate thickness, and carbon formulation, completing prototype mold development in 15 to 25 business days.
Our manufacturing facility operates under ISO 9001 and IATF 16949 automotive quality management standards. Our testing equipment includes computerized inter-bar insulation testers (1500V DC flash testing), optical profile projectors (0.001mm resolution), dynamic runout lasers, and fuel immersion durability rigs capable of simulating 1,000 hours of continuous flex-fuel exposure.
Our commutators, fuel pumps, and armatures are deployed across passenger sedans, light commercial trucks, four-stroke and two-stroke motorcycles, agricultural harvesting machinery, diesel common-rail lift units, and marine inboard/outboard systems for both OEM assembly and Tier-1 aftermarket distribution.
Cylindrical commutators feature segments arranged around the circumference of an insulated core, ideal for standard length motors with radial brush holders. Disc-type (planar) commutators feature segments arrayed flat on the axial end face. Disc commutators drastically decrease motor axial length, making them the preferred architecture for compact in-tank motorcycle and automotive fuel modules.
We utilize an engineered mechanical interlocking anchor system combined with thermosetting phenolic molding compound containing high glass-fiber reinforcement. During compression molding, the compound locks into dovetail grooves in the copper-carbon segments. Our commutators are spin-tested up to 25,000 RPM at 150°C without segment shifting or dimensional distortion.
For standard catalog models (including our HC-QZQE-049C series), samples ship within 3 to 5 business days. For customized tooling projects, initial T1 prototype samples are delivered within 20 to 25 calendar days. Mass production lead times generally range from 25 to 35 days depending on batch volume and shipping packaging specifications.
Our slotting depth and undercutting profile are engineered to prevent carbon dust buildup between adjacent copper segments. Additionally, the high arc-resistance of our molding resin matrix ensures inter-bar dielectric resistance exceeds 500 Megaohms even when operating in humid or fuel-washed environments.
You can use the Request a Catalog function on our website or email your target OE reference numbers directly to [email protected]. Our engineering support desk returns complete 2D tolerance drawings, 3D envelope step models, and material specification sheets within 24 business hours.
Explore 8 key product categories manufactured in our Ruian plant with dedicated button links for technical datasheets, CAD models, and quotes.
Designed for space-restricted motor designs, delivering axial brush contact with minimal friction and maximum thermal dispersion.
Standard profile for automotive in-tank fuel pumps, featuring deep undercutting to prevent brush debris tracking.
High-flow internal rotor design engineered to replace OE pumps across Japanese, European, and American vehicle platforms.
Laser-welded stainless housing protecting zirconia ceramic element against thermal shock and lead poisoning.
Automated slot-insulation, precision fly-winding, and fused commutator hook terminations guaranteeing zero open-circuit faults.
Specially synthesized carbon grain structure resistant to swelling, leaching, and chemical breakdown in M85-M100 racing fuels.
Ultra-compact 30mm diameter pump assembly designed for high vibration scooters, sports bikes, and utility quads.
Reinforced copper segments and high-temperature wire insulation engineered for continuous commercial diesel fuel delivery.
Submit your 2D drawings, 3D step files, or target OE part numbers. Our senior engineering staff in Ruian, Wenzhou will verify tolerances, validate fuel media compatibility, and deliver a detailed technical quote within 24 hours.
