
Core Component

Carbon Commutator Series
Advanced carbon-graphite commutators delivering zero spark erosion and extended runtime in high-corrosion fuels.
View SpecificationExplore OEM-certified fuel pump components, precision armatures, and alcohol-tolerant graphite commutator units engineered by Wenzhou Hualeao Automotive Parts Co., Ltd.
Advanced carbon-graphite commutators delivering zero spark erosion and extended runtime in high-corrosion fuels.
View Specification
Complete EFI fuel pump systems and cores balanced with dynamic-micro precision for continuous steady flow.
View Specification
Upstream and downstream zirconia lambda sensors offering millisecond ECU closed-loop fuel compensation feedback.
View Specification
Industry-standard high-run rate carbon commutator recognized globally by top pump remanufacturers.
View Specification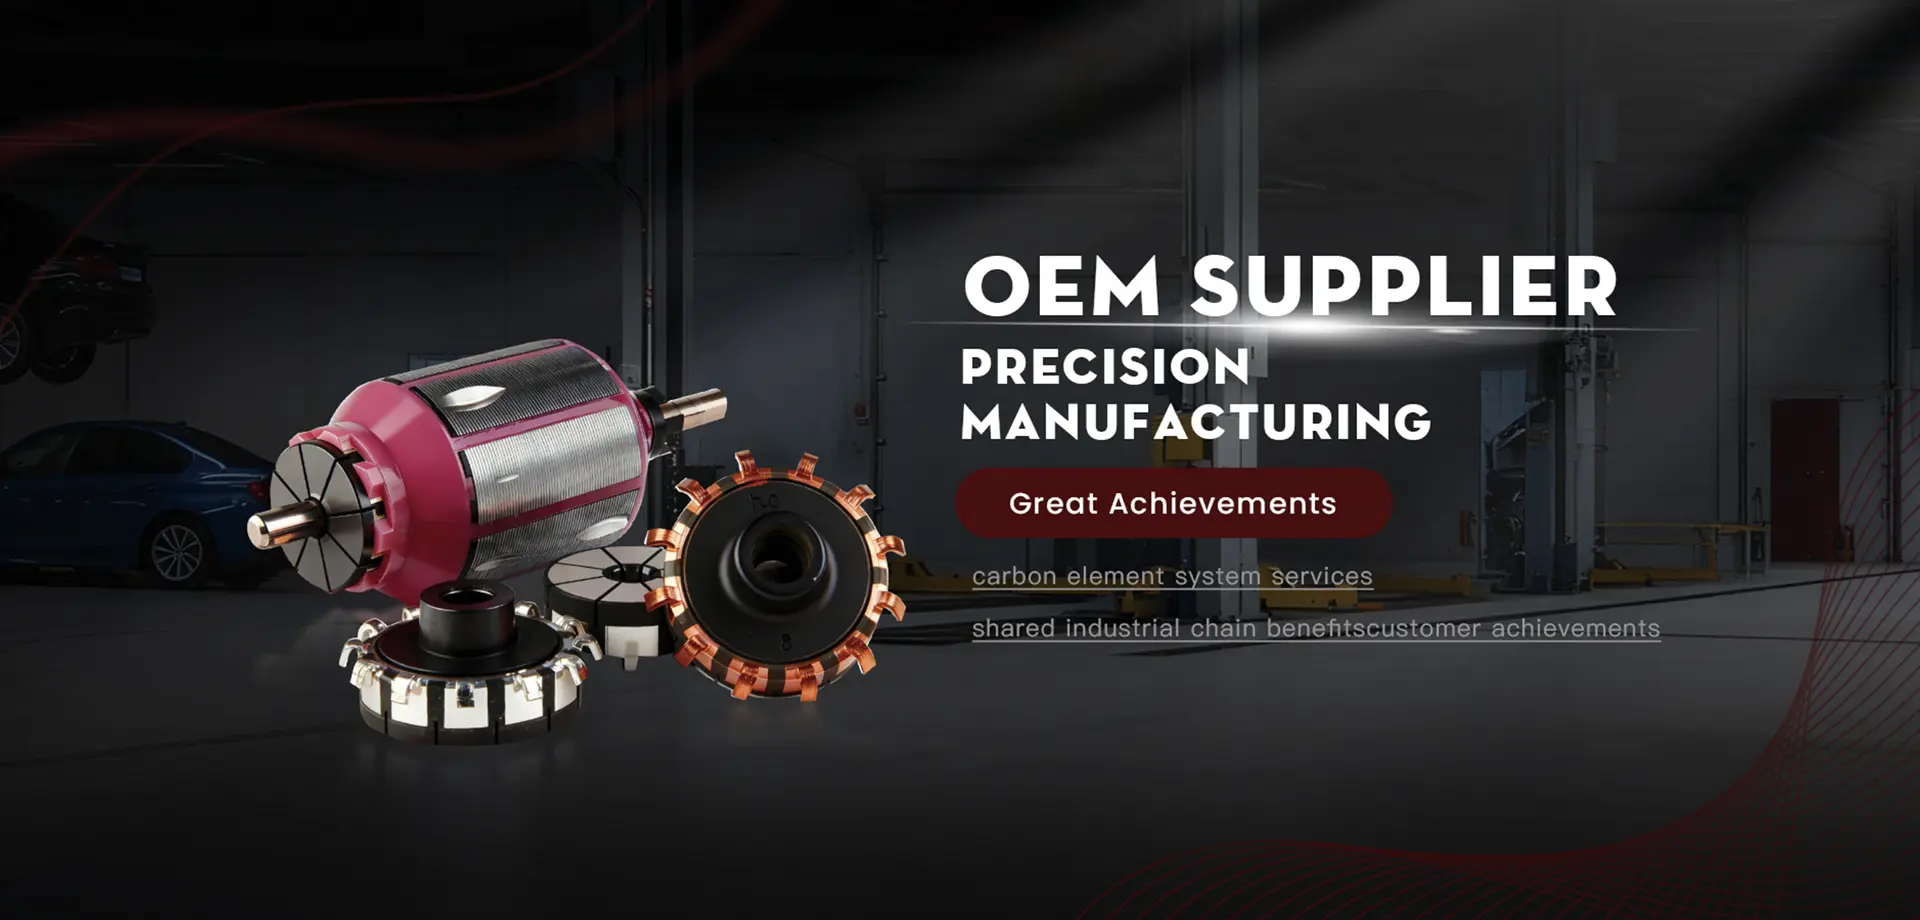
Precision-wound copper wire rotors with high dielectric resin potting to resist aggressive fuel submersion.
View Specification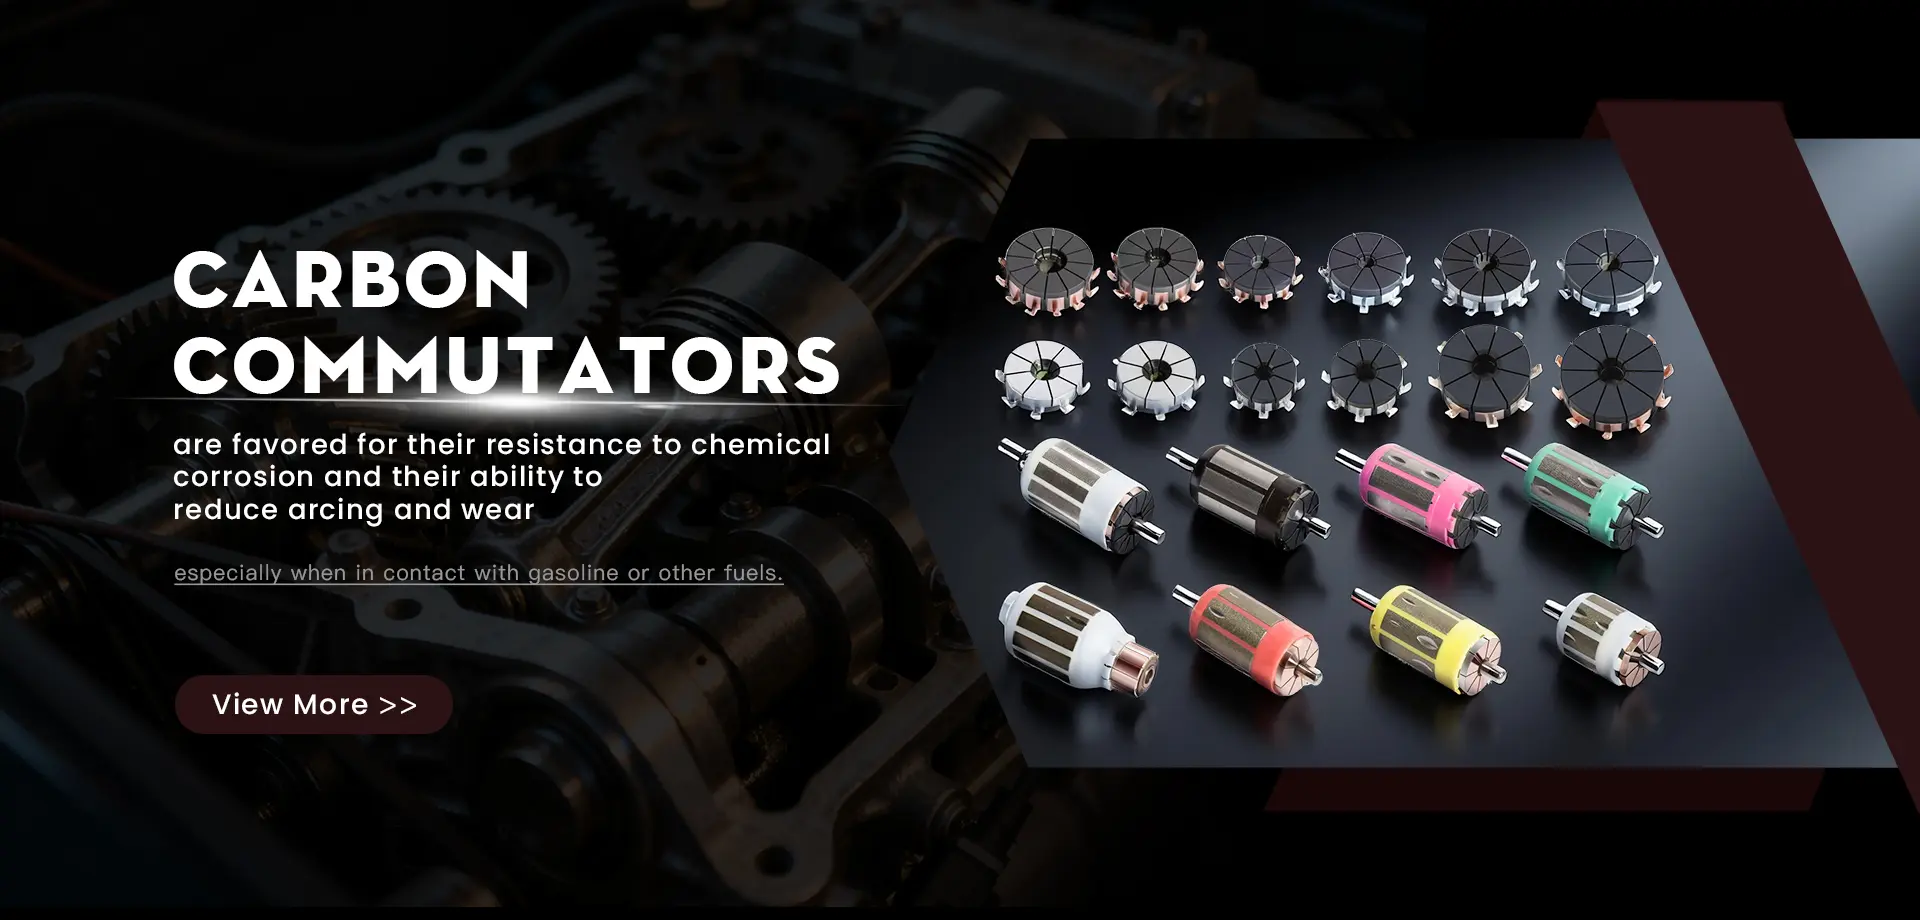
Specifically developed for E85, E100, and methanol applications, overcoming copper de-lamination.
View Specification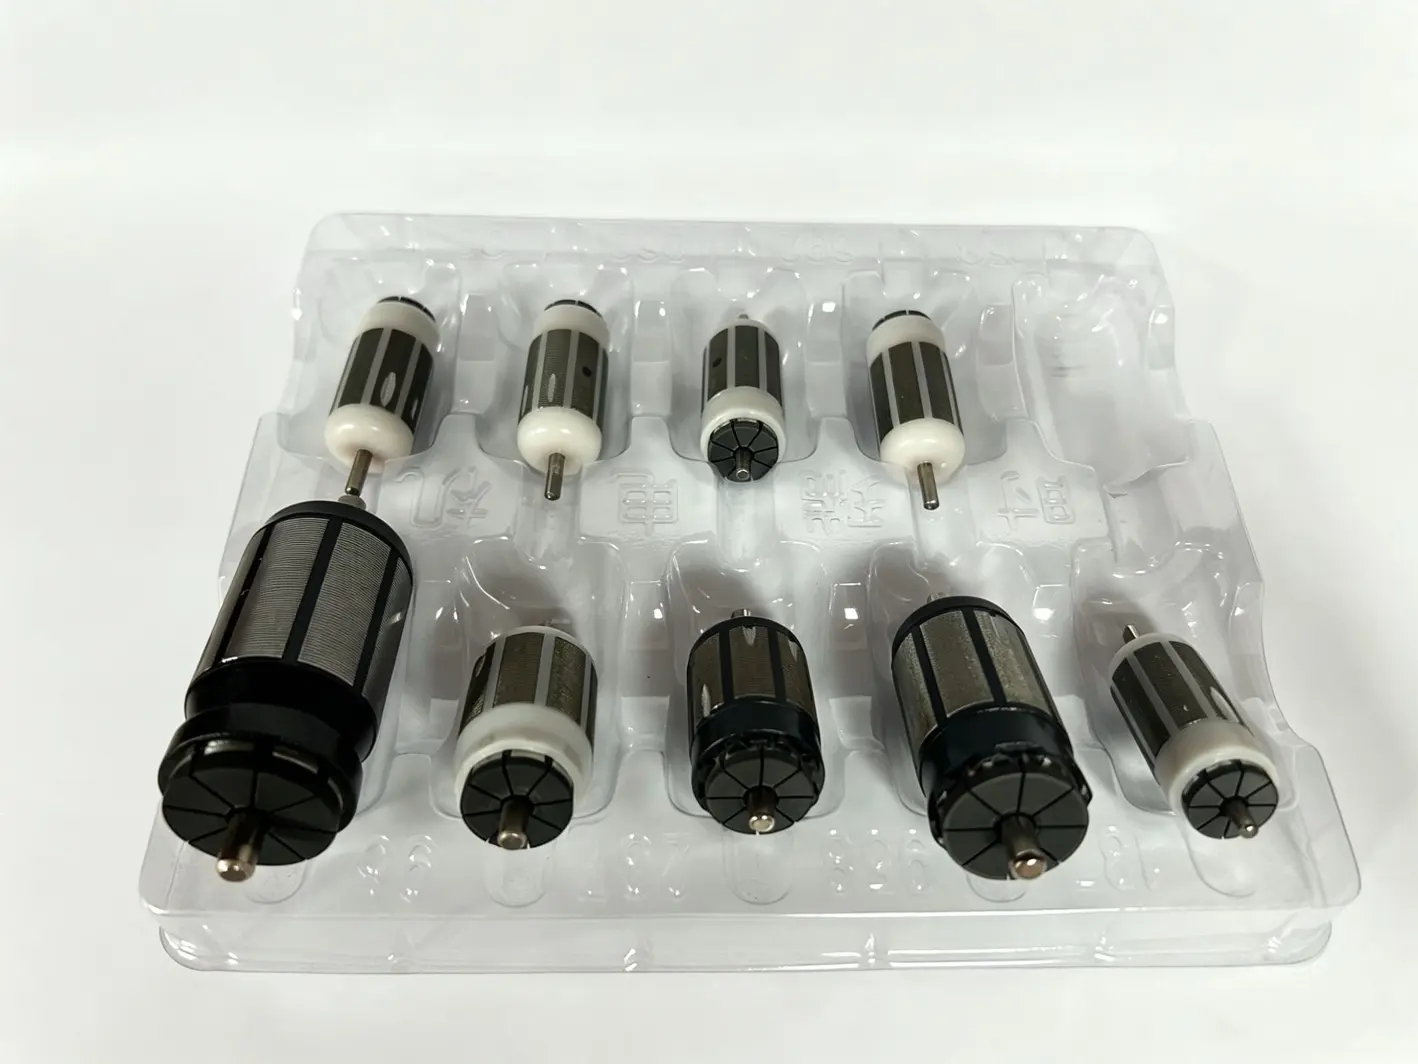
Custom engineered segment counts and hook/groove configurations engineered to custom prints.
View Specification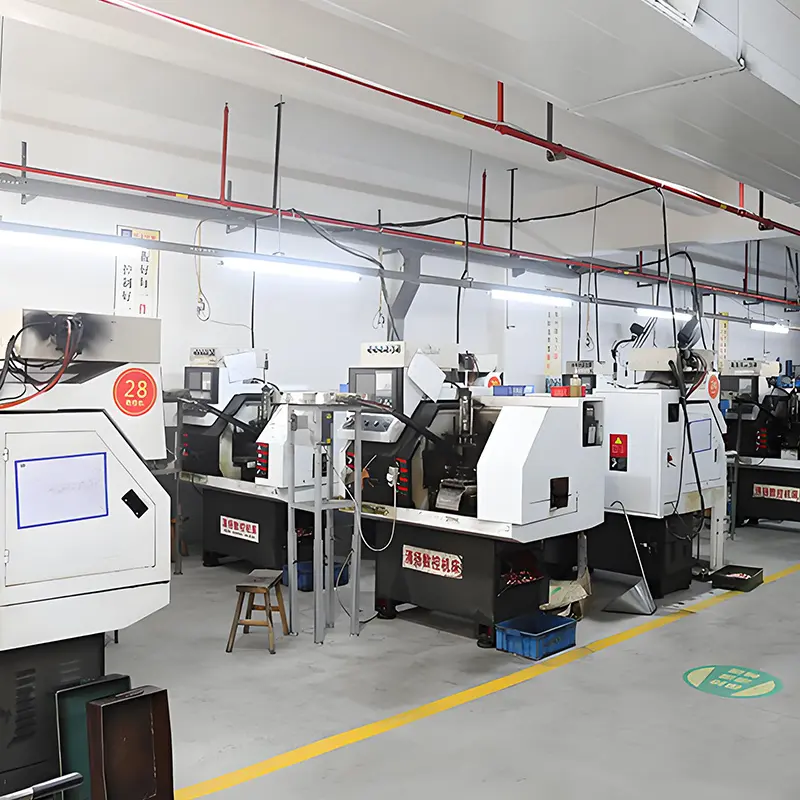
Access our engineering files, complete dimensional tables, and replacement interchange charts.
View SpecificationIn-depth analysis of high-pressure EFI requirements, the global shift toward biofuel blends, and the metallurgical evolution from conventional copper to engineered carbon-graphite segments.
Traditional electric fuel pump rotors relied on copper commutators. However, with global adoption of ethanol-rich fuels (E10 up to E100 flex fuels in Americas and Europe), copper commutators undergo galvanic degradation, spark erosion, and rapid pitting. Carbon-graphite rotor commutators are non-reactive, extending motor lifespan beyond 150,000 miles.
Modern internal combustion and hybrid range-extender engines demand fuel pressure stability between 3.5 to 6.5 bar at high motor speeds exceeding 12,000 RPM. Rotor armatures require dynamic unbalance tolerances within 0.05 g·mm to suppress hydraulic pulsation, decrease in-cabin acoustic vibration, and prevent premature bearing failure.
Submerged fuel pump motors dissipate heat directly into volatile hydrocarbons. Rotor winding coils use ester-imide wire and high-modulus epoxy impregnating resins that maintain structural integrity without outgassing, blistering, or delaminating when continually exposed to fuel additives at -40°C to +85°C.
Wenzhou Hualeao Automotive Parts Co., Ltd. combines advanced European carbon commutator formulations with automated high-speed Chinese stamping and multi-axis winding lines. By maintaining a lean closed-loop ecosystem from raw graphite sintering to computerized testing, we bridge the gap between tier-1 OEM specifications and aftermarket cost structures.
Our facility was recognized as an official National Energy-Saving & Emission Reduction Project under China's 11th Five-Year Plan. Benchmarked continuously against Japanese and German OE benchmarks, we ensure zero compromise on axial runout, dielectric breakdown protection, or contact resistance stability.
Defects cannot be inspected into a product; they must be designed out. Our 4-stage engineering verification protocol guarantees that every fuel pump rotor and commutator meets exact technical thresholds.
Strict spectral and conductivity verification of custom graphite blocks and electrolytic copper substrates. Incoming material lots must pass alcohol immersion durability checks before stamping.
High-precision turning and commutator segment cutting using micro-milling machinery. Segment spacing is calibrated to micron levels to suppress inter-segment micro-arcing.
Computerized tension-controlled multi-pole winding and direct fusion hot-staking. Continuous electrical resistance checking monitors turn-to-turn insulation consistency.
100% computerized runout check, bar-to-bar resistance balance, high-voltage surge impulse test, and full-spectrum dynamic vibration testing prior to protective hermetic packaging.
From high-speed sports motorcycles to off-highway machinery and salt-spray maritime operations, our fuel pump rotors deliver zero-failure reliability.
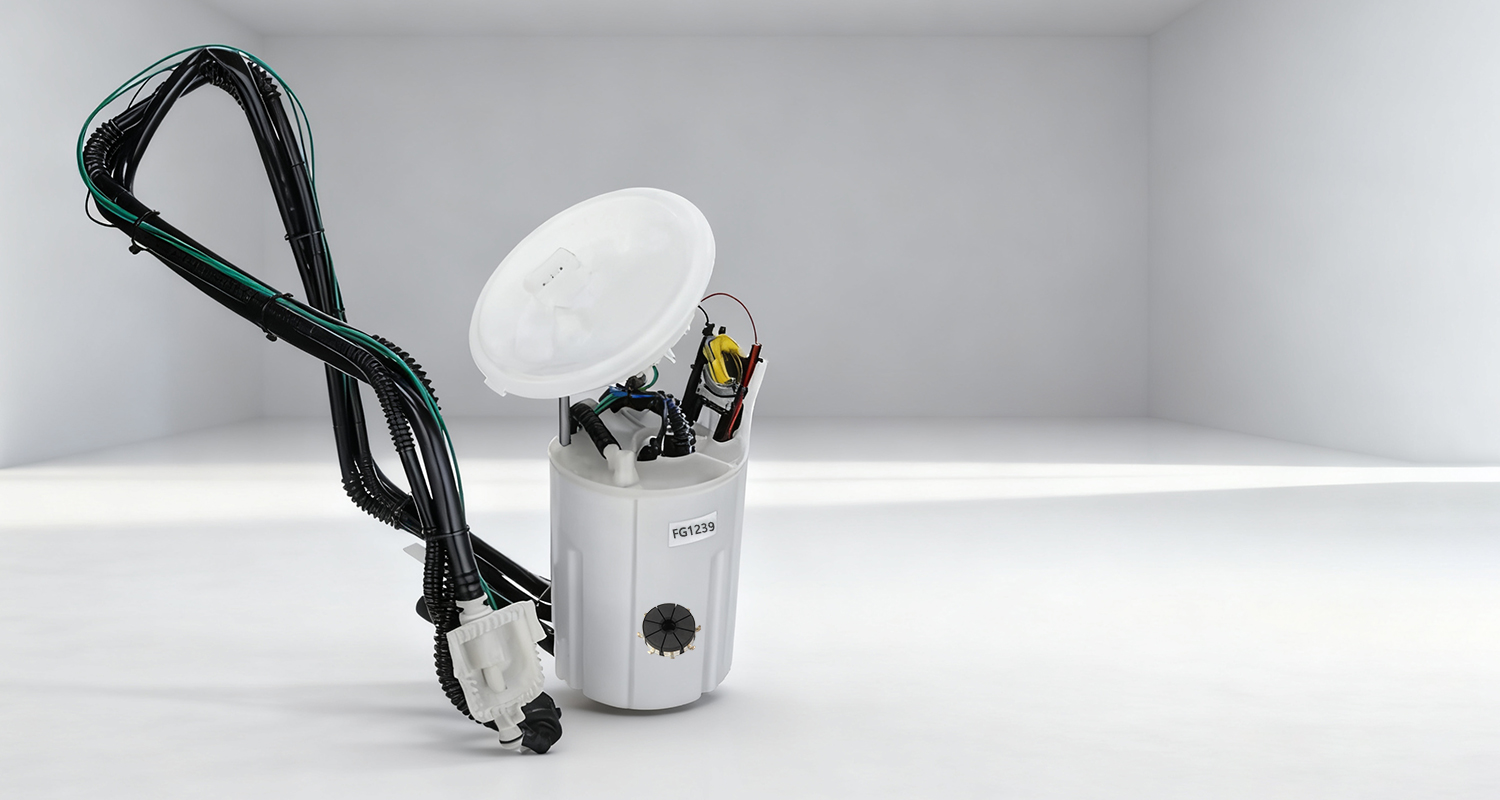
Passenger cars and light commercials using port fuel injection or high-pressure in-tank lift modules running clean or blended fuels.
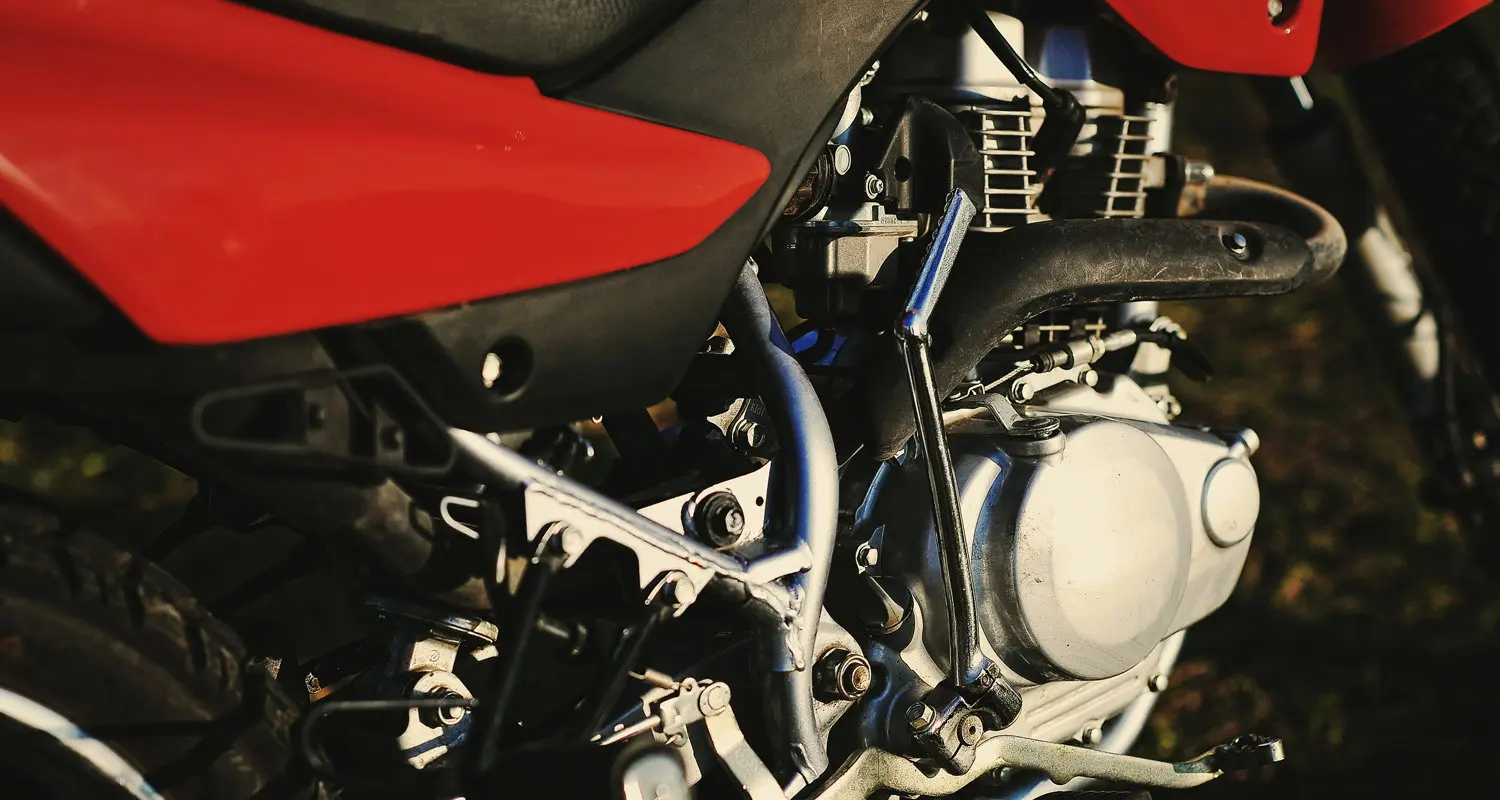
Miniaturized, ultra-compact high RPM rotors engineered to fit restricted tank designs while enduring high vibration.
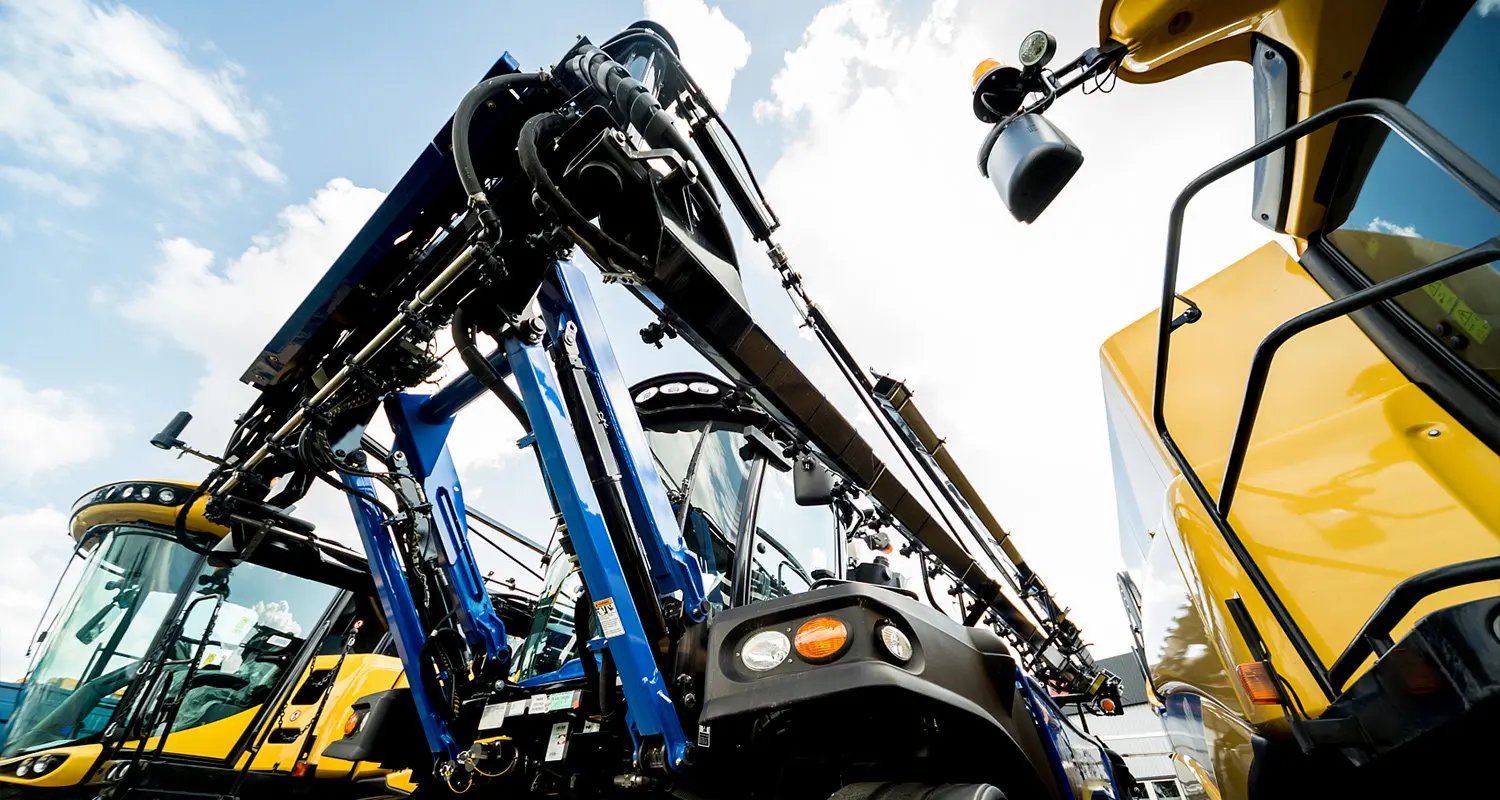
Excavators, tractors, and mining generators operating continuously in severe temperature ranges and high fuel contamination conditions.
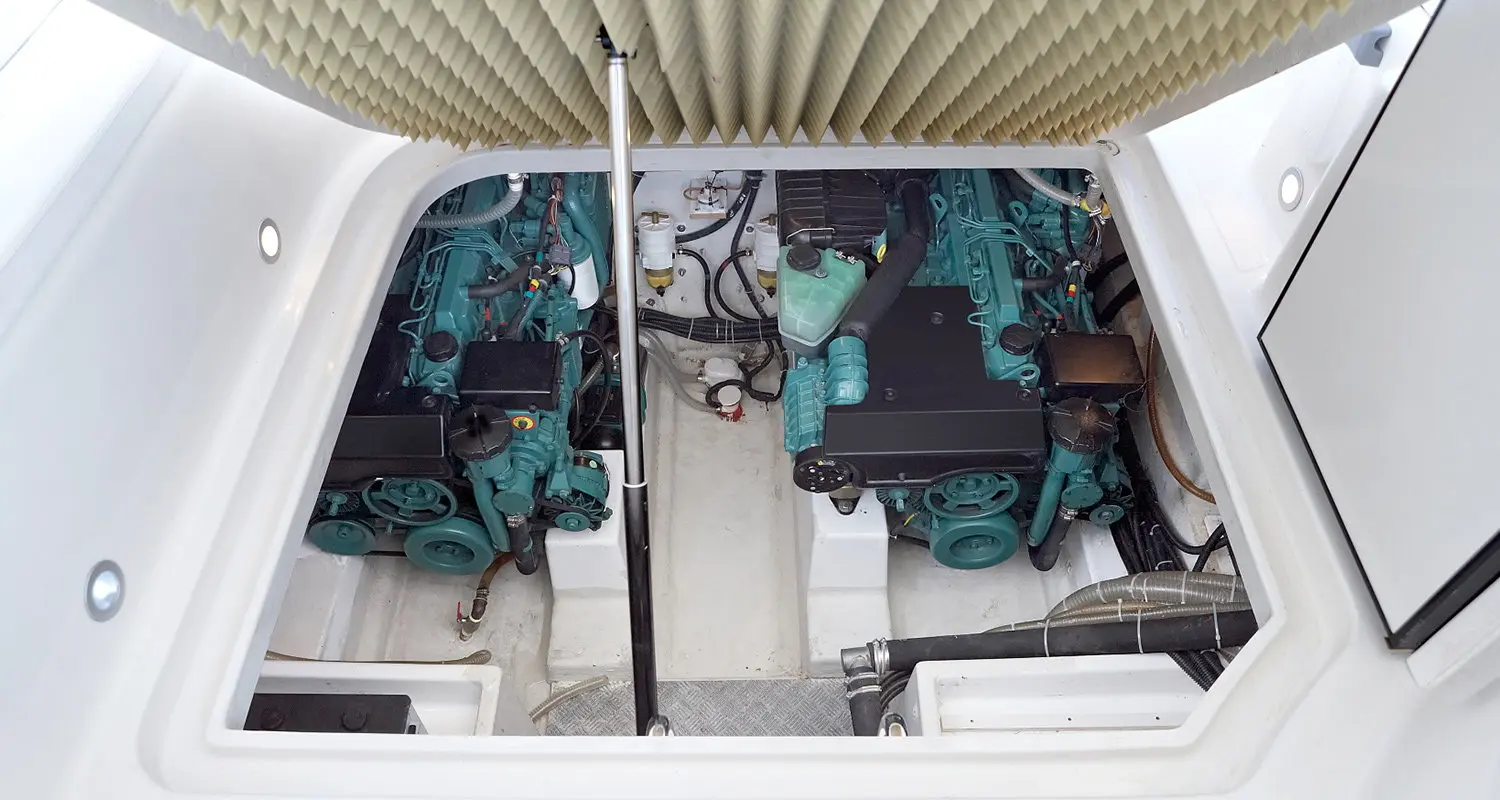
Specialized anti-corrosion barrier coatings protecting against galvanic sea-salt spray and humid watercraft environments.
Explore how precision manufacturing at Wenzhou Hualeao addresses core automotive engineering challenges.
An oxygen (lambda) sensor measures residual post-combustion exhaust oxygen and reports instantaneous millivolt fluctuations to the ECU to safeguard fuel pump delivery and prevent catalytic overheating.
Read Full Technical Paper
Inside submerged DC brush motors, fuel acts as an electrolyte. Learn how carbon-graphite replaces traditional copper segmenting to eliminate sparking, radio interference, and fuel tank degradation.
Read Full Technical Paper
An engineering guide into mechanical polarity switching, brush interface pressure optimization, and how our low-noise armatures minimize electromagnetic field interference (EMI).
Read Full Technical PaperReview our core production models manufactured in our Ruian, Wenzhou facility. Custom dimensions, segment numbers, and hook configurations available on request.
High-density sintered graphite discs for OE assembly and aftermarket remanufacturing programs.
View Specification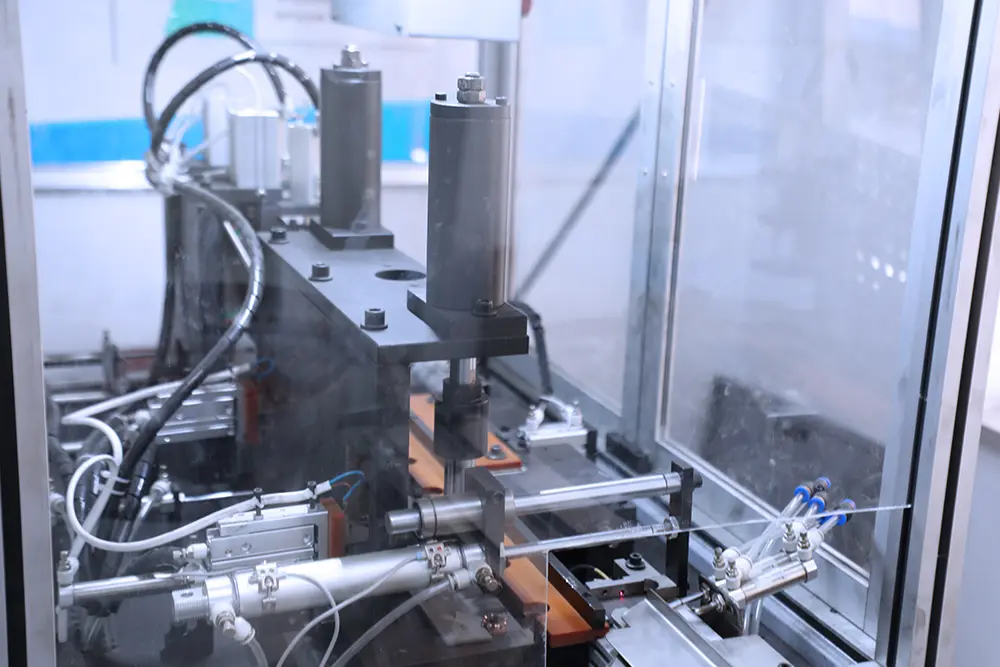
Internal rotor assembly designed for high delivery pressures up to 6.5 bar with quiet operation.
View Specification
Precision-manufactured to client engineering drawings or supplied physical sample components.
View Specification
Rapid warm-up heater element sensors designed for Euro 5 and Euro 6 emission control compliance.
View Specification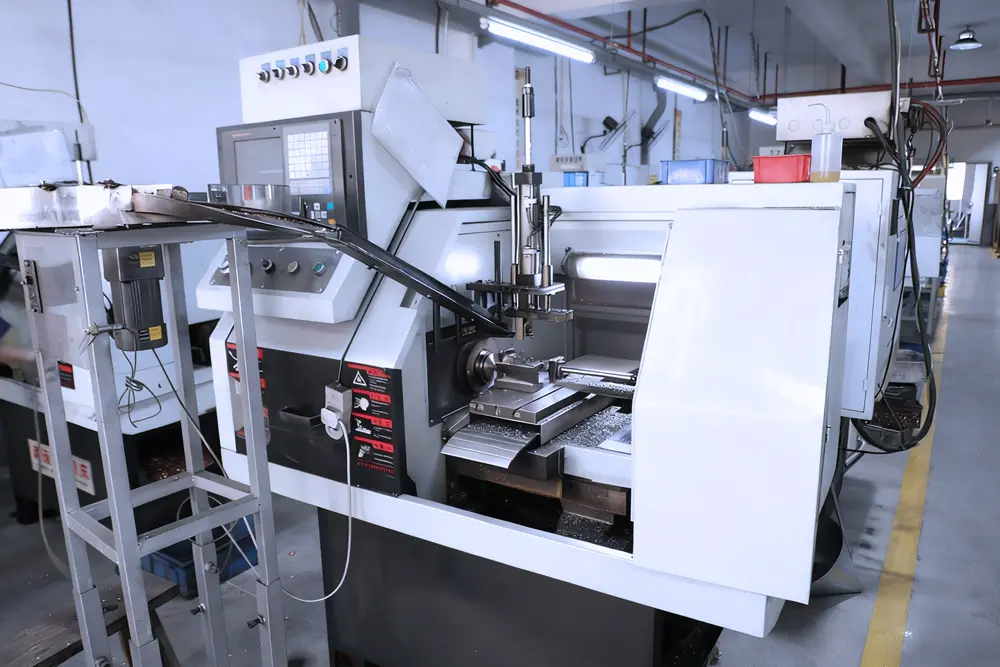
Engineered with high inter-bar breakdown resistance for continuous duty in fleet operations.
View Specification
Fuel supply modules built specifically for high-vibration off-highway and heavy transport usage.
View Specification
Nickel-plated rotor shafts and hermetically treated graphite discs immune to saltwater fog.
View Specification
Direct replacement components packaged for international automotive wholesale distribution.
View SpecificationEssential technical, manufacturing, and logistics details regarding electronic fuel pump rotors and carbon commutators.
The commutator serves as the mechanical rotary switch connecting stationary carbon brushes to the spinning armature coils. It continuously reverses coil current direction so the electromagnetic torque spins the rotor in one direction. Its surface finish, concentricity, and segment conductivity determine motor efficiency, flow stability, and operating lifespan.
Because automotive electric fuel pumps run submerged inside fuel tanks, the fuel acts as a conductor and chemical electrolyte. When exposed to ethanol or methanol blends (such as E20, E85, or M15), copper commutators suffer rapid electrochemical erosion and spark pitting. Carbon (graphite) commutators are chemically inert, eliminate flash sparks, and provide extended service life exceeding standard copper alternatives.
Yes. We offer end-to-end custom engineering. By sharing your 2D/3D CAD drawings (STEP, DWG), OEM part numbers, or physical reference samples, our technical team confirms dimensional tolerances, graphite formulations, and segment configurations to meet your fuel environment specifications.
Our components are widely deployed across passenger car EFI modules, high-displacement powersports motorcycles, heavy-duty construction equipment, agricultural tractors, and marine engines for both OEM lines and global aftermarket replacement networks.
You can request CAD dimensional models or catalog files by navigating directly to our Request a Catalog page, or by emailing our engineering sales desk at [email protected] or messaging WhatsApp: +86 15067763878 with your target part numbers.
Each rotor armature undergoes high-speed dynamic balancing to ISO 1940 G2.5 thresholds (residual unbalance <0.05 g·mm). Dielectric breakdown voltage testing is executed at 1500V AC for 60 seconds with insulation resistance exceeding 500 MΩ, preventing any electrical leakage through the fuel matrix.