

Engineered to exceed OEM standard ISO 9001/IATF 16949 specs. Zero vapor lock, ethanol-resistant armatures, and high volumetric delivery under extreme fuel line thermal stress.



How electrification, alternative fuels, and modern engine architectures are transforming high-pressure inline pump design from mechanical commodity to intelligent fluid dynamics.
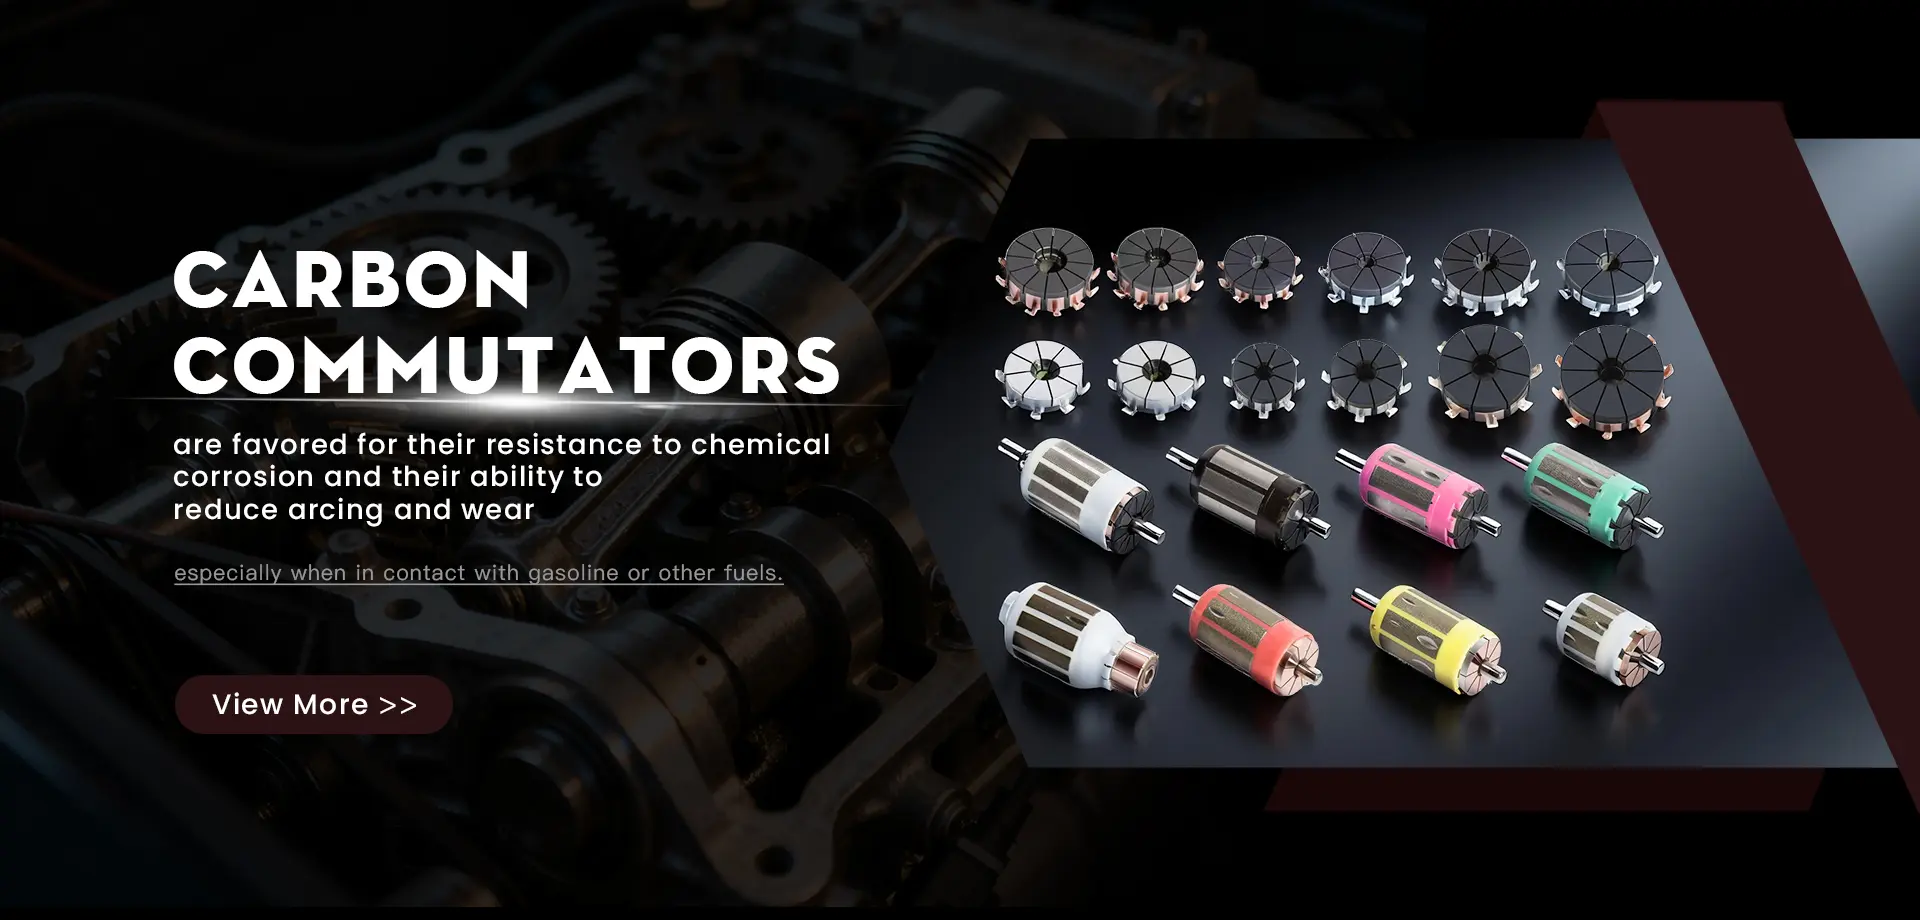
The aggressive adoption of ethanol blends (E10 up to E85) and methanol mixtures in agricultural and automotive markets triggers intense electrochemical galvanic corrosion in conventional copper commutators. Modern inline fuel pump suppliers have completely revolutionized rotor architecture by engineering proprietary carbon-graphite commutators. These assemblies prevent rapid surface oxidation, maintain microscopic surface lubricity, and deliver over 3,000 continuous hours of failure-free operation under aggressive polar solvents.
Unlike in-tank fuel pumps that rely directly on an immense reservoir of fuel for continuous cooling, external inline pumps must dissipate significant motor coil and brush heat independently. Advanced manufacturing integrates aerospace-grade aluminum housings, high-efficiency copper windings, and balanced internal fluid pathways. By balancing volumetric displacement against hydrodynamic resistance, our inline pumps mitigate vapor cavitation even under sustained ambient temperatures exceeding 65°C.
Future emission mandates and hybridization trends demand dynamic variable fuel delivery instead of traditional static flow bypass systems. Integrating digital pulse-width modulation (PWM) ready stators and hardened commutator segments ensures instantaneous throttle pressure response without excessive power consumption, directly supporting hybrid powertrains and performance tuning ecosystems globally.
What Tier-1 system assemblers, international distributors, and performance engine builders demand when qualifying a long-term Chinese manufacturing partner.
Global supply chains demand zero-defect tolerance. Strict statistical process control (CPK > 1.67) and computerized 3D coordinate measuring verify critical segment clearance, runout concentricity, and brush spring tension down to the micron level.
Tier-1 procurement requires rigorous fuel immersion testing. Raw materials undergo multi-thousand-hour cyclic aging tests in synthetic fuels, E100, and methanol to certify zero swelling, no bonding degradation, and uncompromised surface conductivity.
Off-the-shelf catalog models often fall short in specialized applications. Enterprise buyers require responsive prototyping capabilities to fabricate custom commutator geometries, winding resistance, and housing adapters within a 15-day development sprint.
Predictable electrical resistance across 100,000-unit mass productions prevents warranty nightmares. Automated sintering profiles and closed-loop material sorting guarantee unbroken continuity and repeatable fuel rail pressurization curves.
Harnessing the industrial density of Wenzhou Automotive Parts Capital to slash lead times, optimize component economics, and guarantee production scalability.
Situated in Ruian, Wenzhou—China's automotive parts manufacturing epicenter—Wenzhou Hualeao Automotive Parts Co., Ltd. benefits from a dedicated hyper-localized supply network. High-purity electrolytic copper, specialty graphite substrates, precision neodymium magnets, and Viton seals are sourced within a 30-kilometer perimeter, drastically insulating production lines from broader international supply chain shocks.
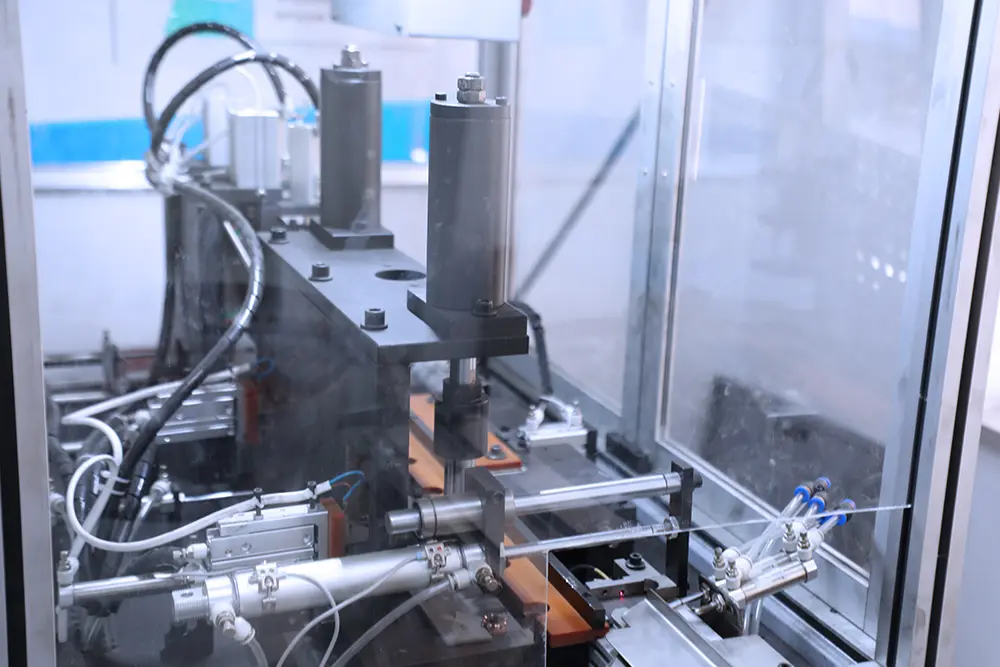
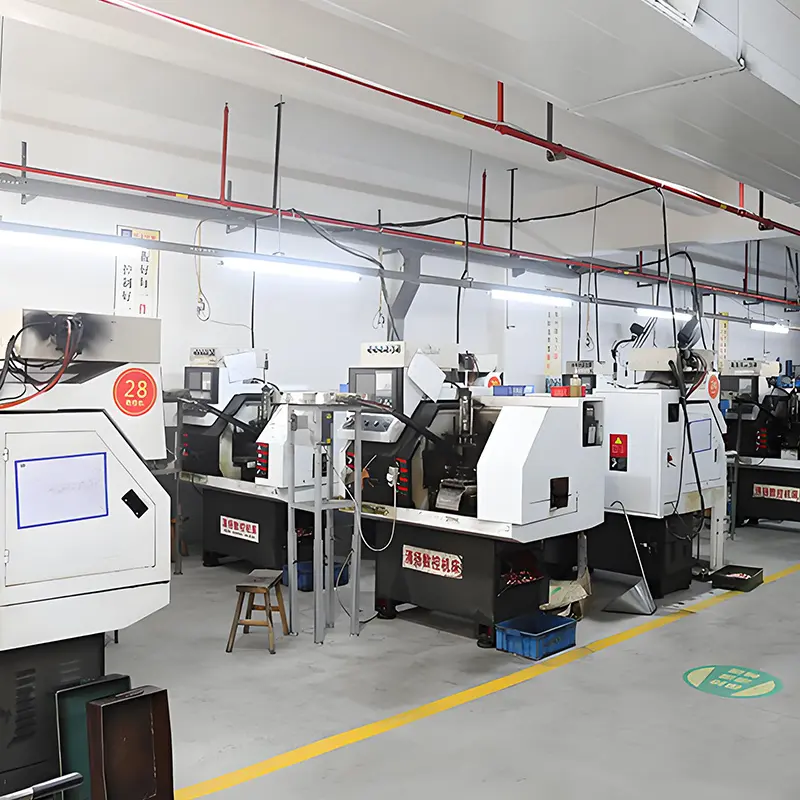
Our workshop integrates advanced multi-station automatic winding machinery, automated hook welding, high-speed balancing centers, and computerized visual surface inspection. By standardizing manufacturing metrics to import-grade international criteria, we deliver equivalent or superior operational longevity compared to legacy German and Japanese brands at a substantially competitive total acquisition cost.
Reflecting our rigorous R&D prowess, Hualeao's low-friction EFI carbon commutator development was designated an official Energy Conservation and Emission Reduction Project under China's 11th Five-Year Plan. This engineering lineage guarantees that our pump assemblies deliver maximum dynamic hydraulic output while consuming minimized electrical wattage from vehicular alternators.
| Technical Parameter | Conventional Copper Commutator Pump | Hualeao Advanced Carbon Matrix Inline Pump | Procurement Advantage |
|---|---|---|---|
| Corrosion Resistance (E85 / M100) | Rapid segment erosion within 400 hrs | Zero erosion / Stable beyond 3,500 hrs | Critical warranty reduction in flex-fuel zones |
| Operating Acoustic Profile | 62 - 68 dB(A) high-frequency whine | < 51 dB(A) balanced fluid dampening | Substantial passenger NVH cabin improvement |
| Dynamic Dynamic Balance | Standard commercial grade (< 0.2g) | Aerospace-grade micron balance (< 0.05g) | Doubles bearing and seal service lifespan |
| Operating Temp Range | -30°C to +80°C | -45°C to +125°C extended duty | Zero vapor-lock failure in desert/extreme duty |
From high-vibration marine outboards to dusty agricultural harvesters, our inline fuel systems are calibrated for absolute mission reliability.
Engineered for seamless inline integration into existing fuel supply systems, secondary booster rails, or standalone injection replacements. Delivers smooth fuel pressure pulses that safeguard injectors and support crisp throttle response across passenger sedans, light trucks, and dual-fuel taxis.
Compact, ultra-lightweight inline pump architectures built to withstand intense centrifugal forces, lean-angle variations, and high-frequency vibrations found in sports superbikes, ATVs, and off-road trail utility vehicles.
Excavators, wheel loaders, and heavy diesel equipment operate in abrasive dust clouds and 24-hour non-stop shifts. Our industrial-grade pump assemblies offer heavy-duty fluid filter screens and fortified thermal insulation against punishing diesel-paraffin viscosities.
Harsh maritime climates inflict relentless galvanic corrosion through saturated saline air. Specially coated outer shells and inert graphite internal matrices protect outboards, speedboats, and trawlers from electrical degradation and sudden open-water stallouts.
A zero-compromise four-stage manufacturing protocol engineered to eradicate in-field failures and preserve long-term brand equity.
Cooperating directly with automotive materials engineering institutes to formulate superior graphite-copper composite ratios matching specialized fuel lubricity parameters and high operating pressures.
Incoming raw copper strips, carbon blocks, and housing alloys undergo spectrometric metallurgical purity validation. Incompatible density or chemical variations are rejected at the factory gate.
High-precision multi-cavity injection molding, automated diamond cutting, and thermal curing deliver smooth segment gaps, eliminating micro-burrs that induce erratic brush arcing.
Every single assembled inline fuel pump undergoes automated dry-run testing, pressure drop analysis, flow volume verification, and dynamic current draw monitoring prior to anti-static packaging.
Comprehensive engineering insights for OEM program managers, global parts wholesalers, and automotive distributors.
An in-tank fuel pump is submerged directly within the vehicle's fuel reservoir, relying heavily on the physical surrounding fluid for constant electric motor cooling and sound dampening. An inline fuel pump is installed externally along the fuel delivery rail or chassis. Inline units require advanced standalone thermal dissipation housings, higher self-priming vacuum capabilities, and superior acoustic decoupling. They offer significantly faster maintenance access and are favored in commercial machinery, dual-fuel conversions, and aftermarket performance enrichment.
Traditional copper commutators experience rapid electrochemical oxidation, spark erosion, and catastrophic segment pitting when exposed to alcohol-blended fuels (ethanol E10–E85, methanol M100). Carbon (graphite) commutators are chemically inert to organic polar solvents, demonstrate lower friction coefficients against the brushes, and maintain uniform electrical transfer without forming insulating copper oxide layers, dramatically tripling pump longevity.
Yes. We provide complete OEM/ODM customized engineering. Our internal R&D team can analyze your 2D/3D CAD blueprints, physical OEM samples, or reference cross-codes (Bosch, Denso, Walbro equivalents). We determine optimal segment geometry, shaft diameters, winding density, and outer casing dimensions to match your exact flow volume and pressure envelope.
Vapor lock occurs when high localized temperatures vaporize fuel before pressurized intake. Hualeao utilizes precision-machined roller-vane and turbine impellers with strict radial tolerances, minimizing internal fluid slippage and recirculation heating. Furthermore, 100% of pump cores undergo dynamic fluid flow pressure testing at elevated temperatures to ensure stable volumetric delivery up to 6.5 Bar.
You can contact our sales engineering division via our Request a Catalog portal or email our direct team at [email protected]. We provide comprehensive parametric tables, cross-reference matrices, CAD envelope drawings, and bulk FOB/CIF quotation schedules within 24 business hours.
Explore our complete export line tailored for high-volume automotive aftermarket replacement, fleet refurbishment, and industrial equipment manufacturing.
Send your part numbers, OEM cross-references, or 3D technical CAD drawings directly to our engineering department in Ruian, Wenzhou. Benefit from factory-direct pricing, certified quality management, and rapid worldwide fulfillment.