Direct supply from China's dedicated specialized manufacturing facility in Ruian, Wenzhou. Fully tested for chemical resistance, high dynamic balance, and extended service cycles.

Planar graphite contact surface configured for submersed micro-motors with ultra-low galvanic reaction.

Industry-standard replacement and OEM component featuring specialized tin-plated lead frame tabs.

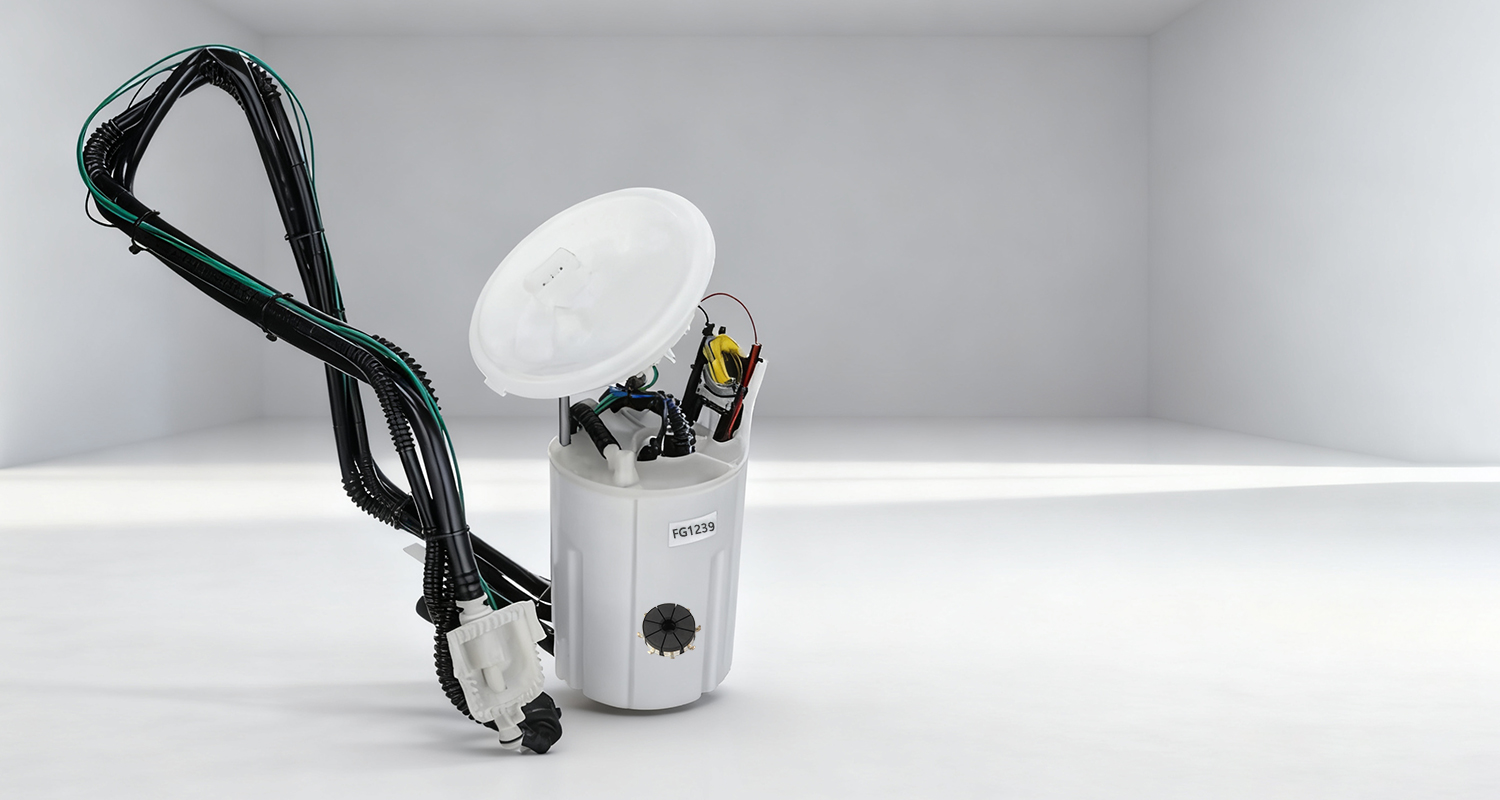
Complete direct-fit electronic fuel delivery pump built around dynamically balanced carbon-commutated rotors.

Precision zirconia element delivering ultra-fast stoichiometric feedback to vehicle powertrain control units.
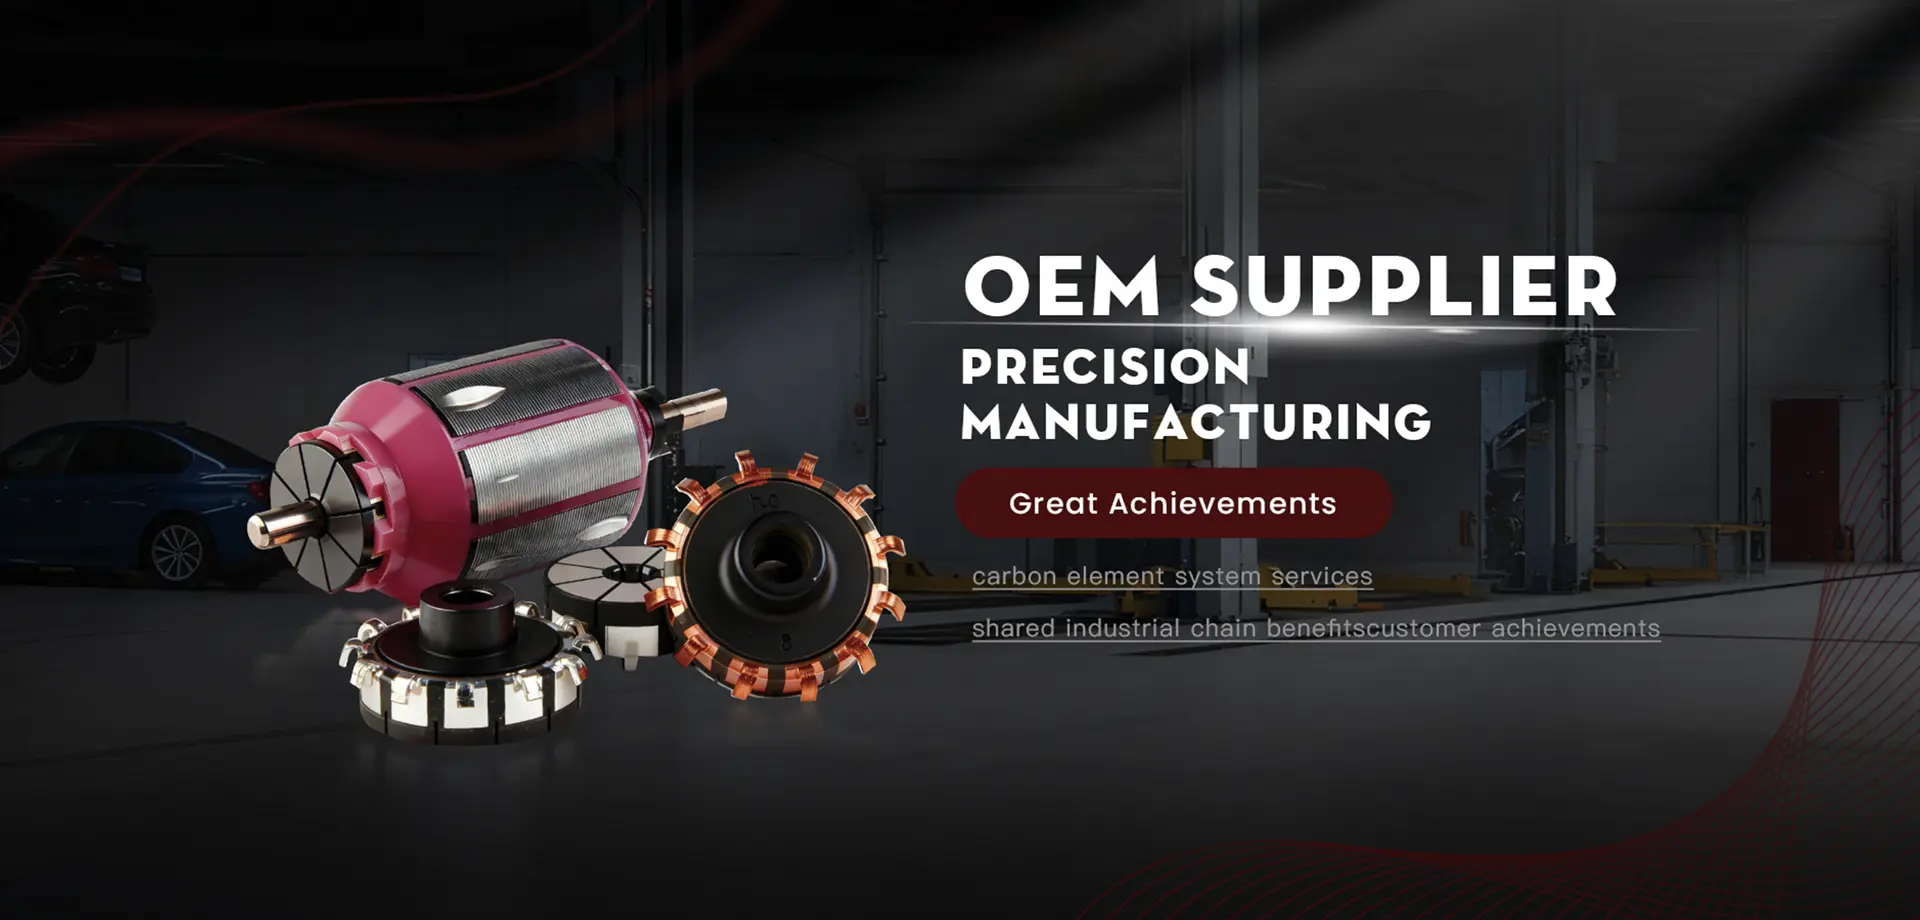
Wound rotor assembly incorporating low-inertia silicon steel laminations and press-fit tin-plated carbon segments.
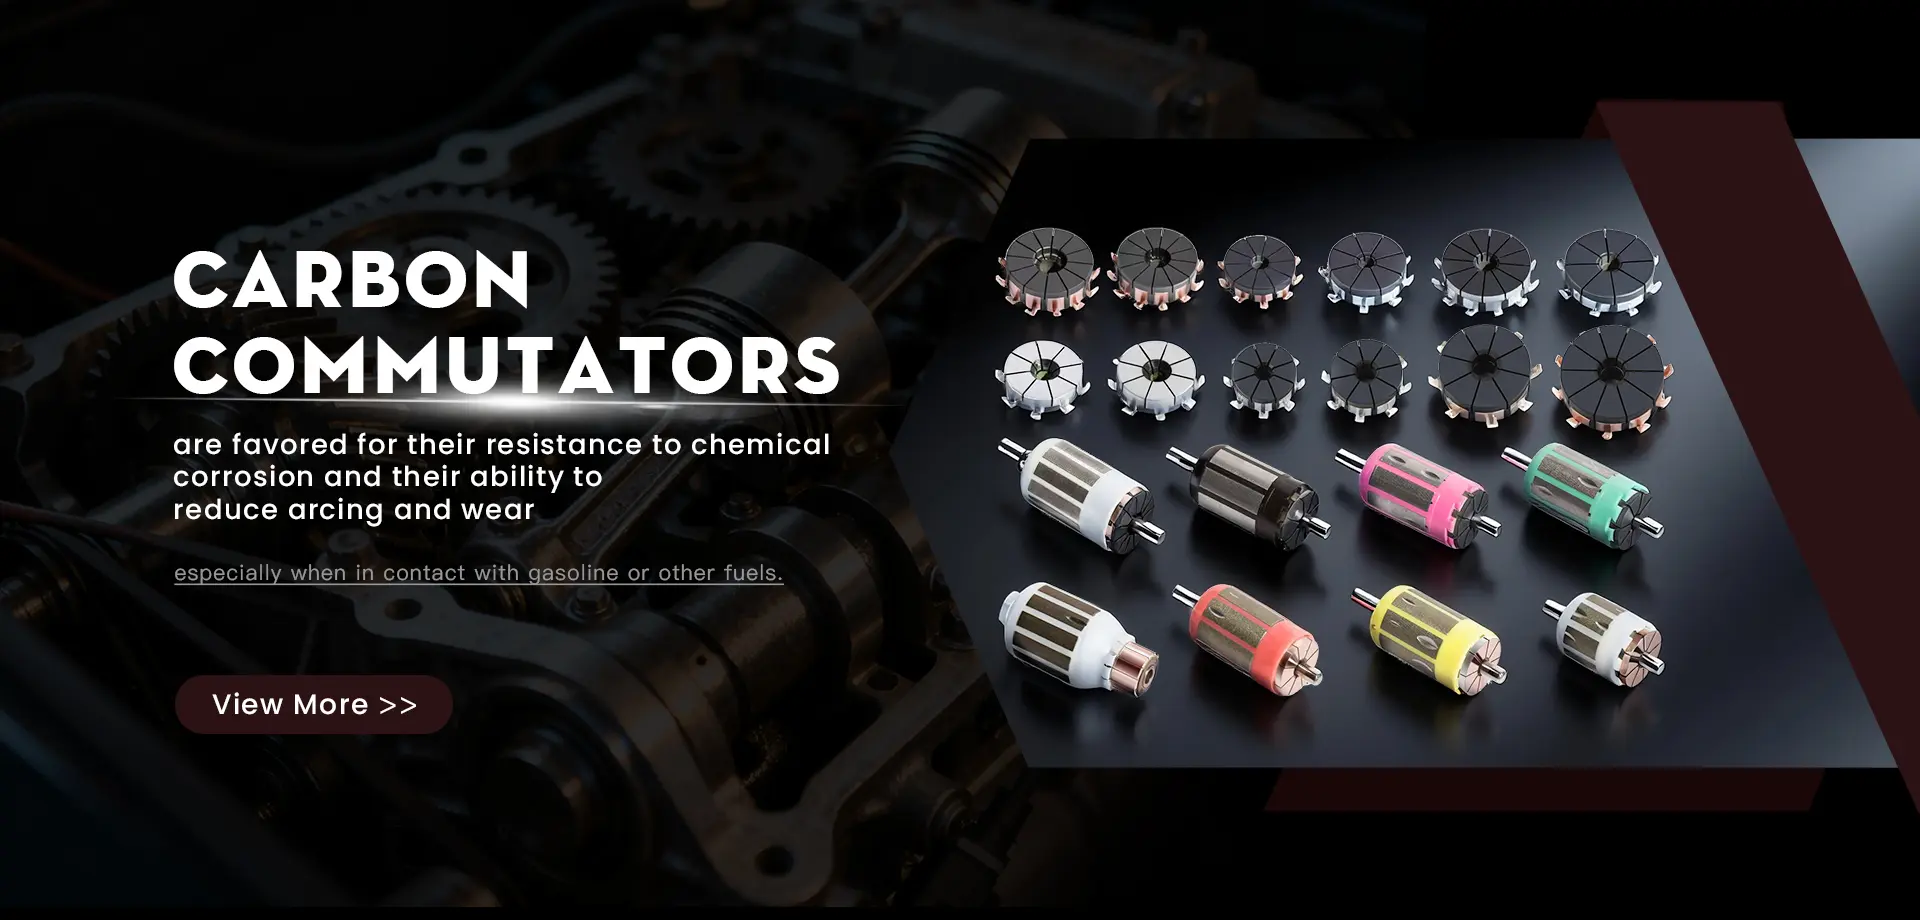
Custom-engineered synthetic resin barrier prevents delamination and swelling in aggressive M85-M100 fuels.
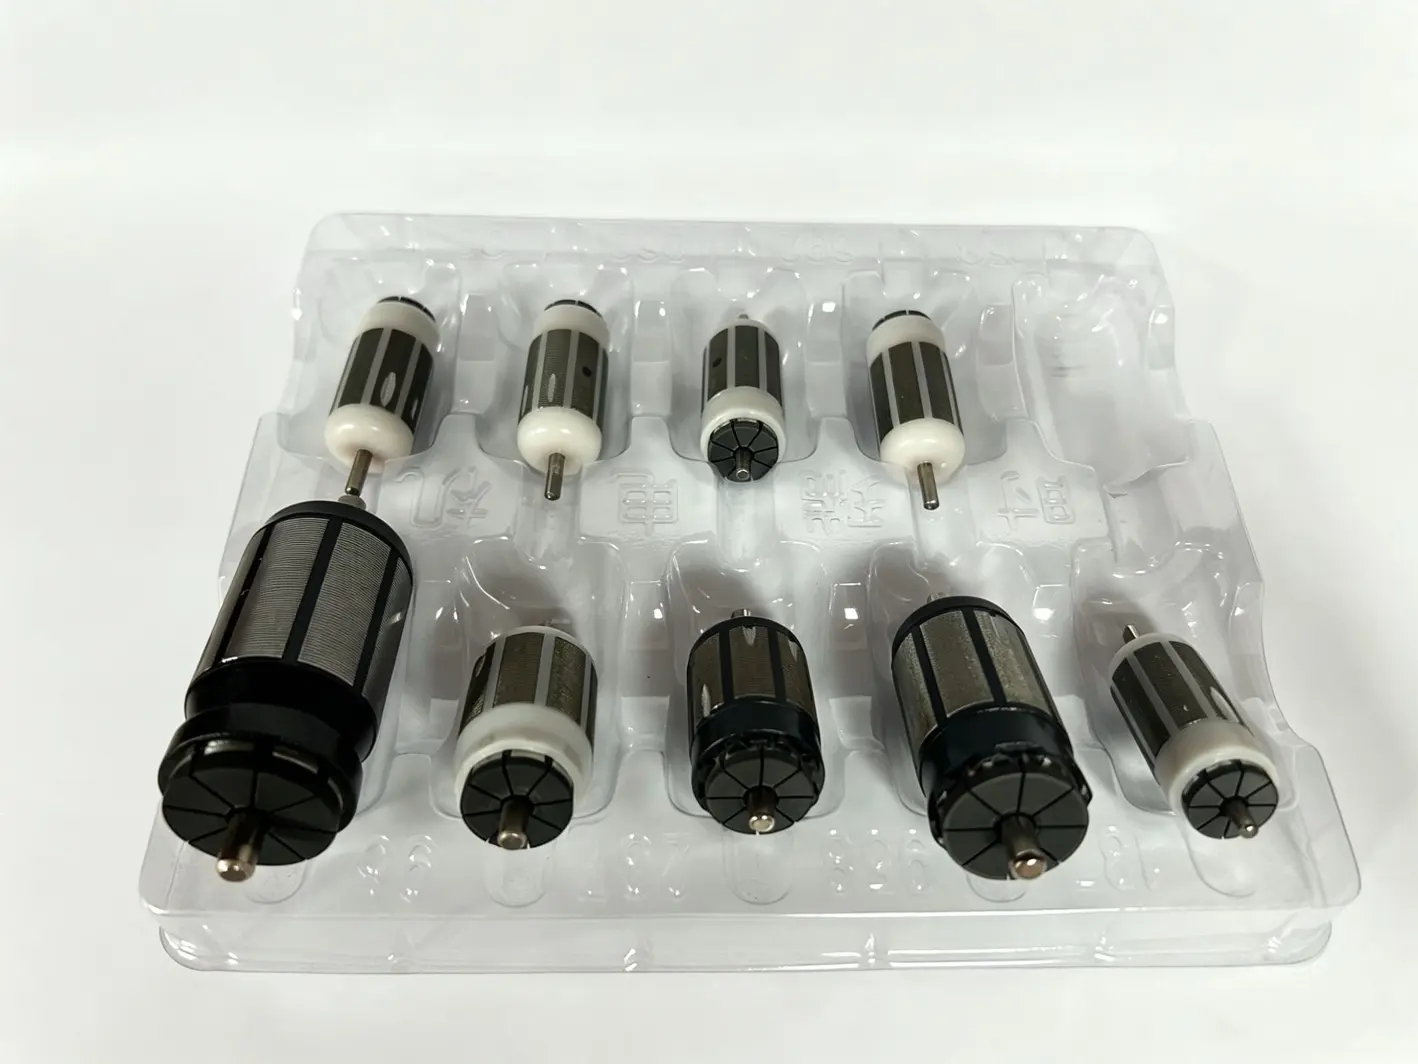
Reinforced mechanical anchoring tabs designed for heavy excavators, harvesters, and high-vibration applications.
Custom multi-segment layout tailored to your specific armature slot count, brush footprint, and current ratings.
Addressing the fundamental electro-mechanical challenges of modern fuel systems: bio-alcohol degradation, terminal oxidation, and galvanic contact corrosion.
In modern internal combustion engines (ICE) and hybrid electric vehicle (PHEV/EREV) auxiliary systems, the electric fuel pump operates submersed entirely within the fuel tank. This "wet motor" design relies on the surrounding fuel for fluid hydrodynamic cooling and continuous brush lubrication. However, the introduction of mandate-driven bio-fuels—such as gasohol blends (E10, E20, E85) and methanol formulations (M15 to M100)—has profoundly exacerbated commutator wear mechanisms. Under such corrosive, highly conductive, and moisture-attracting fluid dynamics, traditional all-copper commutators succumb rapidly to intermetallic erosion, copper dissolution, and accelerated segment groove short-circuiting.
Core Metallurgical Breakthrough: Wenzhou Hualeao Automotive Parts Co., Ltd. resolves this industrial roadblock by synthesizing a specialized carbon-graphite rubbing surface with an advanced electrolytic tin-plated copper core. The tin plating provides a robust diffusion barrier, preventing moisture and alcohol ions from triggering galvanic oxidation at the copper-to-carbon and copper-to-winding mechanical interfaces.
The interface between the copper substrate (which anchors the armature windings via crimping, hot-stacking, or TIG welding) and the carbon segment contact area represents a classical dissimilar-material junction. Without specialized tin plating:
| Engineering Attribute | Traditional Pure Copper Commutator | Standard Carbon Commutator | Hualeao Tin-Plated Carbon Commutator |
|---|---|---|---|
| E85 / M85 Chemical Resistance | Very Poor (< 400 hrs; rapid etching) | Moderate (Carbon stable, copper tangs oxidize) | Exceptional (> 3,500 hrs; zero degradation) |
| Electrical Contact Voltage Drop | 0.2 - 0.4 V (Low initially, spikes when corroded) | 0.8 - 1.2 V (Stable throughout lifespan) | 0.7 - 0.9 V (Optimized current density transfer) |
| Brush Wear Rate (μm / 100 hrs) | 12.5 μm (High abrasive spark erosion) | 3.2 μm (Low, self-lubricating graphite film) | 1.8 μm (Super-fine surface finish ≤ Ra 0.2μm) |
| Tang Solderability Shelf Life | 3 Months (Prone to cuprous oxidation) | 6 Months | > 24 Months (MIL-STD-202G Method 208 compliant) |
| Total Dynamic Runout (T.I.R.) | ≤ 0.006 mm | ≤ 0.005 mm | ≤ 0.003 mm (Precision diamond turned) |
Why Tier-1 automotive manufacturers and electric pump assemblers are migrating strategic commutator procurement to specialized Chinese manufacturing centers.
Historically, high-tier fuel pump manufacturers in North America and Western Europe depended exclusively on a limited oligopoly of Japanese and German carbon commutator suppliers. This resulted in excessive tooling premiums, 20+ week lead times, and inflexible supply terms. Wenzhou Hualeao Automotive Parts Co., Ltd. has disrupted this paradigm by reverse-engineering European standard DIN tolerances and Japanese sintering methods, delivering identical or superior tribological longevity at a 30-45% competitive cost reduction.
Contrary to misconceptions that battery electric vehicles (BEVs) eliminate fuel pump demand, the explosive worldwide expansion of Plug-in Hybrid Electric Vehicles (PHEV) and Extended-Range Electric Vehicles (EREVs)—spearheaded by automotive giants across Asia and the Americas—has actually intensified commutator technical benchmarks. Fuel in PHEV pressurized tanks remains stagnant for longer intervals, generating high peroxide acidities that severely erode substandard commutators. Hualeao's tin-plated carbon components are engineered specifically to survive this corrosive "stagnant-fuel" phenomenon.
With an integrated industrial ecosystem centered in Ruian, Wenzhou—the automotive component capital of China—Hualeao offers an accelerated design-to-production lifecycle. While Western competitors require 6 to 9 months for customized disc or segment commutator tooling, our automated tooling department completes sample tooling, mold flow simulation, and 100-piece pilot batches within 15 to 25 business days, fully supported by ISO/TS traceability data.
Rooted in China's 11th Five-Year Plan national science and technology initiatives. Verified manufacturing metrics, precision laboratories, and rigorous international quality certification.
At Wenzhou Hualeao Automotive Parts Co., Ltd., zero-defect manufacturing is not an aspirational slogan—it is an automated, statistical process control (SPC) reality. Our carbon commutators are subjected to comprehensive 100% automated optical inspections (AOI) to verify segment spacing, surface flatness, and segment-to-segment undercut profiles.
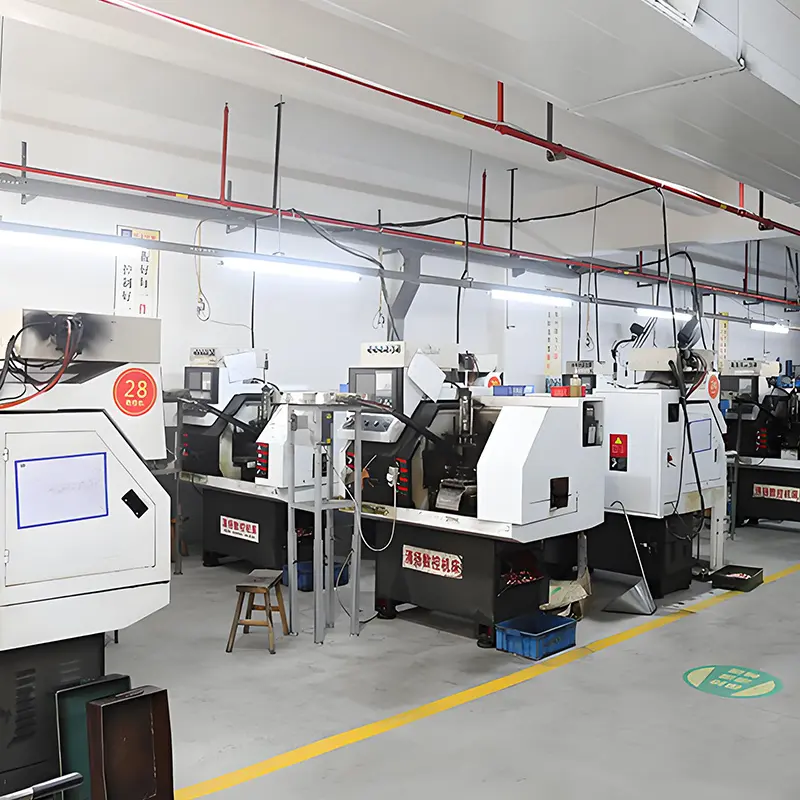
Multi-zone controlled atmosphere sintering furnaces ensuring uniform graphite crystal density.
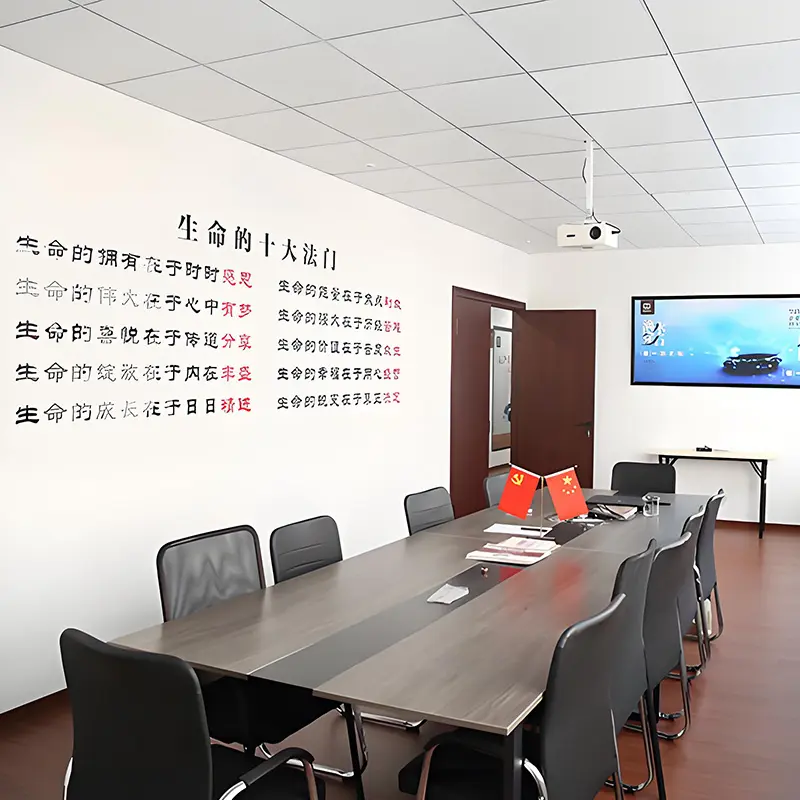
Class-100,000 clean assembly suites minimizing microscopic particulate contamination on commutator faces.
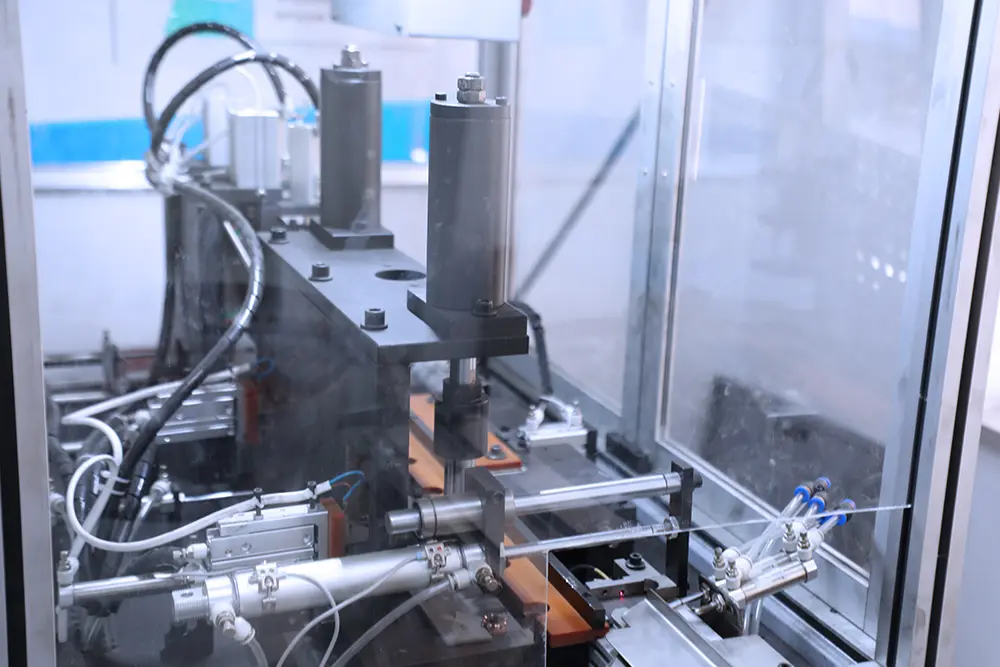
Incoming spectroscopic checks on copper purity (99.95% electrolytic) and specific resin-binder ratios.
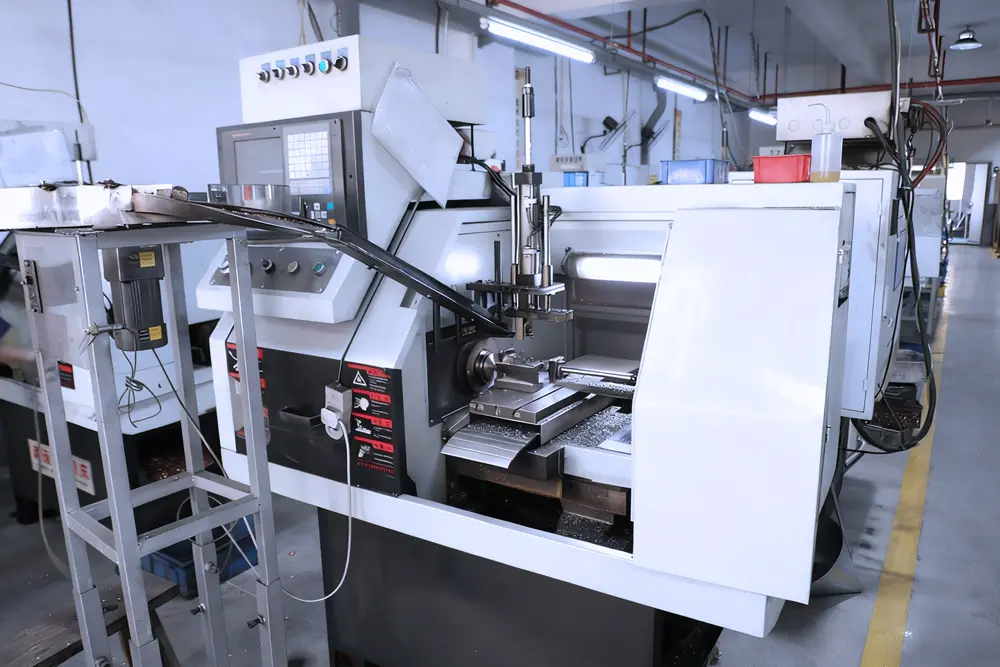
Automated non-contact laser displacement sensors confirming true geometric roundness and planar alignment.
From extreme tropical humidity to arctic cold starts, Hualeao tin-plated carbon commutators sustain uncompromised fuel delivery across four major industrial sectors.
Modern direct-injection (GDI) and port fuel injection (PFI) engines require ultra-stable electrical current transfer to maintain target rail pressures. In hybrid powertrains, frequent engine restart cycles demand instant peak motor torque without commutator contact glazing.
Explore Auto CommutatorsTwo-wheel and recreational all-terrain vehicles feature extremely compact fuel reservoirs and high operating RPMs (> 9,000 RPM). Our miniaturized disc carbon commutators eliminate brush chatter, arc ablation, and localized heating within confined, low-ventilation pump casings.
View Powersport UnitsExcavators, mining haulers, and agricultural tractors experience high shock loads, severe dust, and diesel-fuel bio-additives. Our tin-plated hook commutators withstand heavy mechanical shear forces, preventing terminal fracture under non-stop 24-hour job site duty cycles.
Off-Highway SolutionsMarine fuel modules must contend with severe electrolytic salt-spray condensation inside fuel tanks. Hualeao’s dual-layer tin passivation inhibits chloride pitting on copper brackets, ensuring reliable propulsion and emergency restart readiness out at sea.
Marine Component DataEnsuring complete operational alignment with European Union RoHS, REACH, US EPA tier emissions, and stringent automotive OEM quality warranties.
All tin-plating baths operated by Wenzhou Hualeao are 100% lead-free, cadmium-free, and compliant with EU Directive 2011/65/EU and Regulation (EC) No 1907/2006. We utilize pure matte tin plating processes with proprietary anti-whisker grain refinement chemistry, fully certified by independent third-party laboratories (SGS / Intertek).
For Tier-1 automotive sourcing programs, we supply full Production Part Approval Process (PPAP) Level 3 documentation, comprising design FMEA, process control plans, gauge repeatability and reproducibility (GR&R) studies, and complete material registration into the International Material Data System (IMDS).
To support high-velocity assembly schedules across North America, Germany, Japan, and Latin America, Hualeao collaborates with regional freight forwarders and bonded warehouse networks to establish safety stock reserves, reducing intercontinental supply shock risks to absolute zero.
Anticipating next-generation propulsion fluids: carbon nanotube (CNT) doping, synthetic e-fuels, green e-methanol, and hydrogen carrier combustion.
Standardization of 100% lead-free electrolytic tin deposition with bismuth/silver micro-additions that eliminate tin whisker formation and safeguard tight spacing across sub-millimeter segment grooves.
Incorporation of multi-walled carbon nanotubes (MWCNTs) into the graphite slurry to achieve a 40% reduction in specific electrical resistivity while tripling tensile mechanical strength against thermal shock cavitation.
Tailoring surface active formulations for synthetic hydrocarbons, Fischer-Tropsch paraffinic fuels, and green e-methanol blends that operate at heightened injection pressures exceeding 7.0 Bar in submerged pump modules.
Integration of deep-learning convolutional neural networks (CNN) directly on our CNC diamond turning lines for real-time sub-micron topographic correction and adaptive slot chamfer profiling.
Direct technical answers from Wenzhou Hualeao's metallurgical and design teams to help you accelerate project validation.
Proven reliability trusted across Tier-1 OEM programs and global replacement markets. Select an engineering family below to review specifications or download technical CAD models.
Engineered for compact in-tank fuel pumps with planar brush contact geometries, minimizing rotational noise.
Precision-molded phenolic matrix with tin-plated winding tabs matching international Bosch and Denso footprints.
Complete drop-in pump module integrating internal check valves, high-pressure bypass, and carbon commutation.
Heated planar lambda probe engineered for extreme exhaust gas thermal cycles and prompt closed-loop ECU response.
Armature core with vacuum-impregnated resin, dynamic micro-balancing, and diamond-trued tin-plated carbon segments.
Specially developed to resist swelling and mechanical shearing when exposed continuously to 100% bio-alcohol fuels.
Ultra-low profile design engineered specifically for small-displacement EFI motorcycle and scooter pumps.
Custom multi-segment layout tailored to your specific armature slot count, brush footprint, and current ratings.
Partner with an established China manufacturing pioneer specializing in ethanol- and methanol-resistant carbon commutators, high-pressure electric fuel pumps, and EFI oxygen sensors. Direct engineering-to-engineering collaboration with complete technical disclosure.

Listed New-Vehicle Energy Conservation & Emission Reduction Project Pioneer (China 11th Five-Year Plan). Supplying trusted Tier-1 pump armatures and carbon commutators globally.