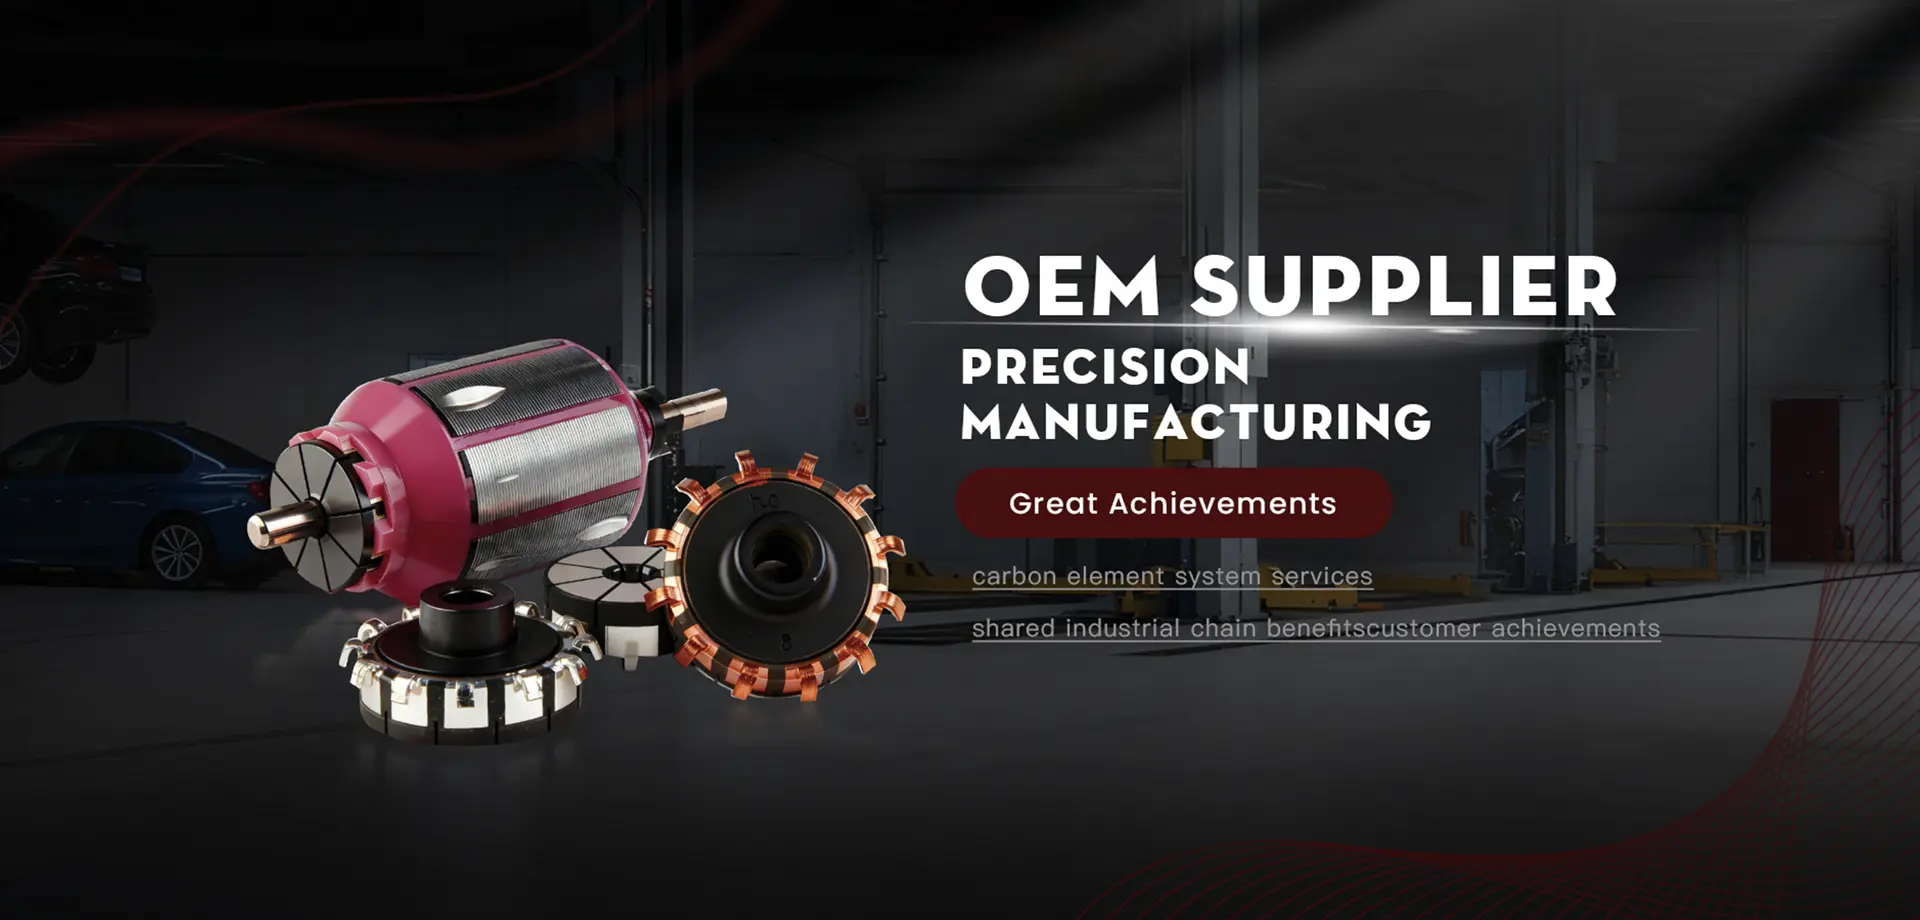
Carbon Commutator Rotor Core
Integrated carbon-graphite contact discs for pump rotors operating submerged in ethanol and methanol blended fuels.
- Tolerance±0.005 mm
- Fuel SubmersionE85 / M100 Safe

Engineered to deliver high transmission accuracy, minimal hydraulic clearance slip, and chemical resilience under alternative fuels.
Integrated carbon-graphite contact discs for pump rotors operating submerged in ethanol and methanol blended fuels.
High-volume automotive rotor assembly engineered for OE pumps requiring whisper-quiet operation and friction minimization.
Complete rotor and motor package calibrated for consistent displacement in gasoline direct injection and common-rail systems.
Zirconia-element lambda sensor delivering exhaust gas feedback to balance fuel pump rotor speed with ECU injection pulse.
High-torque dynamic balanced wound rotor core with resin-bonded segments, preventing thermal delamination under heavy loads.
Custom-formulated isotropic graphite matrix specifically hardened to prevent mechanical erosion in racing and E100 engines.
Multi-lobe inner and outer rotor pair pairing powder metallurgy sintering with computer-controlled cycloidal profile grinding.
Next-generation automotive oil and fluid rotor engineered for brushless and brushed DC continuous immersion pumps.
A technical assessment of modern automotive hydraulic distribution, thermal management in hybrids, and the engineering shift toward high-density sintered pump geometries.
The rise of Hybrid Electric Vehicles (PHEV/HEV) and range-extended drivetrains has fundamentally reshaped oil pump rotor specifications. Engine lubricating circuits now demand auxiliary electric oil pumps (EOP) that operate on-demand independently of engine speed. Rotors must deliver near-instantaneous hydrostatic pressure across wide fluid viscosity fluctuations (-40°C cold crank to 140°C peak thermal loading).
Traditional spur gear pumps suffer from high cavitation risk and high torque ripple at elevated RPM. Modern systemic solutions deploy precision trocho-cycloidal profile geometries. Sintered powder-metal gerotor pairs minimize internal leakage paths along radial and axial running faces, reducing parasitic horsepower losses by up to 18% in modern variable-displacement pump designs.
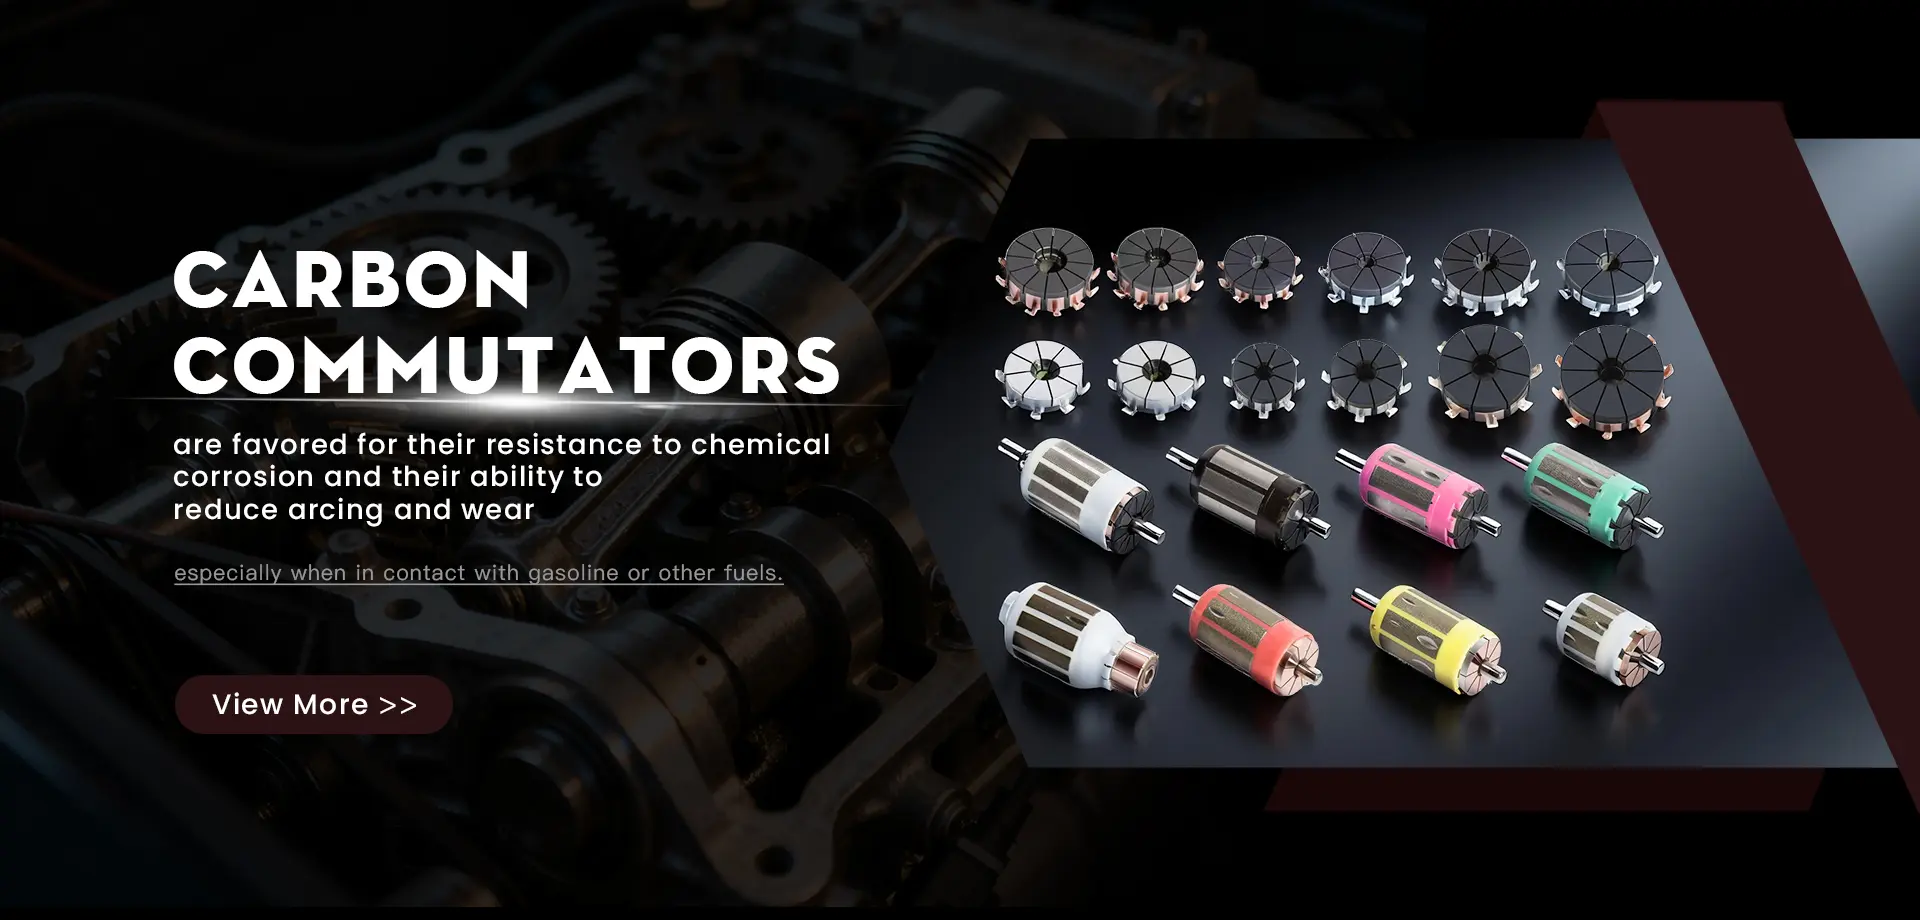
Modern low-carbon fuel mandates (E10, E85, bio-diesels, and neat methanol) introduce high conductivity and aggressive corrosion into the pump module. Standard metal armatures and copper surfaces suffer galvanic erosion and chemical oxidation. Our engineered graphite-carbon matrix rotors and commutators remain completely inert, preventing surface pitting and preserving rotor teeth profiles over lifecycle targets.
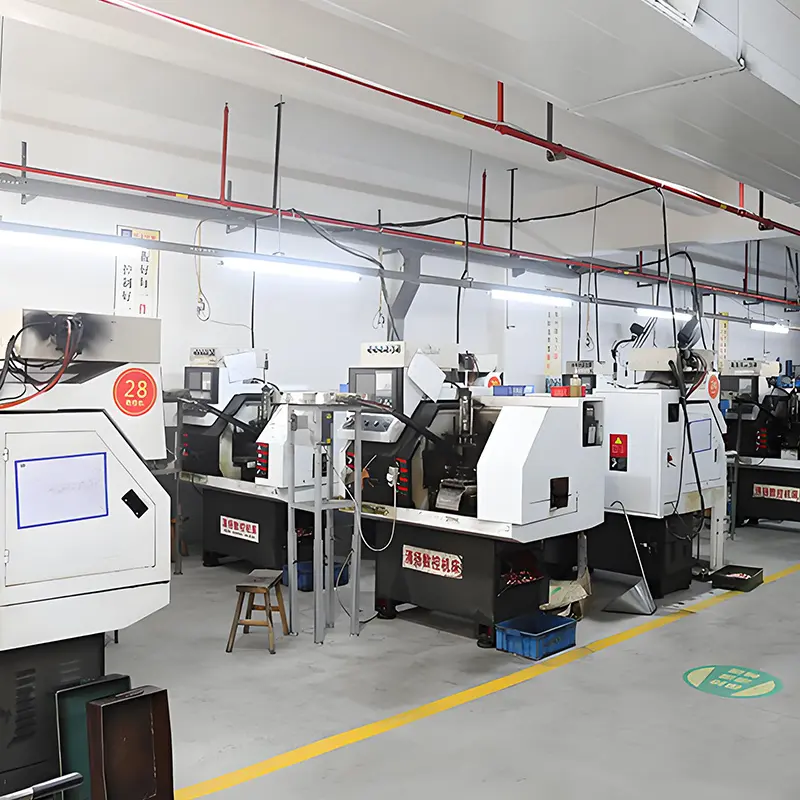
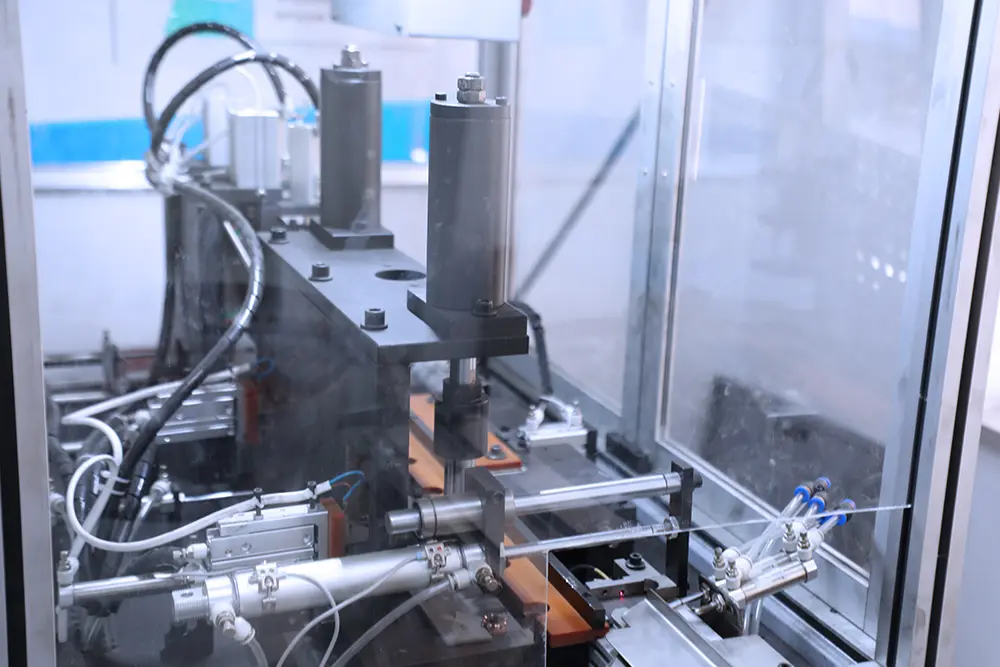
Wenzhou Hualeao Automotive Parts Co., Ltd. bridges high-precision Chinese manufacturing efficiency with overseas metallurgical tolerances. Formally acknowledged in national clean-energy initiatives (listed under China's 11th Five-Year Plan for energy conservation and emission reduction), we utilize computerized powder press compactors, continuous sintering furnaces, and dynamic balancing testers to verify zero-defect performance across every production batch.
| Performance Metric | Standard Market Spec | Hualeao Engineering Spec |
|---|---|---|
| Radial Tooth Runout (TIR) | ≤ 0.015 mm | ≤ 0.005 mm (High Precision) |
| Face Parallelism | ≤ 0.012 mm | ≤ 0.004 mm |
| Sintered Density | 6.6 - 6.8 g/cm³ | > 7.0 g/cm³ (High Structural Strength) |
| E100 / Alcohol Immunity | Susceptible to corrosion | Chemically Inert Isotropic Matrix |
How our continuous quality assurance process guarantees batch-to-batch consistency for Tier-1 assembly lines and international aftermarket distributors.
For OEM programs, we supply Level 3 Production Part Approval Process (PPAP) packages including Control Plans, FMEA, dimensional layout verification, Gage R&R, and full material disclosure via the International Material Data System (IMDS).
Each production run features dedicated barcoded traceability from raw metal/carbon powder delivery through compacting, sintering, double-disc grinding, and computerized optical inspection. Defect tracking is instant and absolute.
To prevent line stoppages for overseas clients across North America, Europe, and Southeast Asia, we support tailored JIT consignment warehousing, VMI buffer stocks, and expedited maritime packaging compliant with ISPM-15 anti-moisture standards.
Direct technical consultation with our engineering division in Ruian, Wenzhou. We review customer 2D/3D CAD drawings (STEP, IGES, DXF) and provide feedback within 24 hours on tooling lead-times, draft angles, and powder alloy selection.
Engineered to withstand high pressure, chemical attack, and high vibration in demanding environments.
Installed inside engine oil management modules, variable cam timing (VCT) actuators, and electric transmission auxiliary pumps. Designed for ultra-quiet acoustic signatures (< 40 dB) and lifetime vehicle reliability without maintenance.
Modern sports and commuter motorcycles operate at extreme engine speeds (up to 14,000 RPM) with high fuel slosh. Miniaturized rotor profiles deliver instant fuel pressurization within small in-tank footprints.
Heavy excavators, wheeled loaders, and mobile cranes endure long duty cycles, high thermal spikes, and heavy vibration. Our high-density sintered materials resist hydraulic shock waves and oil contaminant scoring.
Marine outboard and inboard fuel distribution systems must counter aggressive salt-spray humidity and rapid electrolysis. Optimized graphite formulations protect against galvanic bonding, preventing cold starts and fuel line starvation at sea.
Anticipating next-generation OEM requirements in fluid transfer, friction reduction, and material science.
Application of thin-film Diamond-Like Carbon (DLC) directly onto sintered rotor engagement teeth and thrust faces. Reduces dry-friction coefficient below μ = 0.05, preventing early startup wear during engine start-stop cycles.
Modern internal combustion engines require ultra-low viscosity engine oils to meet global CO&sub2; targets. Our computational fluid dynamics (CFD) group is refining rotor tip sealing clearances to minimize blow-by and maintain continuous volumetric capacity under thin fluid film lubrication.
High-voltage battery packs, silicon carbide inverters, and high-speed e-axles require dedicated dielectric oil immersion cooling. We are engineering composite polymer and sintered rotor pairings engineered for continuous duty in polyalphaolefin (PAO) dielectric fluids.
Clear, direct technical answers for automotive engineers, purchasing managers, and aftermarket importers.
Review additional standard models, OEM replacement units, and sensor integrations manufactured at our Ruian facility.
Segmented disc configuration designed for low spark interference and minimal brush wear in gasoline-ethanol mixes.
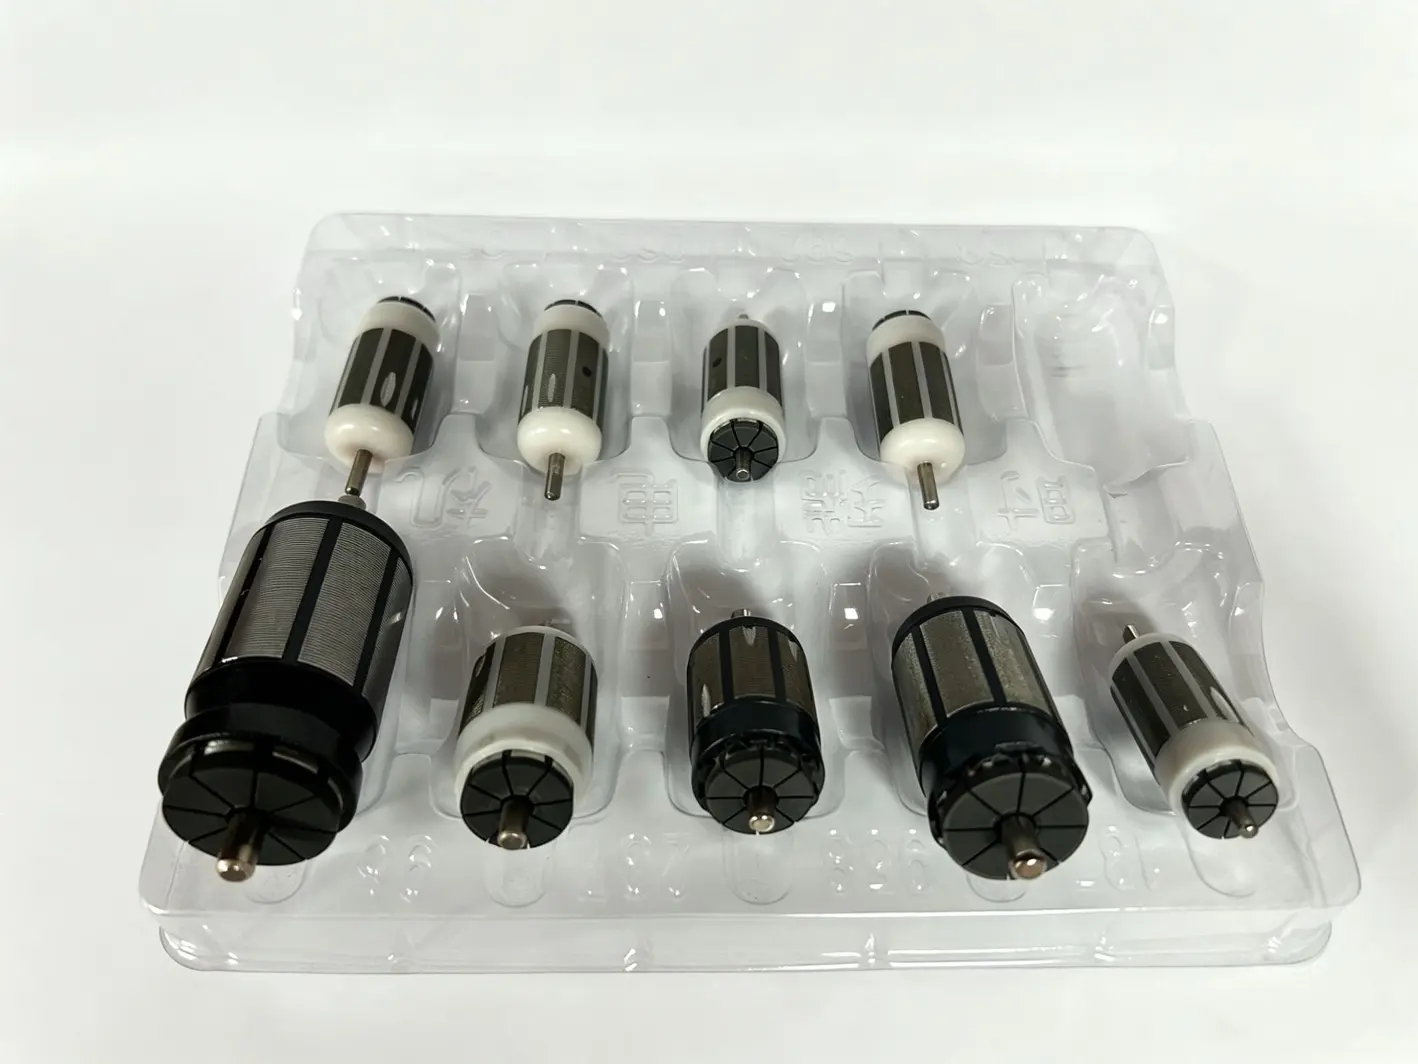
Engineered with dynamic balanced rotor armatures to ensure consistent pressure delivery and low hydraulic pulsation.
Real-time oxygen reading for accurate AFR closed-loop management, protecting three-way catalytic converters from unburned hydrocarbons.
High-volume production standard for OE replacements. Fully interchangeable with international fuel pump platforms.
Precision-wound copper wire core with carbon contact disc for stable torque delivery under high-pressure fuel conditions.
Proprietary composite formulation providing high conductivity, zero swell, and chemical inertness in E85 and M100 fuels.
Mechanical commutation module delivering continuous rotational torque and current reversal for automotive auxiliary drives.
Controlled sintering profiles produce high-density inner and outer rotor geometries with precise tooth profiles and long wear life.
Submit your technical drawings, 3D models, or target OE reference numbers. Our engineering team will review tolerances and return a quotation within 24 hours.