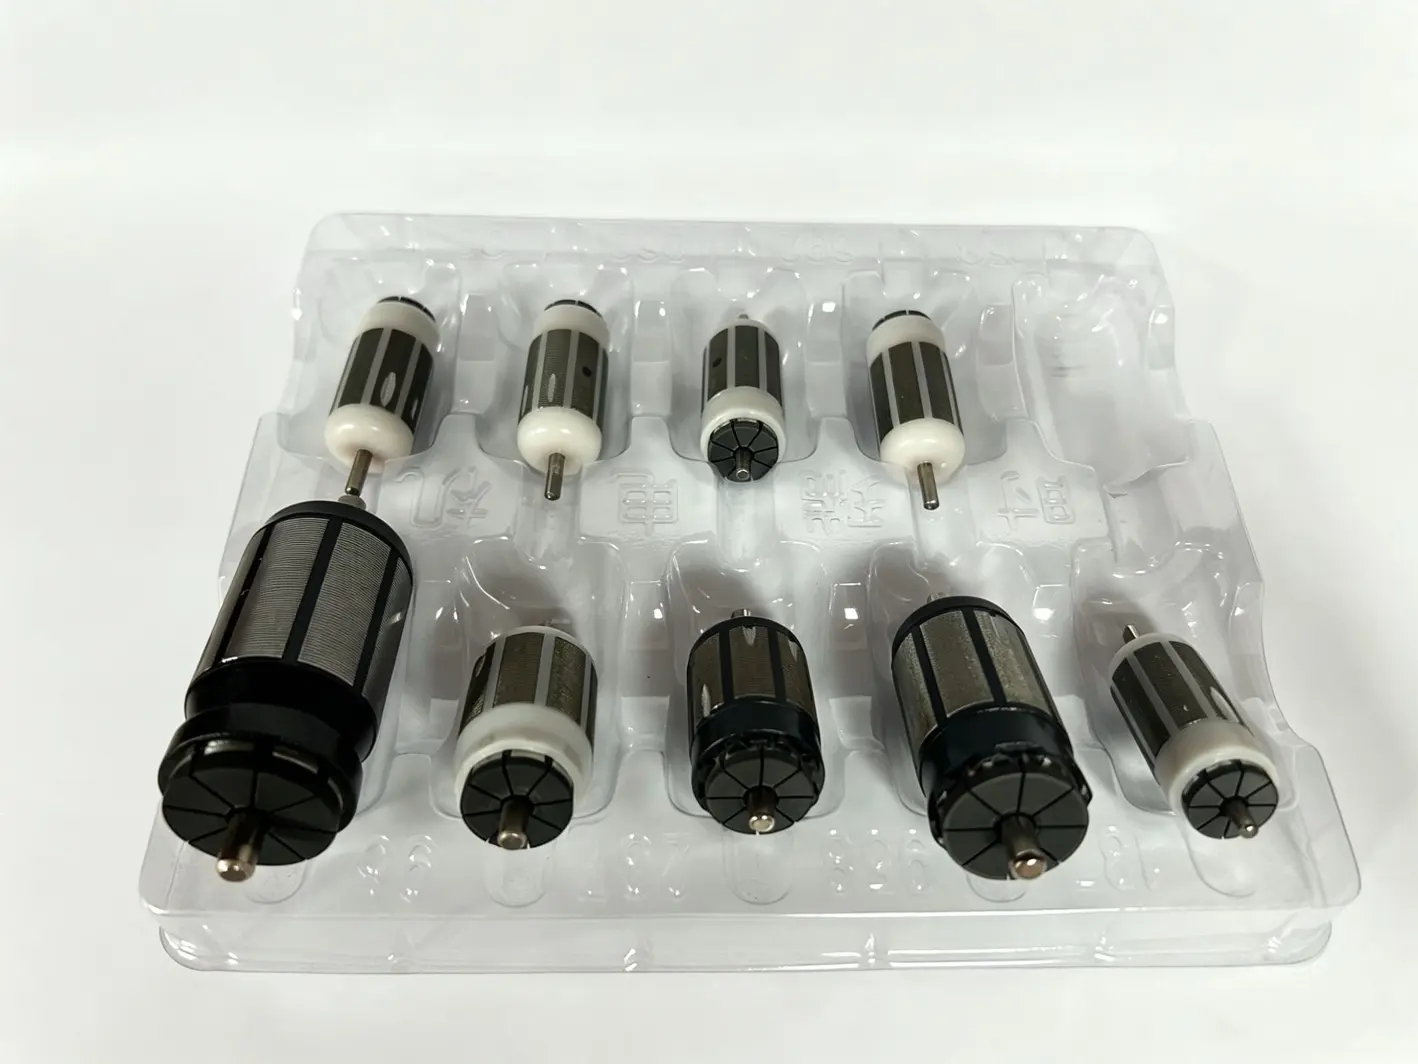
Carbon Commutator Rotor
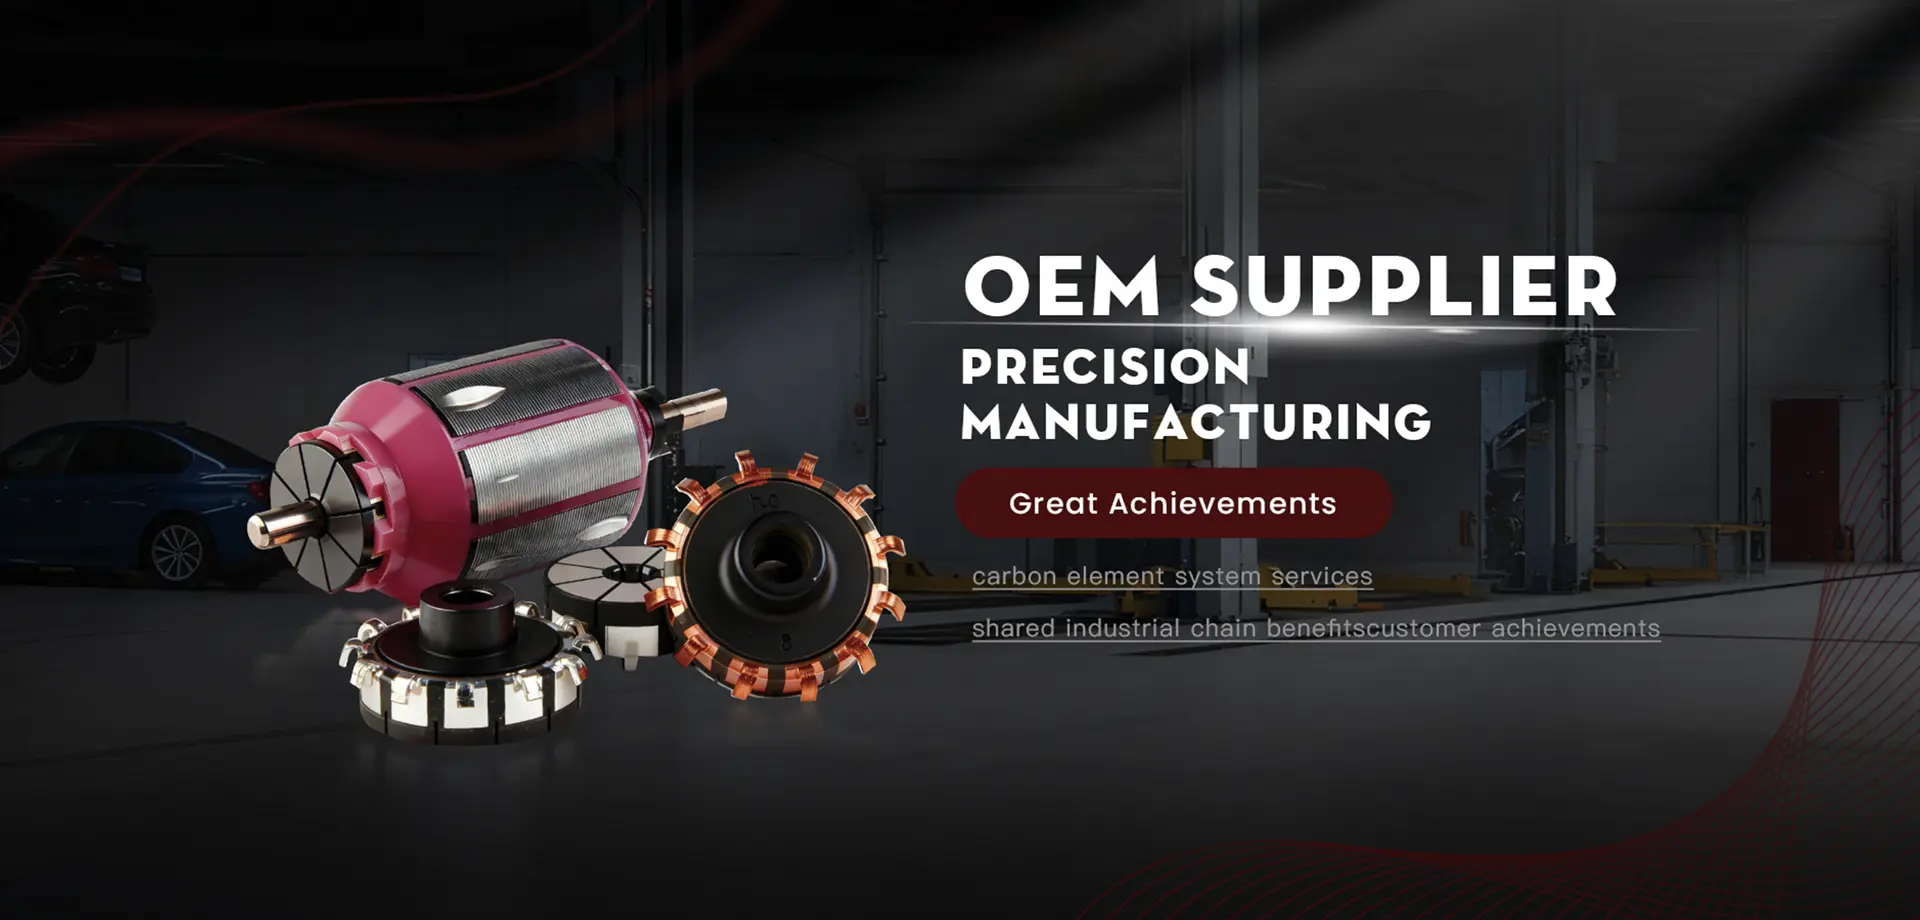
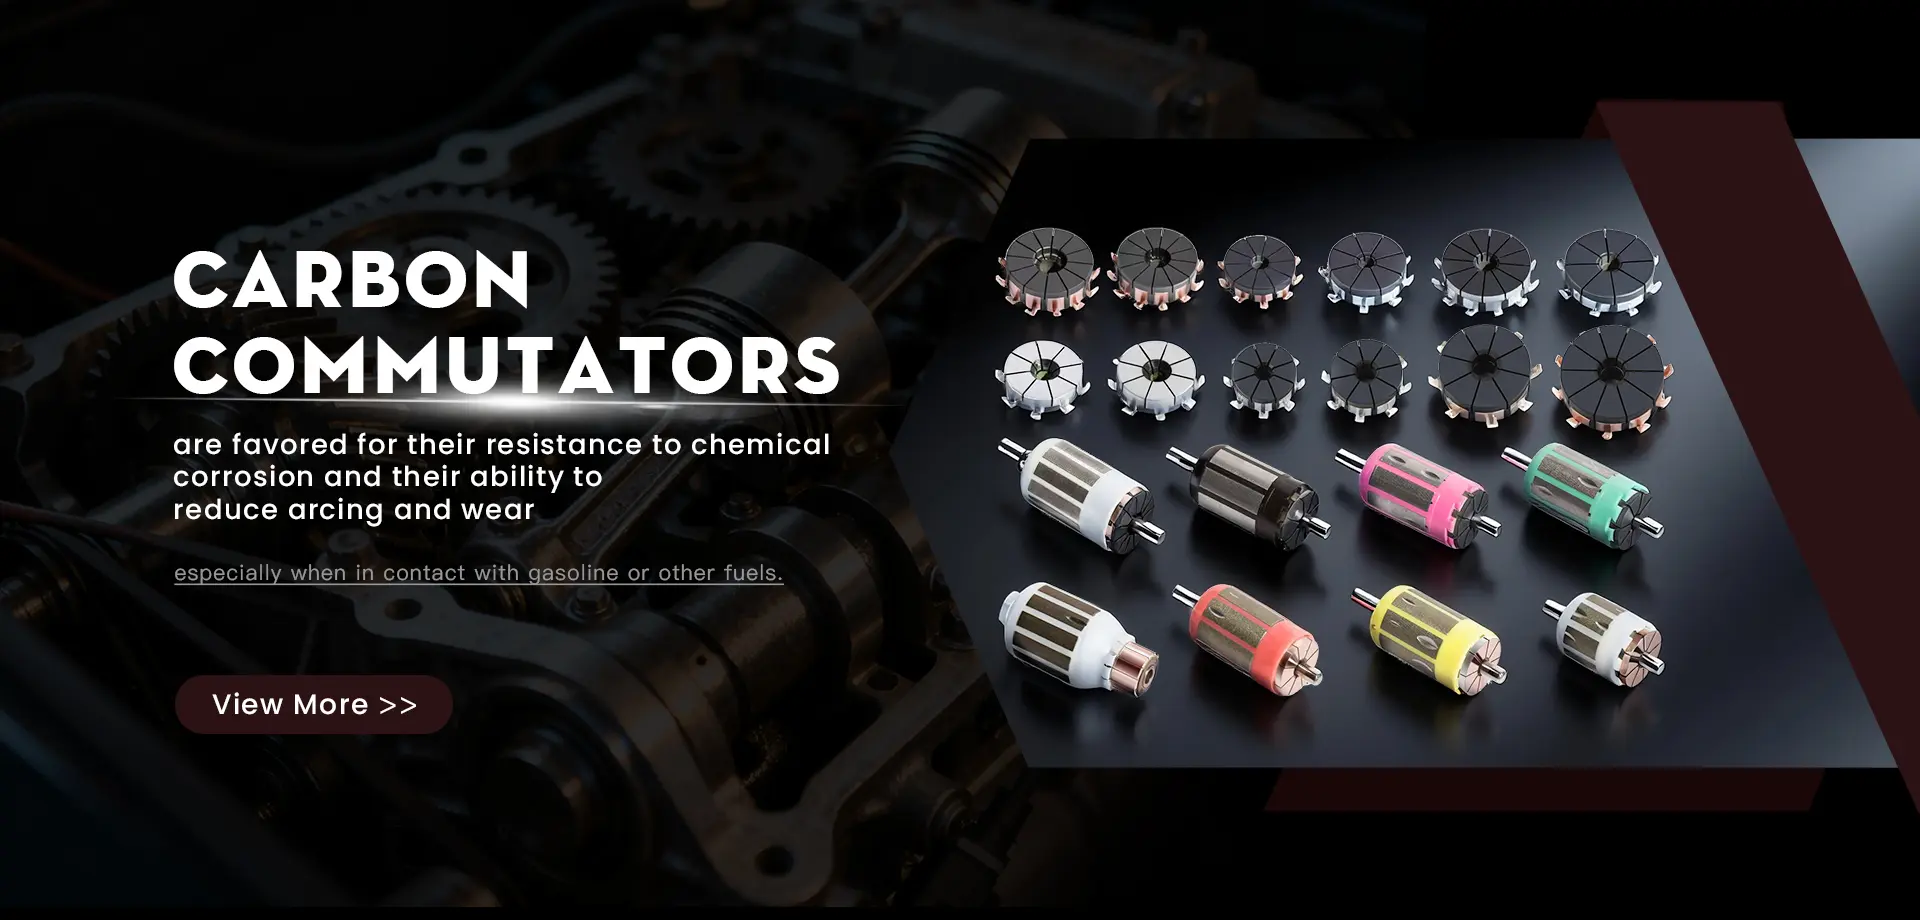
High-purity graphite commutator segment layout engineered for continuous micro-motor rotation, offering superior alcohol and wear resistance.
- MaterialCarbon-Graphite / Cu
- ApplicationBrake Booster & EFI

Explore our certified range of electric brake booster drive motors, high-speed fuel pumps, O2 sensors, and customized graphite commutators engineered for harsh duty cycles.
High-purity graphite commutator segment layout engineered for continuous micro-motor rotation, offering superior alcohol and wear resistance.
Engineered for high delivery stability, vibration damping, and long service life across variable vehicle fuel matrices and electronic injection platforms.
Reference OE 89465-0E040. Fast-response zirconia sensing element feeding closed-loop air-fuel feedback to the vehicle engine management unit.
Engineered explicitly for heavy-duty DC motors requiring negligible surface arc formation, steady torque transfer, and anti-spark protection.
Precision-wound copper core and balanced motor shaft matched to graphite commutators for high-rpm vacuum booster drives and pressure delivery.
Flat profile commutator geometry providing optimized axial contact area for compact electronic vacuum pumps and auxiliary brake boosters.
Designed for low acoustic emissions (<48dB) and high initial breakaway torque to achieve immediate vacuum build-up in emergency braking events.
Heavy duty sintered composite construction resistant to salt fog, heavy machine vibration, and chemically aggressive blended biofuels.
An in-depth engineering assessment of internal combustion downsizing, electric powertrain evolution, and the rise of autonomous braking architectures.
Modern passenger vehicles powered by turbocharged Gasoline Direct Injection (GDI) and Miller-cycle internal combustion engines spend considerable operation windows at positive intake manifold pressure. Consequently, the conventional mechanical vacuum source is virtually eliminated, demanding electric auxiliary brake booster pumps (EVP) to maintain the 500–800 mbar differential pressure required for vacuum boosters.
Battery Electric Vehicles completely dispense with engine manifolds, making standalone, brushless, or precision-commutated DC electric vacuum pumps an absolute safety requirement. Auxiliary vacuum booster units must achieve full vacuum drawdown within 250 to 400 milliseconds, interfacing directly with Electronic Stability Control (ESC) and regenerative hydraulic blending units.
With Autonomous Emergency Braking (AEB) and Level 2+/Level 3 autonomous driver assist systems mandated globally, the brake booster pump is classified under ASIL-B and ASIL-D functional safety regimes. Suppliers must eliminate common electrical failure mechanisms—such as commutator dielectric tracking, brush contact chatter, and thermal runaway.
| Pumping Architecture | Typical Application | Evacuation Time to -60 kPa | Commutator / Motor Technology | Primary Industrial Constraint |
|---|---|---|---|---|
| Direct-Drive Vane Brake Booster Pump | Turbocharged Downsized ICE | < 380 ms (0.5L reservoir) | Carbon-Graphite Submersible Disc | Thermal dissipation under engine bay soak (125°C) |
| Diaphragm Auxiliary Vacuum Pump | PHEV / Range Extender | < 550 ms (0.5L reservoir) | Precision Sintered Copper-Graphite Core | Acoustic isolation (< 50 dBA target) |
| Integrated Electro-Hydraulic Booster | Full BEV / Level 3 Autonomous | Instantaneous Hydraulic Rise | High-RPM Brushless / Dynamic Commutator | Long-term wear resistance under rapid micro-cycles |
How Wenzhou Hualeao Automotive Parts leverages vertically integrated supply clusters, national energy-saving engineering recognition, and automated high-yield fabrication.
Located in Ruian, Wenzhou—China’s global epicenter for automotive components. Raw graphite sourcing, copper terminal stamping, dynamic balancing, and assembly tooling are integrated within a 15-kilometer radius, drastically compressing lead times.
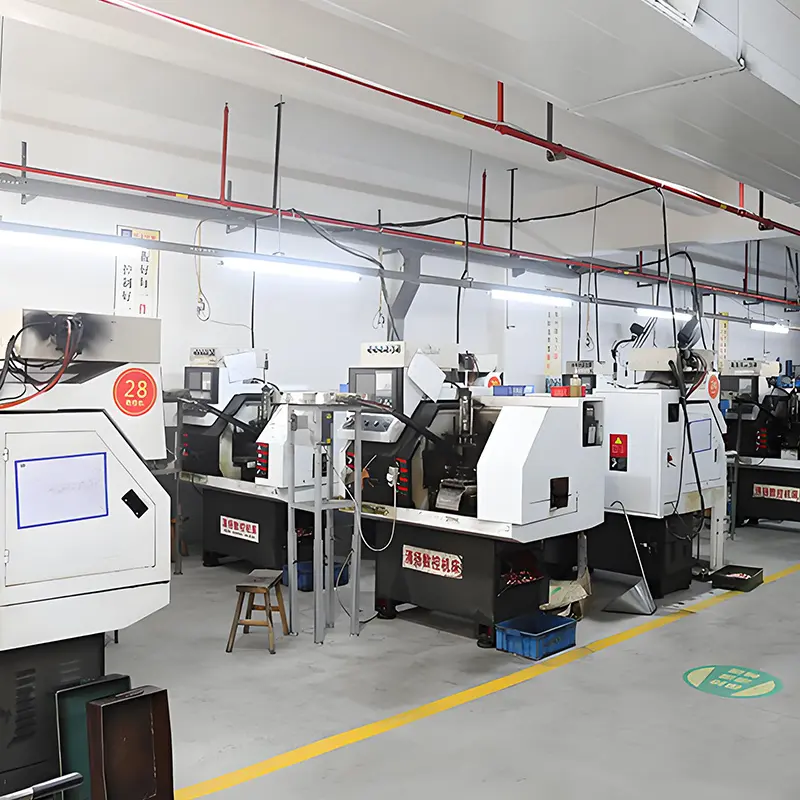
Equipped with micron-precision automated grinding, segment slotting, and armature spin-test benches. Total indicated runout (TIR) is held consistently within ≤ 0.003 mm, matching and replacing expensive Tier-1 European components.
Our proprietary formulation for anti-corrosion carbon commutators was recognized under China’s prestigious 11th Five-Year New Vehicle Energy Conservation and Emission Reduction Program, reflecting proven academic and industrial credibility.
Where Western manufacturing lines face 24-week retooling periods, our tooling and rapid prototyping department delivers validated customized prototypes according to CAD models, 2D drawings, or reverse-engineered samples within 14 to 21 business days.
From high-altitude cold starts to salt-spray marine duty and heavy mining shock loads, our micro-motors and commutators guarantee unwavering physical reliability.
Operating inside electronic fuel injection (EFI) tanks and engine compartment vacuum lines. Our ethanol-resistant graphite prevents degradation caused by E10, E85, and pure methanol fuels, ensuring stable line pressure and consistent brake pedal assistance across 300,000+ kilometers.
Compact motorcycles demand miniature fuel pumps and auxiliary actuators capable of withstanding 12,000+ motor RPMs. Our precision dynamic balancing prevents brush bounce, minimizing electrical interference with motorcycle digital clusters and ECU modules.
Hydraulic excavators, heavy wheel loaders, and mining haulers operate in high-ambient dust, extreme mechanical shock, and steep temperature fluctuations. Reinforced armature housings and wear-resistant commutators ensure auxiliary braking assists never experience vacuum lock.
Submerged in salt-laden coastal atmospheres and running high-sulfur or ethanol-modified marine fuels. Our specialized resin-impregnated graphite formulations eliminate anodic copper pitting and prevent internal salt-crust short-circuits.
What automotive Tier-1 purchasing managers, aftermarket distributors, and engineering contractors demand when auditing brake booster and fuel system manufacturing partners.
With aggressive alternative fuels (E20 to E100) accelerating globally to curb carbon emissions, traditional electrolytic copper commutators suffer rapid galvanic dissolution. Sourcing departments in North America, Brazil, and Europe are transitioning their approved vendor lists (AVL) exclusively to carbon-graphite composites.
Global OEMs require complete Production Part Approval Process (PPAP Level 3) submittals, including full material disclosure via the International Material Data System (IMDS). Buyers require traceable spectrometer analysis of raw graphite blocks and cadmium/lead-free soldering compliance.
Turbulent maritime logistics and geopolitical volatility have pushed procurement officers toward established Chinese factories with guaranteed buffer stock, documented financial stability, and flexible EXW, FOB, CIF, or DDP multi-currency terms (USD, EUR, RMB).
Wenzhou Hualeao Automotive Parts Co., Ltd. operates state-of-the-art sintering furnaces, automatic segment cold-pressing presses, dynamic balance analyzers, and high-frequency spark test units. Our engineering team bridges the gap between scientific graphite chemistry and real-world micro-motor durability.
In-depth technical articles written by our engineering lab exploring electrical contact physics, lambda exhaust regulation, and DC motor commutation dynamics.
An oxygen (lambda) sensor monitors the post-combustion exhaust stream, relaying millivolt fluctuations to the engine ECU to maintain the stoichiometric ratio (14.7:1 for gasoline). Learn how upstream and downstream sensors safeguard catalytic converters.
Read Whitepaper →Ethanol and methanol fuels promote extreme electrochemical wear on copper contacts. Discover how graphite crystalline orientation and natural lubricating properties prevent dielectric film breakdown and prolong pump motor lifespan 3-fold.
Read Whitepaper →A commutator acts as an automated mechanical phase inverter, maintaining continuous unidirectional torque inside micro-motor armatures. Explore our analytical approach to slot design, mica undercutting, and brush interface optimization.
Read Whitepaper →Direct answers for automotive systems engineers, procurement specialists, and global importers.
Comprehensive specifications for Tier-1 replacement units, repair kits, and custom manufacturing platforms available for worldwide commercial export.
High-density resin graphite structure engineered for high-rpm auxiliary electric vacuum brake pumps and submerged electronic fuel delivery.
High-efficiency electric motor assembly delivering rapid evacuation and stable differential vacuum for passenger car brake servos.
Engineered for rigorous exhaust gas measurement, with fast ceramic light-off heaters and high chemical resistance against fuel additives.
Global aftermarket benchmark for fuel pumps and micro vacuum drive motors, manufactured with automated molding technology.
Reinforced copper winding structure combined with an anti-friction shaft and graphite commutator interface for extended operational longevity.
Designed for compact space installations inside electronic braking booster systems, eliminating axial length while ensuring maximum contact.
Designed to deliver high initial starting torque, ensuring instantaneous vacuum chamber evacuation under severe emergency braking scenarios.
Constructed specifically for heavy-duty commercial transport and off-road engineering machinery exposed to severe continuous shock and dirt ingress.