Explore our core industrial configurations engineered for dimensional runout precision (<0.003mm), anti-delamination resin matrices, and dynamic operating balance up to 12,000 RPM.

Planar graphite contact face engineered for submerged automotive fuel pump armatures running high-blend ethanol fuels.

Our flagship high-demand disc commutator, selected globally by electric fuel pump rebuilders and OE assembly operations.

Integrated dynamic-balanced electric fuel pump motor assembly outfitted with our corrosion-proof carbon disk rotor interface.

Upstream/downstream zirconia feedback sensor matching OE 89465-0E040 to maintain closed-loop AFR stability with EFI motors.
Reinforced mechanical segment lock engineered for high thermal spikes and continuous duty cycles in excavation platforms.
Sub-compact profile tailored for space-constrained fuel pump designs on modern Euro 5 / BS-VI fuel-injected motorcycles.
Proprietary silver-graphite alloy interface designed to eradicate galvanic corrosion in outboard and marine inboard engines.
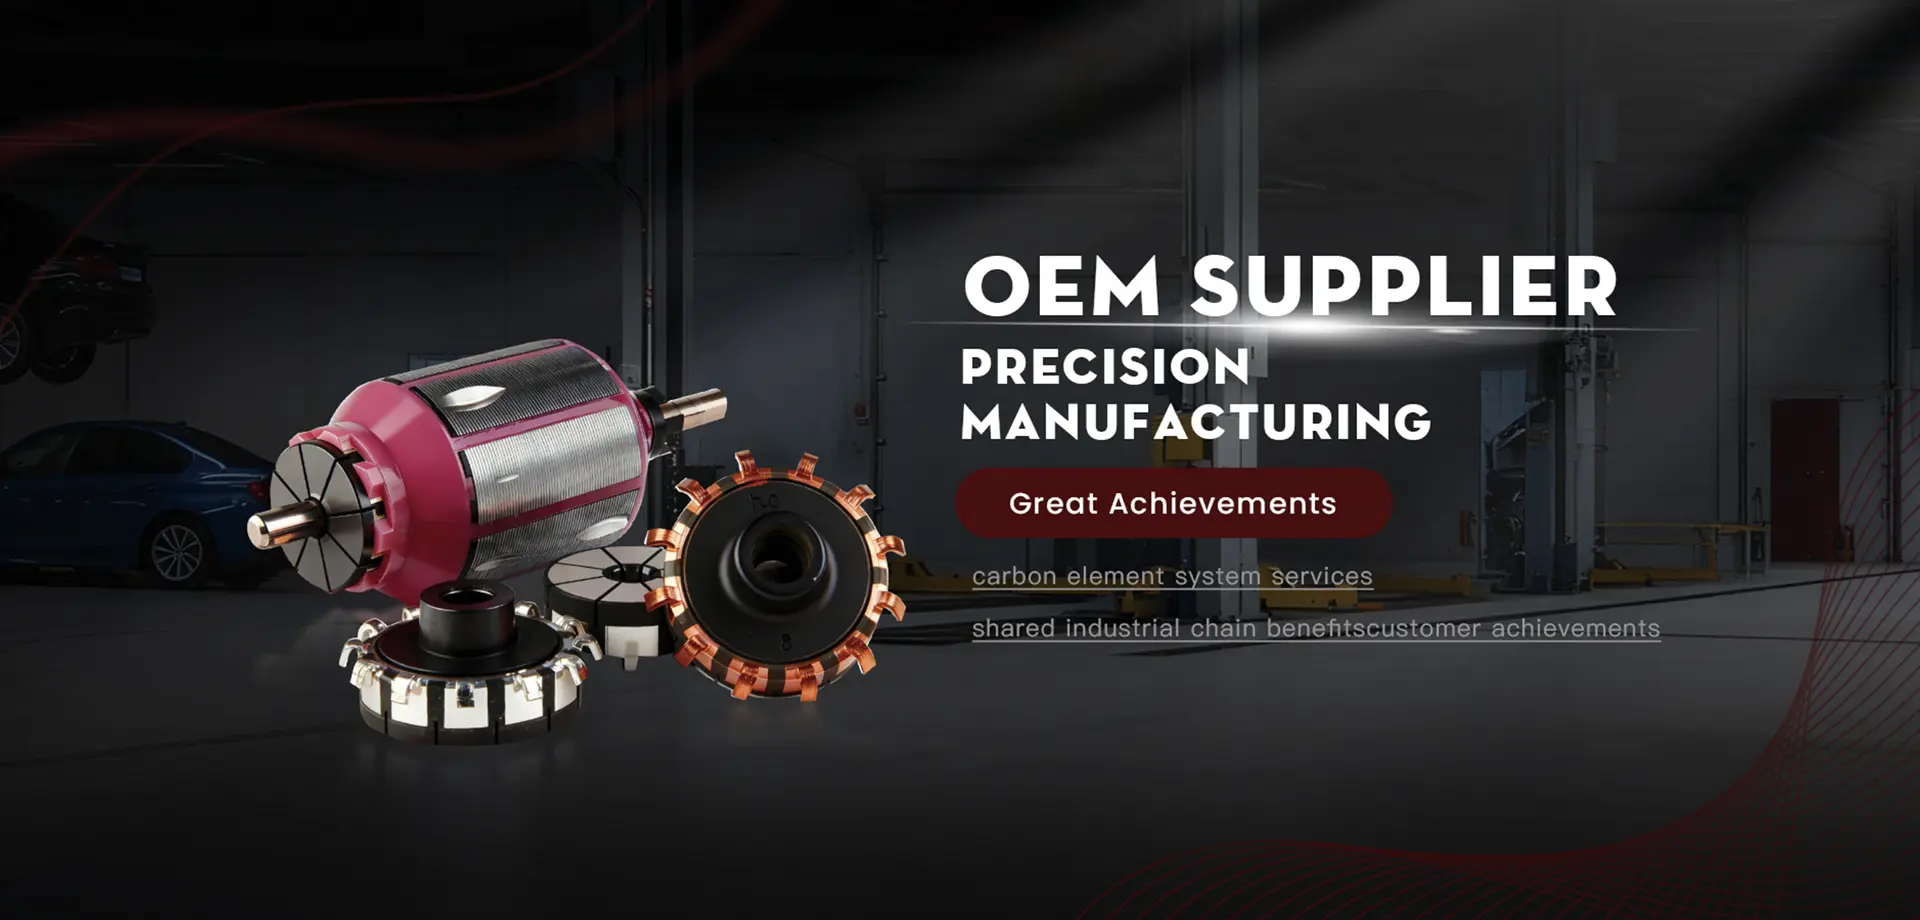
Pre-balanced rotating armature core featuring precision wire hook brazing and diamond-faced carbon disc finishing.
A rigorous examination of electrical contact mechanics, tribological behavior under bio-fuel immersion, and why planar graphite architecture has replaced copper segments in critical automotive fuel pumps.
Traditional electric fuel pump motors utilized pure electrolytic copper segments on cylindrical commutators. While copper possesses exceptional electrical conductivity (~58 MS/m), it exhibits fatal vulnerabilities when submerged in modern oxygenated motor fuels:
1. Electrochemical Corrosion & Pitting: Commercial ethanol (E10, E27, E85, E100) contains ionic impurities, acidic residues (acetic acid), and hygroscopic water content. Under applied DC electrical potential, copper undergoes rapid anodic dissolution, forming copper oxide (Cu2O/CuO) and acetate crusts that escalate contact resistance exponentially.
2. Spark Erosion & Commutation Arcing: As non-conductive dielectric films develop on copper bars, the brush-commutator contact face suffers micro-arcing. This thermal spark vaporization reaches localized temperatures >3,000°C, accelerating bar wear, segment grooving, and catastrophic motor stall within 200–500 operational hours.
Carbon disk commutators eliminate electrochemical degradation by presenting a chemically inert, high-purity graphite contact plane bonded securely onto a copper conductor skeleton. Key operational superiorities include:
1. Solid-State Self-Lubrication: The anisotropic hexagonal crystal lattice of graphite enables basal planes to shear smoothly under low shear stresses. In submerged fuel conditions, graphite establishes an ultra-low friction boundary layer (μ < 0.12), drastically decreasing frictional drag and mechanical brush wear.
2. High Arc Suppression & Uniform Resistivity: Carbon possesses an intermediate electrical resistivity (15–45 μΩ·m) compared to pure copper. This bulk resistance acts as a built-in current limiter during segment bridging, suppressing reactive commutation sparks, electromagnetic interference (EMI), and radio frequency interference (RFI).
| Evaluation Parameter | Conventional Copper Segment Commutator | Hualeao Isostatic Carbon Disk Commutator | Technical Advantage & Impact |
|---|---|---|---|
| Ethanol Corrosion Resistance (E85/E100) | Rapid anodic oxidation, severe pitting, segment lifting | Zero chemical reactivity, 100% inert graphite matrix | Extended pump service life (> 3,500 continuous hours) |
| Methanol Fuel Tolerance (M15-M85) | Catastrophic breakdown within <150 operational hours | Immune to formic acid attack & ionic leaching | Permits direct deployment in methanol flex-fuel powertrains |
| Friction Coefficient (μ) in Gasoline | 0.28 – 0.42 (High mechanical brush abrasion) | 0.08 – 0.15 (Graphitic self-lubricating transfer film) | Lower motor amp-draw, runs 15°C cooler at peak delivery |
| Surface Flatness Runout (Total Indicator) | ± 0.008 – 0.015 mm (Thermal expansion barrel form) | ≤ 0.003 mm (Sub-micron diamond precision lathing) | Negligible brush bouncing, eliminates high-frequency noise |
| Resin Core Thermal Stability | Standard phenolic (Tg ~ 130°C) prone to shrinkage | Specialized glass-reinforced phenolic (Tg > 180°C) | Prevents segment displacement under dry-run motor lockup |
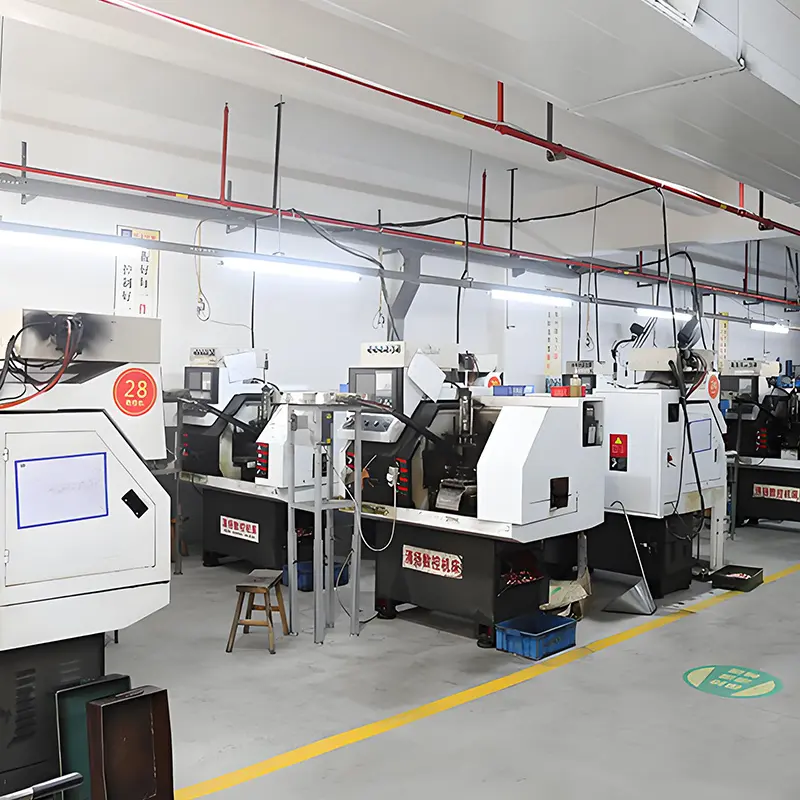
Based in Ruian, Wenzhou—China’s premier automotive component manufacturing cluster—our 6,200 m² production complex operates under stringent IATF standards to deliver zero-defect commutators worldwide.
Recognized as a certified new-vehicle energy conservation and emission reduction technical initiative under China’s 11th Five-Year Plan, our electronic fuel injection (EFI) carbon commutators match overseas benchmarks in mechanical integrity, dielectric strength, and chemical endurance while providing unparalleled supply chain cost-efficiencies.
Modern micro-commutation demands precise adaptation to localized fuel formulations, duty cycles, and environmental harshness across varied global markets.
In regions such as Brazil and North America where bio-ethanol concentrations reach E85 to E100, standard fuel pumps fail precipitously. Hualeao’s isostatic graphite disk preserves structural integrity under extreme organic ester exposures, ensuring steady fuel delivery across daily commuting cycles without drop in rail pressure.
Two-wheelers in India, Vietnam, and Indonesia face stringent emission standards (BS-VI / Euro 5) alongside tropical heat and heavy traffic idling. Our ultra-thin, low-inertia disc commutators maintain dynamic balance up to 14,000 RPM, preventing hot-fuel vapor lock and ensuring instantaneous throttle response in congested urban centers.
Excavators, wheel loaders, and mining dumpers operate in high-vibration, dust-laden terrains with irregular fuel cleanliness. Featuring glass-fiber reinforced high-Tg phenolic substrates, our commutators withstand continuous 25G shock loads and elevated fuel tank temperatures exceeding 90°C without segment shifting.
Salt spray, ambient humidity, and marine fuel condensation create severe galvanic electrolytic cells inside submerged marine pumps. Hualeao utilizes passivated copper terminal hooks and resin impregnations that achieve >500 hours ASTM B117 salt fog endurance, protecting luxury boats and commercial fishing armatures.
How Wenzhou Hualeao leverages vertical integration, localized raw material clusters, and high-velocity tooling to ensure 100% on-time delivery across fluctuating global trade cycles.
Situated in Ruian City (known globally as the Auto & Motorcycle Parts Capital of China), Hualeao operates within a sub-20-kilometer radius of specialized mold-makers, precision copper stamping suppliers, and polymer compounding laboratories. This geographic clustering truncates production lead times by over 40% compared to dispersed manufacturing footprints.
From primary isostatic graphite sintering and copper disk stamping to robotic brazing, molding, and high-speed CNC diamond finishing, all critical steps occur within our 6,200 m² plant. Eliminating external subcontracting guarantees end-to-end traceability, tighter batch-to-batch tolerance (≤0.003mm), and zero IP slippage for custom OE armatures.
We maintain permanent strategic reserves of aerospace-grade synthetic graphite powders, high-purity electrolytic oxygen-free copper, and imported UL94-V0 rated phenolic compounds. Even amid international supply shocks or shipping bottleneck spikes, our scheduled delivery accuracy remains verified at 99.4%.
While battery-electric vehicles dominate headlines, the internal combustion engine (ICE) and hybrid-electric vehicle (HEV/PHEV) fleets remain vast and evolving toward zero-carbon synthetic fuels.
Modern hybrid vehicles subject electric fuel pumps to severe start-stop cycles. Unlike legacy continuous-running engines, HEV fuel pumps encounter repeated thermal cycling and pressure spikes within brief drive windows. Conventional commutators develop surface oxidation during cold dormant phases. Hualeao’s carbon disk commutators provide instantaneous electrical transfer without contact film breakdown, guaranteeing instant fuel pressure buildup during rapid electric-to-combustion transitions.
With an estimated global operating vehicle fleet of over 1.45 billion units, aftermarket demand for high-reliability fuel pump replacements has reached historic highs. Cheap rebuilds utilizing copper commutators frequently fail within warranty periods when end-users fuel up with E10/E15 gasoline. Tier-1 rebuilders and aftermarket brands partner with Hualeao to supply carbon-equipped assemblies that eliminate costly warranty claims and protect brand equity.
Every single carbon disk commutator produced in our Wenzhou plant progresses through four uncompromising stages of precision engineering.
We deploy finite element analysis (FEA) to simulate thermal stress, brush contact pressures, and electromagnetic flux patterns across segment transitions. Material compositions are continuously tailored in partnership with leading university research alliances.
Graphite materials undergo rigorous densification, grain boundary analysis, and spectrographic verification. Raw copper coils for terminal hooks are tested for 99.95% oxygen-free purity to prevent hydrogen embrittlement during resistance welding.
High-tonnage hydraulic presses compress specialized phenolic molding compound under controlled thermal curves. Automated vacuum silver-copper eutectic brazing ensures the carbon-to-copper interface achieves shear bond strength > 35 MPa.
Natural diamond cutting inserts machine the carbon contact face in climate-controlled rooms, achieving surface roughness Ra ≤ 0.2 μm. Automated vision systems verify segment gap spacing, inter-bar insulation (>100 MΩ), and dynamic balance.
How Hualeao is evolving fuel micro-motor architectures to maintain leadership in an era of alternative synthetic e-fuels, carbon neutrality, and ultra-high-efficiency mobility.
Integrating multi-walled carbon nanotubes (MWCNTs) and exfoliated graphene nanoplatelets into our isostatic graphite mixes. Laboratory prototypes demonstrate a 28% reduction in specific electrical contact resistance, 40% higher fracture toughness, and total operational lifespans exceeding 6,000 continuous hours in harsh E100 ethanol fuels.
As global commercial aviation and marine shipping shift toward synthetic paraffinic kerosenes (e-Kerosene) and e-Methanol synthesized from captured CO2 and green hydrogen, commutator resins must withstand previously unseen organic peroxide and formic acid concentrations. Our R&D is formulating polyimide-matrix commutators resistant to chemical dissolution up to 220°C.
Development of micro-embedded resistive telemetry tracks within the phenolic core of the commutator. These tracks allow real-time diagnostic reporting of brush wear, contact face temperature, and electrical arcing status directly to the vehicle’s Central Powertrain ECU, enabling predictive maintenance prior to fuel starvation.
Delivering frictionless global procurement through complete regulatory compliance, full CAD/STEP interoperability, and dedicated bilateral engineering consulting.
Send our engineering team your 2D blueprints, 3D CAD files (STEP, IGES, SolidWorks), physical sample armatures, or OEM reference codes. We evaluate axial tolerances, segment angles, and hook clearance, outputting validated rapid prototypes within 10 to 15 business days.
All raw carbon blocks, phenolic molding compounds, brazing alloys, and copper terminal hooks are certified 100% compliant with EU REACH Annex XVII regulations, RoHS Directive 2011/65/EU (lead-free, cadmium-free), and TSCA chemical standards for hassle-free customs clearance across Europe and the Americas.
Direct communication with senior electromechanical engineers. We support motor coil designers with winding diameter calculations, hook tang staking guidance, and hot-staking thermal profiles to maximize winding pull-off strength during automated production runs.
Essential reading for automotive fuel system architects, pump rebuilders, and procurement directors looking to optimize lifespan and lower warranty return rates.
An oxygen (lambda) sensor measures residual oxygen concentrations in engine exhaust, relaying millivolt data to the ECU. Learn how rapid sensor switching prevents fuel pump over-fueling, preserves catalytic converters, and stabilizes fuel delivery demand.
Read Technical GuideInside every modern submersible EFI fuel pump motor, the commutator operates directly immersed in fuel. Discover the tribological physics behind how graphite eliminates spark erosion and why copper commutators cannot survive in modern ethanol fuel blends.
Read Technical GuideA deep mechanical exploration of the commutator as a rotary mechanical inverter that reverses armature coil currents synchronously with magnetic flux. We analyze contact bounce, segment mica depth, and brush track wear mitigation.
Visit Knowledge HubSelect your required component category below to access dimensional technical drawings, cross-reference part numbers, and direct factory quotation pricing.
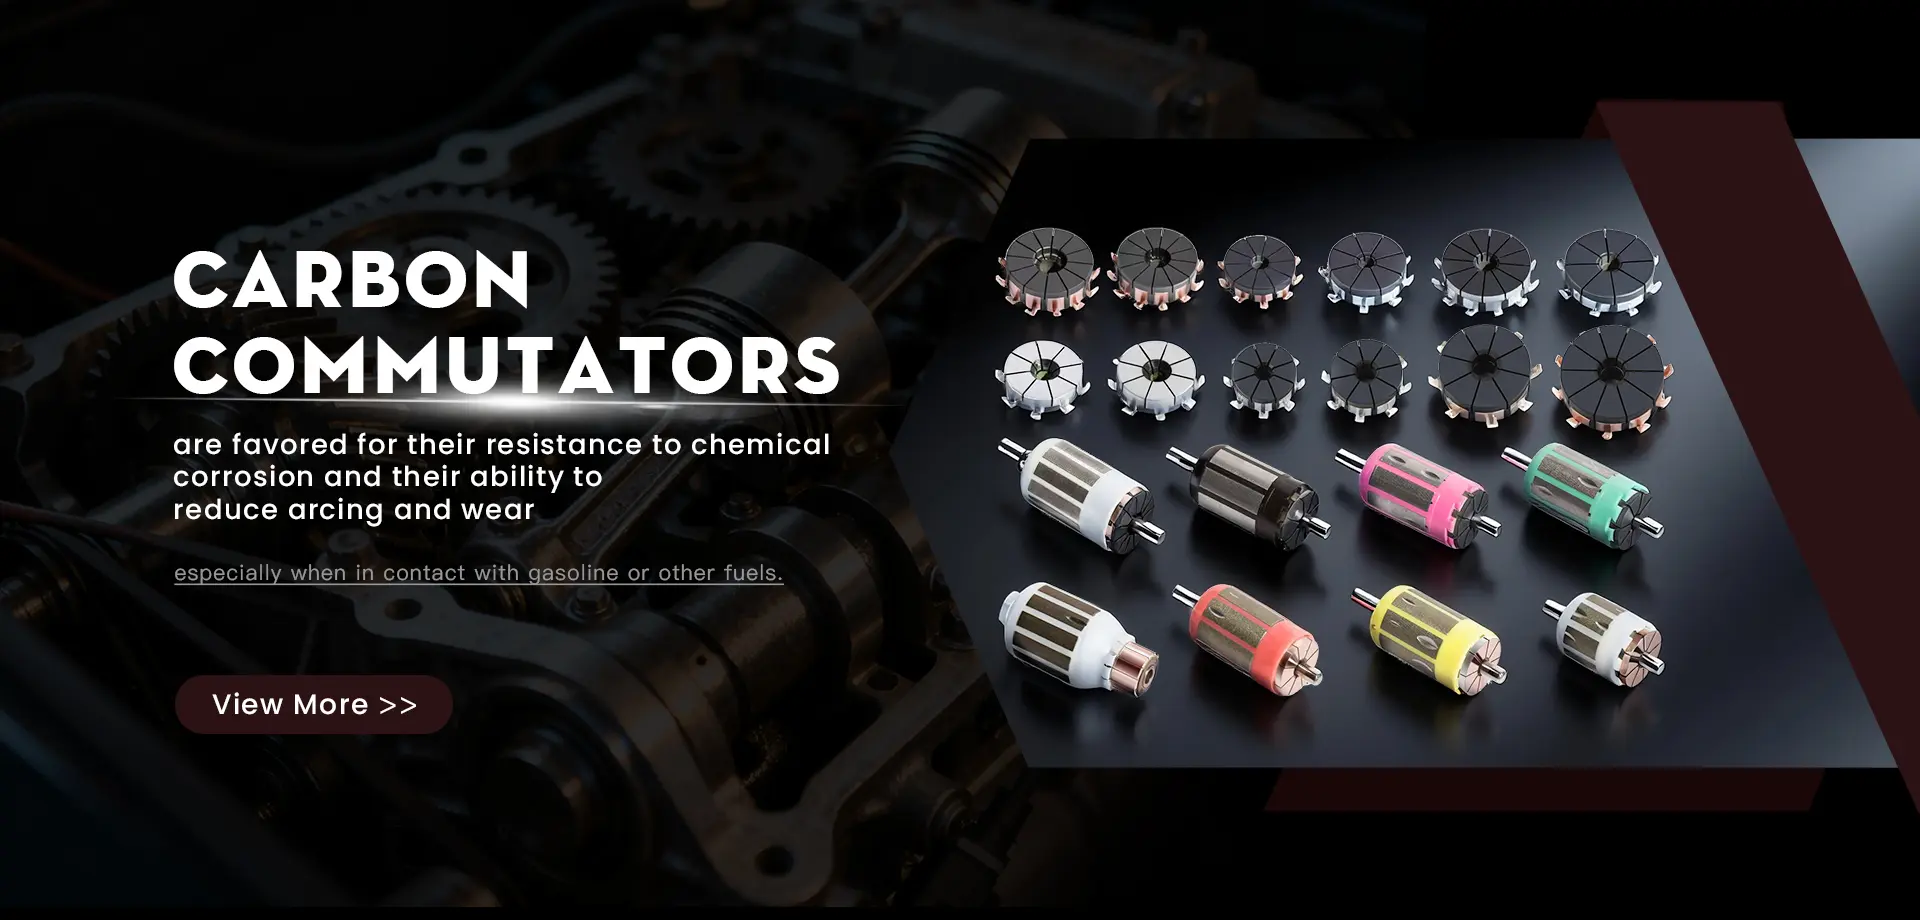
Industry-standard 8-to-12 segment disk configuration designed for seamless integration into OEM EFI fuel pump rotors.
High-efficiency turbine pump assembly with an integrated carbon disk commutator motor core for steady, pulse-free fuel delivery.
OEM replacement sensor engineered for rapid light-off times and ultra-precise lambda tracking across all exhaust gas temperatures.
The global aftermarket benchmark for high-reliability fuel pump rebuilding, featuring proprietary graphite segment reinforcement.
Formulated with specialized polyimide thermoset matrix engineered to resist continuous 180°C operating oil/fuel temperatures.
Fully wound, resin-impregnated, and dynamically balanced rotor cores incorporating our carbon disk commutators.
Built for racing and modified automotive engines requiring high-amperage, high-voltage stable micro-commutation.

Direct fit for popular passenger SUVs and sedans, featuring laser-welded dual protective tubes and anti-poisoning coatings.
Detailed engineering and procurement answers covering tribology, customization, quality assurance, and international logistics.
The commutator functions as a mechanical rotary switch that transfers electrical current from the stationary carbon brushes to the rotating armature windings of the pump motor. By reversing current flow direction twice per revolution as the armature turns, it ensures continuous, unidirectional torque to drive the fuel impeller. Because the electric fuel pump motor is submerged in fuel, the commutator’s contact quality, material purity, segment planarity, and wear resistance directly determine the fuel flow stability, hydraulic efficiency, and operational lifespan of the entire fuel delivery module.
Modern automotive electric fuel pumps run directly submerged in fuel for motor cooling and lubrication. In modern ethanol-blended gasolines (such as E10, E27, E85, or E100) and methanol blends, copper segments suffer rapid electrochemical oxidation, spark erosion, and catastrophic pitting under DC electrical potential. Carbon (graphite) commutators are chemically inert, providing complete immunity to ethanol, methanol, and organic acid corrosion. Furthermore, graphite’s solid-state self-lubricating characteristics drastically lower mechanical friction and wear, allowing fuel pumps to operate reliably for more than 3,500 continuous hours.
Yes. Wenzhou Hualeao specializes in custom engineering and rapid prototyping. Buyers can send 2D engineering drawings, 3D CAD files (STEP, IGES), physical sample parts, or OE part numbers. Our in-house technical department evaluates overall diameter, bore size, segment count, copper hook angles, and carbon layer thickness. We create dedicated molds, match specific resin and graphite grades to your target fuel environment, and deliver test samples with full dimensional inspection reports.
Our carbon commutators, fuel pumps, and oxygen sensors are widely deployed in passenger automobile EFI fuel systems, high-revving motorcycle engines (Euro 5 / BS-VI standards), heavy-duty construction machinery and excavators, agricultural vehicles, and marine inboard/outboard marine engines. We serve both global Tier-1 OEM manufacturing programs and premier aftermarket replacement distributors worldwide.
Prospective clients can request complete technical specifications by emailing our sales engineering office directly at [email protected], reaching out via WhatsApp at +86 15067763878, or visiting our dedicated catalog request portal. Our team typically returns dimensional cross-reference drawings, model cross-match charts, and pricing schedules within 12 hours.
We utilize ultra-high-speed diamond lathing machines to finish the carbon disc contact surface. In high-volume production runs, our carbon face total indicator runout (TIR) is held strictly under ≤ 0.003 mm, with surface roughness controlled to Ra ≤ 0.2 μm. For complete wound armatures, dynamic balancing meets ISO G2.5 standards to eliminate high-speed harmonic vibrations and audible motor whirring.
Our 6,200 m² production complex operates under certified IATF automotive quality frameworks. We apply statistical process control (SPC) across every workstation, including incoming spectrographic metal analysis, 100% automated inter-segment dielectric breakdown testing (>500V DC), ultrasonic carbon-copper bonding verification, and automated optical inspection (AOI) for segment spacing.
For catalog-standard models, warehouse stock can dispatch within 48 to 72 hours. For customized commutators requiring dedicated stamping dies or injection tooling, prototype samples are delivered within 10 to 15 business days. Full container production runs are completed in 25 to 35 days, facilitated by our proximity to Ningbo and Shanghai deep-water container ports.
