Discover our primary lineup of ethanol/methanol-resistant carbon commutators, dynamic-balanced armatures, and electronic fuel pump cores engineered in Ruian, Wenzhou.

Planar face and barrel graphite commutators tailored for submerged automotive EFI fuel pump armatures.

Benchmark OEM replacement segment commutator designed for prolonged duty cycles in E85/E100 biofuels.

High-pressure electronic fuel pump with dynamic-balanced rotor ensuring consistent fuel rail pressure.

Precision exhaust lambda sensor providing millivolt feedback loops to ECUs for closed-loop stoichiometry.
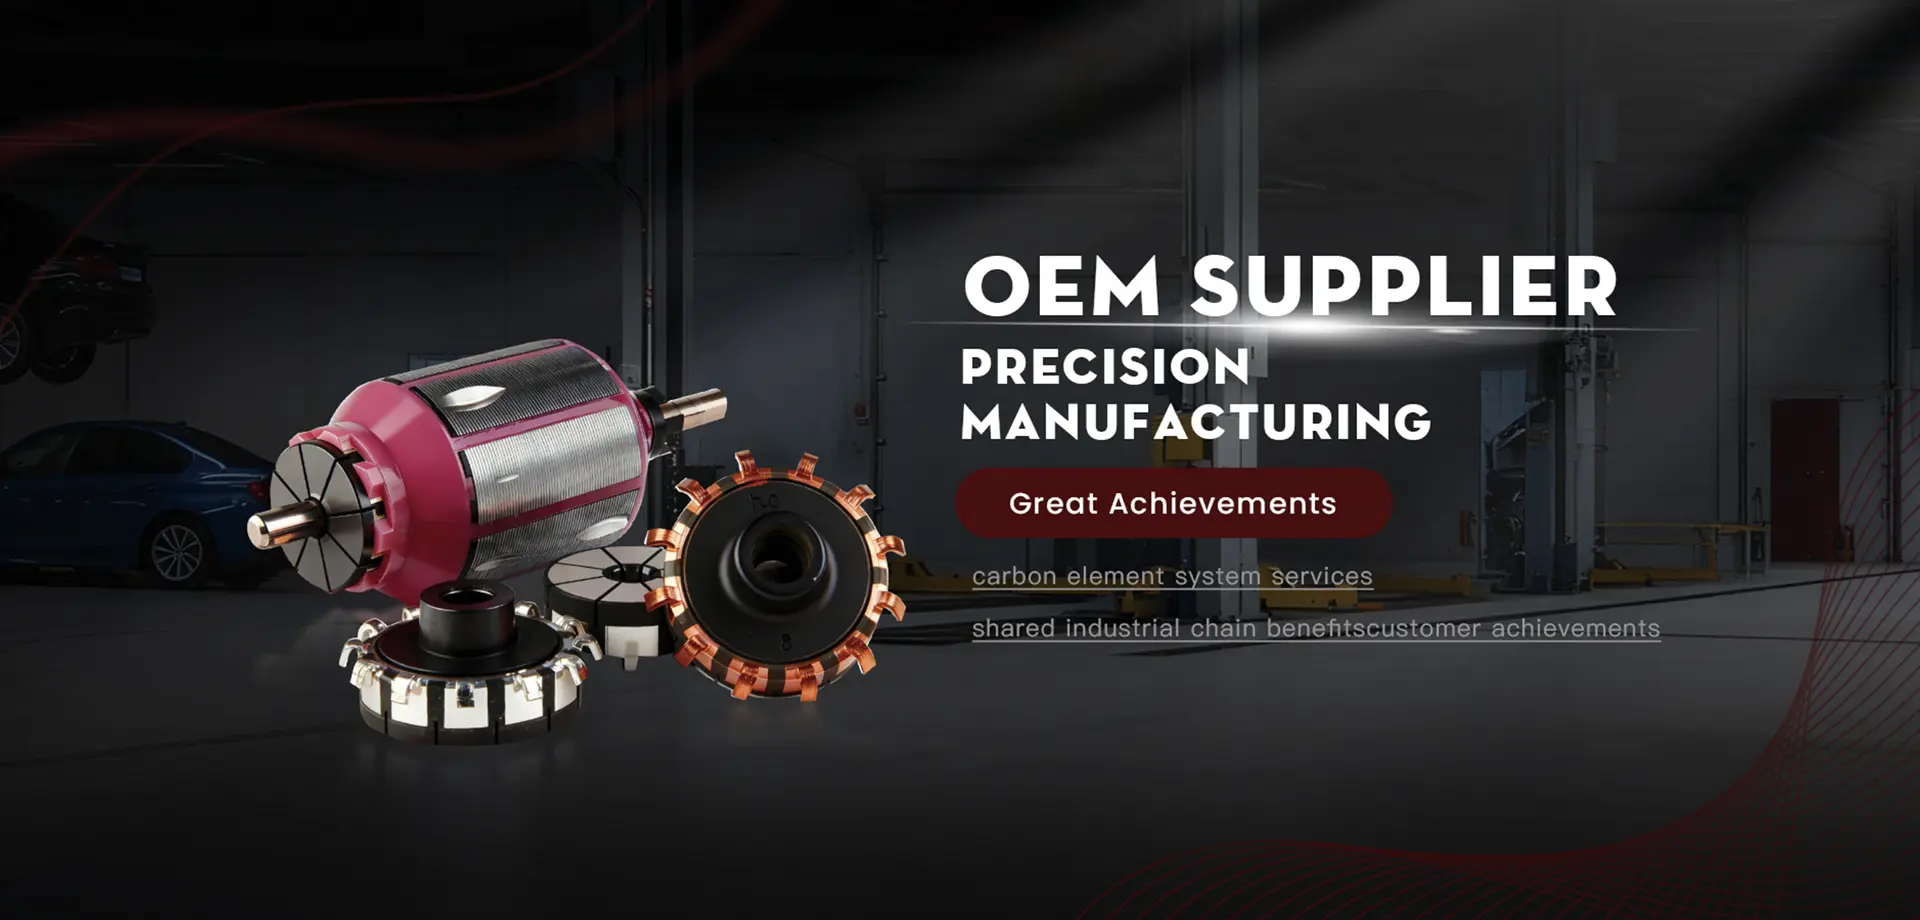
Precision wound and balanced armature assemblies integrated with high-purity graphite commutators.
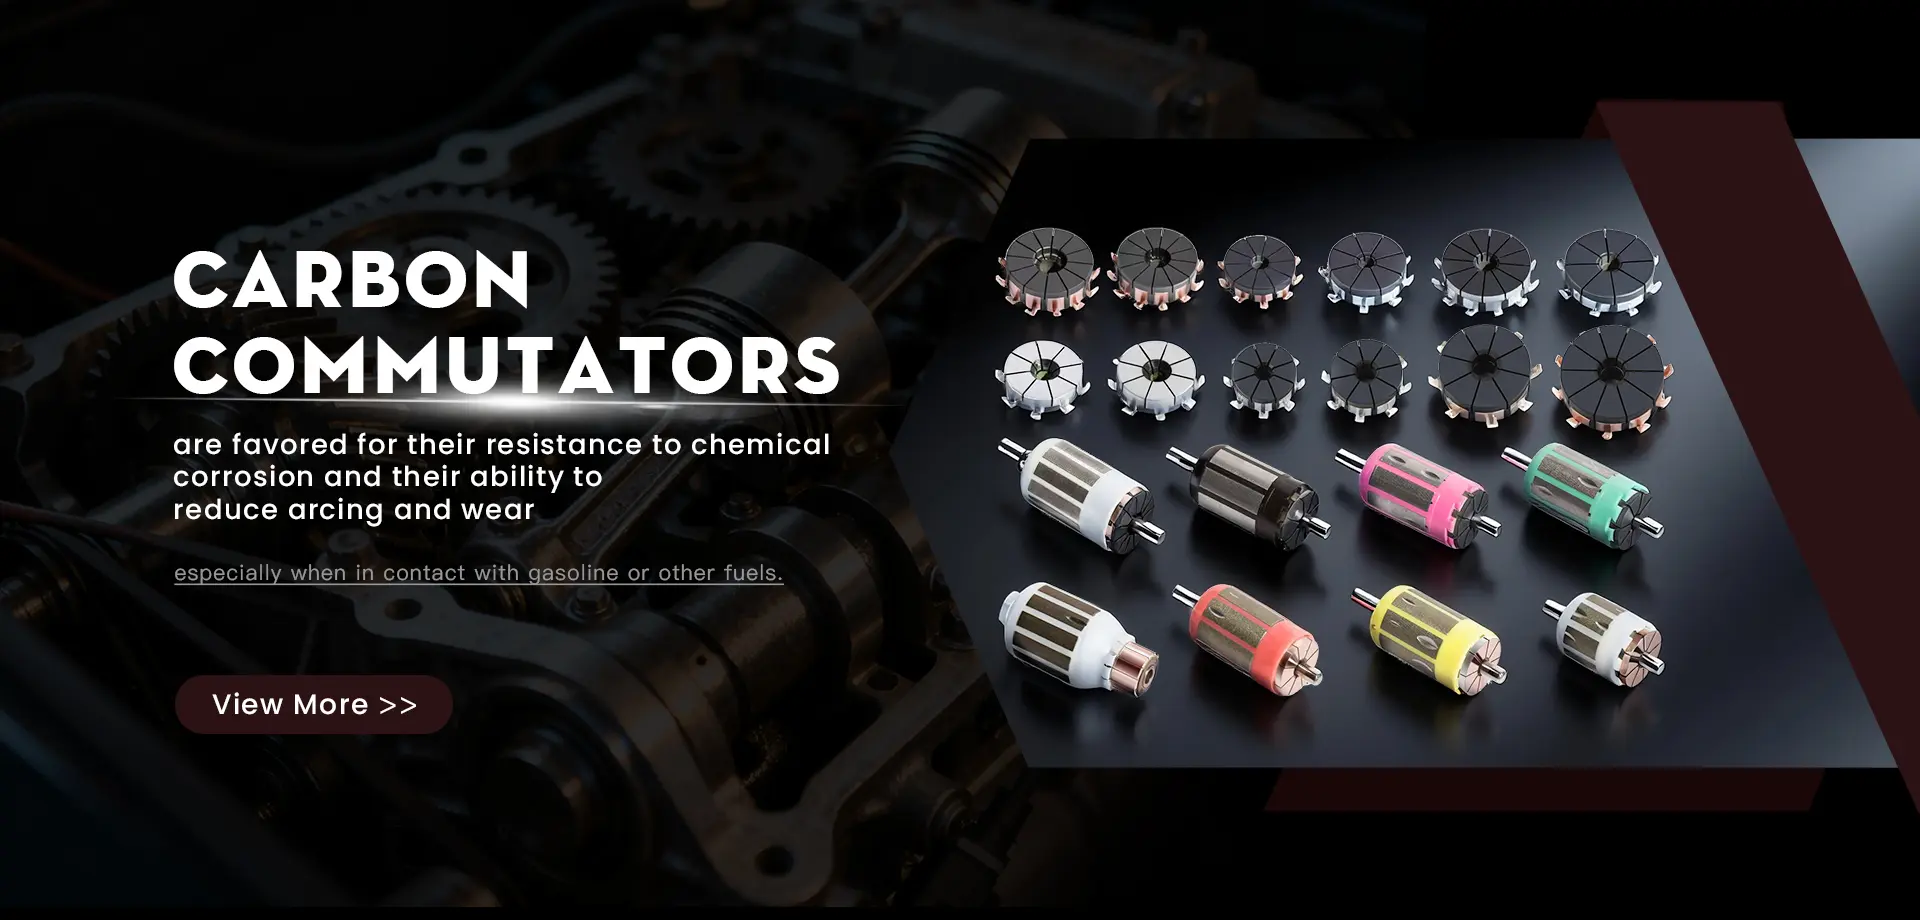
Specially formulated graphite-copper sintering resisting extreme electrochemical erosion in Flex-Fuel cars.
Segmented DC commutator engineered for ultra-high rotational velocity (12,000+ RPM) micro-actuators.
Reinforced silver-copper alloy and graphite segments built for high current density and harsh machinery.
In direct-current (DC) electromagnetic rotating machinery, the commutator operates as an intrinsically synchronized rotary mechanical rectifier and inverter. For decades, conventional direct current motors utilized segmented electrolytic copper bars insulated by mica sheets. However, as operating environments transitioned from benign ambient air to submerged immersion within aggressive hydrocarbon compounds, alcohol fuels, and variable chemical solvents, traditional copper commutation rapidly reaches its physical boundaries.
A high-performance commutator must simultaneously fulfill four conflicting engineering constraints: maintain sub-micron dimensional stability under centrifugal forces exceeding 35 m/s peripheral velocity; preserve dielectric isolation across adjoining bars under high thermal gradients; sustain stable galvanic current density transfer across brush interfaces; and withstand catastrophic chemical dissolution caused by oxygenated fuels such as ethanol (E10, E85, E100) and methanol (M15, M85).
Unlike cylindrical barrel commutators prone to high centrifugal centrifugal bar-lift, planar face disc commutators distribute wear evenly across axial brush contact surfaces, significantly mitigating mechanical vibration and brush chatter in compact fuel pump motors.
Utilizing high-glass-transition (Tg > 180°C) phenolic molding compounds reinforced with specialized inorganic micro-fibers, our commutator cores prevent segment creep, bar displacement, and moisture absorption even when continuously submerged at 70°C.
High-precision diamond CNC machining guarantees segment-to-segment height step variance ≤ 0.0015 mm and Total Indicated Runout (T.I.R.) ≤ 0.003 mm, drastically eliminating high-frequency micro-arcing and minimizing conducted Electromagnetic Interference (EMI).
In standard automotive electronic fuel injection (EFI) assemblies, the DC pump motor operates totally submerged inside the fuel tank. This submerged configuration utilizes the circulating fuel as an active coolant and lubricant for the commutator and carbon brush assembly. However, when oxygenated or alcohol-blended fuels are introduced, trace water moisture reacts with ionic sulfur, chloride, and formic acid impurities created during fuel aging. Under DC galvanic voltages, bare copper segments suffer from rapid galvanic pitting, intergranular corrosion, and accelerated spark-erosion wear. This degradation quickly increases contact resistance, reduces fuel delivery flow rate, elevates pump motor amperage, and results in catastrophic engine stalls.
To overcome this failure mode, Wenzhou Hualeao Automotive Parts Co., Ltd. engineered composite carbon-graphite commutators. By bonding a high-density, isostatically pressed synthetic graphite contact layer onto the copper conductor segment through advanced diffusion sintering and mechanical dovetail interlocking, the commutator eliminates copper contact with the liquid medium. The graphite matrix remains chemically inert to ethanol, methanol, and organic acids, reducing wear by over 80% compared to pure copper bars.
Validated empirical test data under continuous 13.5V DC submerged operation across aggressive media and extreme load cycles.
| Technical Characteristic | Traditional Copper Commutator | Hualeao Carbon-Graphite Commutator | Engineering Advantage & Impact |
|---|---|---|---|
| Ethanol / Methanol Compatibility | Poor (Pitting & Wear) | Superior (Chemically Inert) | Zero chemical degradation in E10, E85, E100, and M15–M85 fuel blends. |
| Spark Erosion & Commutation Arcing | Moderate to High; creates copper spatter | Extremely Low; self-quenching spark profile | Substantially reduced brush sparking, prolonged brush life > 3,500 hours. |
| Segment Hardness & Friction Coeff. | HB 85 – 110; μ ≈ 0.28 – 0.35 | Shore Hardness 65 – 80; μ ≈ 0.10 – 0.18 | Self-lubricating graphite film minimizes rotational mechanical drag. |
| Total Indicated Runout (T.I.R.) | ≤ 0.008 mm | ≤ 0.003 mm (Diamond Machined) | Reduces commutator ripple voltage, acoustic noise, and brush bounce. |
| High-Temperature Creep Resistance | Moderate; prone to segment bar rise | High; inorganic fiber reinforced phenolic | Structural integrity preserved under extreme thermal shocks (-40°C to +150°C). |
| EMC / EMI Compliance | Requires heavy filtering chokes | Naturally compliant with CISPR 25 Class 3/4 | Drastically reduced radiated electromagnetic emissions across RF bands. |
How our centralized production hub in Ruian, Wenzhou delivers unmatched cost structures, vertical material integration, and rapid production velocity for global Tier-1 clients.
Situated at the heart of Ruian—China's premier capital of automotive components—we leverage an immediate 15-kilometer radius supply chain encompassing precision stamping, mold manufacturing, and specialized copper smelting.
From raw isostatic graphite block procurement and ultra-fine carbon powder micro-milling to proprietary high-temperature resin compounding, full vertical integration yields absolute batch-to-batch chemical homogeneity.
Historically dependent on European and Japanese commutator imports, Tier-1 automotive fuel pump builders achieve 30% to 45% bill-of-materials (BOM) cost reduction by transitioning directly to Hualeao's benchmarked quality.
Accelerated CAD/CAM mold engineering allows us to turn custom engineering blueprints into functional first-article samples within 14 working days, drastically compressing vehicle platform development cycles.
Procurement directors and quality engineers at multinational automotive Tier-1 corporations face stringent operational hurdles when sourcing micro-motor components. The commutator is a zero-defect critical component: if a fuel pump commutator fails prematurely, the entire vehicle experiences engine shutdown, triggering massive automotive recall liabilities. Consequently, Hualeao adheres to rigorous automotive quality management systems that govern every stage of production.
We fully support the Production Part Approval Process (PPAP Level 3), furnishing comprehensive DFMEA, PFMEA, Control Plans, Process Capability Studies (Cpk ≥ 1.67), and Gage R&R measurement variance analyses.
Our carbon commutator research was formally acknowledged and incorporated into China's 11th Five-Year Plan as a critical new-vehicle energy conservation and emission reduction technology program.
All resin compounds, graphite blends, and copper conductor alloys fully comply with European RoHS 3.0 and REACH chemical limits, complete with full material tracking within the International Material Data System (IMDS).
To eliminate international sourcing friction for clients across North America, Latin America (notably Brazil's flex-fuel ethanol market), Western Europe, and Southeast Asia, Hualeao provides dedicated bilateral technical support. Our engineering department reviews customer 2D component drawings (GD&T) and 3D STEP/IGES models to evaluate winding tang clearance, press-fit shaft interference tolerances, and brush commutation overlap. We maintain multi-lingual sales engineers who provide cross-time-zone communication, DDP/CIF logistics coordination, and direct technical consultations.
From compact high-RPM motorcycle fuel pumps to heavy construction machinery and harsh marine applications, our products adapt to rigorous operational cycles.
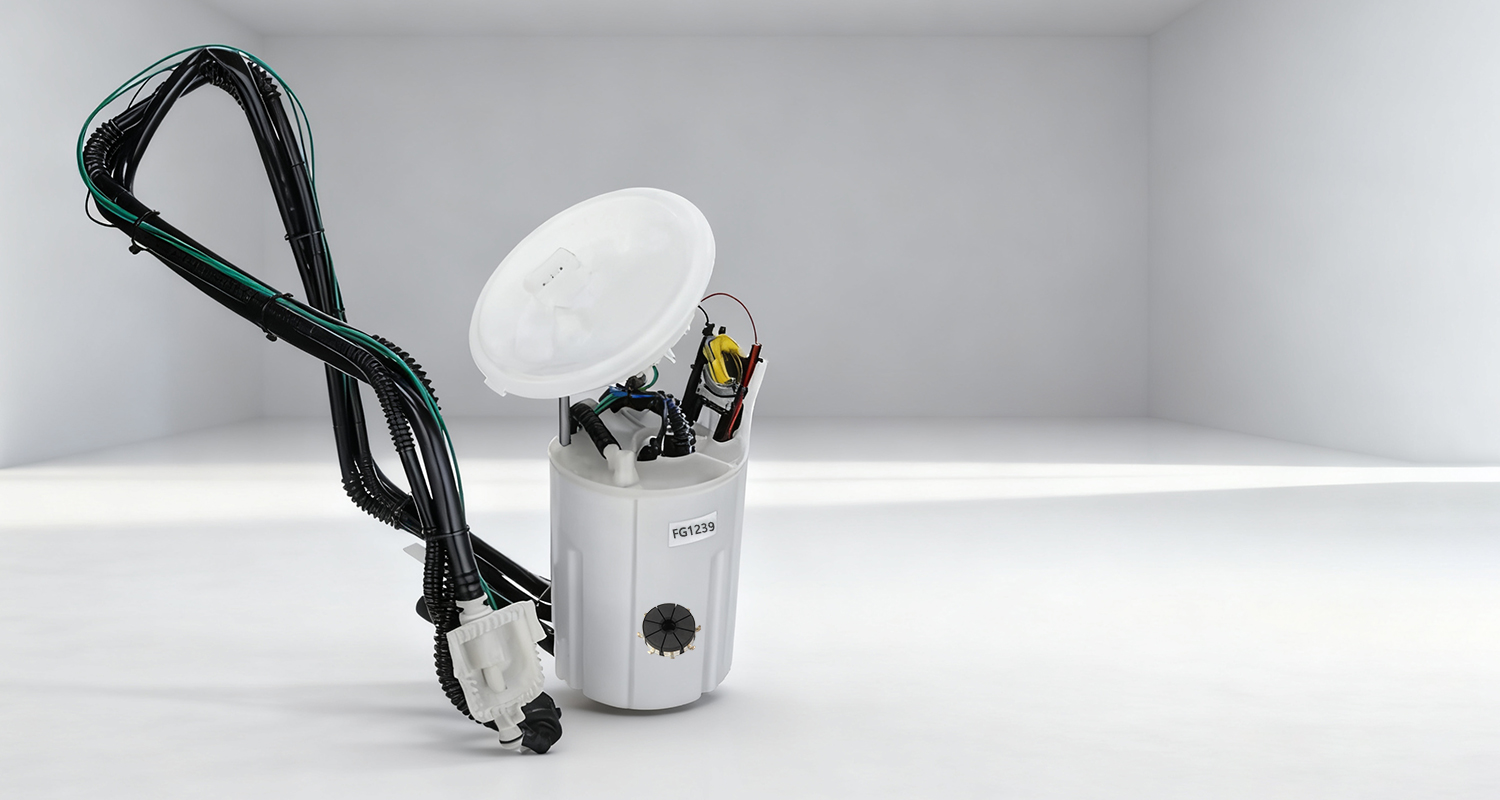
Submerged in flex-fuel tanks, operating from freezing cold-start (-40°C) to high-speed highway cruising with zero electrochemical corrosion.
Explore Applications
Ultra-compact disc commutators capable of handling 10,000+ RPM rotor speeds in restricted fuel tank envelopes with low parasitic drag.
Explore Commutators
Heavy excavators and cranes subject to constant mechanical shock, continuous 24-hour operation, and low-grade contaminated diesel/biofuel.
Explore Assemblies
In high-humidity, salt-fog maritime environments, our proprietary composite material resists galvanic salt-spray oxidation indefinitely.
Contact EngineersWhile the rise of electric propulsion has accelerated brushless DC (BLDC) motor adoption in primary vehicle traction drives, brushed DC machines with advanced carbon commutators continue to dominate auxiliary automotive actuators, micro-motors, and fuel supply subsystems. The industrial drivers behind this sustained preference are definitive:
Brushed DC motors do not require complex microcontroller inverters, Hall-effect magnetic sensors, or sensitive gate-driver silicon. In cost-critical automotive applications, brushed architectures reduce overall electronic BOM cost by upwards of 40%.
With global decarbonization driving the adoption of carbon-neutral synthetic fuels, E85 bioethanol, and methanol, conventional copper systems fail. Carbon commutators are the proven, high-reliability solution enabling these transitional fuels.
In enclosed fuel delivery environments, external silicon semiconductor controllers pose heat-dissipation challenges. Mechanical carbon commutation inside the hermetically sealed pump remains the benchmark for intrinsically safe packaging.
Furthermore, material sciences continue to push carbon commutator boundaries. Innovations in resin binder graphitization, nano-scale copper impregnation, and laser-assisted surface texturing are further lowering interfacial contact resistance while doubling operational lifecycle limits to exceed 10,000 continuous operating hours.
Detailed answers regarding technical specifications, minimum order quantities (MOQ), custom tooling, and material longevity.
Review our secondary selection of specialized graphite discs, armatures, sensors, and assemblies engineered for demanding duty cycles.
Advanced diffusion-bonded graphite layer designed to eliminate copper pitting in high-temperature E100 fuels.
Precision-balanced segment arrangement engineered for direct insertion on high-speed automated winding lines.
Complete low-noise electric fuel pump core engineered for whisper-quiet in-cabin acoustic performance (< 38 dB).
Exhaust gas analyzer offering rapid light-off heating element technology to comply with Euro 6 emission standards.
Multi-pole wound armature core integrated with a planar carbon commutator for uniform flux transfer.
Specially compounded non-porous graphite preventing fuel seepage into armature windings.
Miniature DC motor commutator engineered for precision throttling, valve control, and automotive servo drives.
Built-to-print prototypes tailored to custom client drawings, unique tang profiles, and specific brush grades.
Have a technical drawing, prototype sample, or OE reference number? Submit your specifications directly to our engineering team in Ruian, Wenzhou for feasibility analysis and a competitive volume quotation.
Facility Address: Building 5, Lianjiang Industrial Park, Pantai Street, Ruian City, Wenzhou, Zhejiang Province, China
Telephone Inquiry: +86 0577-66811811 | Direct WhatsApp: +86 15067763878
Direct Engineering Email: [email protected]
