Precision-manufactured fuel pump rotors, dynamic-balanced armatures, and corrosion-resistant graphite commutators compatible with global OEM standards and demanding aftermarket specifications.

Advanced disc and barrel carbon commutators designed for submerged EFI fuel pump armatures running high-blend ethanol.

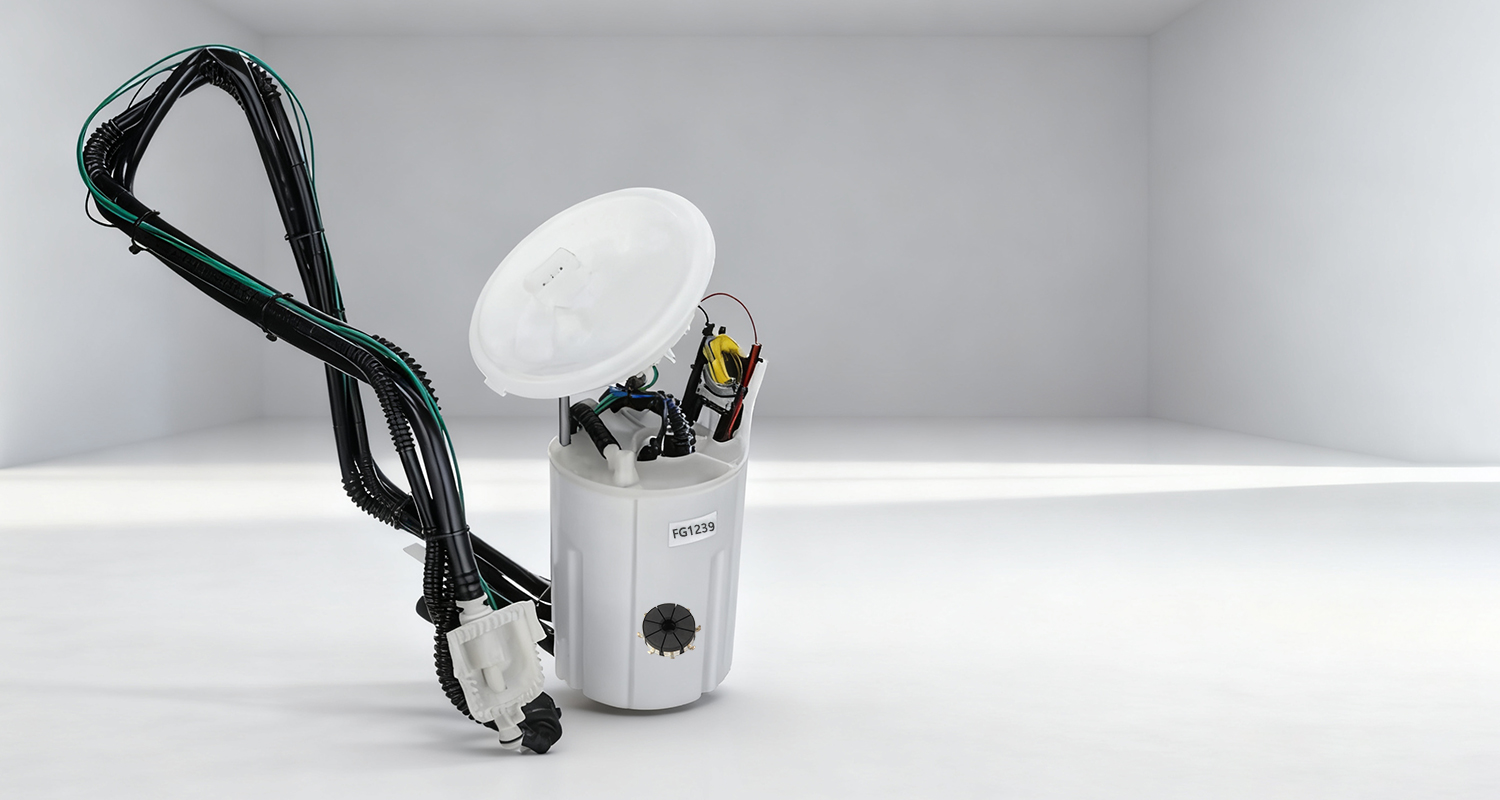
Dynamic-balanced fuel pump complete core assembly delivering linear fuel pressure curve and low electrical noise.

Heavy-duty precision-engineered carbon commutator proven in high-flow aftermarket and OEM replacement platforms.

Fast-switching zirconium lambda sensor matching OEM 89465-0E040 for closed-loop air-fuel calibration.
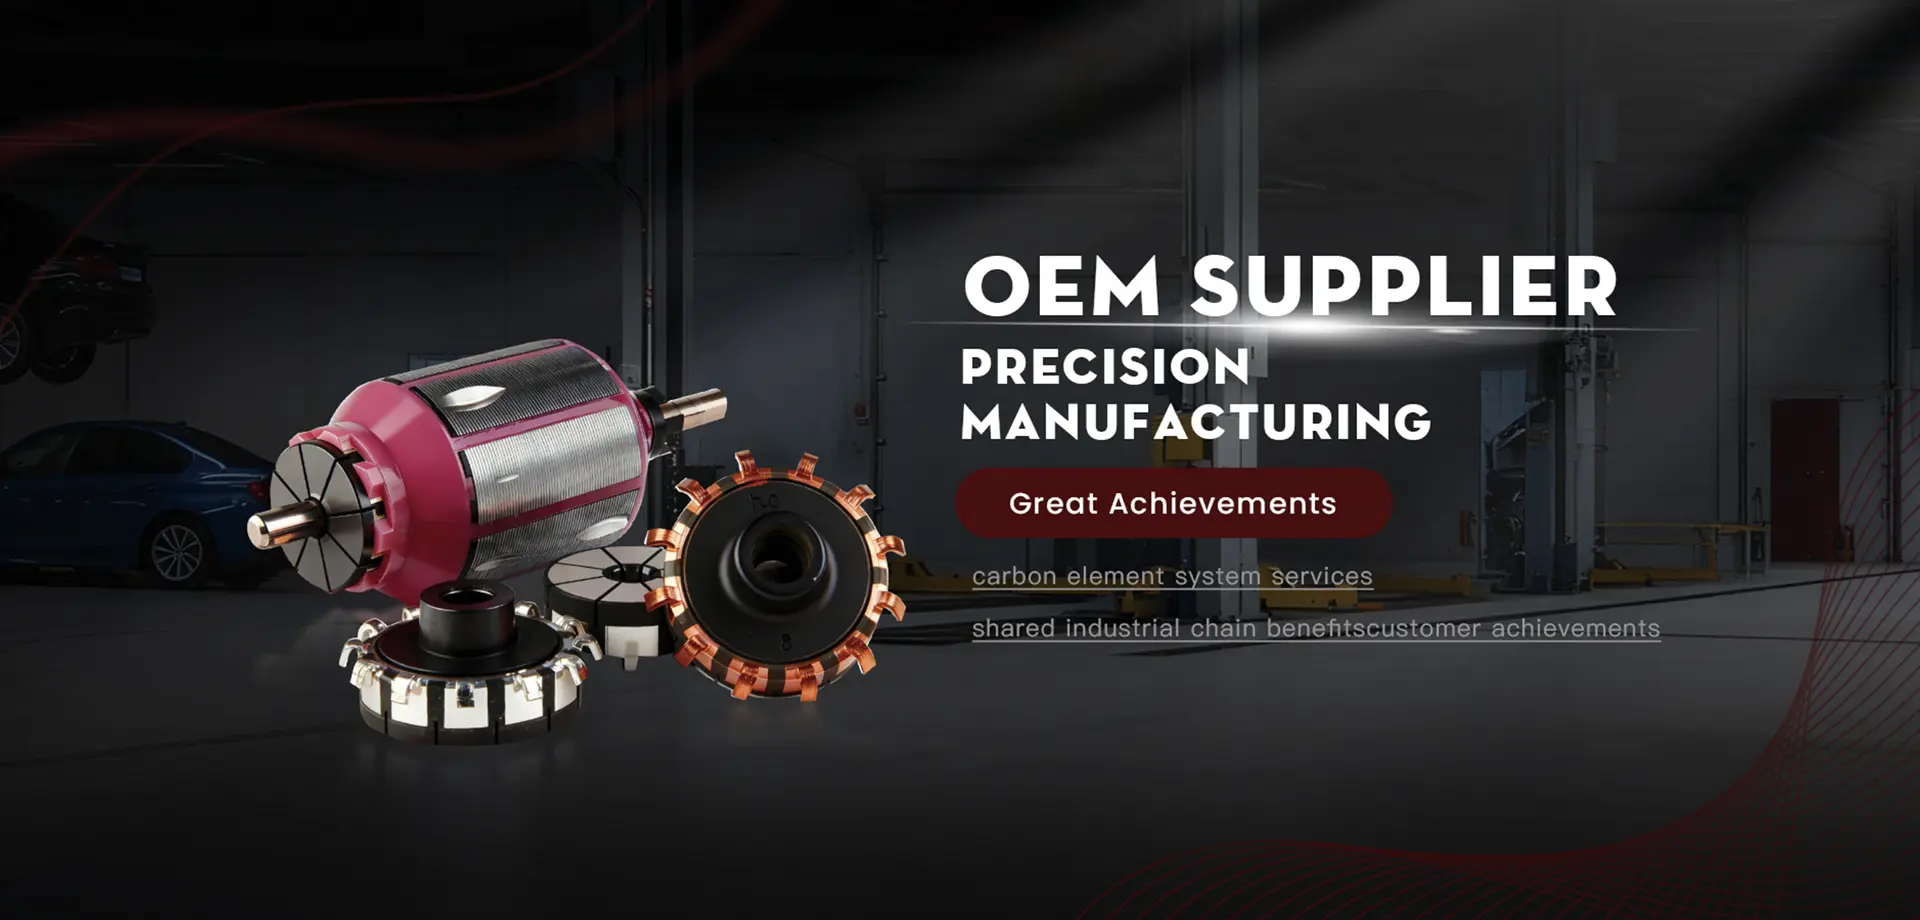
High-silicon steel laminated armature stack wound with Class-H insulated copper wire for long-term continuous duty.
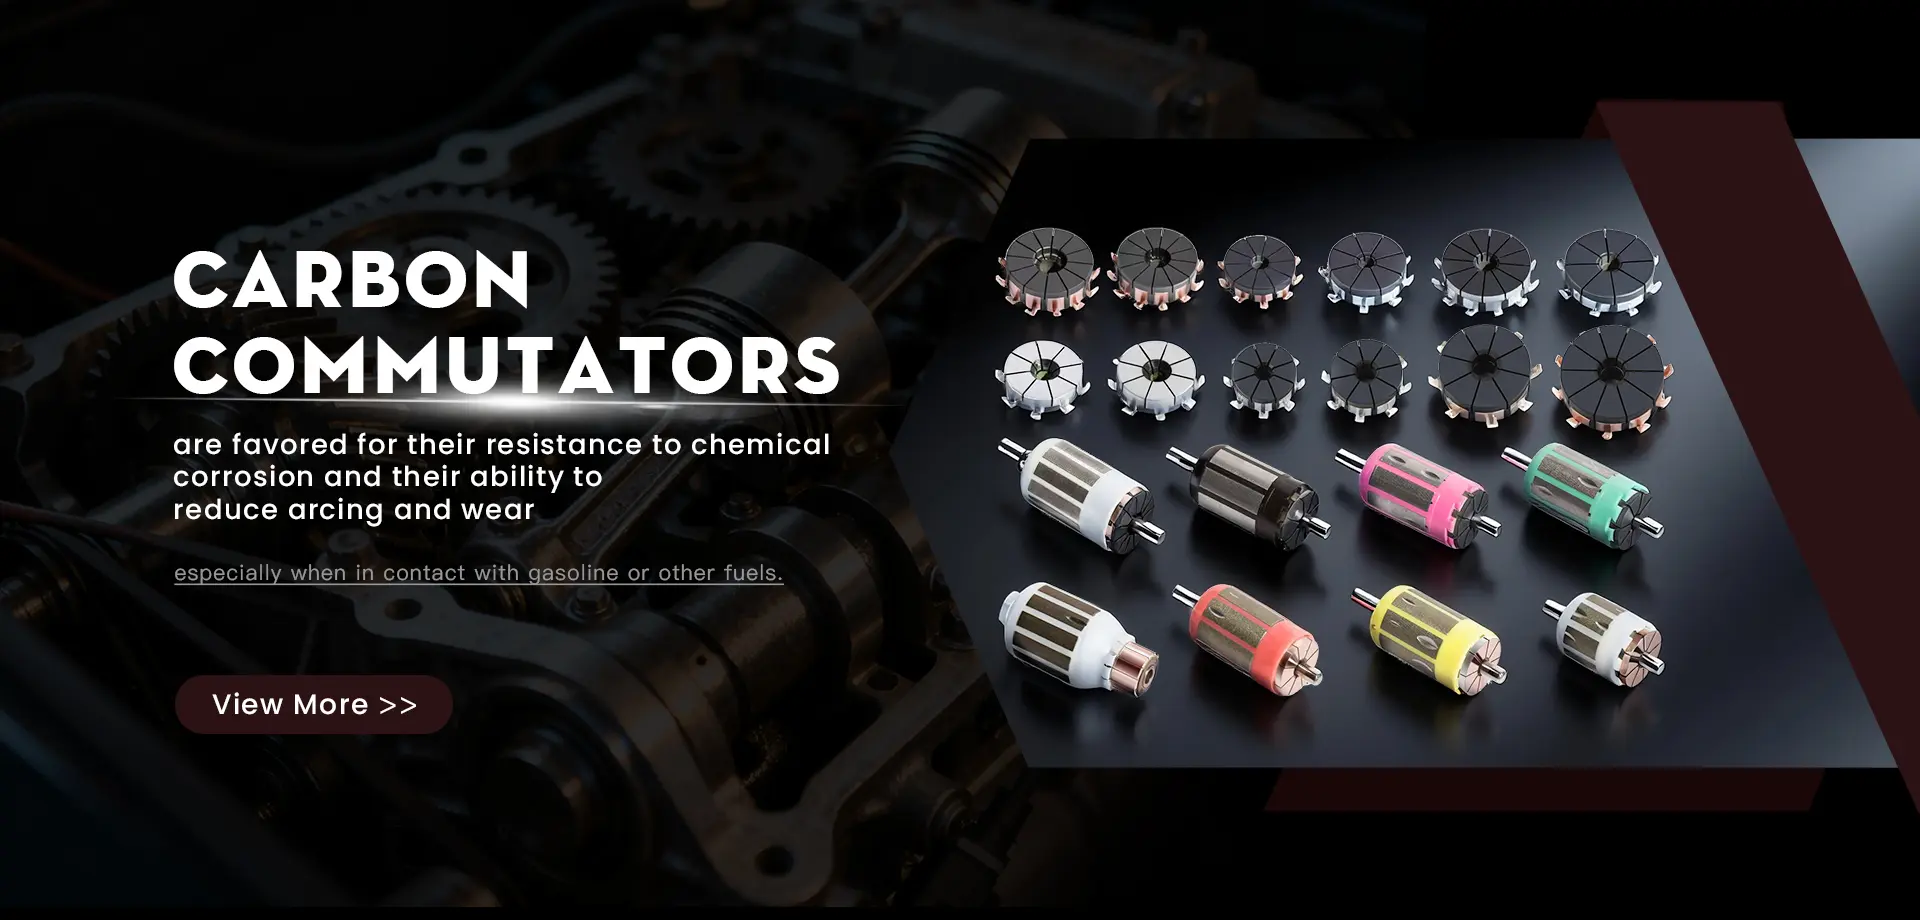
Planar commutator technology engineered for high-density compact fuel pumps, preventing spark erosion in corrosive media.
Pre-balanced motor core with pressed carbon commutator, micro-welded coils, and anti-cavitation shaft grooves.
Build-to-print motor armatures manufactured to exact dimensional tolerances, slot angles, and magnetic flux profiles.
As internal combustion engines (ICE), flex-fuel systems, and extended-range electric vehicles (EREVs) encounter corrosive alternative biofuels, the internal fuel pump motor armature represents the critical failure point for vehicle reliability.
Global transition to ethanol blends (such as E10 in North America/Europe, E27 to E100 in Brazil) and methanol blends (M15 to M85 across Asia-Pacific) creates severe electro-chemical de-alloying in traditional metallic components. Copper commutators suffer rapid electrochemical erosion and galvanic pitting when submerged in alcohol fuels with trace moisture. Hualeao utilizes high-density isostatic graphite commutators chemically fused to copper substrate bars, eradicating chemical degradation and delivering an unyielding mechanical contact layer.
Modern hybrid powertrains operate with discontinuous engine engagement. Fuel pump armatures face intermittent start-stop cycles where high inrush currents surge across cold commutators. Our optimized armature winding configuration, combined with precision Class-H resin trickle impregnation, resists repeated thermal shock spikes up to 180°C. This avoids internal winding short circuits, ensures instantaneous fuel line pressurization, and protects fuel rails from pressure cavitation.
With passenger cabin noise floors dropping drastically in modern automotive designs, fuel pump resonance and brush arcing must be strictly controlled. Hualeao armatures are dynamically balanced under ISO 1940 G1.0 thresholds. Combined with tailored carbon-brush contact friction coefficients, our components minimize acoustic hum (< 38 dB(A) at operational RPM) while significantly curtailing electromagnetic radiation that could interfere with CAN-bus telematics.
A microscopic examination of why Hualeao electronic fuel pump armatures match and exceed foreign tier-1 benchmark components in mechanical rigidity, electrical commutation efficiency, and lifecycle durability.
Our armature cores use low-iron-loss, high-permeability cold-rolled non-oriented silicon electrical steel sheets (0.35mm to 0.50mm thickness). High-speed progressive stamping tooling ensures slot profiles have zero burr margins (< 0.01mm), eliminating microscopic lacerations to slot insulation paper and ensuring high magnetic saturation with reduced eddy current losses.
Rotating at angular velocities exceeding 10,000 RPM, uncorrected rotor mass imbalances create destructive bearing wear and shaft runout. Every Hualeao fuel pump armature undergoes automated double-plane dynamic balance milling. Removal of balancing weight via automated cutter notches guarantees residual imbalance levels below 0.2 mg·mm, maintaining hydrodynamic axial stability.
Unlike simple copper-commutator pumps that spark and melt in bio-alcohols, our graphite-based segments are engineered with proprietary phenolic binder networks. Commutator face runout is held within 0.003 mm total indicator reading (TIR), preventing brush jump, reducing high-frequency arcing, and guaranteeing flat wear tracks over 150,000 km of vehicle operation.
| Engineering Parameter | Standard Commercial Armatures | Hualeao Heavy-Duty Armatures | Validation / Verification Method |
|---|---|---|---|
| Commutator Segment Material | Electrolytic Tough Pitch Copper (ETP) | Isostatic Nano-Graphite Matrix + Cu Base | Energy-Dispersive X-Ray Spectroscopy (EDS) |
| Ethanol Corrosion Degradation (E85) | Pitting & Segment Lift within 400 hrs | Zero Degradation / Stable at > 3,500 hrs | ASTM D5185 Immersion Accelerated Endurance |
| Dynamic Rotor Balancing Grade | ISO 1940 G6.3 to G2.5 | ISO 1940 G1.0 Precision Standard | Dual-Plane Schenck Dynamic Balance Analysis |
| Total Radial Runout (TIR) | ≤ 0.015 mm | ≤ 0.003 mm - 0.005 mm | Non-Contact Laser Micrometer Measurement |
| Winding Wire Thermal Rating | Class F (155°C) Conventional Enamel | Class H (180°C - 200°C) Polyamide-imide | Dielectric Breakdown Voltage at Temperature |
| Shaft Hardness & Surface Finish | HRC 48-52 / Ra 0.4 μm | HRC 58-62 / Superfinished Ra ≤ 0.1 μm | Rockwell Hardness & White Light Interferometry |
From compact ultra-high-revving motorcycle tanks to commercial marine vessels facing corrosive maritime atmospheres, our armatures deliver steady fuel delivery across demanding environments.
Operating from our 6,200 m² high-precision facility in Ruian, Wenzhou, Hualeao utilizes end-to-end automated testing to guarantee zero PPM defect rates for global supply chains.
Every single armature moving along our assembly cells is subjected to computerized impulse surge testing, inter-turn insulation testing (2,000V DC breakdown test), and winding resistance symmetry inspection to identify sub-micron copper necking or winding shorts prior to encapsulation.
High-resolution telecentric optical sensors scan every carbon commutator face for surface porosity, micro-cracks, segment gap alignment, and micas undercutting depth. Dimensional tolerances for shaft journals are verified to sub-micron standards, keeping concentricity tightly regulated.
Certified across more than 10 qualification standards, our manufacturing workflows follow strict PPAP (Production Part Approval Process) Level 3 documentation, FMEA defect forecasting, and full heat-lot material traceability from raw copper ingot to finished palletized armature assemblies.
Strategic material and design evolution as powertrain architectures embrace zero-emission e-fuels, cryogenic hydrogen combustion (H2-ICE), and variable-speed pulse-width modulated (PWM) pumping units.
While brushless motors enter premium sectors, high costs and driver-inverter electronics failures in fuel tanks keep optimized brushed motors dominant in 82% of global vehicles. Hualeao is closing the gap with carbon commutators featuring nano-diamond additives, extending operational life toward 8,000 hours without the electronics cost penalties of BLDC systems.
Synthetic e-fuels created via captured CO2 and green hydrogen possess unique non-lubricating dry properties that cause premature scuffing on normal commutators. Our advanced research teams in Wenzhou are piloting self-lubricating carbon-graphite formulas infused with synthetic polymers to maintain ultra-low friction even in ultra-low lubricity fuels.
Modern Engine Control Units (ECUs) constantly vary fuel pump speed via high-frequency pulse-width modulation (PWM) to conserve electrical energy. Hualeao armatures feature low-inductance segmented winding topologies that curtail voltage kickback spikes, preserving brush life and preventing thermal hot spots during frequent speed transitions.
Comprehensive engineering insights from our Chief Technology Officer and R&D laboratories regarding fuel pump armature specification, maintenance, failure modes, and customization.
Explore our complete catalog of electric fuel pump rotors, custom motor armatures, carbon disc commutators, and engine management sensors ready for global volume distribution.
Specially treated graphite-copper segment commutator built to endure high methanol concentration fuels without flaking.
High-output in-tank fuel pump unit delivering silent, vibration-free turbine pumping action for modern direct injection engines.
Reinforced carbon commutator armature core engineered for commercial transport and fleet service running high annual mileage.
Precision ceramic sensing element offering rapid activation within 15 seconds to cut cold-start exhaust emissions.
Industrial grade DC motor armature wound with 200°C rated enameled magnet copper wire and high-dielectric epoxy slot liners.
Planar disc face commutator providing compact axial profile, ideal for low-profile modular fuel delivery assemblies.
Built with oversized shaft diameters and high-permeability steel laminations to power fuel feed pumps in severe construction machinery.
Complete custom co-development program matching customer specific drawings, shaft splines, and special brush material pairings.
