Engineered for full bio-fuel compatibility (E10, E85, E100, M15-M85), superior dynamic balancing, and extended operational lifespan across extreme duty cycles.

Carbon-graphite disc commutators designed specifically for alcohol-submerged armatures. Eliminates electrochemical copper erosion.
View Commutators
High-pressure electronic fuel injection assemblies featuring dynamic balanced micro-rotors and low-noise operational acoustic profiles.
View Fuel Pumps
Direct ECU feedback lambda sensors maintaining stoichiometric closed-loop accuracy across variable ethanol air-fuel ratios.
View Sensors
Our flagship high-conductivity carbon commutator engineered to withstand aggressive sulfurized and moisture-laden bio-ethanol fuels.
Explore Hot Products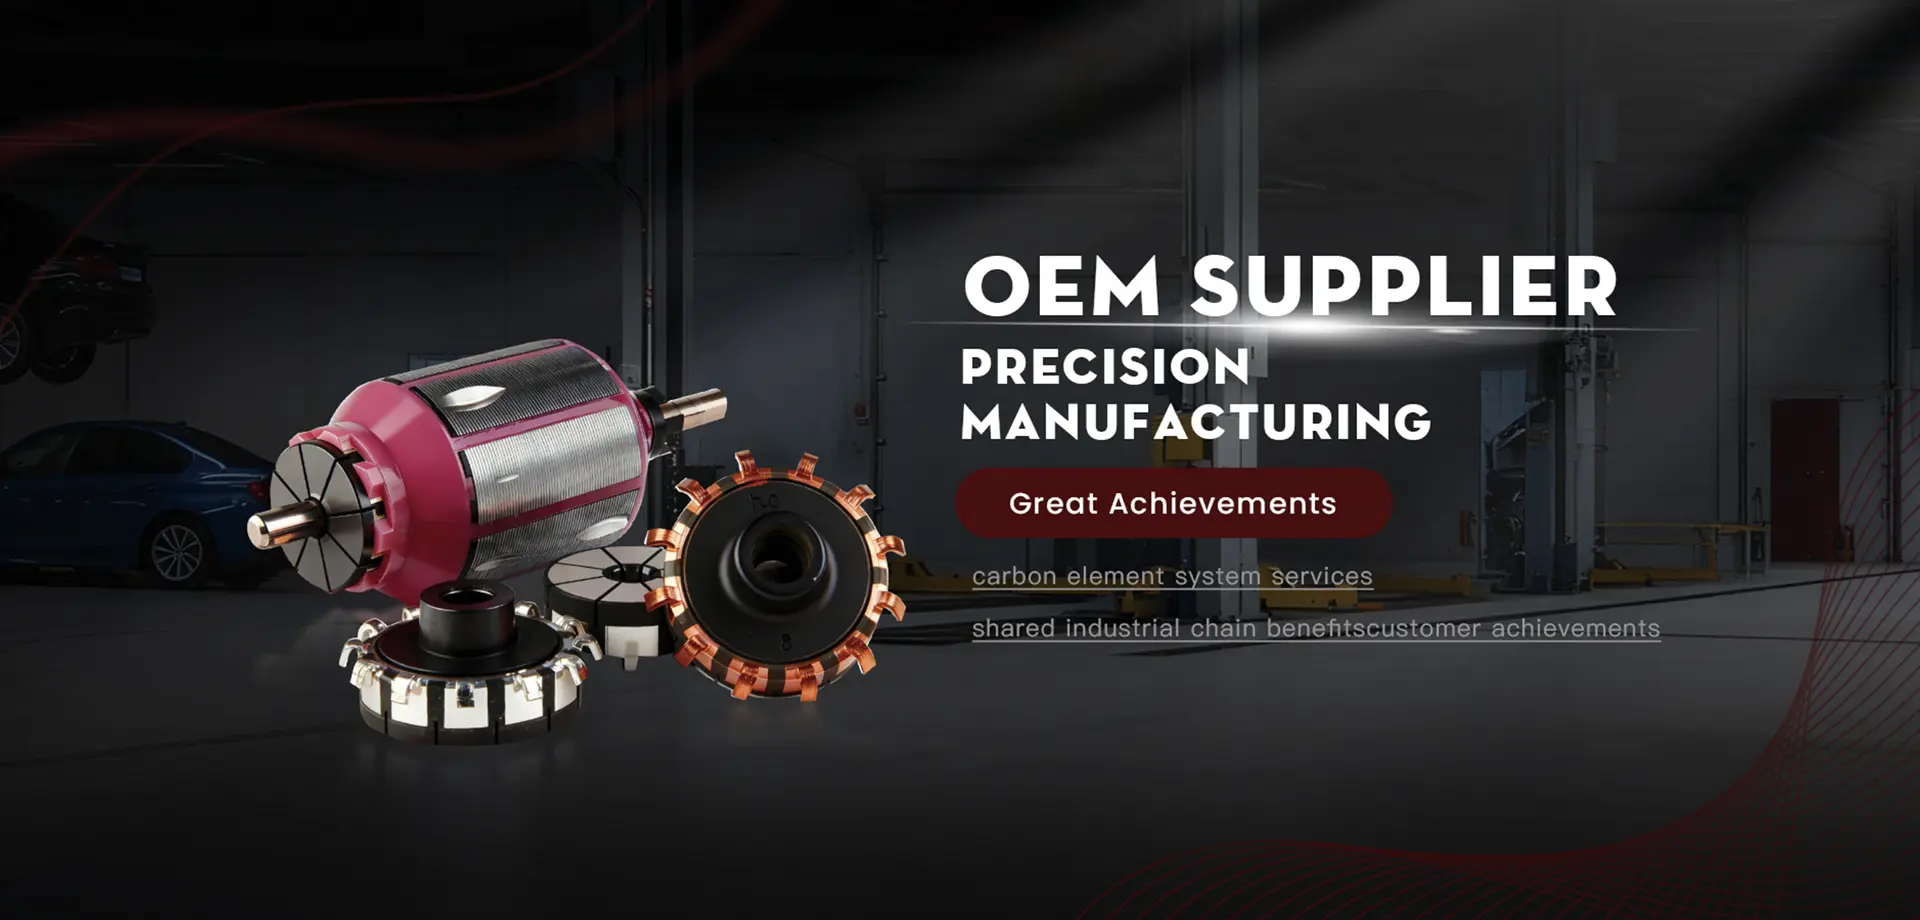
Ultra-precision dynamic balance armatures designed with high-density copper winding and ethanol-grade slot insulation varnishes.
View Armature Series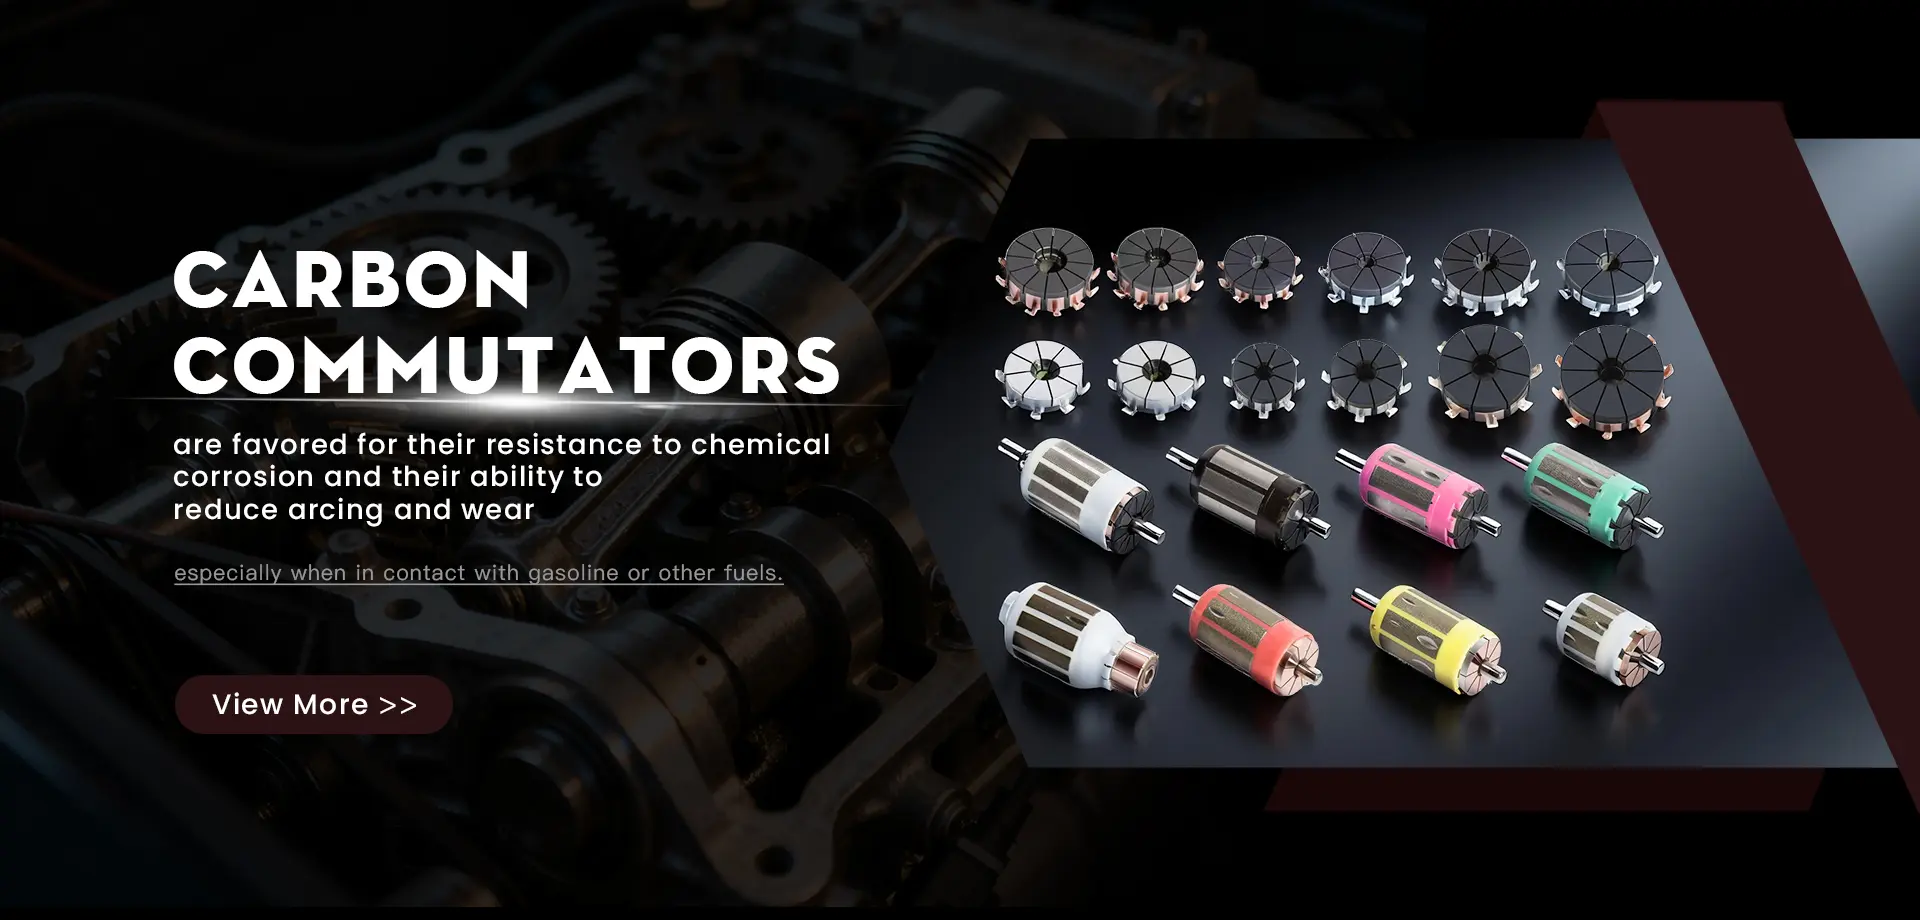
Specialized sintered graphite compounds engineered to prevent pitting, brush dusting, and dielectric breakdown in aggressive alcohols.
Discover Solutions
Sub-micron dimensional runout tolerance commutators ensuring zero arcing and whisper-quiet motor operation in flex-fuel vehicles.
Request Technical Sheet
Bespoke segment numbers, custom shaft lengths, and engineered graphite-copper alloy compositions fabricated to customer 2D/3D CAD prints.
Request CAD / SpecsA systematic analysis of electrochemical corrosion mechanisms, tribological brush interfaces, and metallurgic advancements within submerged alternative fuel motor environments.
Ethanol (C2H5OH) and methanol (CH3OH) introduce high hygroscopicity, conductivity, and acidity into automotive fuel rails. In submerged electronic fuel pumps (EFIs), conventional electrolytic copper commutators undergo severe galvanic oxidation, rapid dielectric film breakdown, and spark erosion within hours of running high-percentage alcohol blends (E85/E100).
By replacing pure copper contacts with high-purity, resin-impregnated graphite-carbon matrix segments bonded to copper bases, modern commutators establish an inert, self-lubricating tribological film. This neutralizes ionic transfer, suppresses spark energy, and stabilizes contact resistance across -40°C to +135°C operating temperatures.
Armature rotors operating at speeds between 6,000 and 12,000 RPM demand stringent dynamic balancing to prevent mechanical shaft deflection and premature carbon brush disintegration. Utilizing automated multi-plane milling balancing machines, modern rotors achieve residual unbalance figures well within ISO 1940 Grade G1.0.
| Performance Parameter | Standard Copper Armature Rotor | Hualeao Carbon-Graphite Rotor | Engineering Gain / Impact |
|---|---|---|---|
| E85 / E100 Bio-Ethanol Compatibility | Poor (< 150 Operating Hours) | Superior (> 3,500 Operating Hours) | Complete prevention of segment delamination & copper dissolution |
| Dynamic Total Radial Runout (T.I.R.) | ≤ 0.015 mm | ≤ 0.003 mm | Drastic reduction in brush bounce and high-frequency acoustic noise |
| Galvanic Corrosion Index | High (Anodic pitting in fuel moisture) | Chemically Inert (Zero galvanic reaction) | Long-term electrochemical stability in sour gas and ethanol phase separation |
| Spark Arcing Energy | Moderate to High (> 35 mJ) | Low-Suppressed (< 8 mJ) | Eliminates spark-induced pitting; ensures compliance with CISPR 25 EMC limits |
| Maximum Working Temperature | 105°C | 160°C Continuous | Compatible with dry-run conditions and engine-bay heat soak cycles |
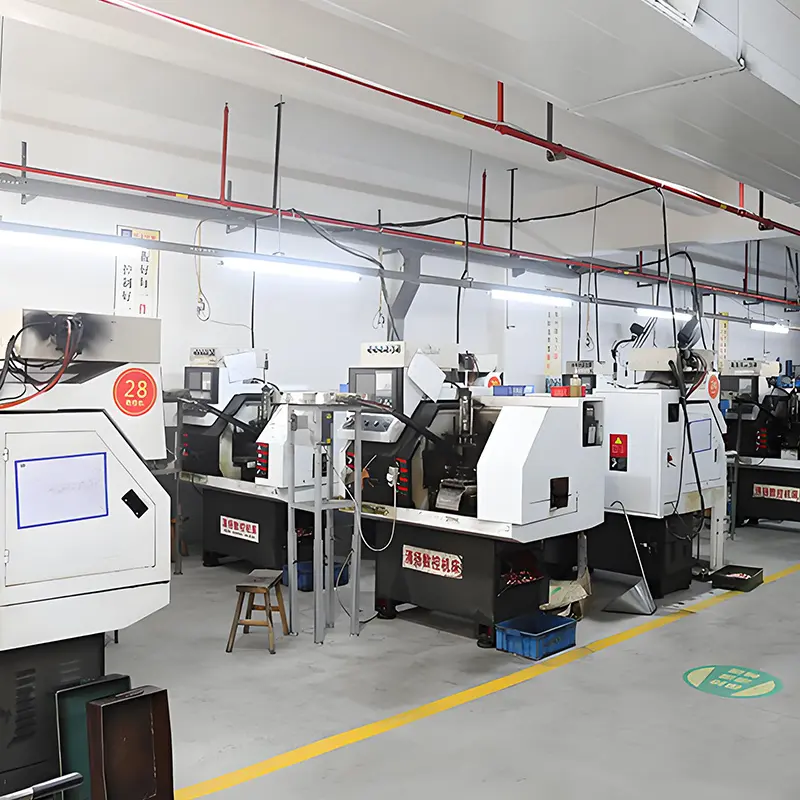
Located in Ruian, Wenzhou—China's capital of automotive electronics—Wenzhou Hualeao Automotive Parts Co., Ltd. operates a vertically integrated production ecosystem designed to mitigate global supply disruptions. By mastering every step from raw synthetic graphite formulations to high-speed dynamic winding, we deliver tier-1 level repeatability.
Officially awarded for breakthrough innovations in reducing vehicular energy consumption through low-friction micro-commutator architecture.
Automated vision systems monitor outer diameter, concentricity, bar-to-bar mica undercut depth, and weld joint resistance on 100% of finished assemblies.
Domestic supply network integration delivers a 25%–40% cost advantage compared to European and Japanese imports while maintaining identical metallurgical properties.
Engineered for global reliability. Backed by scalable manufacturing plants and rigorous laboratory compliance.
Every armature rotor and commutator segment undergoes non-negotiable gateway verifications prior to dispatch.
Spectrometric verification of synthetic carbon purity, resin density, and uniform copper grain alignment to ensure anti-oxidation integrity.
Micro-controlled thermal profile bonding ensuring superior physical sheer adhesion between carbon contacts and copper core substrate.
High-precision turning of the brush contact track to achieve surface roughness below Ra 0.2 µm and bar-to-bar steps under 0.002 mm.
Continuous endurance testing submerged in high-concentration ethanol bath under full 14.5V continuous dynamic electrical load.
Operating environments where fuel quality varies widely and downtime results in catastrophic operational losses.
Powers passenger and commercial vehicles running flexible fuel options ranging from standard E10 to pure E85 and E100. Guarantees uniform fuel rail pressure and instantaneous throttle response.
Miniaturized armature rotors capable of sustained 10,000+ RPM under tight volumetric constraints and severe vibration profiles inherent to two-wheelers and all-terrain recreational vehicles.
Excavators, wheel loaders, and agricultural tractors operating in high-particulate, harsh-temperature job sites where contaminated or water-cut fuels frequently destroy standard pumps.
Submerged fuel delivery systems subjected to saline moisture ingress, high humidity, and prolonged seasonal storage where bio-fuels separate into corrosive water-alcohol phases.
How international OEMs and tier-1 fuel module manufacturers navigate biofuel mandates, decarbonization shifts, and supply security.
With Brazil's widespread adoption of hydrous ethanol (E100) and North American EPA mandates boosting E15 and E85 blender pumps, pump manufacturers require Tier-1 certified carbon armatures that withstand severe seasonal alcohol dilution without field failure.
As the European Union implements strict Euro 7 emission targets, the integration of synthetic e-fuels and bio-methanol requires micro-motor commutators that exhibit zero resin swelling and ultra-low hydrocarbon permeability.
Global assemblers are aggressively transitioning away from high-cost single-source European commutator makers. Direct sourcing partnerships with certified Chinese manufacturers like Hualeao offer immediate margins and compressed R&D cycles for new pump platforms.
Send our senior engineering team your 2D/3D CAD drawings (STEP, DWG), OEM part numbers, or physical benchmark samples. We deliver DFM feedback within 24 hours.
Comprehensive technical answers regarding rotor dynamics, material science, and custom OEM manufacturing.
Standard copper commutators fail in alcohol blends primarily due to electrochemical corrosion and chemical dissolution. Ethanol readily absorbs atmospheric moisture and often contains trace amounts of acetic acid and ionic chloride contaminants. When an electric potential (12V–14V) is applied across submerged copper segments, galvanic micro-cells form, causing rapid anodic leaching of the copper. This results in segment pitting, heavy electrical arcing, brush wear acceleration, and eventual total motor circuit failure. Carbon-graphite segments are chemically non-reactive, eliminating this failure path completely.
Hualeao utilizes a proprietary sintered carbon-graphite composite impregnated with high-grade synthetic phenolic or epoxy resins. The graphite flakes provide optimal electronic conductivity and dry self-lubrication, while the specialized binder matrix imparts mechanical compressive strength exceeding 120 MPa. This dual-phase microstructure resists brush track grooving, withstands continuous peripheral speeds above 15 m/s, and maintains uniform current densities across the commutator surface.
For high-performance automotive EFI fuel pump motors, our precision CNC diamond turning operations maintain a dynamic Total Indicated Runout (T.I.R.) within ≤ 0.003 mm (3 microns), and bar-to-bar step height differences under 0.0015 mm. These tight dimensional bounds eliminate carbon brush vibration, suppress high-frequency mechanical noise, and prevent dielectric flashover at operating speeds up to 12,000 RPM.
Yes. Our in-house engineering and metrology laboratory specializes in reverse engineering and DFM (Design for Manufacturability) optimization. By providing an OE reference number, a 2D/3D CAD model, or a physical sample, our team evaluates slot geometry, wire gauge, stack height, commutator segment count, and copper base bonding. We can manufacture drop-in OEM replacements or upgraded aftermarket components within 3 to 4 weeks for prototype tooling.
Our production facilities operate strictly under the IATF 16949 automotive quality management system. Testing procedures include 100% automated inter-bar dielectric strength testing (500V AC), weld contact resistance measurement, high-temperature continuous fuel immersion tests, dynamic multi-plane rotor balancing, and salt-spray environmental chamber validation for marine-grade components.
The oxygen sensor acts as the primary feedback loop to the engine control unit (ECU). When an engine operates on fluctuating ethanol concentrations (which require varying stoichiometric ratios: 14.7:1 for pure gasoline vs. 9.8:1 for E85), the oxygen sensor detects residual exhaust oxygen and commands the ECU to modulate fuel injector pulse widths and fuel pump rotor duty cycles, preventing lean knock and thermal overload.
Direct supply line components for automotive parts importers, pump remanufacturers, and global distributor networks.
Ultra-low noise, high electrical efficiency carbon commutators designed for ethanol & methanol flex-fuel injection systems.
View Part Specifications
Direct replacement high-pressure internal pump cores engineered for passenger vehicles, delivery vans, and off-road engines.
Browse Fuel Pumps
Fast-light-off heated ceramic zirconia sensors providing rapid ECU closed-loop operation for strict emission standards.
Browse Sensor Models
Industry-standard carbon commutator segments preferred by worldwide rebuilders for heavy duty and high-ethanol environments.
View Best Sellers
Dynamically balanced armature rotor fitted with precision shaft, copper windings, and anti-corrosive carbon commutator disc.
View Catalog Listing
Specialized resin compositions engineered specifically to overcome severe chemical attack from corrosive M15-M85 methanol fuels.
Explore Commutator Tech
Benchmarked directly against leading Japanese and German OEM designs, providing equivalent life at factory direct wholesale terms.
View Product Series
Custom shaft splines, armature laminations, and tailored commutator profiles fabricated for proprietary electric fuel pump lines.
Request Drawing Review
Building 5, Lianjiang Industrial Park, Pantai Street, Ruian, Wenzhou, Zhejiang, China | Tel: +86-577-66811811