Engineered with proprietary carbon-graphite formulas, high-precision dynamic balancing, and ethanol resistance to prevent electrochemical cavitation in advanced EFI injection assemblies.

High transmission accuracy, wear-resistant carbon-graphite disc segments formulated specifically for submerged electric fuel pump motors.
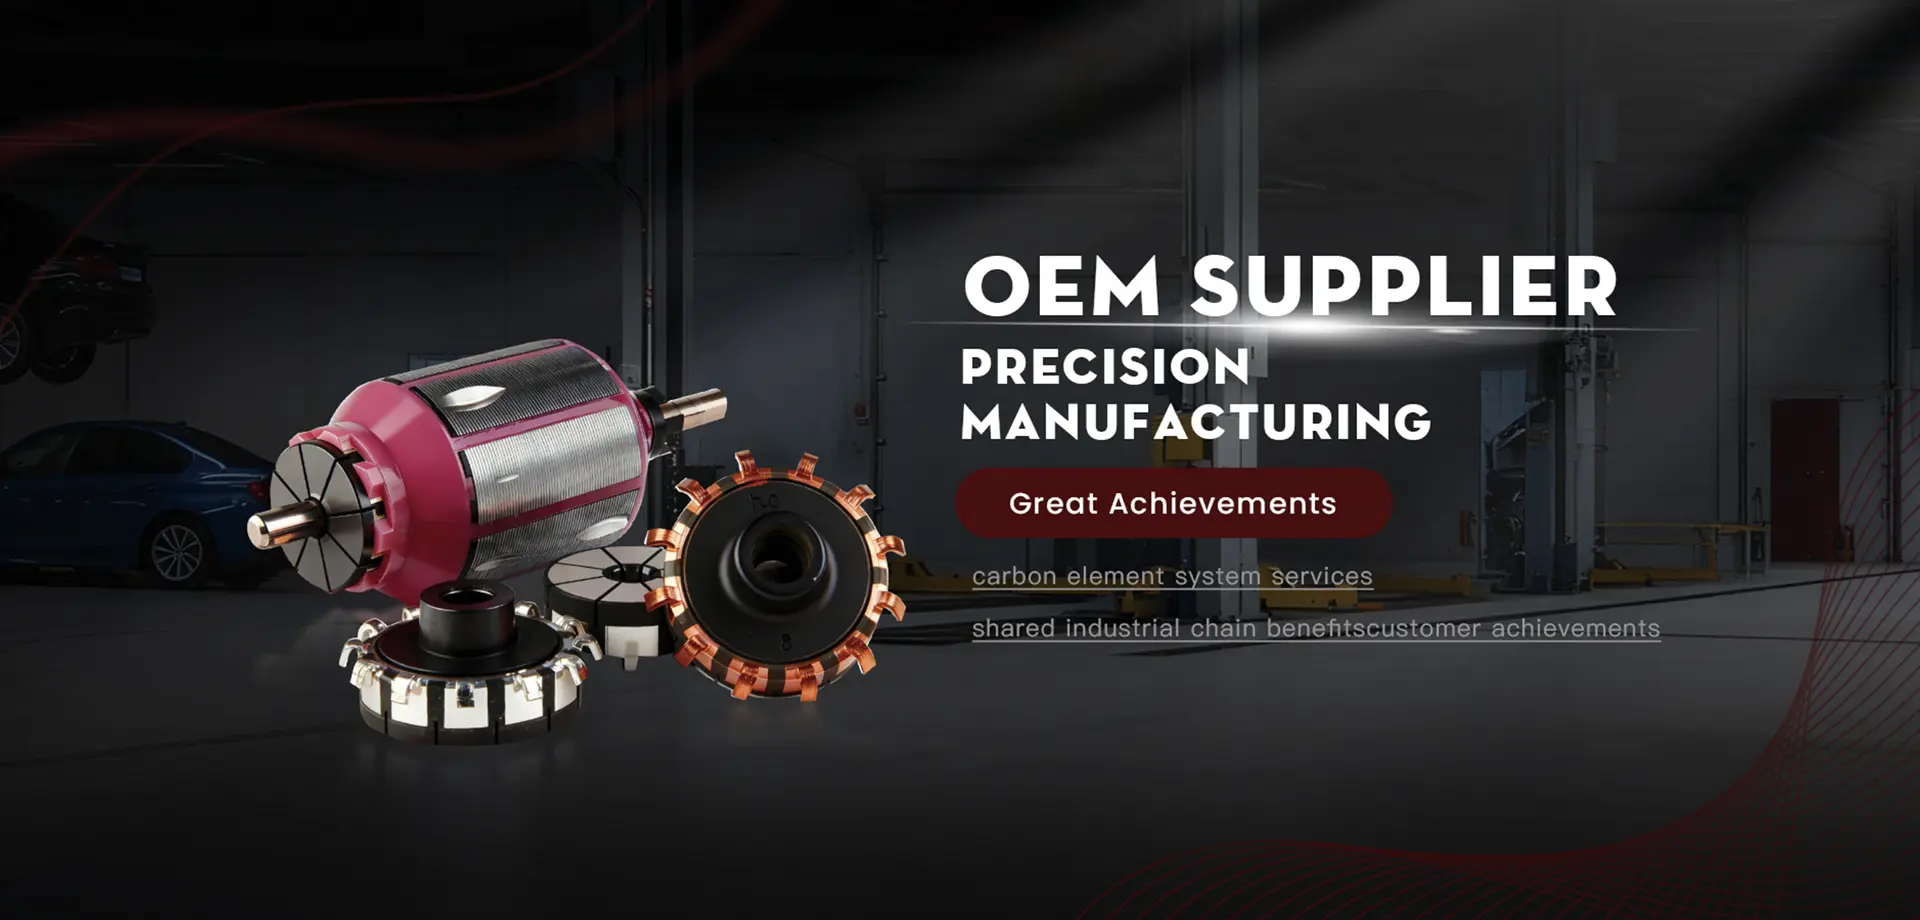
Submerged DC motor armatures with integrated graphite commutators, optimized dynamically for continuous operation in aggressive E85/M15 fuels.

High-pressure fuel injection pump core assembly featuring zero-spark commutation and low vibration for passenger cars and motorcycles.

Precision lambda sensor delivering real-time exhaust oxygen feedback to ECU closed-loop controls, ensuring stoichiometric combustion balance.

Industry-standard carbon disc commutator, heavily deployed by tier-1 pump rebuilders requiring strict segment isolation and prolonged brush life.
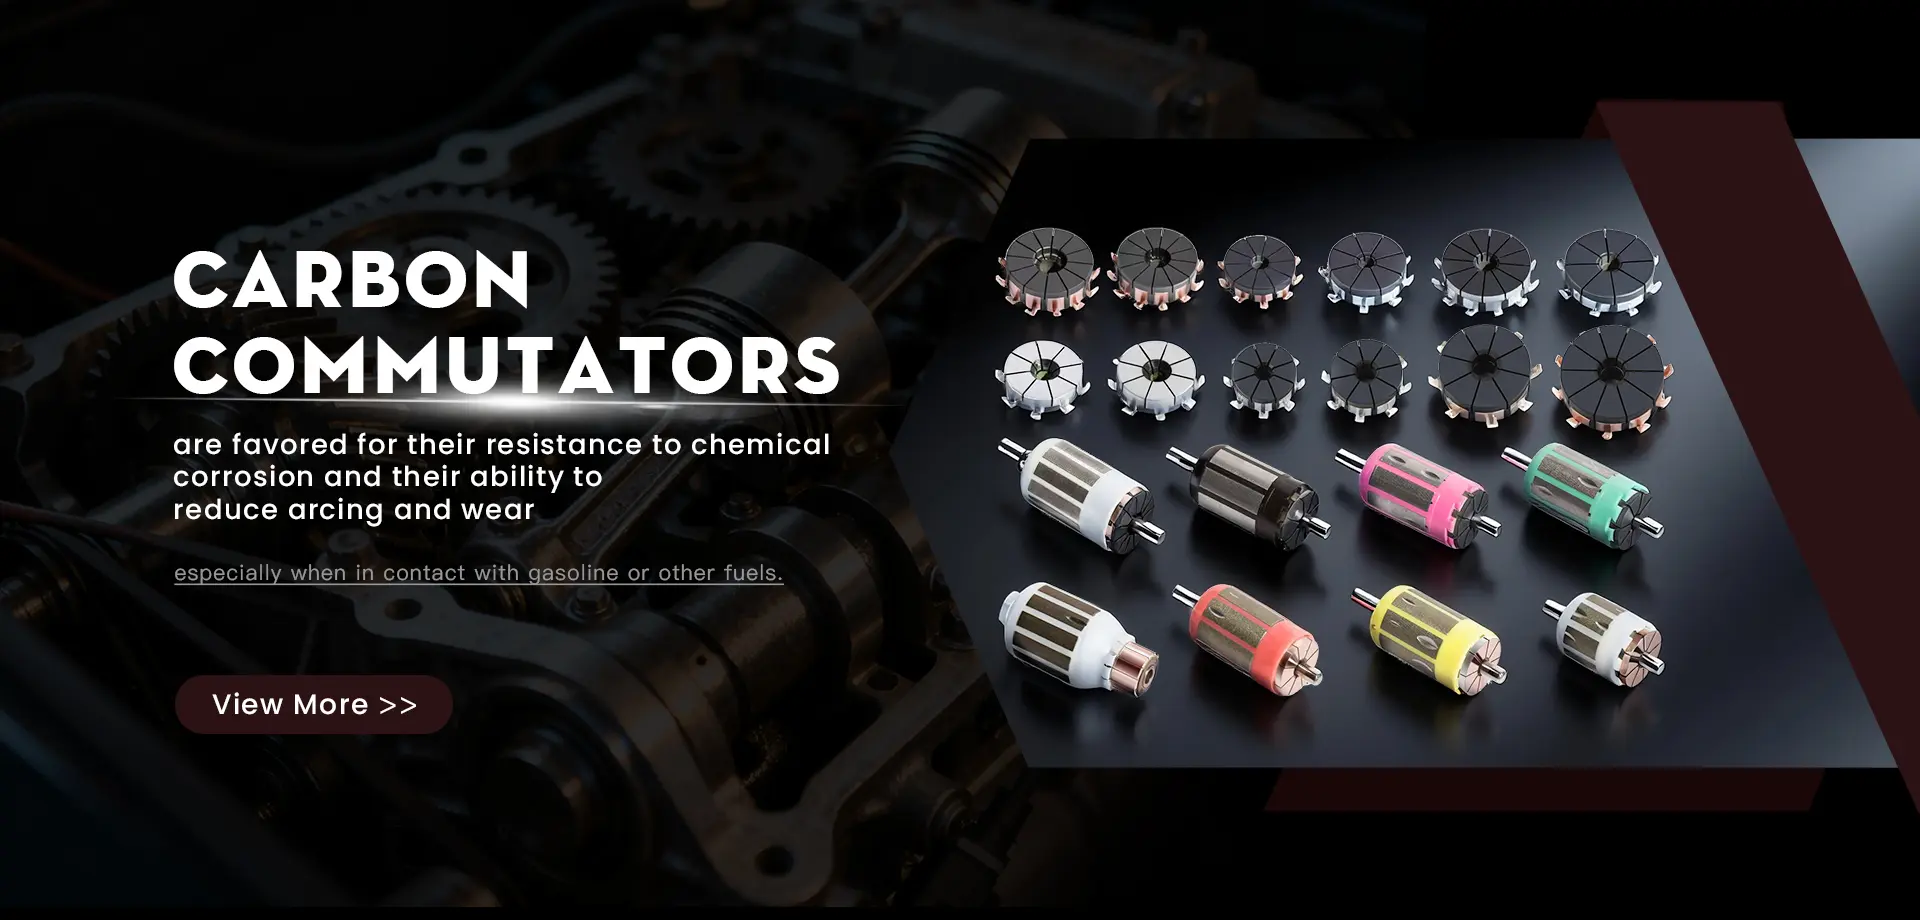
Proprietary phenolic binder combined with ultra-pure isostatic graphite preventing dielectric degradation in flex-fuel E100 engines.
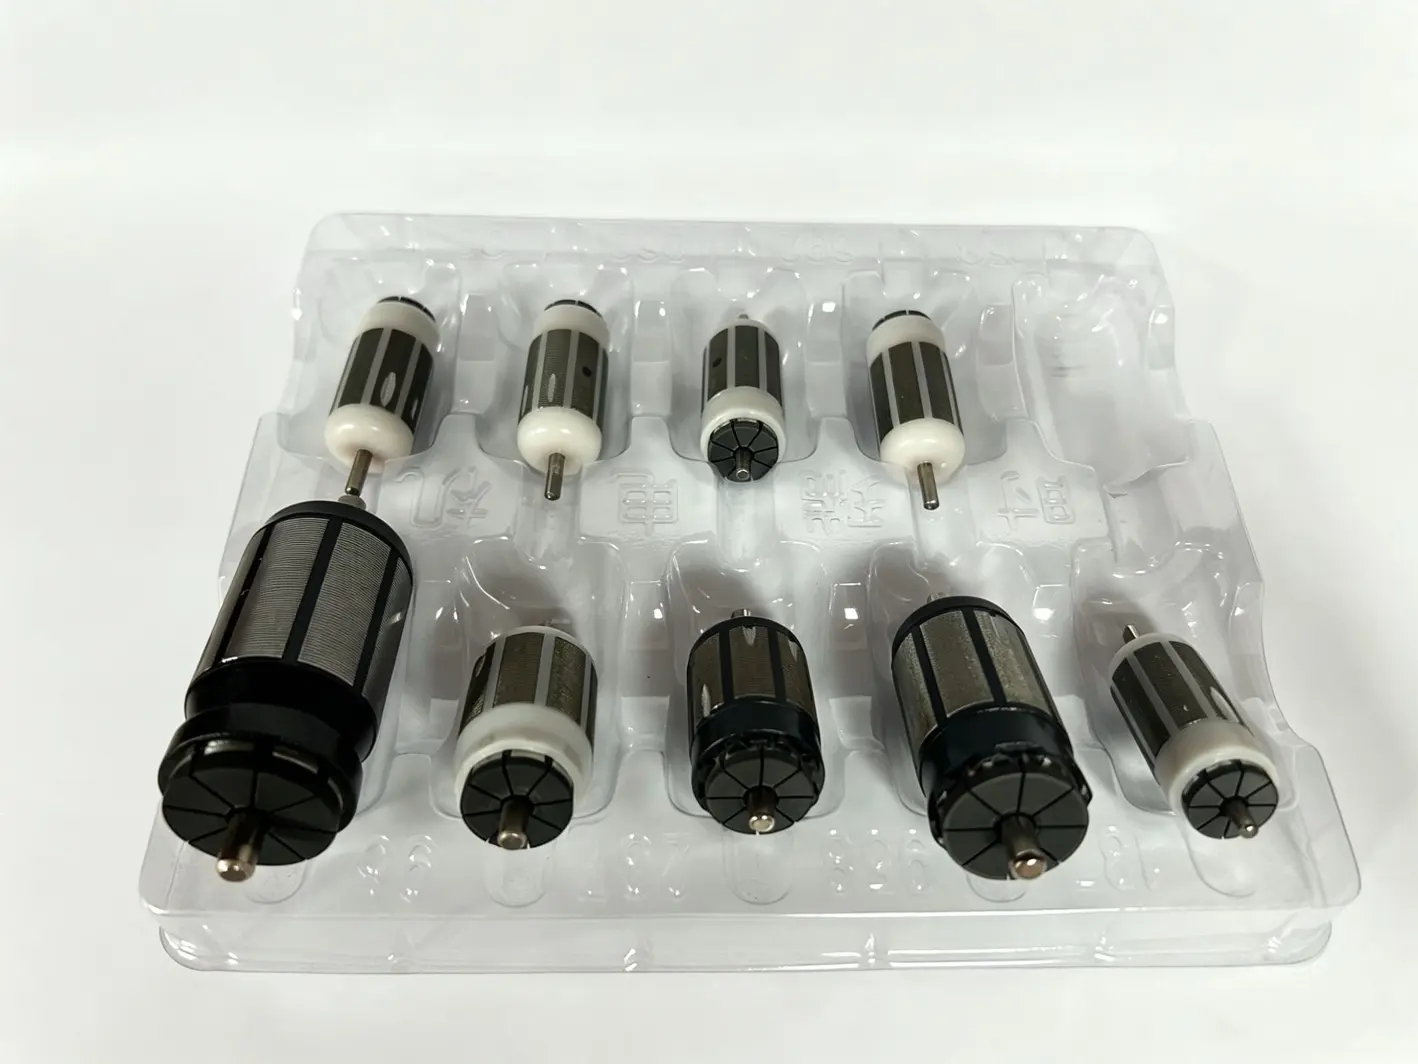
Silicon steel laminated cores assembled with high-temperature epoxy bonding, delivering minimal hysteresis losses and stable magnetic flux.
Reinforced rotor cores engineered for construction excavators and mining equipment enduring heavy cyclic thermal load and shock vibrations.
In modern electronic fuel injection (EFI) architectures, the fuel pump armature operates continuously submerged inside the fuel tank. This submerged immersion setup utilizes volatile hydrocarbons for convective armature cooling and lubrication. However, as global regulatory mandates mandate increased concentrations of oxygenated renewable additives—such as anhydrous ethanol (E10 up to E85) and fuel-grade methanol (M15 to M85)—traditional copper commutators experience accelerated electro-chemical corrosion, rapid commutator bar undercutting, and premature dielectric breakdown.
Ethanol-blended fuels exhibit high hygroscopic traits, absorbing ambient moisture that creates an ionic conductive path between adjacent copper bars. In conventional armatures, electric arcing generates copper hydroxide and copper salt deposits, leading to catastrophic short-circuits. Synthetic graphite and carbon composites possess superior chemical inertness, creating an impenetrable barrier against alcohol oxidation and formic acid corrosion.
Graphite crystals are arranged in hexagonal planar lattices with weak Van der Waals interlayer bonding. As the carbon brushes ride against the graphite armature face, microscopic carbon transfer films are deposited. This continuous self-healing solid-film lubrication drastically reduces the mechanical coefficient of friction (μ < 0.15), eliminating brush chatter, reducing electromagnetic radio interference (EMI), and ensuring silent motor operation.
Under repeated cold-cranking and high-rpm wide-open-throttle conditions, commutator spark transients can exceed 1,100°C locally. Unlike copper, which softens and deforms at elevated temperatures, graphite maintains mechanical dimensional integrity up to 2,500°C in non-oxidizing liquid envelopes, mitigating arc erosion and preserving segment planar flatness within ±1.5 µm.
| Performance Characteristic | Standard Copper Armatures | Hualeao Isostatic Graphite Armatures | Engineering Impact on EFI Pumps |
|---|---|---|---|
| Corrosion in E85 / M15 Biofuels | Severe Rapid salt dendrite build-up | Chemically Inert Zero oxidation | Prevents fuel tank stalls, pump seizure, and ECU injector blockage. |
| Operating Service Life (Hours) | 1,200 – 2,500 Hours Maximum | 6,000 – 10,000+ Hours Continuous | Meets 150,000+ mile OEM powertrain warranty requirements. |
| Contact Voltage Drop & Arcing | Variable, severe spark discharge | Low, uniform micro-arc quenching | Reduces brush brush-wear debris and preserves fuel filter cleanliness. |
| Acoustic Decibel Output (dBA) | 58 – 65 dBA (Noticeable whine) | < 42 dBA (Whisper-quiet) | Significantly enhances in-cabin passenger acoustic comfort (NVH). |
| Dynamic Rotor Balancing Standard | Standard G6.3 | ISO 1940-1 Class G2.5 Precision | Eliminates bearing fatigue and shaft seal deflection under high RPM. |
Located in Ruian City, Wenzhou—recognized as China's premier automotive components production cluster—Wenzhou Hualeao Automotive Parts Co., Ltd. integrates 6,200 m² of precision production workshops, advanced carbon-sintering furnaces, automated coil-winding lines, and certified quality-inspection facilities.
Hualeao's specialized EFI carbon commutator technology was acknowledged as a benchmark energy-conservation and emission-reduction breakthrough under China's 11th Five-Year Plan.
By adopting state-of-the-art Japanese isostatic pressing principles and German high-purity carbon matrices, our armatures directly match Tier-1 European and Japanese aftermarket standards at competitive factory-direct pricing.
From customized synthetic graphite compounding, die-casting of copper substrates, sub-micron machining of segment gaps, to armature automated coil winding and dynamic balancing—every phase is controlled in-house.
Whether producing replacement parts matching OEM codes (Bosch, Denso, Delphi cross-references) or developing new micro-motor armature architectures from 2D/3D CAD specifications, rapid tooling is guaranteed.
Take an inside look at our modernized Ruian manufacturing plant, showing high-speed progressive tooling, CNC armature balancing workstations, and automated continuous test stands simulating 1,000+ hours of continuous fuel immersion.
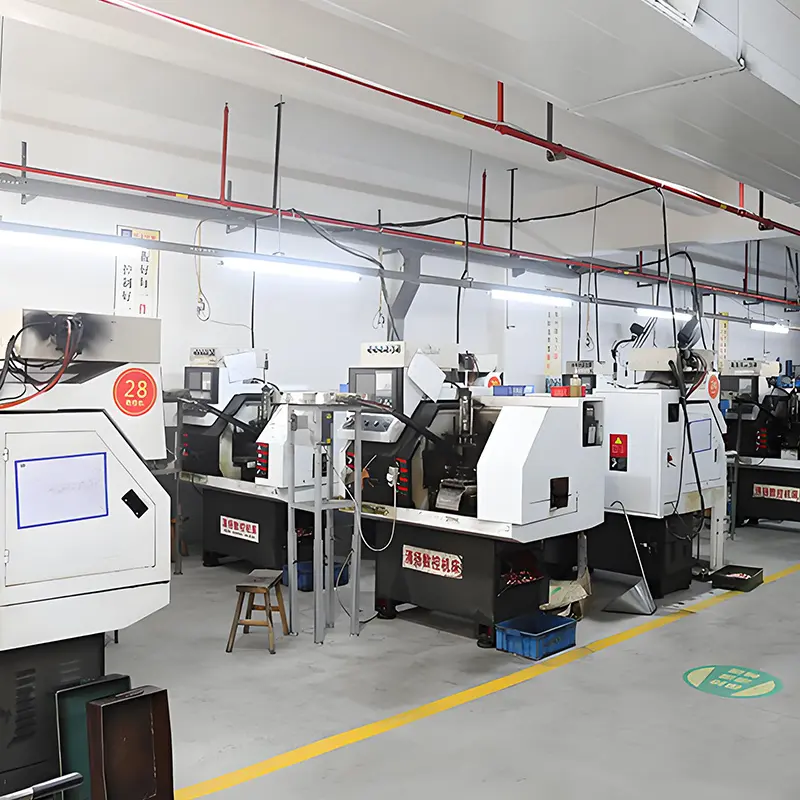
Commutator failure results in immediate fuel delivery cutoff. We implement a rigorous 4-step quality assurance cycle to guarantee absolute batch-to-batch repeatability across high-volume production runs.
Every batch of high-purity natural and synthetic graphite undergoes X-ray diffraction and ash content screening (purity ≥ 99.8%). High-conductivity electrolytic copper sheets are tested for grain boundary uniformities to maximize thermal dissipation.
Graphite powder and high-temperature thermosetting phenolic resins are pressed under multi-axial isostatic pressure, followed by computer-controlled step curing. This process eliminates internal micro-voids, guaranteeing uniform electrical resistivity (≤ 18 μΩ·m).
Mica slotting and commutator segment isolation are machined with ultra-precision CNC slotting diamond wheels. Commutator runout is kept within ≤ 0.003 mm, ensuring zero copper-drag across segment boundaries and preventing inter-segment flashover.
Armatures undergo automated dual-plane dynamic balancing, followed by 1,500V high-voltage insulation tests between shaft and windings. Fuel immersion test benches verify zero chemical swelling in hot aggressive alcohol solutions for 1,000+ hours.
From compact micro-pumps handling high RPM motorcycle accelerations to heavy industrial mining engines operating under salt spray or dusty atmospheres, our graphite commutators and fuel armatures deliver continuous reliability.
Provides OEM and replacement motor assemblies for standard multi-port injection (MPI) and high-pressure gasoline direct injection (GDI) lift pumps, with full compatibility for E10 to E85 fuels.
High RPM miniaturized armatures engineered to deliver high fuel flow under ultra-compact physical envelopes, resisting intense road vibrations and high ambient fuel tank temperatures.
Robust 12V and 24V fuel pump armatures crafted for earthmovers, heavy excavators, and agricultural diesel engines enduring prolonged high-vibration duty cycles.
Reinforced anti-corrosion motor armatures specifically treated to withstand salt-fog penetration, high humidity, and electrolytic water-in-fuel conditions encountered in marine environments.
While battery-electric vehicles expand in passenger urban sectors, the commercial automotive, hybrid (HEV/PHEV), range-extended electric vehicle (EREV), motorcycle, and flex-fuel sectors are experiencing unprecedented demand for high-efficiency, ethanol-tolerant electric fuel pumps. Global pump assemblers face severe bottlenecks from aging European and American component suppliers. Wenzhou Hualeao answers these global sourcing needs through:
By leveraging China's integrated raw material ecosystems—including nearby high-purity spherical graphite producers and precision copper rolling mills—we reduce production costs by 28% to 40% compared to Western manufacturers while matching identical micro-durability indicators.
Developing new commutator tooling or winding mandrels often takes 6–9 months with traditional vendors. Our dedicated CAD/CAM rapid tooling cell delivers fully functional PPAP Level 3 prototypes within 25–35 business days from drawing confirmation.
To shield global Tier-1 clients from international freight surges and volatile raw material pricing, Hualeao offers warehouse buffer agreements and blanket order fulfillment, guaranteeing on-time maritime and air shipping from Ningbo or Shanghai ports.
Detailed technical, commercial, and manufacturing answers designed to resolve purchasing ambiguities for automotive fuel system engineers and global aftermarket procurement teams.
The carbon commutator acts as an alternating mechanical rotary switch located at the shaft terminal of the fuel pump's DC micro-motor. As the armature core rotates between permanent magnets, the carbon commutator segments slide against opposing carbon brushes, periodically reversing current direction through the copper armature coils. This maintains steady unidirectional electromagnetic torque, powering the regenerative turbine or gerotor impeller to supply continuous, high-pressure fuel to the engine's fuel rail.
Traditional electric fuel pumps relied on copper bar commutators. However, modern commercial fuels are enriched with ethanol (such as E10, E20, or flex-fuel E85) and methanol (M15, M85). Because electric fuel pumps are submerged inside the tank, alcohol fuels conduct micro-currents that dissolve copper into metal oxides, leading to rapid pitting, catastrophic segment flaking, and spark discharge. Graphite commutators are chemically inert, providing zero electrochemical reaction, superior thermal tolerance, and lower brush wear friction (μ < 0.15).
Yes. Wenzhou Hualeao operates a dedicated custom engineering department. Buyers can supply 2D engineering drawings (PDF / DWG), 3D CAD models (STEP / IGES), or worn physical OE reference samples. Our engineering team evaluates dimensions, segment quantities, mica depth, copper substrate specifications, and electrical parameters, offering tailored DFM (Design for Manufacturability) suggestions and sample tooling within 25–35 days.
Our production facilities operate strictly under certified quality management systems aligned with ISO/TS automotive component standards. Our EFI carbon commutator was officially listed as a new-vehicle energy conservation and emission reduction project under China's 11th Five-Year Plan. Every armature batch is subjected to ISO 1940-1 Class G2.5 dual-plane dynamic balance inspection, 1,500V dielectric breakdown testing, and automated optical dimensional measurement (CMM).
Our components are broadly integrated across four primary segments: (1) Automotive passenger and light commercial vehicle EFI fuel delivery systems; (2) High-speed motorcycle and scooter fuel injection systems; (3) Heavy-duty engineering machinery, agricultural tractors, and construction vehicles; (4) Marine inboard/outboard engines requiring salt-spray corrosion protection.
We maintain strict vertical control over critical manufacturing steps. We do not source pre-mixed carbon composites from unstable open markets; rather, we utilize vetted raw-material suppliers who provide constant-density isostatic graphite matrices. Our automated sintering ovens, continuous slotting laser sensors, and robotic coil winders continuously monitor line tolerances, ensuring dimensional variations remain within ±0.005 mm across batches of 100,000+ units.
Global procurement teams can initiate an RFQ by visiting our Request a Catalog portal, or by emailing our engineering sales desk at [email protected]. Please provide target OE cross-reference numbers (e.g., Bosch, Denso, Delphi), required monthly/annual volumes, and target fuel environment (Standard Gasoline, E85, or Methanol) for an expedited response within 24 hours.
Review our specialized commutator architectures, precision lambda sensors, and electric fuel pump assemblies built for global automotive, marine, and industrial duty cycles.
Designed for submerged high-volume automotive fuel pumps, providing uniform contact surfaces and low commutator undercut wear.

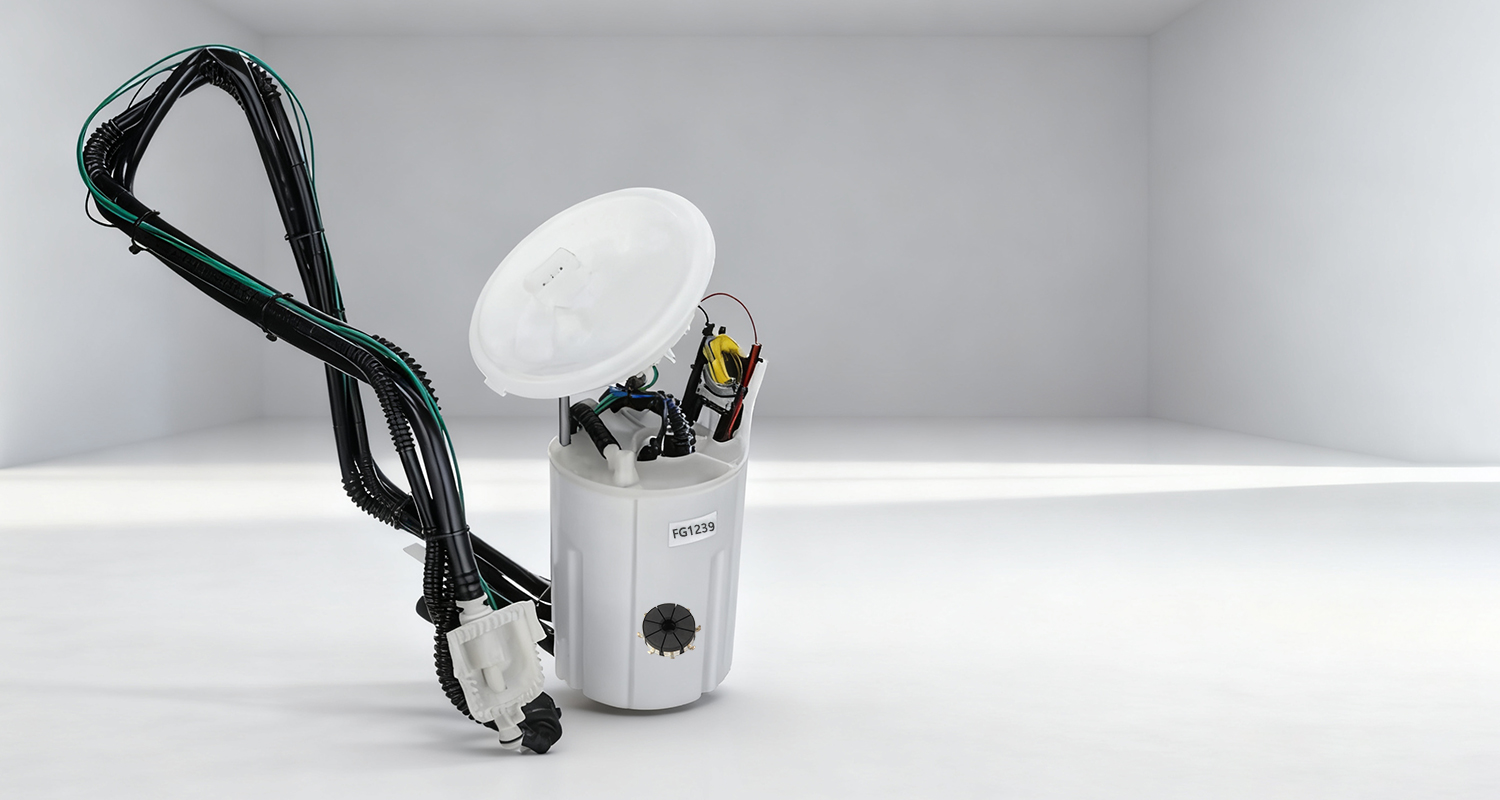
Complete drop-in electric fuel pump assembly fitted with graphite motor cores, offering steady fuel delivery for 1.0L to 4.0L gasoline engines.
High-sensitivity planar exhaust oxygen sensor supporting Euro V and Euro VI emission feedback standards with integrated ceramic heaters.
Engineered for high-amperage starting conditions, featuring reinforced copper hook tangs for reliable armature coil fusing.
Engineered according to custom OEM winding patterns and shaft lengths for special agricultural sprayers and industrial DC pumps.
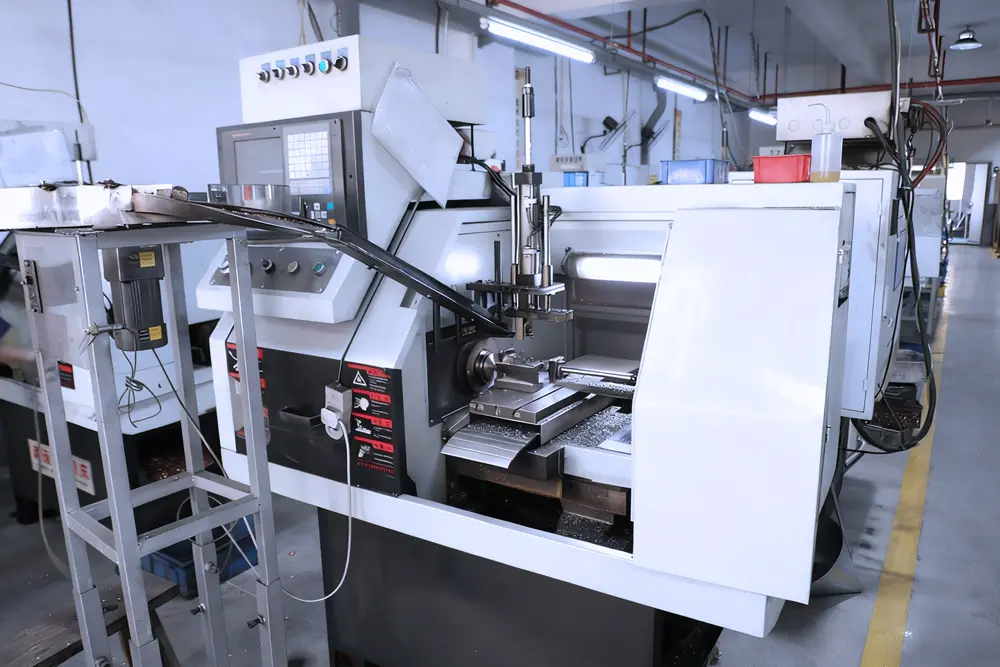
Dynamically balanced at 18,000 RPM to prevent centrifugal carbon separation in high-performance racing motorcycle pump modules.
Treated with proprietary protective surface passivations, guarding against galvanic corrosion in coastal saltwater and high-moisture air.
Available in 6, 8, 10, or 12 segment layouts to match existing DC motor brush cards and winding designs with zero retrofitting.
Send your 2D/3D technical drawings, sample parts, or OEM interchange references to our engineering desk. Our team will verify materials, run simulations, and supply certified samples for bench testing.