Exacting dimensional tolerance, superior tribological stability in aggressive alcohol biofuels, and dynamically balanced rotation up to 18,000 RPM. Browse our benchmarked flagship offerings.

Planar disc and radial graphite commutators engineered specifically for immersed fuel pump DC armatures operating in high-corrosion flex-fuel blends.

Complete electric fuel pump assembly with dynamically balanced armature core, integrated check valves, and ultra-quiet carbon commutation.

Zirconia solid-electrolyte planar lambda sensors delivering sub-second ECU feedback for closed-loop air-fuel ratio management and emissions control.

Standard OE-replacement disc-type carbon segment commutator with reinforced phenolic backing for high thermal-shock endurance and spark suppression.
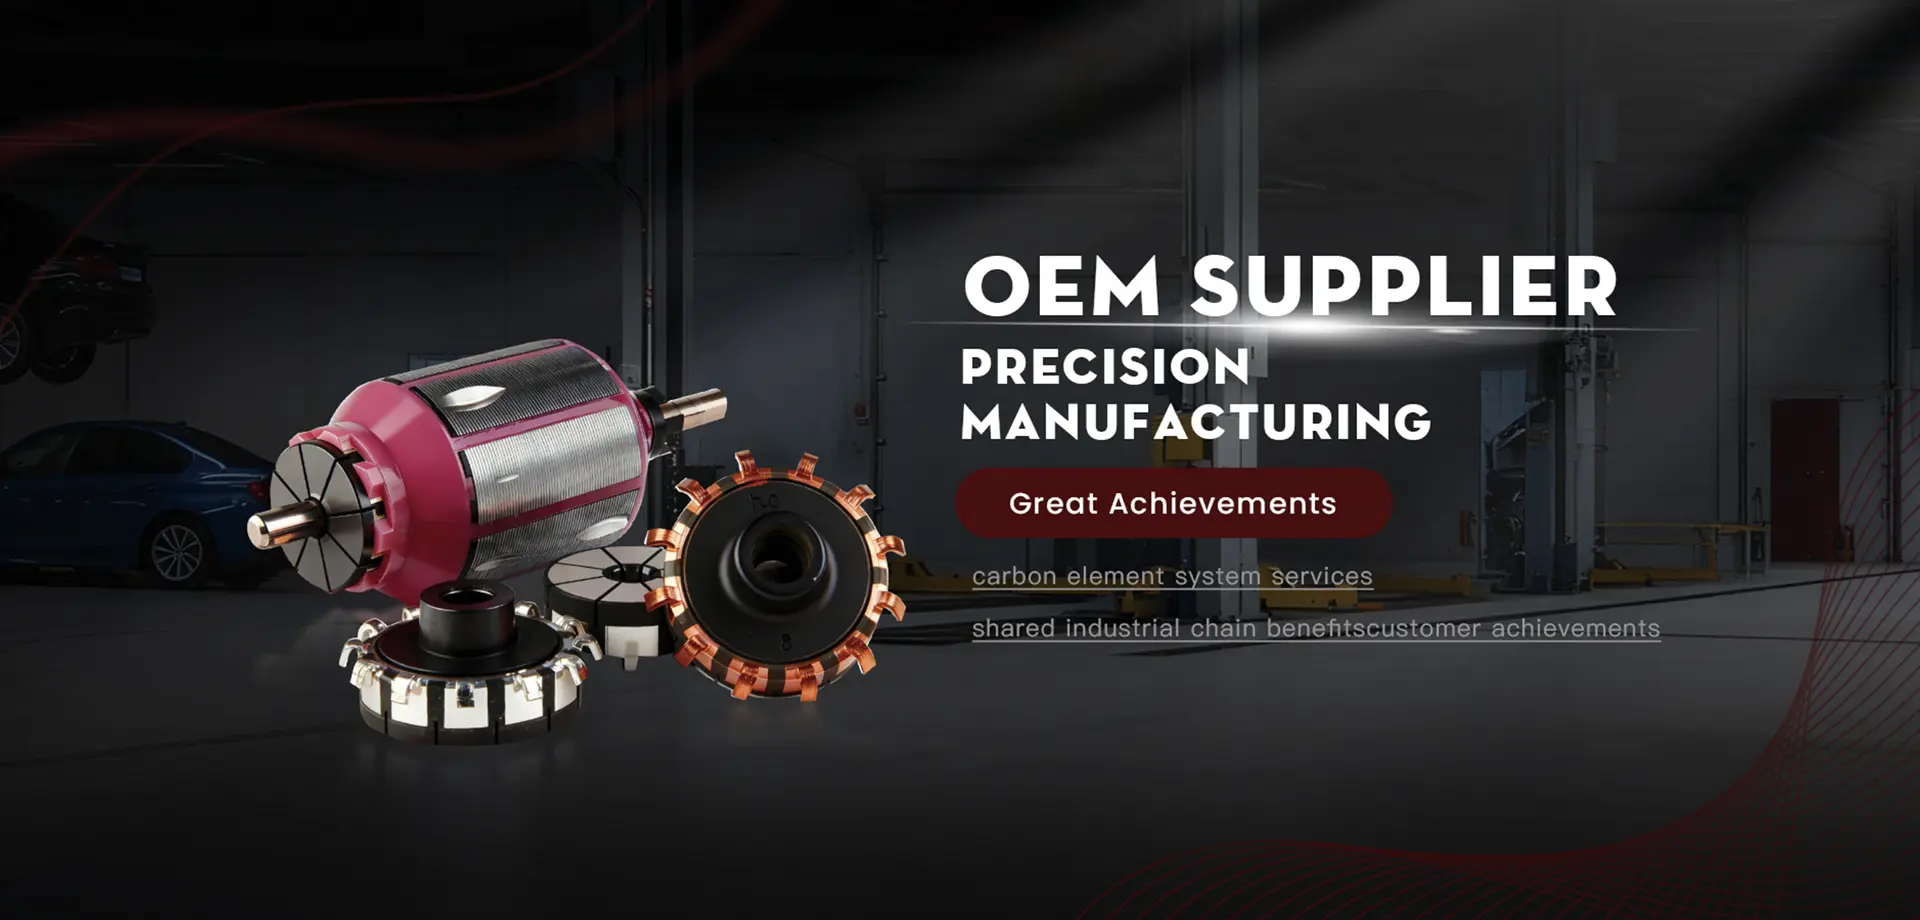
Full armature assembly integrating precision-stamped silicon steel laminations, high-conductivity enamelled copper windings, and micro-balanced shafts.
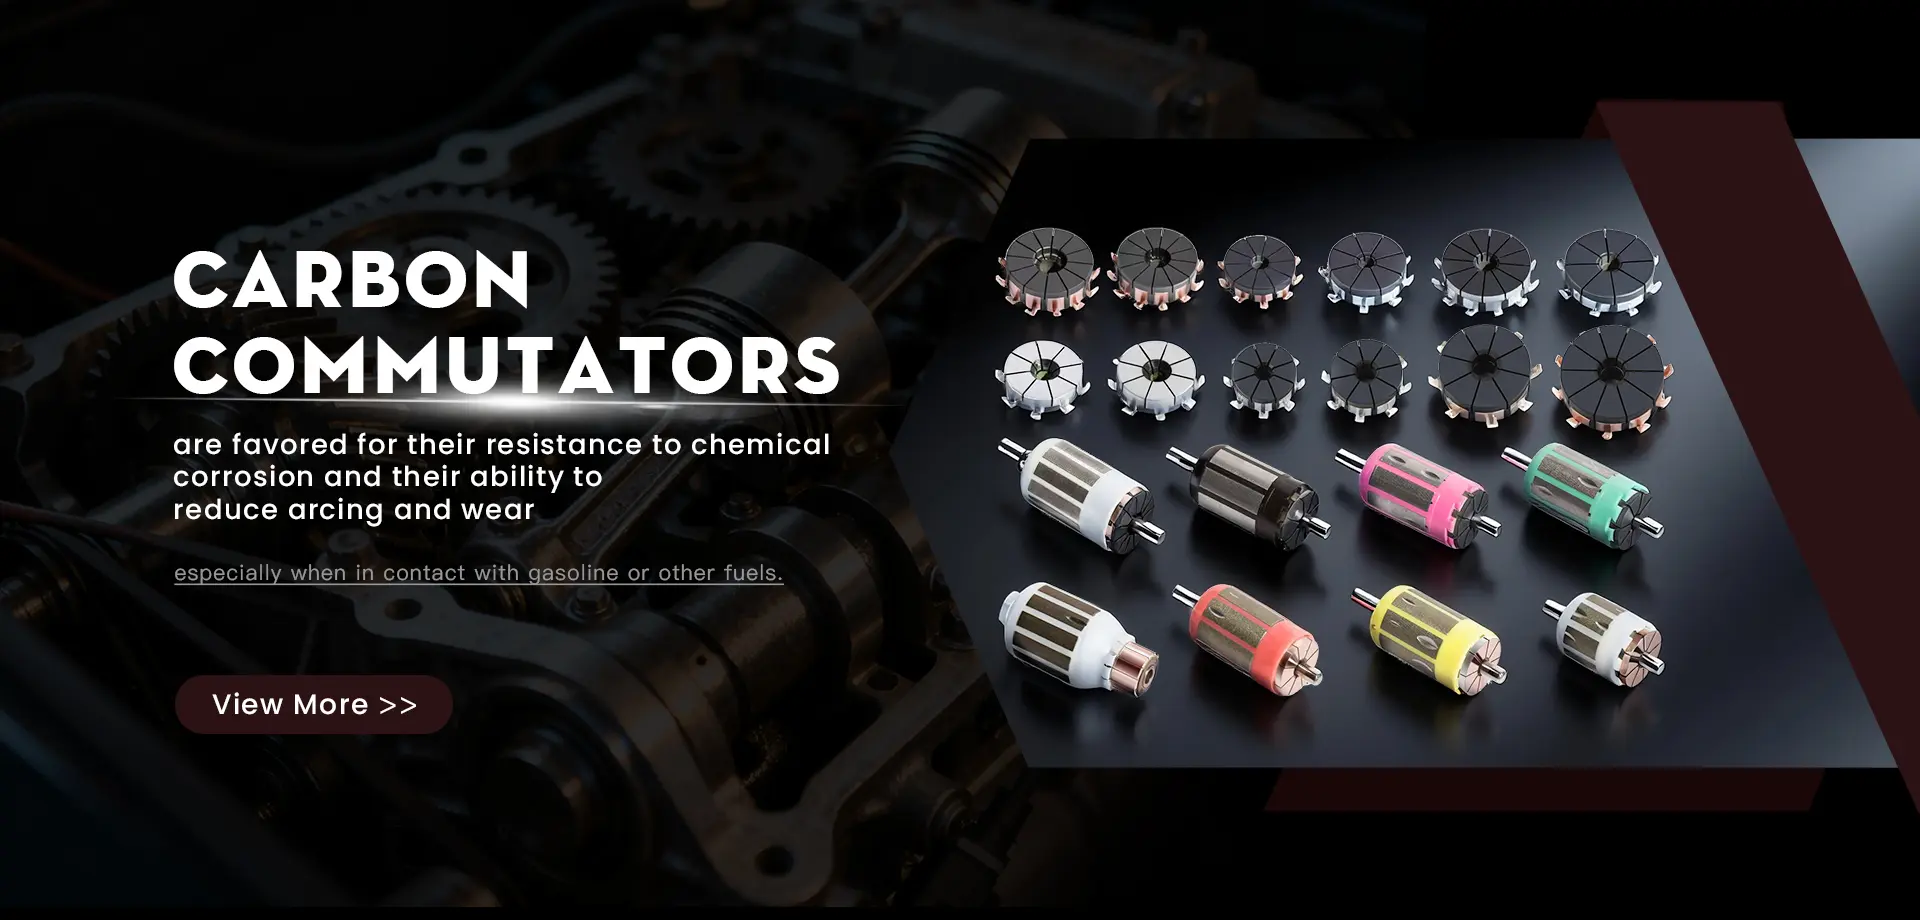
Custom multi-segment commutators treated with chemical anti-swelling binders to eliminate segment delamination in corrosive oxygenated fuels.
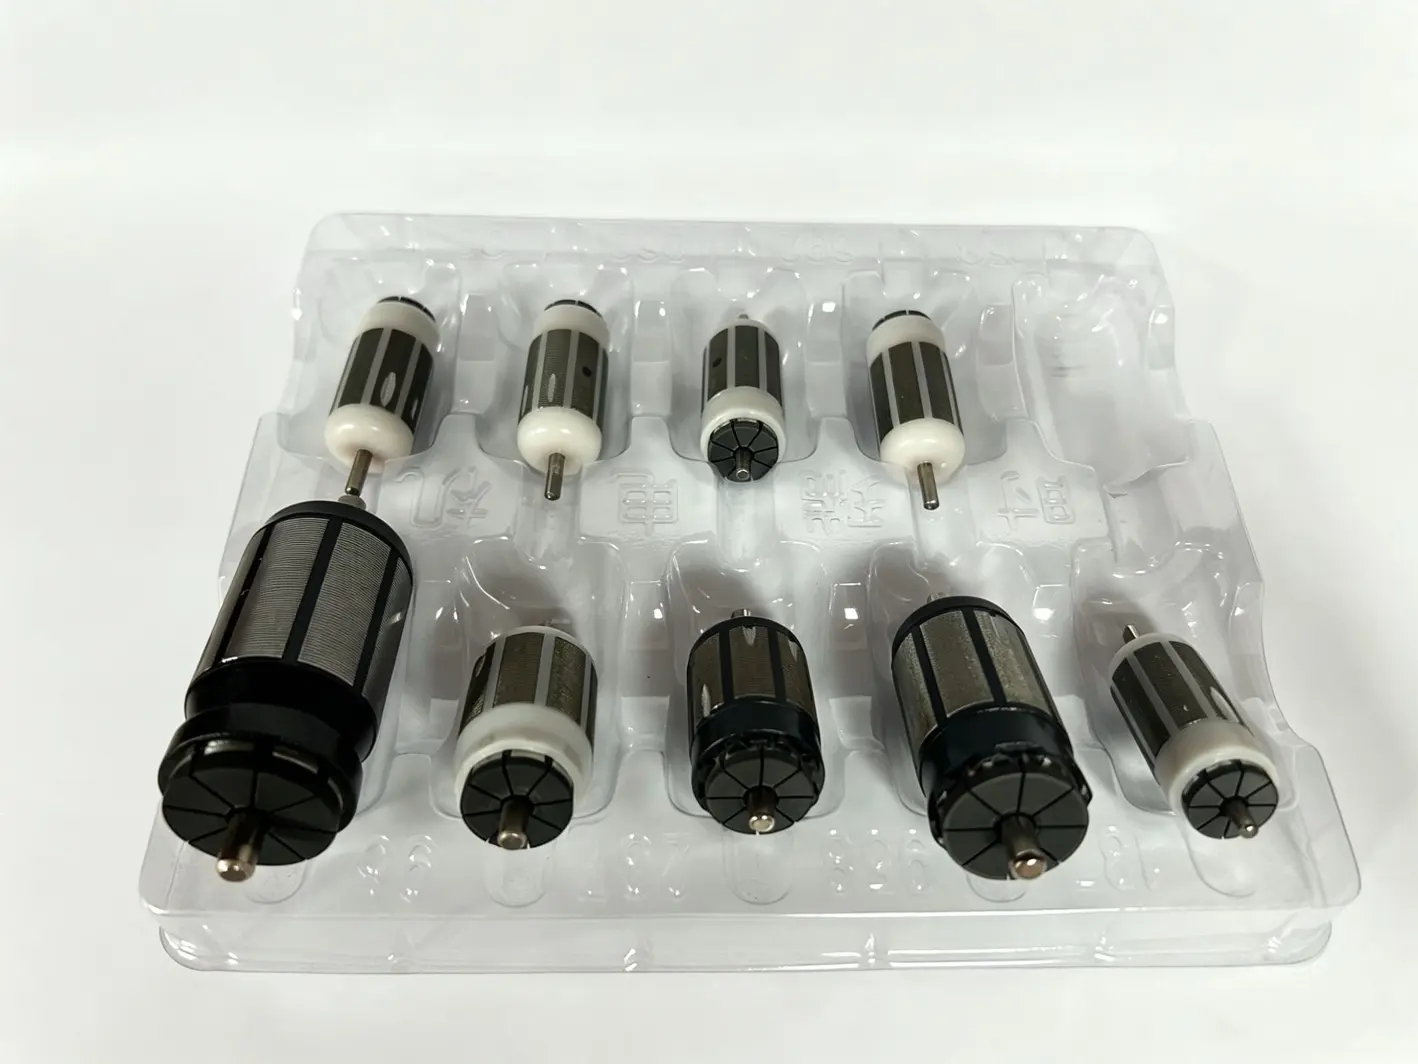
Ultra-compact radial copper-to-carbon commutators for automotive auxiliary actuators, window lifters, throttle bodies, and motorcycle starters.
Heavy-duty armature core lamination stacks and heavy-gauge commutators designed for construction hydraulic pumps and harsh marine outboard systems.
Understanding the micro-mechanics of current commutation, electrochemical dissolution in alcohol fuels, and metallurgical precision required for zero-defect automotive motor armatures.
In standard automotive DC motor environments, metallic copper commutators paired with electrographite brushes provide adequate current density and thermal dissipation. However, the immersion of electric fuel pumps directly inside the fuel tank—a standard architecture in modern Electronic Fuel Injection (EFI) and Gasoline Direct Injection (GDI) low-pressure feed systems—creates an aggressive tribological and electrochemical environment. With global fuel standards mandating increasing blends of bio-ethanol (e.g., E10, E20, up to pure hydrated hydrous E100 in Brazil) and methanol (M15 to M85), standard copper segments suffer from catastrophic accelerated degradation.
When current arcs across rotating copper segments immersed in polar alcohol molecules, electrolytic micro-corrosion quickly strips the copper ions. This ionic migration causes copper segment pitting, leading to severe commutator surface roughness, increased brush chatter, high contact drop, and eventual short-circuiting between adjacent segments due to conductive copper slurry accumulation.
Wenzhou Hualeao Automotive Parts Co., Ltd. circumvents this physical limitation through proprietary planar carbon-graphite disc matrix technology. By bonding an isostatically pressed, resin-impregnated graphite contact disc to a high-conductivity copper terminal substrate, the arcing contact interface is entirely shielded by chemically inert graphite. Carbon exhibits near-zero chemical reactivity with ethanol, methanol, organic acids, and corrosive sulfur compounds, extending fuel pump operational lifespans beyond 3,500 continuous running hours (equivalent to >250,000 vehicle kilometers).

High-dielectric thermosetting phenolic resins (Bakelite) engineered for zero expansion under persistent alcohol fuel submergence, maintaining inter-segment isolation > 100 MΩ even at 140°C thermal peaks.
Rotor shafts and core windings are processed via automated multi-plane dynamic balancing machines, eradicating radial runout down to ≤ 0.003 mm and mitigating high-frequency acoustic resonance inside passenger cabins.
High-precision diamond saw undercutting ensures segment gap edges have zero burrs and precise 0.25mm to 0.45mm depth profiles, preventing carbon particulate buildup and flashover arc bridging.
Navigating regional biofuel mandates, electrified hybrid powertrain demands, and the critical role of precision armatures in sustaining internal combustion efficiency.
With Brazil’s RenovaBio policy mandating widespread hydrous ethanol (E100) and flex-fuel fleets commanding >80% market share, carbon commutators are non-negotiable OE requirements to counter intense water-induced electrochemical corrosion.
Expanding E15 adoption and EPA Tier 3 ultra-low emission standards require fuel pump armatures to operate without vapor lock across severe seasonal temperature gradients (-40°C to +60°C ambient).
Plug-in hybrid electric vehicles (PHEVs) leave fuel dormant in tanks for extended periods, causing fuel stagnation and acidic peroxide formation. Hualeao’s acid-resistant carbon commutators safeguard fuel delivery reliability during sudden ICE engagements.
India's accelerated national transition to E20 fuel by 2025 has triggered an urgent overhaul of two-wheeler and commercial vehicle fuel systems, creating immense OEM and replacement demand for high-durability armature assemblies.
From high-frequency vibration powersports to harsh maritime brine and continuous heavy-duty industrial cycles, our motor armatures perform without compromise.
Low-pressure in-tank fuel feed modules for multi-point port injection and direct-injection engines. Delivers uniform fuel volumetric delivery without electrical pulse ripple, preventing fuel pressure fluctuations that trigger misfires.
High-revving two-wheelers encounter extreme vibration harmonics (up to 12G). Our compact armatures employ locked winding tangs and reinforced disc commutators to eliminate wire fracturing and segment detachment under high RPMs.
Construction excavators, generators, and agricultural harvesters operating in extreme dust and continuous 100% duty cycles. Our armature assemblies resist high-sulfur diesel, bio-diesel blends, and severe thermal load cycles.
Maritime vessels experience saline atmosphere penetration inside vented fuel cells. Specially passivated copper tangs and graphite segments pass 96-hour neutral salt-spray (ASTM B117) testing without galvanic oxidation.
Pioneering next-generation tribological formulations, nano-composite brushes, and hybrid brushless sensor architectures to meet future global vehicle requirements.
High-precision cold press sintered carbon disc hot-bonded with copper current collectors using proprietary conductive adhesive interlayers. Yields total shear adhesion strength > 28 MPa, resisting thermal shock cycles from -40°C to +150°C.
Integrating multi-walled carbon nanotubes into the graphite substrate to boost electrical conductivity by 35% while slashing friction coefficients to < 0.12, dramatically lowering brush mechanical wear and heat dissipation.
Expanding beyond brushed armatures toward integrated brushless DC (BLDC) pump rotors. Developing high-coercivity bonded neodymium magnet rings and precision balancing sleeves for zero-contact high-efficiency wet-running motors.
Modern Production Facility in Ruian, Wenzhou
Specialized Engineers & Technical Staff
Automotive Qualification Certifications
Global OEM & Aftermarket Supply Partners
Anchored in Ruian, China’s capital of auto parts, Hualeao merges vertical industrial clustering with deep raw material integration to deliver unmatched value and lead times.
From raw graphite isostatic pressing, copper stamping, and high-temperature Bakelite injection molding to diamond-tool finishing and dynamic rotor balancing—100% of critical manufacturing processes are housed internally, eliminating subcontractor markups and delay risks.
Leveraging Wenzhou's mature precision tooling ecosystem, we transition from customer CAD step files or reverse-engineered OE physical samples to first-article dimensional prototypes in as little as 10 to 14 working days.
Producing millions of commutator units annually provides exceptional purchasing power for premium copper coils, electrical steel, and specialized graphite. We deliver import-grade German and Japanese benchmarked performance at a 30% to 45% competitive cost edge.
Our commitment to the E-E-A-T benchmark is demonstrated through 100% automated optical inspection (AOI) on commutator segment pitch and diametrical runout. Every production batch undergoes dielectric strength testing at 1,500V AC, inter-bar resistance validation, and endurance soaking in 60°C heated M15 aggressive methanol fuel solutions.
Guarantees zero micro-short circuits between commutating segments before armature winding insertion.
Commutators are sample-spun up to 35,000 RPM at 120°C to verify mechanical hook and segment locking integrity.
Meeting international environmental mandates and providing turnkey drawing-to-part engineering for multinational distributors and automotive pump rebuilders.
All phenolic resins, copper alloys, and graphite formulations are strictly certified lead-free, cadmium-free, and compliant with EU RoHS 2011/65/EU and REACH (SVHC) regulations for environmental health.
Whether you provide detailed 3D step files, 2D GD&T mechanical prints, OE part cross-references (Bosch, Denso, Delphi, Walbro), or physical worn pump samples, our metallurgical lab conducts coordinate measuring machine (CMM) mapping for direct OE drop-in fitment.
Serving over 3,000 clients across North America, Europe, South America, and Southeast Asia. We support scheduled releases, flexible container consolidation, and customized VMI (Vendor Managed Inventory) buffering to guard against supply chain disruption.
Direct factory supply from Wenzhou, China. Access technical CAD models, OE cross-reference data, and material certifications across our entire core line.
Ultra-flat disc commutator providing zero axial chatter, low electrical noise, and high spark quenching inside compact automotive pump housings.
Ultra-quiet single-stage turbine impeller pump driven by balanced carbon-commutated armature. Minimizes fuel pulsations and electrical draw.
OE-matching wiring harness, anti-seize coated stainless housing, and laser-welded dual-protection tube for extreme thermal exhaust shock.
Proven carbon commutator module tailored for aftermarket replacement in high-volume Japanese and European passenger car platforms.
Laminated electrical steel cores with precision epoxy insulation coating on slot edges to safeguard against magnet wire breakdown during winding.
Special resin-impregnated graphite composition providing maximum chemical immunity against methanol-fuel oxidation and acidic fuel decay.
Engineered for low electrical noise (EMC) compliance, minimal spark generation, and low mechanical friction in auxiliary automotive micro-motors.
Tailored commutator outer diameters, custom core stack lengths, and hook or slot-type segment terminations machined exactly to client drawings.
Crucial technical answers for automotive electrical system designers, fuel pump engineers, and international procurement executives.
Our engineering office in Ruian provides cross-reference confirmation, CAD modeling, and custom tooling analysis directly with your R&D team.
Email Engineering Team