Engineered for low parasitic losses, extreme alcohol tolerance, and verified hydraulic stability across high-pressure cycles.

Molded carbon-graphite disc commutators built for high-speed fuel pump rotors, ensuring wear resistance against volatile fuels.
Explore Specifications
Precision dynamic-balanced pump assembly delivering continuous fuel volume with ultra-low acoustic signature and high thermal limits.
Explore Specifications
Zirconia lambda sensors offering microsecond-level stoichiometric feedback to ECU systems for optimal air-fuel balancing.
Explore Specifications
Heavy-duty carbon rotor commutator benchmarked against Tier-1 European and Japanese specifications for long-life armatures.
Explore Specifications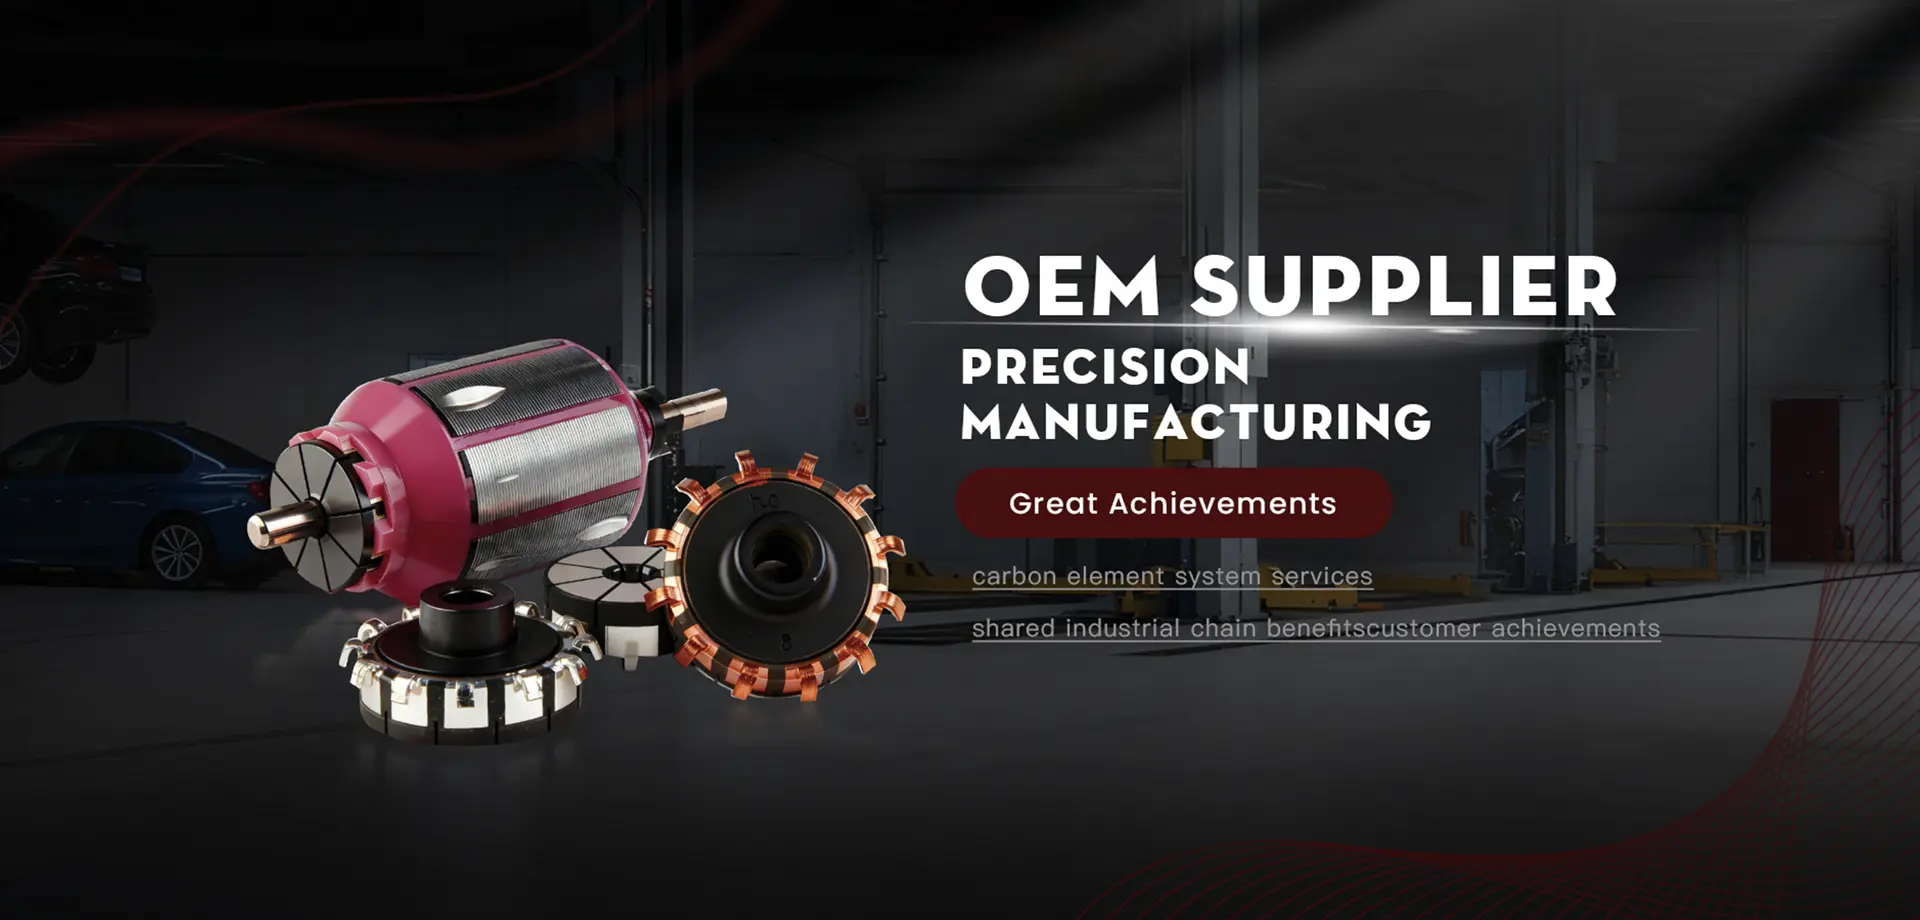
Complete rotor sub-assembly engineered with high concentricity and stacked silicon steel laminations for low eddy current losses.
Explore Specifications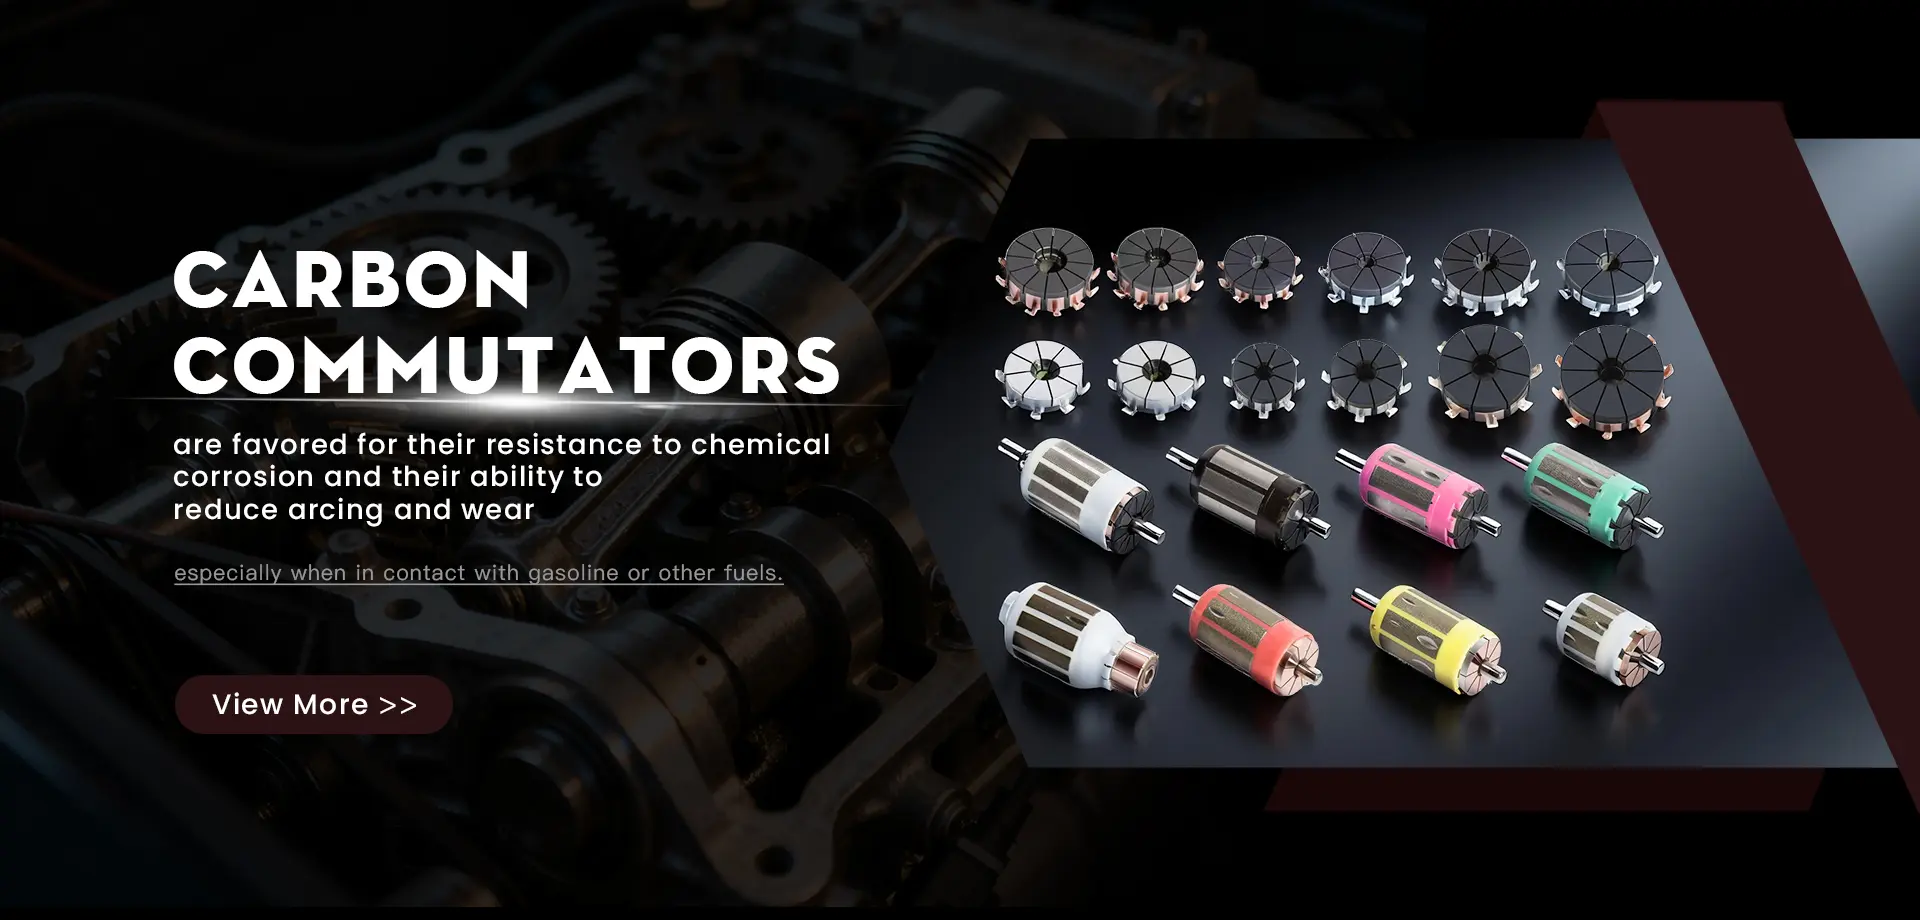
Specialized graphite polymer composite formulated specifically for M15/M85/M100 flex-fuel systems without surface pitting.
Explore Specifications
Enhanced torque transmission design intended for high-stress hydraulic, auxiliary lubrication, and heavy duty off-highway units.
Explore Specifications
Full engineering adaptation based on customer CAD/drawings or physical samples, calibrated for strict rotational tolerance standards.
Explore SpecificationsA comprehensive examination of cycloidal gerotors, submerged armature rotors, and tribological mechanics in modern internal combustion and hybrid powertrains.
Rotor oil pumps utilize trochoidal inner and outer gear sets (gerotors) to move fluid through positive displacement. As the inner drive rotor rotates, its teeth sweep past the outer rotor pockets, causing volume expansion at the intake port (creating suction) and volume reduction toward the discharge port (generating pressure). The volumetric efficiency (ηv) of a rotor oil pump is governed directly by radial and axial clearances. Conventional manufacturing often yields clearances of 0.06–0.09 mm, resulting in high internal recirculation (slip) at low engine RPM and hot oil conditions. Wenzhou Hualeao maintains precision tooling matrices holding rotor profile clearances below 0.025 mm, preventing cavitation and maintaining stable volumetric output across temperatures ranging from -40°C to 150°C.
Using alloyed sintered iron-copper-carbon powders subjected to high-tonnage multi-action compacting and protective atmosphere sintering, our rotor components achieve high surface micro-hardness (HRB 75-95) and compressive fatigue resilience.
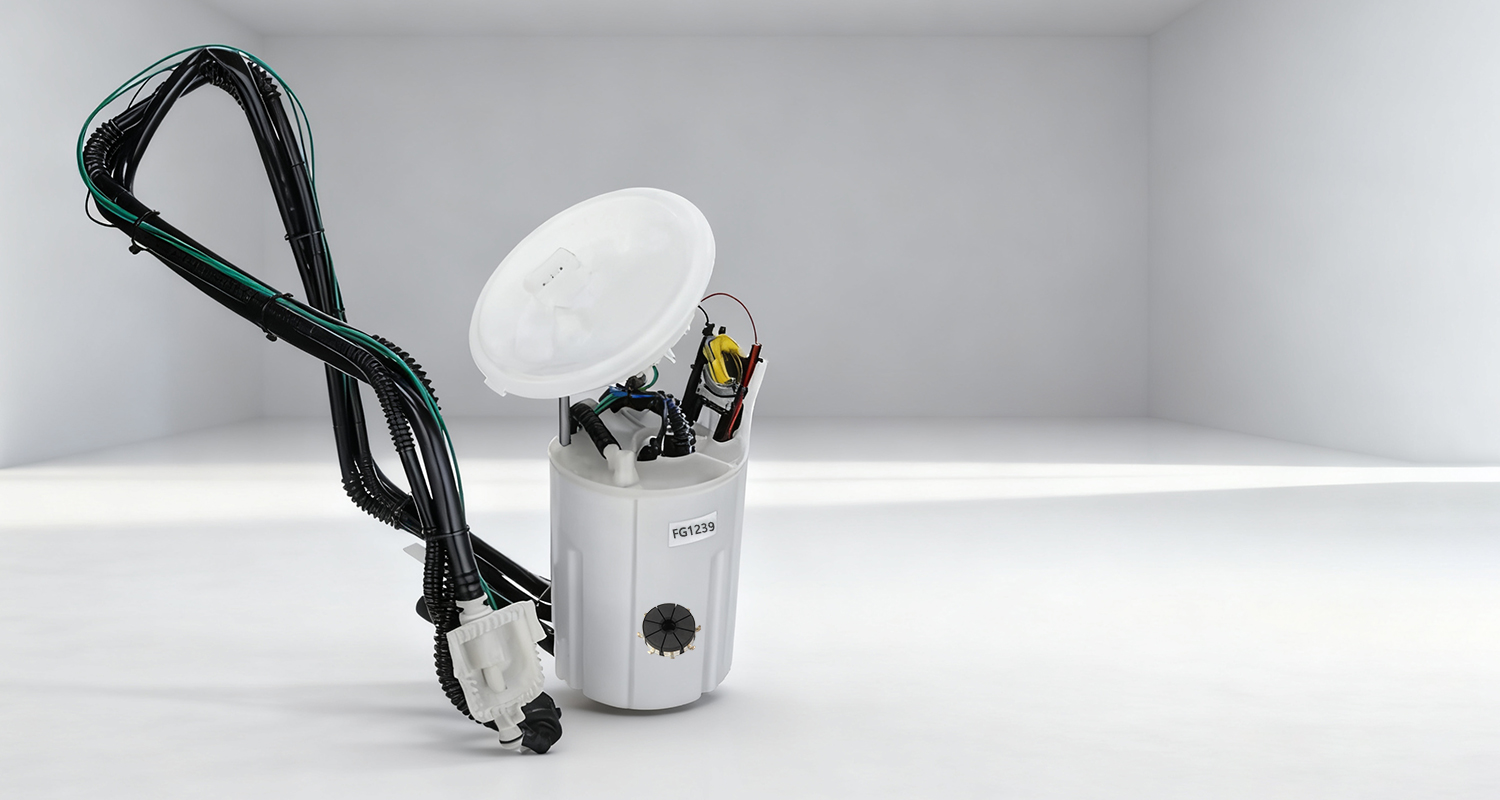
In electric fuel delivery, fuel flows directly through the motor armature. Our proprietary carbon (graphite) commutators eliminate electrochemical copper leeching, providing high reliability in modern pressurized fuel tanks.
| Critical Parameter | Industry Standard (Aftermarket) | Hualeao Engineering Benchmark | System Impact & Benefit |
|---|---|---|---|
| Rotor Radial Clearance | 0.060 – 0.090 mm | 0.020 – 0.035 mm | Eliminates low-RPM internal hydraulic slip, boosts cold-start pressure by 22% |
| Face Axial End Play | 0.045 – 0.080 mm | 0.020 – 0.040 mm | Maintains uniform film lubrication, prevents galling under continuous load |
| Armature Dynamic Imbalance | ≤ 0.15 g·mm | ≤ 0.05 g·mm | Suppresses high-frequency micro-vibrations, extending pump bearing longevity |
| Commutator Segment Runout | ≤ 0.012 mm | ≤ 0.004 mm | Minimizes mechanical brush bouncing, virtually eliminating arc-erosion |
| Biofuel Corrosion Rate | Severe copper oxidation in E85 | Inert / Carbon Passivated | Impervious to ethanol/methanol galvanic corrosion over 200,000+ km |
From high-shear urban automotive stop-starts to corrosive open-sea marine propulsion, our rotor components are calibrated for specific environmental conditions.
Modern Euro VI and EPA Tier 3 powertrains require variable delivery rotor oil pumps to reduce parasitic engine drag. In hybrid electric vehicles (PHEVs/HEVs), frequent start-stop duty cycles demand instant oil pressure buildup to prevent journal bearing wear before the combustion cycle stabilizes. Hualeao rotor sets provide fast suction response within 0.18 seconds of crank activation.
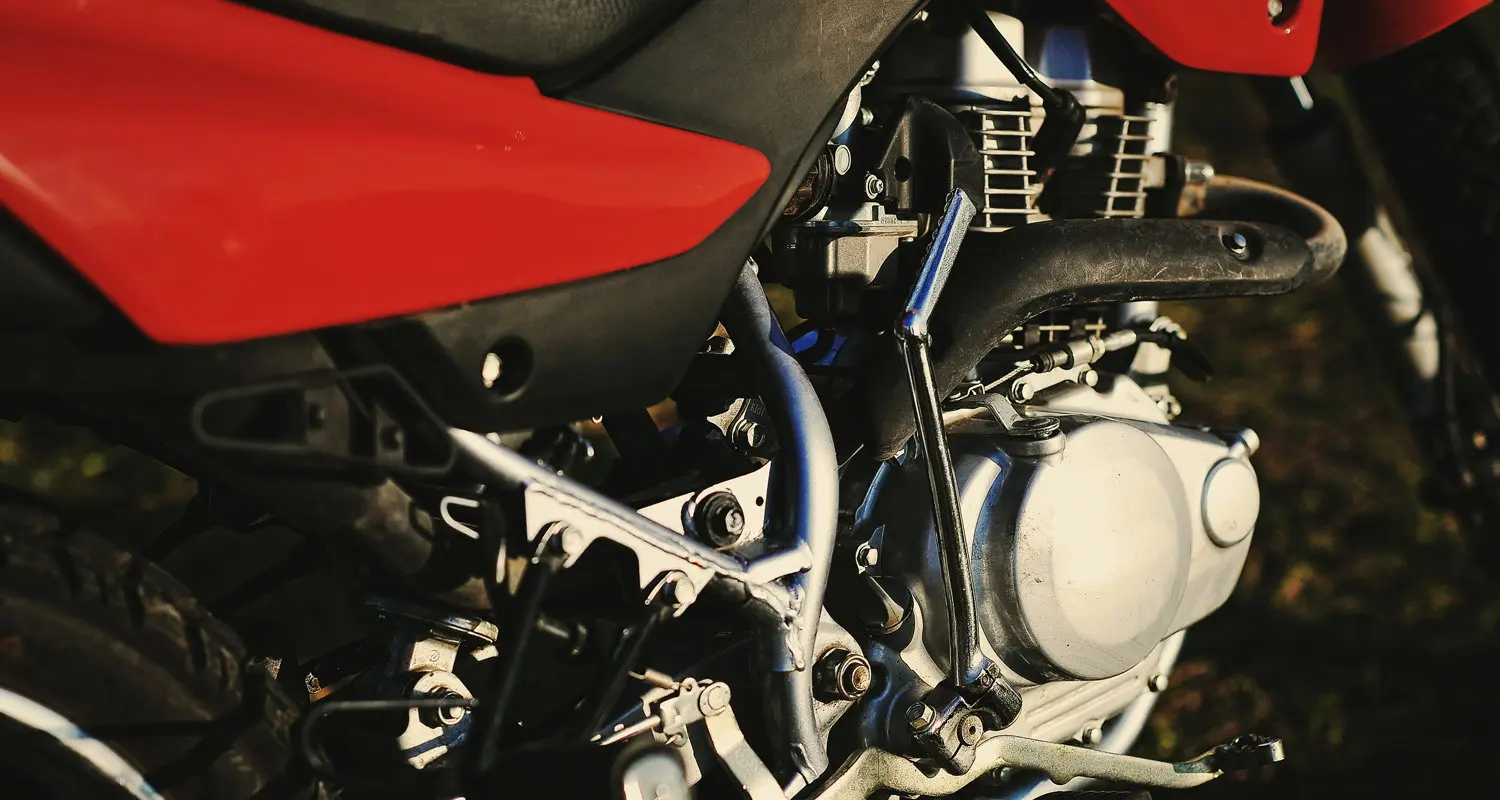
Operating in environments exceeding 10,000 RPM, motorcycle rotor oil and fuel pumps face high centrifugal stress and severe cavity vibration. Our miniaturized carbon commutators and high-density gerotors fit within compact, weight-critical crankcases while preventing boundary layer oil film breakdown under extreme thermal conditions.
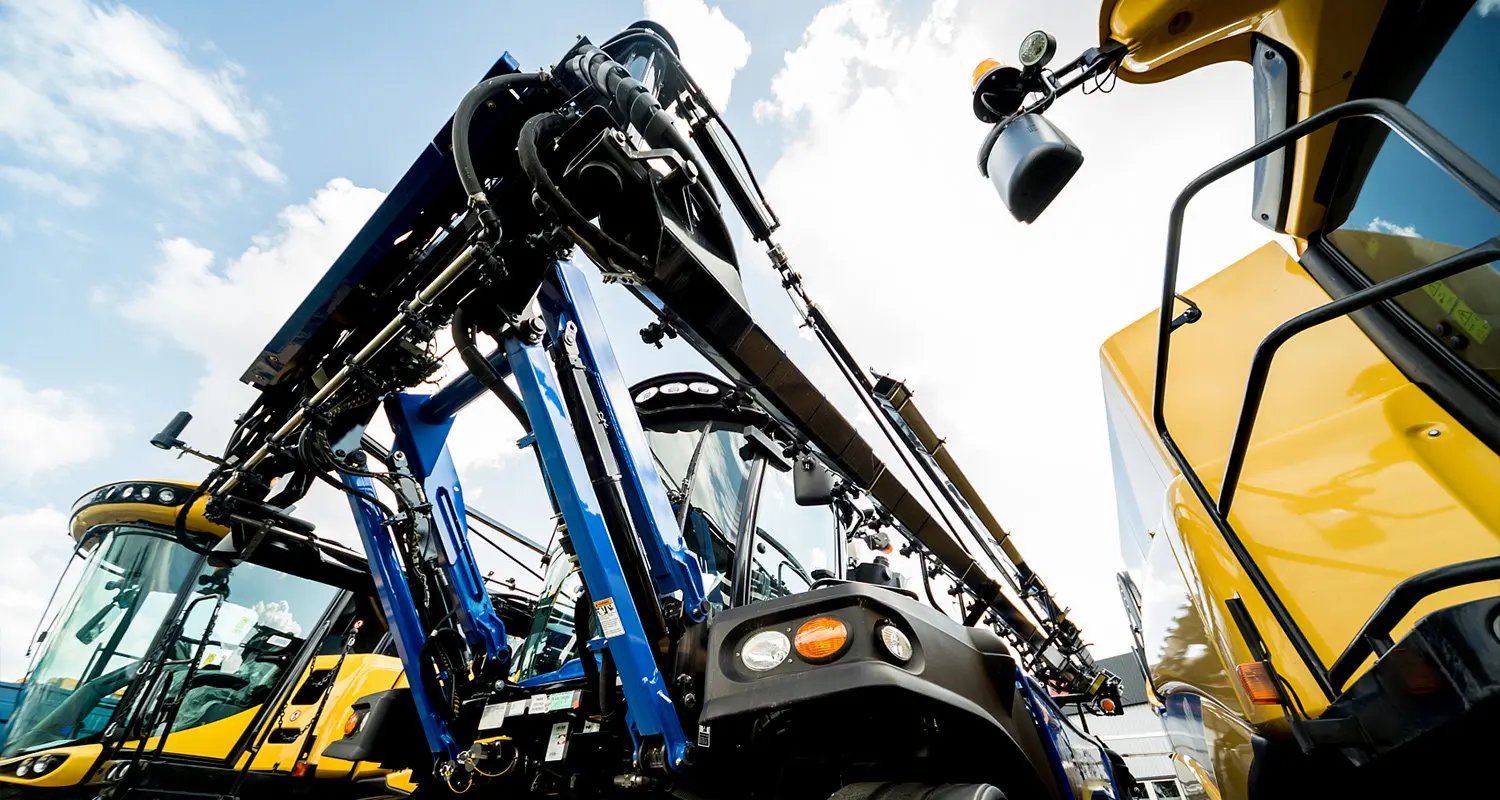
Hydraulic excavators, bulldozers, and mining haulers operate in high-dust, heavy-shock, and continuous load conditions. Hualeao manufactures reinforced rotor sets and heavy-duty armatures with surface treatments that resist micro-abrasive foreign particles suspended in lubricating fluids and hydraulic circuits.
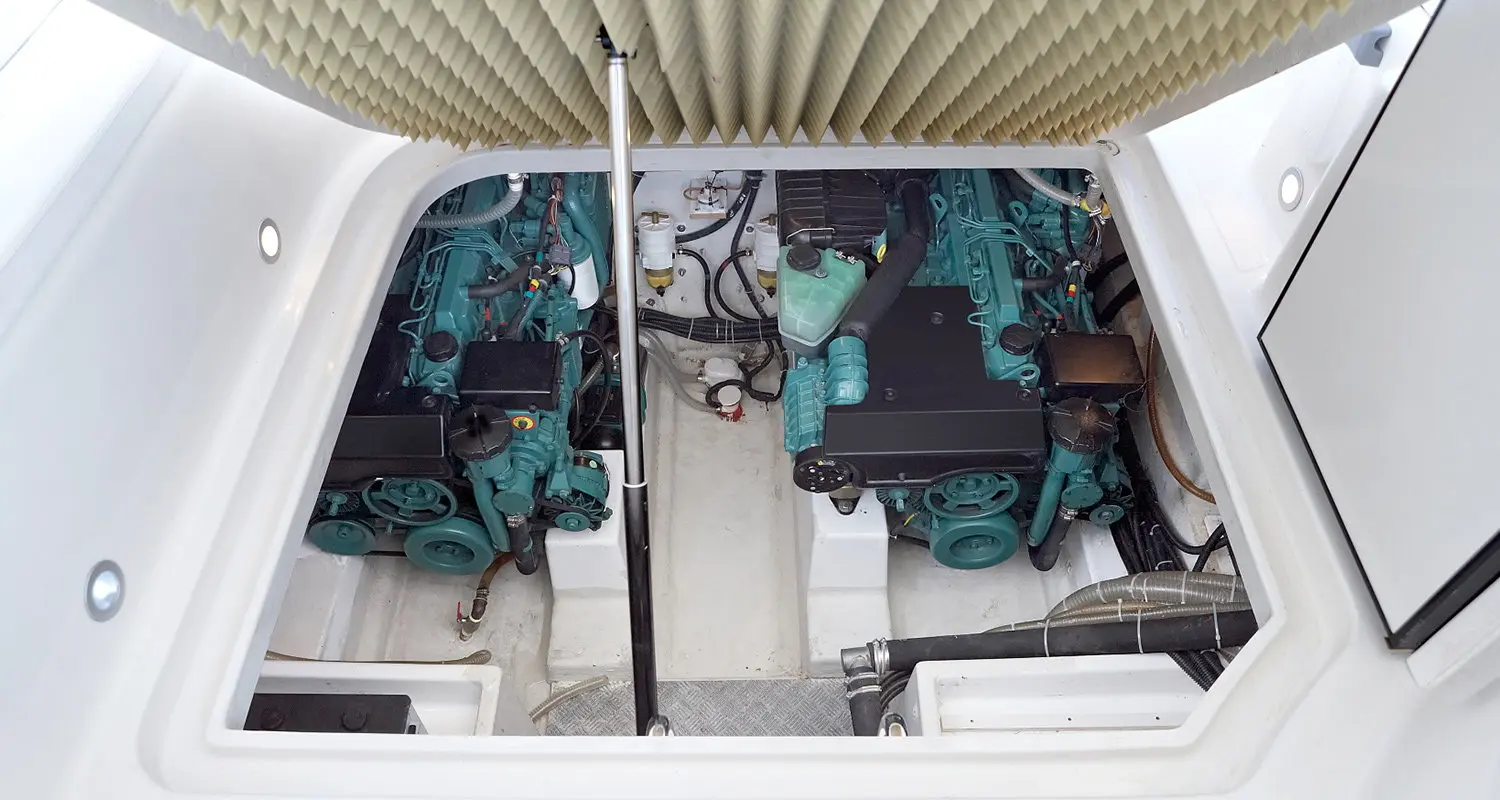
Salt spray, high relative humidity, and galvanic cell formation represent common failure causes in marine pump components. By combining graphite-rich commutators with nickel-alloy treated rotor materials, our assemblies resist salt-crust corrosion and prevent motor brush bonding during prolonged seasonal lay-offs.
In regions such as Brazil, North America, and parts of Europe where ethanol blends (E25, E85, E100) and methanol (M15, M85) are standard, standard copper commutators deteriorate via rapid organic acid attack. Hualeao’s carbon-commutated pump rotors remain stable, resisting dielectric fuel breakdown.
How localized industrial agglomeration in Ruian, Wenzhou delivers rapid prototyping, vertical integration, and cost stability for international supply partners.
Situated within Ruian, the recognized "Auto & Motorcycle Parts Capital of China", our factory accesses an integrated supply perimeter for specialized metallurgical powders, precision stamping dies, automated winding systems, and inspection fixtures within a 25-kilometer radius.
In-house tooling design and EDM spark erosion machining allow us to transition from client CAD drawings to first-article prototype production (FOT) in as few as 14 to 21 business days, compared to the 8 to 12-week lead times common with traditional Western component makers.
We maintain multi-tier contracts for high-purity natural and synthetic graphite flours, electrolytic copper strip, and phenolic novolac resins. With a continuous 60-day safety stock buffer, our clients remain protected from international freight disruptions and raw material commodity spikes.
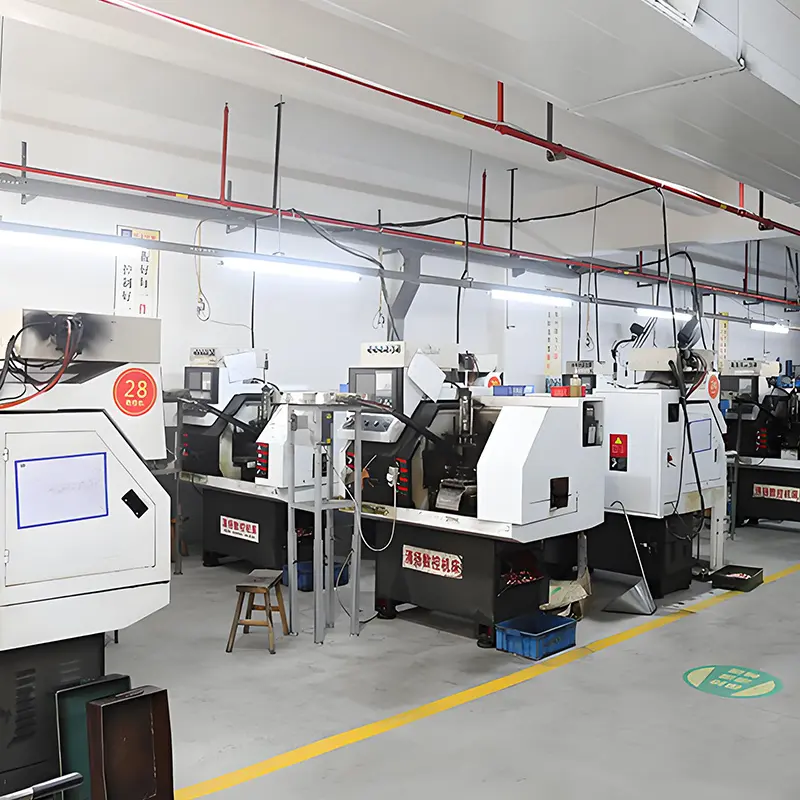

Validated direct and tier supplier for automotive electronics and high-pressure fuel pump assemblies.

Joint tribological research partnerships with universities specializing in electrical discharge and sintered metallurgy.

Immediate access to Ningbo and Shanghai deep-water container ports for scheduled global maritime export.

Recognized under national energy-saving vehicle component development programs for low-emission designs.
Architecting the next phase of fluid displacement: low-viscosity lubrication, brushless electronic drives, and synthetic e-fuel resilience.
As modern automotive engines transition to SAE 0W-16, 0W-8, and 0W-4 ultra-low viscosity engine oils to maximize fuel economy, oil pumps risk losing hydrodynamic film separation. Hualeao’s R&D is focused on Diamond-Like Carbon (DLC) coated gerotor tooth flanks and micro-textured rotor surfaces that preserve volumetric boundary pressure at 130°C without scoring.
The industry is progressively decoupling oil and fuel pump speeds from mechanical crankshaft rotation. In response, our product roadmap introduces fully integrated Brushless DC (BLDC) rotor architectures with embedded permanent magnets, enabling CAN-bus commanded variable displacement tailored to instantaneous bearing demand.
Future internal combustion configurations operating on direct-injected green hydrogen, e-methanol, and ammonia present extreme challenges regarding zero-lubricity combustion byproducts. We are advancing ceramic-matrix composites (CMC) and self-lubricating polymeric rotor matrices designed to deliver long component life in the absence of traditional petroleum films.
Ensuring engineering consistency from the raw powder batch to arrival at overseas assembly lines through certified process control.
All production lots follow standard APQP, FMEA, and PPAP Level 3 documentation requirements. Full material batch heat numbers and inspection logs are archived for 10 years, ensuring complete traceability down to specific powder blend lots.
Rotor profiles are validated using automated Zeiss CNC Coordinate Measuring Machines (CMM) and Taylor Hobson surface roughness profilometers to verify complex trochoid curves within 0.002 mm contour tolerances.
Every product line complies with international RoHS, REACH, and California Proposition 65 regulations. Chemical testing verifies the absence of hazardous polycyclic aromatic hydrocarbons (PAHs) and lead compounds in all composite matrices.
Dedicated sales engineering specialists provide on-demand technical consulting, reverse engineering, cross-referencing (Bosch, Denso, Delphi, Aisin interchange catalogs), and localized warranty support for Tier-1 and aftermarket operations worldwide.
Detailed engineering answers address tolerances, material choices, lubrication mechanics, and customized prototyping.
Rotor oil pumps (gerotors) utilize internal cycloidal/trochoidal gearing where the inner rotor drives the outer rotor within an eccentric housing. This geometry provides lower flow ripple, superior volumetric efficiency at both idle and peak RPM, and significantly lower acoustic output. Because contact stress is distributed along sweeping trochoidal profiles rather than localized pitch points, gerotors demonstrate lower mechanical wear over extended engine lifecycles.
Electric fuel pumps operate submerged in fuel. Modern commercial fuels frequently contain oxygenated additives such as ethanol and methanol, which generate organic acids and conduct stray electric currents. In these conditions, traditional copper segments undergo rapid galvanic erosion and spark pitting, which can lead to pump failure within 400 to 800 hours. Carbon-graphite commutators are chemically inert, providing stable contact resistance and runtimes exceeding 4,000 continuous hours.
Concentricity is maintained through multi-station precision progressive compaction dies followed by rotary surface grinding with automated in-process gauging. Axial thickness is controlled within a strict ±0.005 mm window, while face planarity and parallelism are verified using optical interferometry, preventing hydraulic cross-chamber leakage.
Yes. Our metrology facility utilizes high-precision optical CMM scanners and laser profile digitizers capable of extracting exact trochoidal curve equations and eccentric offsets from worn samples. Our engineering team can reconstruct original nominal parameters, optimize tip clearances, and generate new tool paths for direct manufacturing.
We utilize specialized sintered powder grades containing iron, copper (1.5–3.5%), nickel (1.0–2.0%), molybdenum, and carbon. Following high-temperature sintering at 1,120°C in endothermic gas, components undergo steam treatment to develop a continuous magnetite (Fe3O4) passivation layer, yielding surface hardness levels up to HV 550 and strong cavitation resistance.
Standard lead times for new custom rotor development involve 15–20 days for tooling development and initial sample testing. Upon PPAP Level 3 approval, full-scale production runs are completed within 25–35 business days, supported by buffer stocking programs for repeat recurring orders.
Every armature assembly passes through computerized dual-plane dynamic balancing equipment operating at speeds up to 10,000 RPM. Automated micro-milling removes minute amounts of material from designated rotor balance rings, keeping dynamic balance within 0.05 g·mm, which helps reduce bearing vibration and brush noise.
Our manufacturing and assembly systems operate under accredited ISO 9001 and IATF 16949 automotive quality certifications. We maintain comprehensive documentation including continuous calibration protocols, gage R&R studies, and standardized inspection reporting across all component batches.
Direct supply options for fuel systems, oil lubrication loops, and engine management electronics.
Precision-pressed carbon commutator engineered for continuous automotive EFI pump armatures.
View Product Details
Complete drop-in pump motor module with balanced rotor core and noise-dampening impellers.
View Product Details
Pre-calibrated planar oxygen sensor providing real-time air-fuel ratio telemetry to vehicle ECUs.
View Product Details
Heavy duty, reinforced segmented commutator for high-pressure fuel pump applications.
View Product Details
High-permeability core stack featuring integrated graphite commutator and epoxy impregnation.
View Product Details
Engineered for alternative fuel markets, resisting chemical wear from high ethanol contents.
View Product Details
Passivated sintered rotor profiles formulated for marine outboards and construction equipment.
View Product Details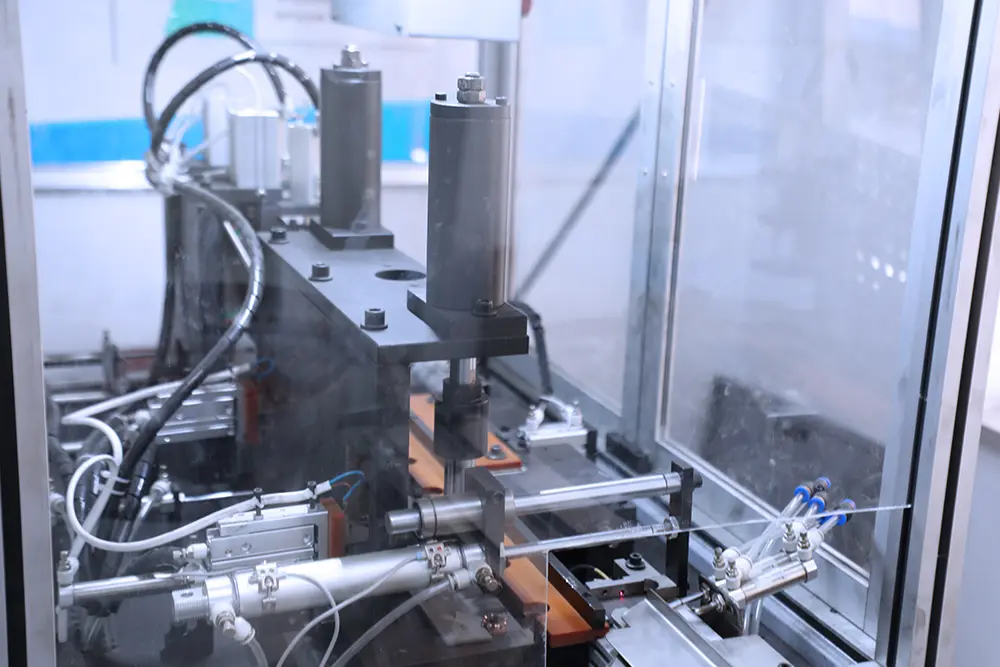
Custom trochoid profile engineering designed to client flow rate specifications and envelope dimensions.
View Product DetailsSubmit your CAD models (STP, IGS, DWG), sample parameters, or OE reference numbers. Our powertrain engineers review clearances, material specifications, and volumetric requirements within 24 business hours.
