Explore our flagship, precision-machined armatures, ethanol-resistant graphite commutators, and high-efficiency motor cores designed for OEM Tier-1 assemblies and global aftermarket reliability.

Advanced graphite disc commutators delivering superior transmission stability, minimal electrical sparking, and zero fuel wear.
Configure Product
Complete rotor-stator integrated fuel pumps built with high-torque precision balanced micro-armatures for steady EFI delivery.
Configure Product
Precision lambda feedback sensor (89465-0E040 standard) ensuring closed-loop ECU calibration and catalytic converter protection.
Configure Product
High-volume OEM replacement graphite commutator tailored for heavy alcohol and ethanol blends with ultra-low resistance.
Configure Product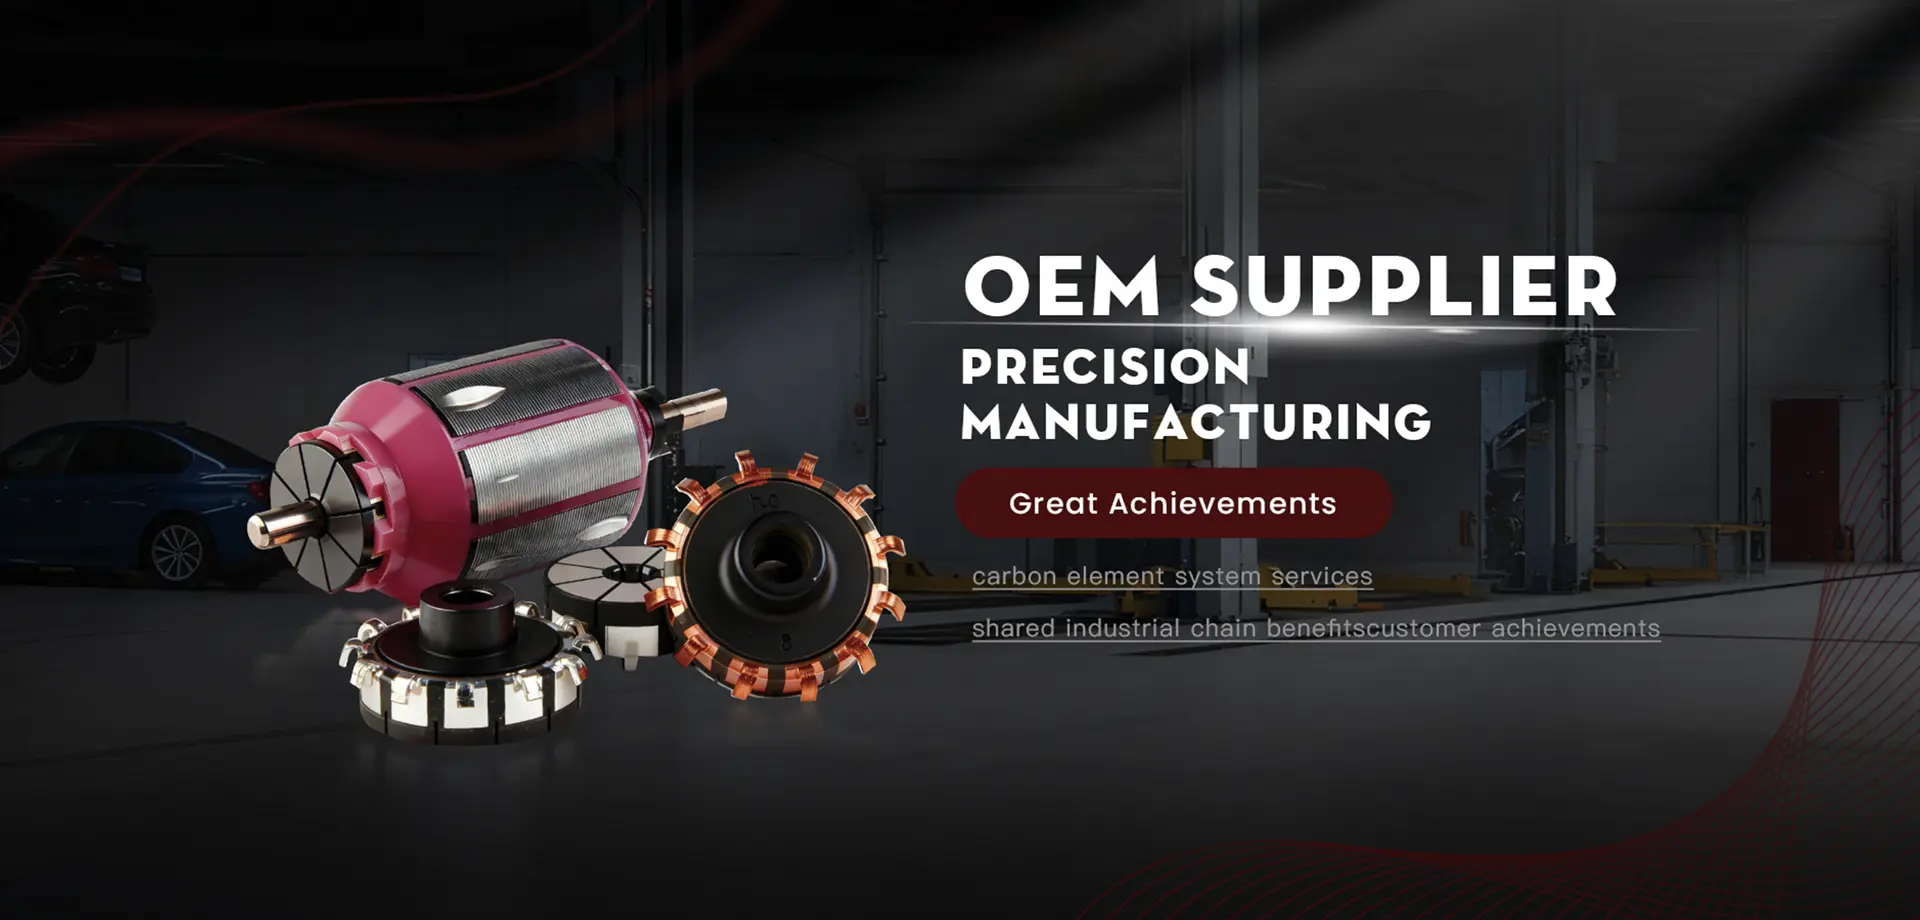
Cold-rolled silicon steel laminated stators offering minimal core losses, optimized magnetic circuits, and vibration-proof coils.
Configure Product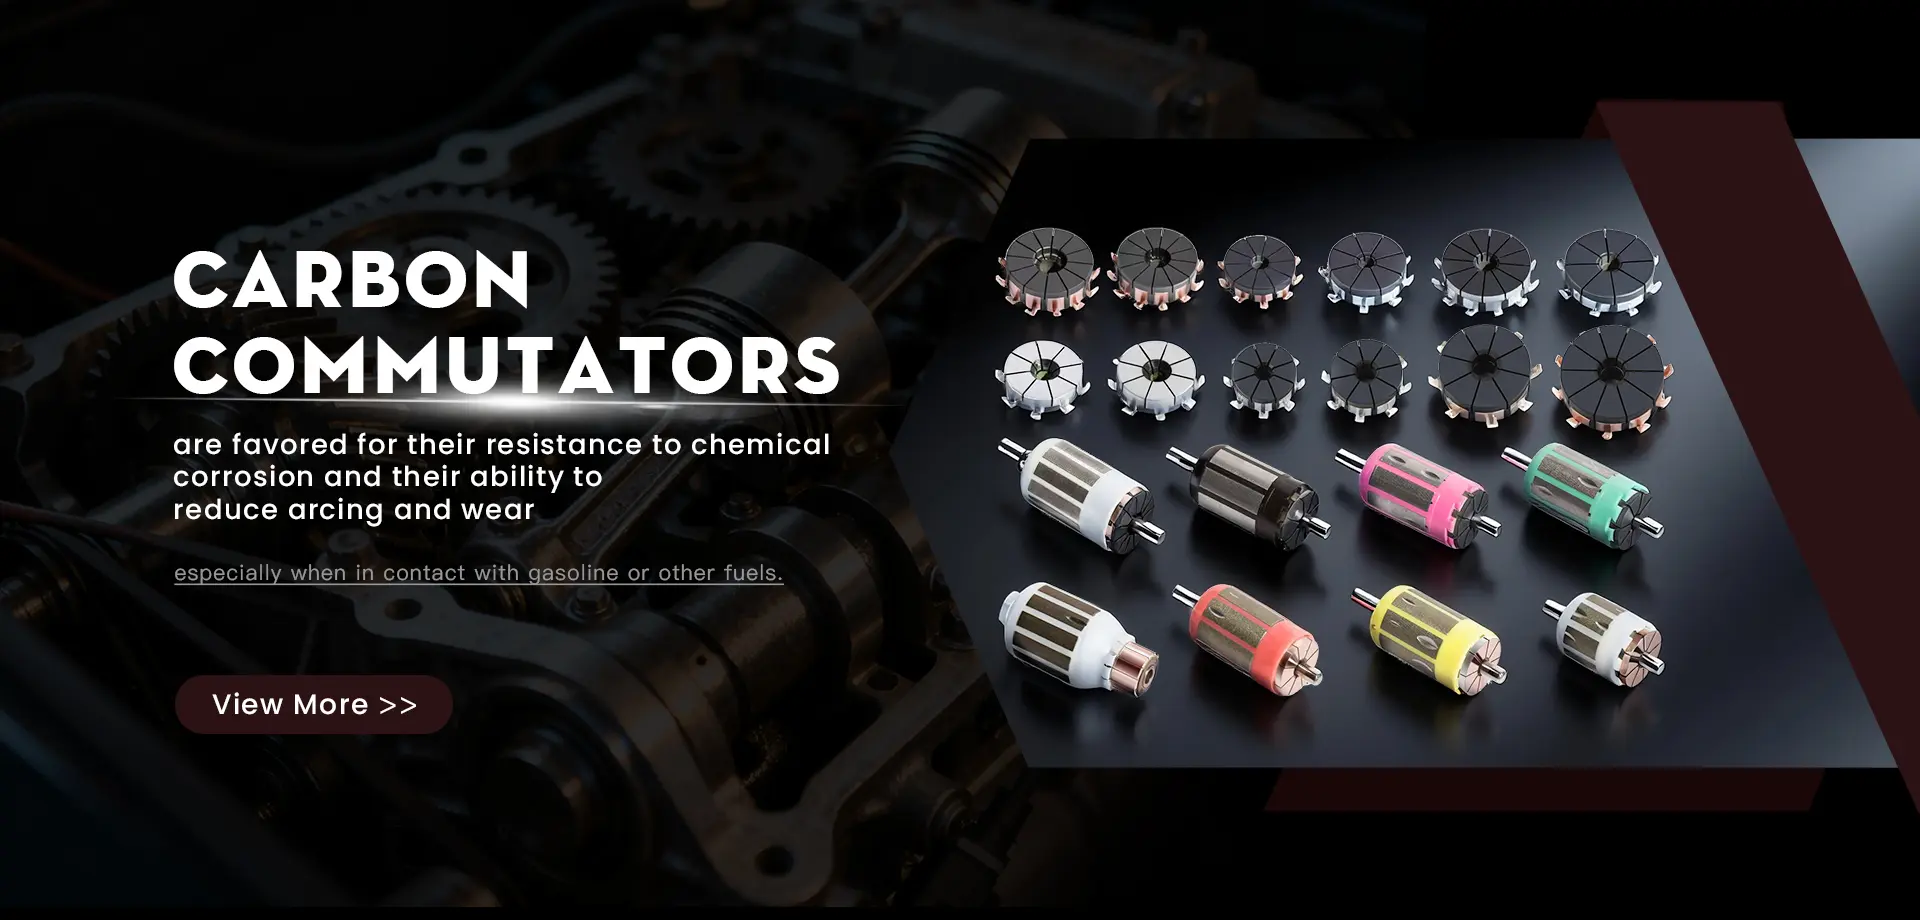
ISO G1.0 dynamically balanced wound armatures for low-noise, high-RPM automotive sub-assemblies and actuator pumps.
Configure Product
Specialty micro-stator and commutator sets engineered for instantaneous start-up torque in gasoline direct injection (GDI) circuits.
Configure Product
Bespoke armature windings, customized segment layouts, and high-temp resin potting matched strictly to OE engineering drawings.
Configure ProductHeadquartered in Lianjiang Industrial Park, Pantai Street, Ruian City, Wenzhou Hualeao Automotive Parts Co., Ltd. has established world-class manufacturing infrastructures dedicated to electromagnetic rotor and stator innovation.
Meeting modern vehicle energy conservation metrics demands seamless integration from pure raw material procurement to end-of-line electrical testing.

Trusted supplier to established automotive electronics, powertrain developers, and fuel-system manufacturers globally requiring zero-defect micro-motor commutators.

Ongoing technical collaborations with national universities and scientific research institutes to advance anisotropic graphite formulations and reduce high-frequency hysteresis.

Strict auditing of high-density phenolic resins, high-conductivity copper segments, and refined graphite blocks ensures lot-to-lot homogeneity across multi-million piece annual runs.

Successfully replaced high-cost European and Japanese carbon commutators and motor cores across multiple passenger vehicle platforms, slashing procurement costs while matching service life.
An analytical overview of electric motor core manufacturing, electromagnetic efficiency mandates, and why carbon-commutated armatures remain essential in next-generation fluid handling.
The global stator and rotor market is experiencing transformative growth, driven by vehicle electrification, stringent Euro 7 and EPA emissions caps, and the rapid shift toward highly integrated mechatronic actuators. Electric fuel injection (EFI) systems, auxiliary powertrain pumps, and industrial fluid delivery loops demand electric motors with operational efficiencies exceeding 85%.
Traditional copper-commutator armatures are rapidly degrading when exposed to modern oxygenated biofuels (E10, E85, and neat methanol), creating a massive market vacuum for specialized stator-rotor topologies fitted with chemically inert carbon-graphite contact segments.
A stator's core function is to guide electromagnetic flux with minimal losses. Modern high-speed automotive pumps demand low-loss electrical silicon steel laminations (e.g., 0.35mm to 0.50mm non-grain-oriented grades). Precision progressive stamping and interlock stamping prevent burr formation, which directly reduces interlaminar eddy current loops.
Wenzhou Hualeao aligns stator magnetic circuit geometry with skewed-slot rotor architectures. This minimizes cogging torque, attenuates high-frequency acoustic harmonics, and ensures stable torque transfer across cold starts (-40°C) to engine bay peaks (+135°C).
In electric fuel delivery modules, the motor stator and rotor operate entirely submerged inside volatile fuel to provide natural convective cooling. However, alcohol-blended fuels exhibit aggressive electrolytic conductivity and low lubricity. Under direct electrical potential, standard metallic commutators experience severe spark erosion, chemical pitting, and segment short-circuiting.
Our carbon-graphite disc and ring commutator rotors establish a microscopic lubricating transfer film on the brush contact zone. This eliminates metallic pitting and guarantees a maintenance-free working lifecycle of over 10,000 continuous hours.
Every stator, rotor armature, and commutator manufactured in our Wenzhou production hub passes through four closed-loop validation stages to ensure uncompromising performance.
Finite element analysis (FEA) optimizes flux lines across stator tooth profiles and rotor winding slots. Slot fill factors are maximized while minimizing winding overhang to restrict ohmic losses.
Refined natural and synthetic graphite particles are compounded with specialized thermosetting phenolic binders. Hydrostatic pressing followed by inert-atmosphere graphitization provides high compressive density.
Precision multi-axis automated flyers wind enameled copper wire directly onto insulated rotor cores with tension control. Hook terminals are hot-stake welded or laser fused to graphite contact pads.
Rotors undergo dual-plane computer dynamic balancing (ISO G1.0 specification), cutting residual vibration. Final testing checks surge voltage insulation, bar-to-bar resistance, and roundness (TIR < 0.003mm).
Whether operating under high hydrostatic pressure, deep salt-spray conditions, or prolonged dry runs, our stators and rotors exceed rigorous Tier-1 specifications.
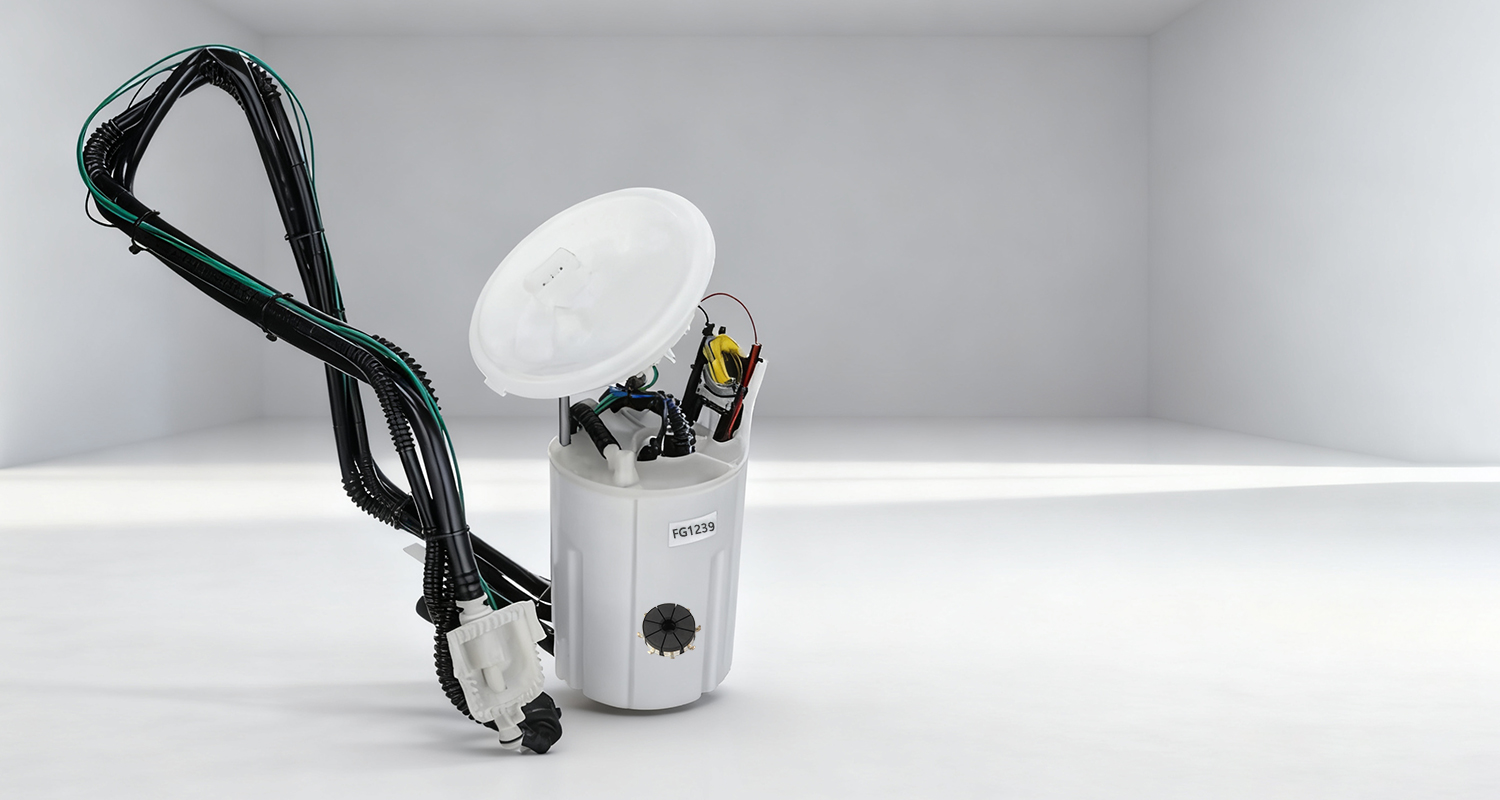
Modern passenger vehicles with gasoline direct injection (GDI) require constant rail pressure of 3.5 to 6.5 bar. Hualeao rotors deliver continuous torque with low electromagnetic interference (EMI), protecting onboard ADAS sensors and CAN-bus control units from voltage ripple spikes.
Explore Automotive Armatures
Motorcycle EFI fuel modules feature constrained mounting geometries. Our compact carbon commutator rotors are engineered for high angular velocities up to 12,000 RPM, providing immediate cold-start throttle response and resisting vibrations up to 20G.
Explore Powersport Rotors
Excavators, loaders, agricultural tractors, and mining haulers face contaminated diesel fuels, heavy shock loads, and high engine compartment temperatures. Our stator laminations feature high-temperature H-class insulation resins to prevent thermal shorting.
Explore Heavy Duty Stators
Salt spray and humid marine conditions rapidly corrode conventional copper motor components. Hualeao carbon-impregnated commutators and passivated stator cores pass 500-hour neutral salt-spray tests without galvanic degradation or loss of insulation resistance.
Explore Marine AssembliesAnticipating the transition to carbon neutrality, synthetic e-fuels, and ultra-high-speed electric auxiliary actuators through our strategic R&D trajectory.
Integration of multi-walled carbon nanotube (MWCNT) reinforcement within graphite matrices. This reduces electrical resistance by 18% while enhancing mechanical shear strength during sudden high-pressure backflow.
Expansion into ultra-thin (0.20mm) cobalt-iron and high-grade electrical steel laminations for brushless sensorless fuel pumps, achieving operating efficiencies exceeding 92% in 48V mild-hybrid platforms.
Pioneering non-sparking commutation interfaces for auxiliary thermal management and cryogenic pumps serving liquid hydrogen and renewable methanol fuel-cell mobility ecosystems.
Wenzhou Hualeao Automotive Parts Co., Ltd. combines German and Japanese manufacturing methodologies with lean domestic cost advantages. Our 6,200m² specialized facility houses continuous automated sintering furnaces, CNC commutator profiling lathes, high-precision automated armatures winders, and computerized end-of-line electrical diagnostic benches.
We serve leading fuel system developers, pump rebuilders, and Tier-1 integrators globally, providing standard catalog fulfillment as well as rapid rapid drawing-to-sample OEM custom engineering.
Review our application guides and technical whitepapers regarding motor commutation physics, oxygen feedback loops, and DC armature reliability.
An oxygen (O2) sensor is located within the exhaust manifold to monitor unburned oxygen concentrations post-combustion. It communicates real-time stoichiometric voltage feedback to the ECU, fine-tuning fuel injection duration to preserve catalytic convertors and meet Euro 6/7 standards.
Read Sensor GuideTraditional copper commutators rapidly oxidize and pit when exposed to oxygenated ethanol blends (E10 to E85). Graphite commutators feature lower friction coefficients, self-lubricating dry properties, and total chemical immunity to organic acids found in fuel blends.
Read Commutator GuideA precision commutator acts as an alternating rotary switch, reversing current polarity across armature coil groups as they traverse opposite magnetic poles. Proper segment geometry eliminates inductive arc-over and electromagnetic brush noise.
Read Dynamics WhitepaperIn-depth answers covering material selection, geometric tolerances, custom prototyping, and severe fuel durability for purchasing teams and development engineers.
The carbon commutator functions as an electromechanical rotary interface that transfers electric current between stationary carbon brushes and the rotating armature windings. By reversing current flow precisely at the neutral magnetic zone, it generates uninterrupted unidirectional electromagnetic torque. Because electric fuel pumps operate immersed in fuel, the carbon material provides natural boundary lubrication, prevents electrolytic pitting, and maintains constant fuel pressure without premature brush failure.
Standard copper commutators react corrosively with bio-ethanol (E10, E20, E85) and methanol blends. In the presence of fuel water content and electrical potential, copper undergoes rapid electrolytic corrosion and galvanic erosion, leaving deep micro-trenches that shred brushes within 200–500 operational hours. Synthetic resin-bonded graphite carbon commutators are chemically inert, providing wear resistance up to 10× greater than pure copper in aggressive oxygenated fuels.
Yes. Over 60% of our production capacity is dedicated to custom OEM and Tier-1 engineering contracts. Our engineers evaluate customer 2D/3D CAD models (STEP, DWG, IGES) or physical samples, checking segment layout, lamination stack height, hook terminal geometry, wire gauge, and thermal insulation requirements. We fabricate dedicated tooling, conduct mold-flow simulation, and deliver rapid verification prototypes within 15 to 25 working days.
Our automated high-speed rotor finishing line enforces dynamic balance standards adhering to ISO 1940-1 Grade G1.0 or G2.5 depending on operational RPM. Armature shaft runout (Total Indicated Runout - TIR) is kept within 0.003mm, and commutator segment surface roundness is controlled to under 0.0025mm, preventing brush bounce, acoustic whining, and high-frequency EMI noise spikes during operation.
Our stator and rotor assemblies are deployed across North America, South America (particularly Brazil's massive flex-fuel ethanol market), Europe, and Southeast Asia. Key applications span passenger vehicle EFI engines, motorcycle fuel injection systems, heavy diesel construction excavators, marine coastal power units, and industrial fluid metering devices.
We implement a strict IATF 16949-aligned closed-loop quality management system. This includes automated optical inspection (AOI) for commutator segment spacing, high-potential dielectric breakdown testing (up to 1,500V), bar-to-bar micro-ohm resistance profiling, and batch endurance testing in temperature-controlled E85/M15 fuel chambers under continuous full load.
Review our complete lineup of high-precision graphite commutators, complete pump assemblies, lambda sensors, and electric motor sub-components ready for global distribution.
High-density isotropic carbon face engineered for compact in-tank fuel pump motors with minimal axial profile requirements.
Request CAD & Data
Engineered for high-pressure multi-port fuel injection, featuring precision-machined impeller vanes and balanced micro-stators.
Request CAD & Data
Fast-heating zirconia ceramic element with laser-welded stainless steel shielding for immediate closed-loop stoichiometric fuel control.
Request CAD & Data
Direct drop-in replacements for standard Denso, Bosch, and Walbro pump models with 100% matched copper terminal tangs.
Request CAD & Data
Interlocked silicon steel laminations coated with anti-rust oil, optimized for brushless and brushed micro-actuators alike.
Request CAD & Data
Reinforced with chemical-resistant epoxy potting to safeguard copper winding wire from high alcohol concentrations.
Request CAD & Data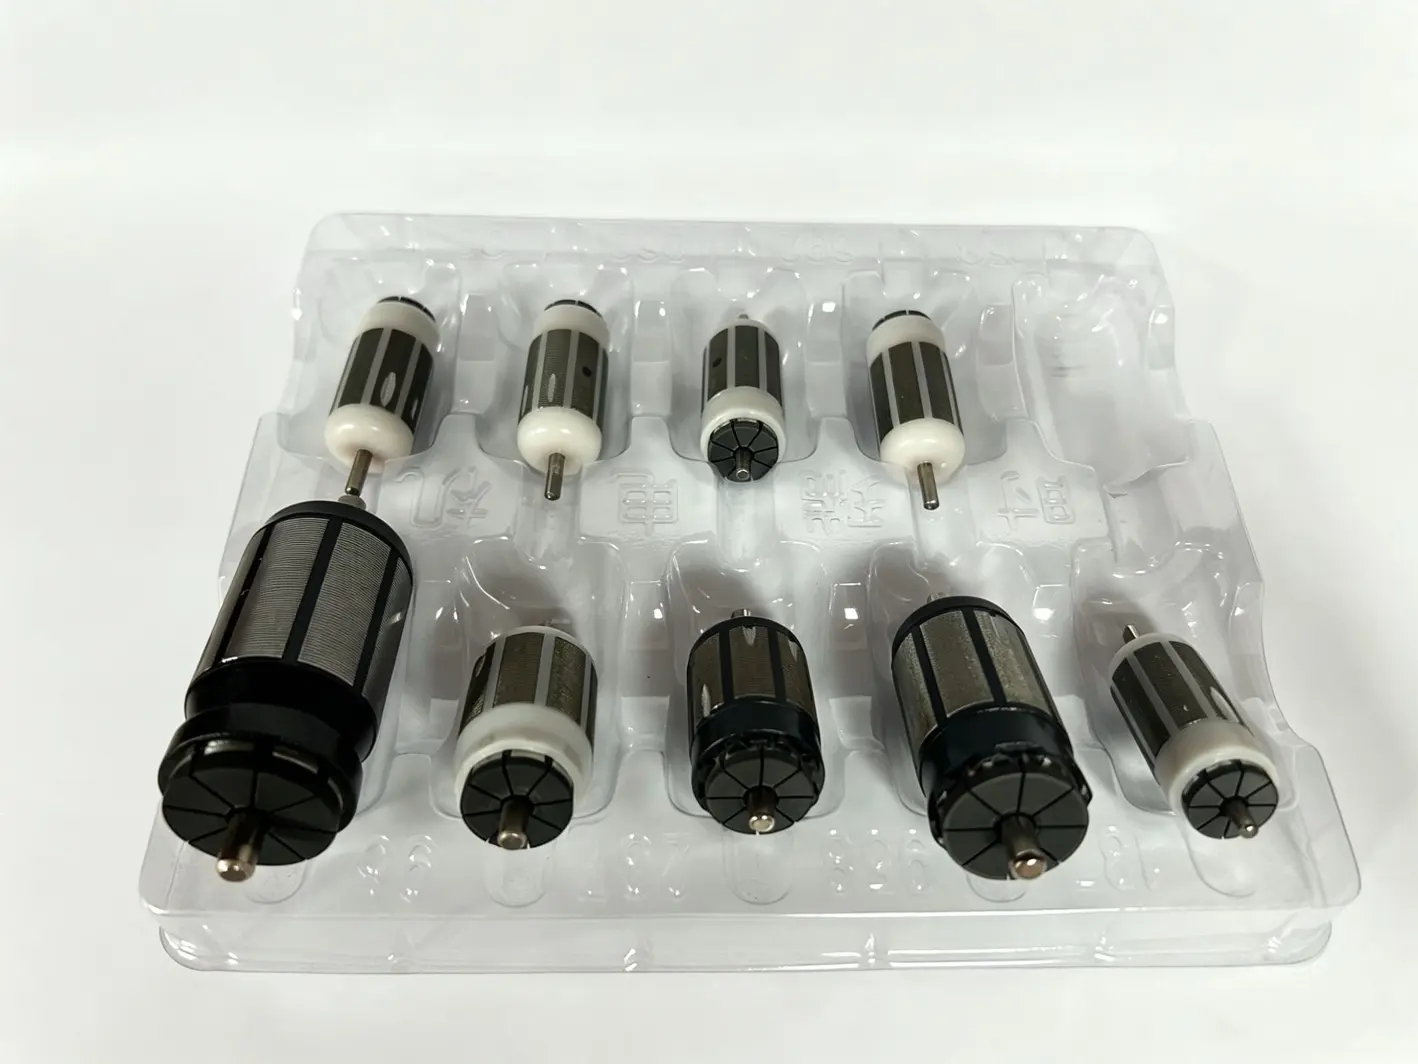
Designed for severe duty cycles in earthmoving hydraulic pumps and high-vibration off-road engine enclosures.
Request CAD & Data
Custom insulator bases and commutator segment arrays manufactured to client specifications for specialty robotics and actuation.
Request CAD & DataWhether you are developing next-generation flex-fuel pumps, localizing import commutators, or seeking high-volume batch supply, our engineering sales group is prepared to provide comprehensive drawings, validation data, and volume quotes.
