Direct supply of corrosion-proof carbon commutators, precision EFI electric fuel pumps, oxygen lambda sensors, and best-selling core assemblies built for alpine duty cycles and European fuel compliance.

Formulated with graphite-copper matrix to withstand aggressive ethanol (E10/E85) fuels across Austria and Central Europe without copper dissolution or premature erosion.

High-output in-tank and inline electric fuel pump assemblies delivering smooth hydraulic pressure up to 6.5 Bar, optimized for cold-crank stability in Alpine winter conditions.

High-precision upstream and downstream planar zirconia sensors that communicate with engine control units to deliver stoichiometry control and protect catalytic systems.

Our internationally recognized commutator assemblies including model HC-QZQE-049C, widely sourced by high-volume pump remanufacturers across Central Europe.
Austria is not simply a consumer market for automotive components; it is an engineering epicenter of global renown. Anchored by the ACstyria Mobility Cluster, the automotive industrial corridor stretching from Graz to Steyr represents the frontier of powertrain engineering, vehicle contract assembly (such as Magna Steyr), and advanced propulsion testing (spearheaded by AVL List). Supplying electric fuel pumps into this landscape requires adhering to technical tolerances and validation rigor that far exceed conventional commercial standards.
In Austria, electric fuel pumps must contend with the physical extremes of the Alpine climate. Vehicles operating in Tyrol, Vorarlberg, or Carinthia encounter sustained sub-zero temperatures down to -30°C, accompanied by steep altitude fluctuations exceeding 2,500 meters above sea level. Under these environments, fuel viscosity increases, atmospheric pressure drops, and cold-cranking resistance demands instant hydraulic pressurization without brush arcing or cavitation.
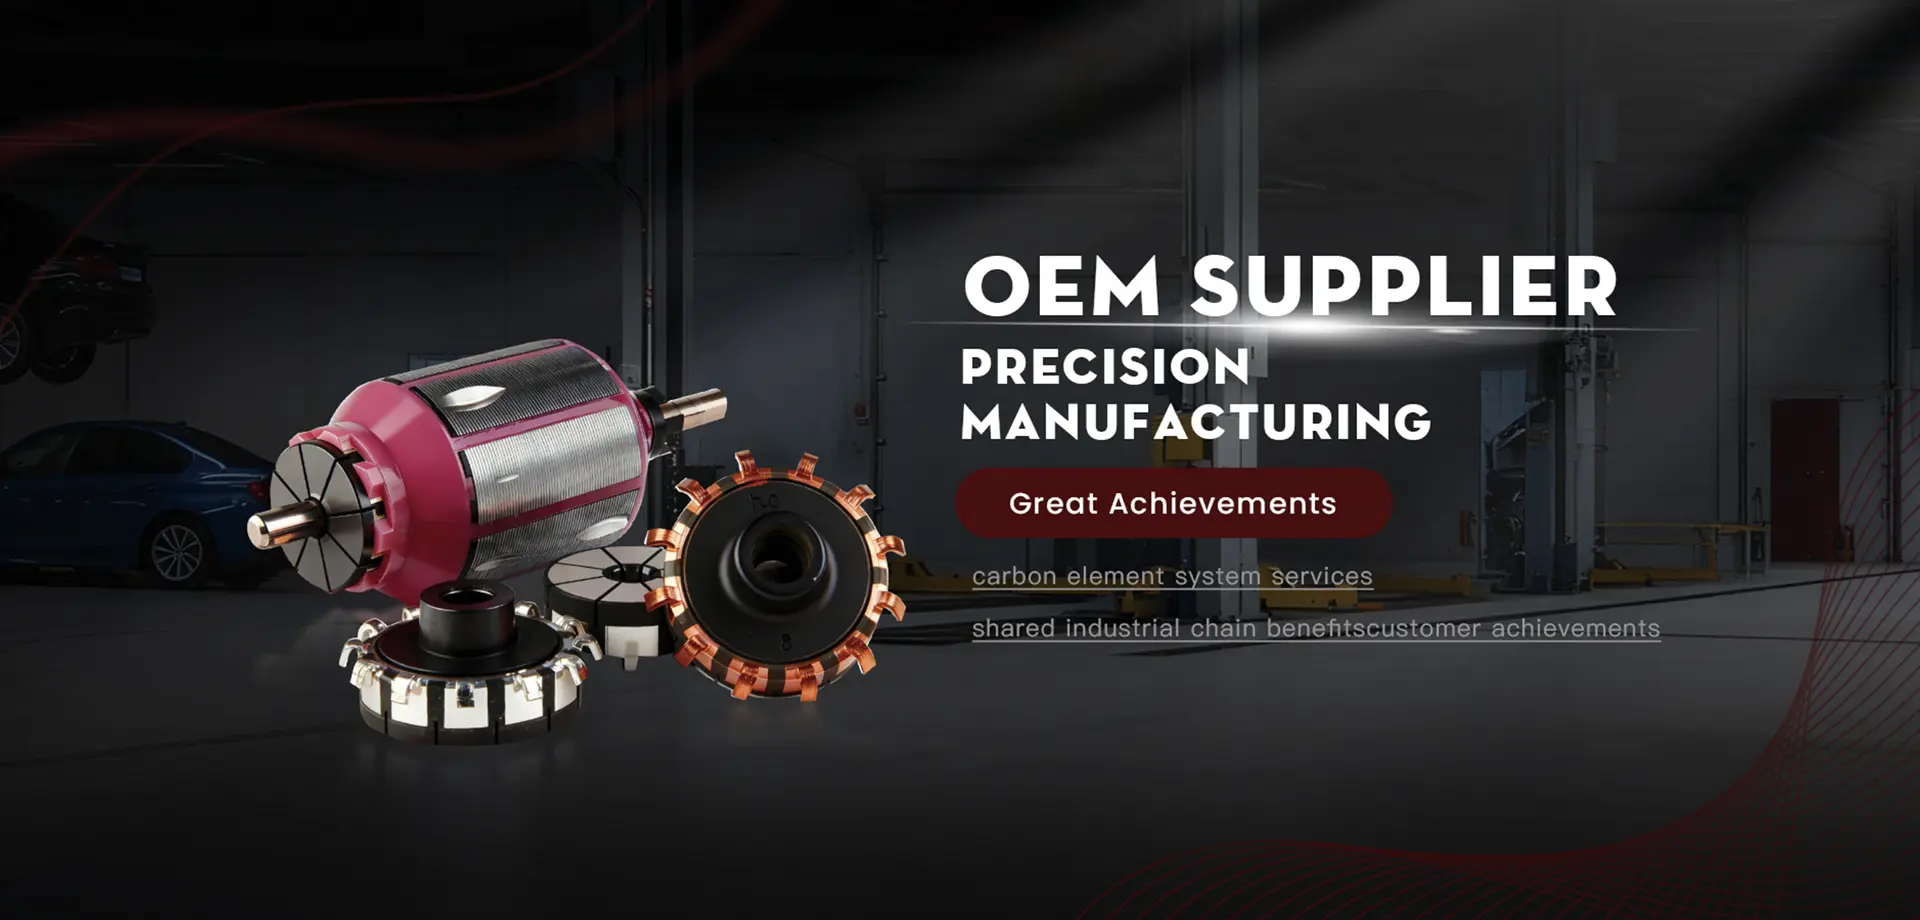
Why Austrian Tier-1 engineering teams and fleet remanufacturers are systematically phasing out conventional copper commutators in favor of advanced graphite matrixes.
| Evaluation Parameter | Standard Copper Commutators | Hualeao Carbon (Graphite) Commutator System | Advantage for Austrian Operators |
|---|---|---|---|
| Ethanol Corrosion (E10/E85) | Severe galvanic oxidation & copper dissolution | Chemically inert; zero galvanic oxidation | Eliminates pump seizure in European alcohol-blended fuels |
| Operating Lifespan | 1,200 – 1,800 Operational Hours | > 5,000+ Continuous Operational Hours | Drastically cuts replacement frequency in transit and alpine fleets |
| Commutation Sparking & EMI | High electrical noise; brush pitting | Self-lubricating surface, minimal micro-sparking | Protects delicate ECU logic and hybrid powertrain sensors |
| Alpine Cold-Start Reliability | High friction coefficient in cold fuel (-25°C) | Constant low friction coefficient across -40°C to +120°C | Guaranteed instantaneous cold starting on mountain passes |
| Dimensional Runout (TIR) | ± 0.008 mm nominal | ≤ 0.003 mm precision diamond turned | Near-silent cabin operation; reduced hydraulic vibration |
The global fuel pump sector is undergoing a profound structural shift. While battery electric vehicles capture urban headlines, the enduring reality of commercial transport, off-highway engineering, alpine emergency fleets, and global hybrid platforms requires electric fuel pumps manufactured to higher durability standards than ever before.
For European Tier-1 procurement teams, the challenge has always been balancing the prohibitive production overheads of domestic European facilities with the uncompromising reliability required by European standards. Wenzhou Hualeao Automotive Parts Co., Ltd. solves this equation by operating in China's automotive capital — Ruian, Wenzhou — integrating complete upstream raw material synthesis with end-to-end robotic machining.
Our facility does not rely on third-party sub-contractors for critical phases. From raw carbon block pressing and copper terminal staking to automated diamond cutting and helium leak detection, every stage is contained within our 6,200 m² production site. This delivers up to 38% cost-efficiency gains over European domestic equivalents without conceding a single micrometer in dimensional tolerance or IATF 16949 conformance.
Our micro-motor assemblies and fuel pump technologies are purposefully deployed across five core sectors within Austria and surrounding Central European territories.
Providing high-reliability submerged pumps for 4WD platforms, ensuring seamless fuel atomization during continuous steep-incline operations along Grossglockner and Brenner transit corridors.
Explore Passenger RangeUltra-compact, high-RPM (up to 12,000 RPM) miniature electric fuel pump armatures serving Austrian motorsport, enduro, and adventure bike configurations.
Explore PowersportsHeavy-duty feed pumps installed in tractors, harvesters, and Alpine slope forestry machines requiring heavy vibration resistance and zero vapor locking in summer heat.
Explore Agricultural RangeDedicated corrosion-resistant assemblies running on Austrian lakes (e.g. Lake Constance, Wörthersee) engineered to prevent fuel leakage and galvanic pitting.
Explore Marine GradeHeadquartered in Lianjiang Industrial Park, Ruian, Hualeao combines certified infrastructure with direct engineering collaboration for international OEMs and warehouse distributors.
We serve as a primary contract partner to automotive electronics and fuel-system assemblies that require continuous batch reliability, zero line stoppages, and OE interchangeability.
Active R&D cooperation with material science institutes accelerates our high-density graphite formulation and nano-coating resilience against aggressive European bio-additives.
Long-term upstream sourcing ensures certified high-purity electrolytic copper and uniform graphite batches, securing uninterrupted repeat production schedules year-round.
Every fuel pump armature and commutator manufactured in our Wenzhou facility passes through four strictly documented verification stages to ensure compliance with European standards.
Finite element analysis (FEA) and fluid-dynamic modeling ensure commutation geometry, segment insulation pitch, and dynamic balance match OE operational profiles.
Strict spectroscopic incoming checks verify graphite purity, copper electrical conductivity, and resin dielectric properties prior to pressing and compounding.
Multi-axis automated diamond turning lines hold segment runout under 0.003 mm, guaranteeing micro-smooth brush seating and zero electrical arcing.
100% computerized inspection benches verify dielectric withstand (hi-pot test), bar-to-bar resistance, dynamic balance, and hydraulic output under load.
Explore technical guides authored by our engineering department detailing the tribological and electronic mechanisms that govern fuel delivery longevity.
An in-depth analysis of how zirconia ceramic elements provide real-time air-fuel ratio telemetry to modern engine management systems, cutting exhaust emissions and preserving catalyst longevity.
Read Engineering Guide
Why modern alcohol-blended petrol (E10, E85) oxidizes copper armatures and how graphite self-lubrication extends pump life beyond 5,000 continuous hours.
Read Material Study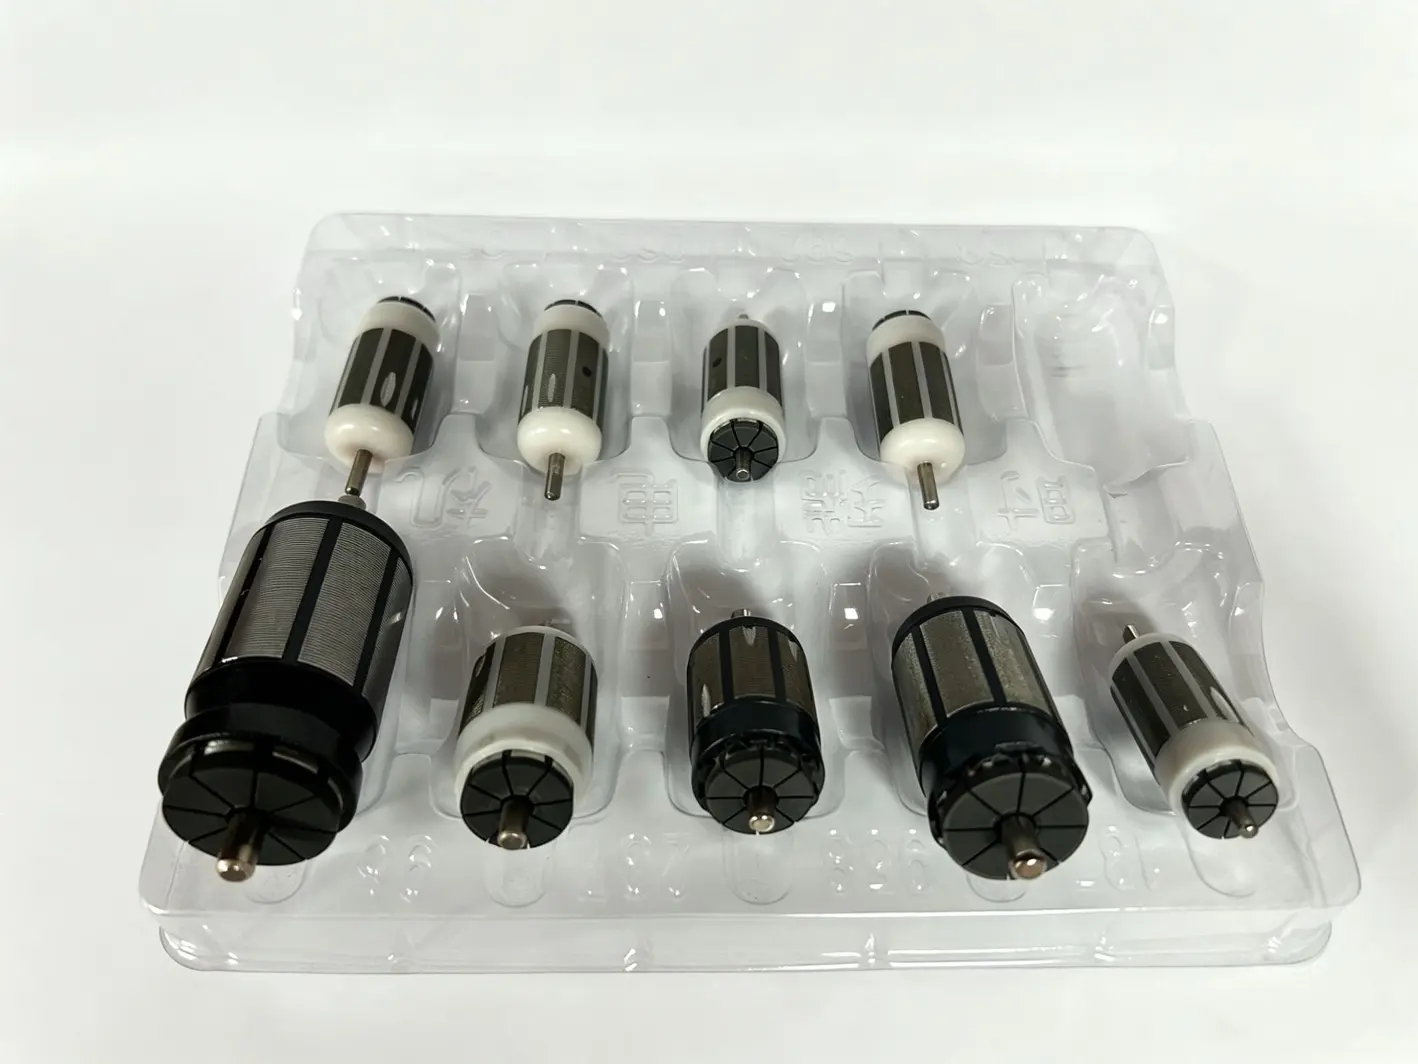
A breakdown of mechanical switching, reversal of winding magnetic fields, spark quenching, and rotational torque consistency in micro-motor armatures.
Read Physics Guide
Navigating global supply chain fluctuations, raw graphite commodity trends, and best practices for European importers sourcing directly from Chinese Tier-1 hubs.
Browse Tech BlogDirect answers for purchasing directors, component buyers, and automotive system engineers specifying electric fuel pumps and commutators.
Explore our complete catalog of electric fuel pump cores, graphite commutators, lambda sensors, and replacement assemblies available for direct container or palletized shipment.
Designed for compact, axial-flow fuel pump configurations where axial length is constrained. High copper-graphite interfacial bond strength.
Direct-injection feed pump core delivering sustained 4.5 to 6.0 Bar hydraulic pressure, optimized for modern turbocharged gasoline engines.
High-sensitivity lambda probe engineered with internal heating element for rapid activation within 15 seconds of cold engine start.
Our flagship export model for automotive remanufacturers across Central Europe. Extreme anti-pitting resilience under continuous duty.
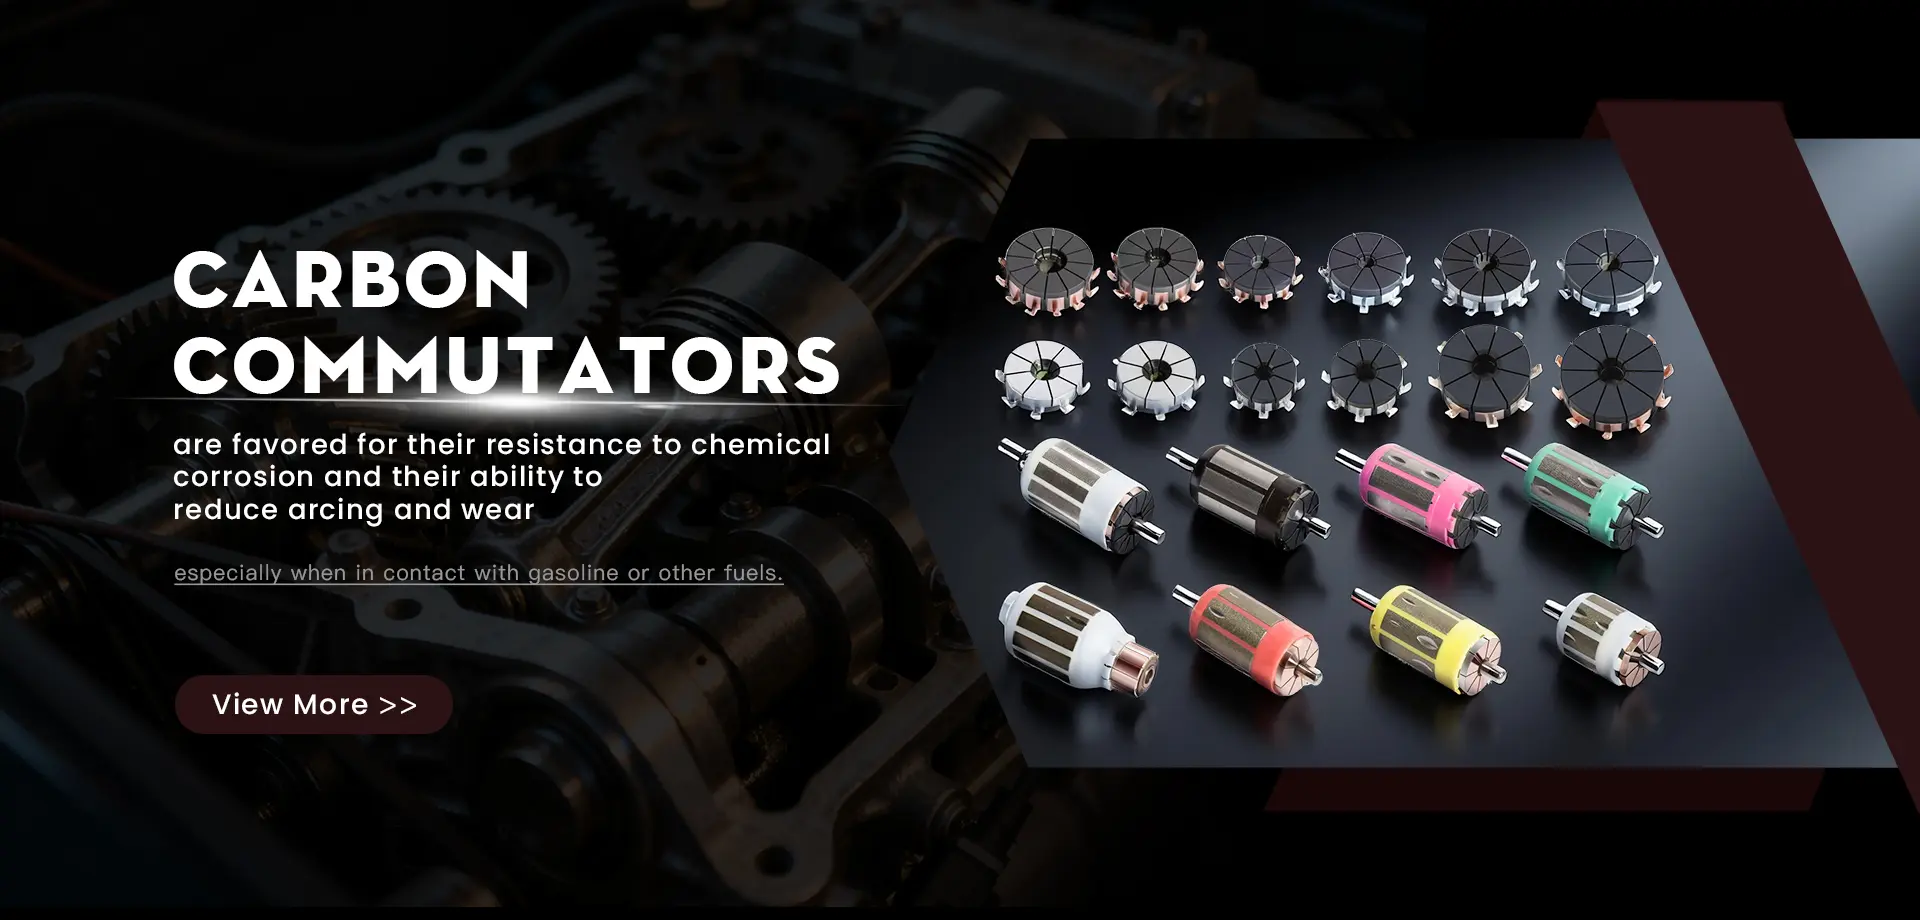
Industry-standard cylindrical configuration with high-purity graphite overlay and reinforced phenolic resin core for heavy thermal stability.
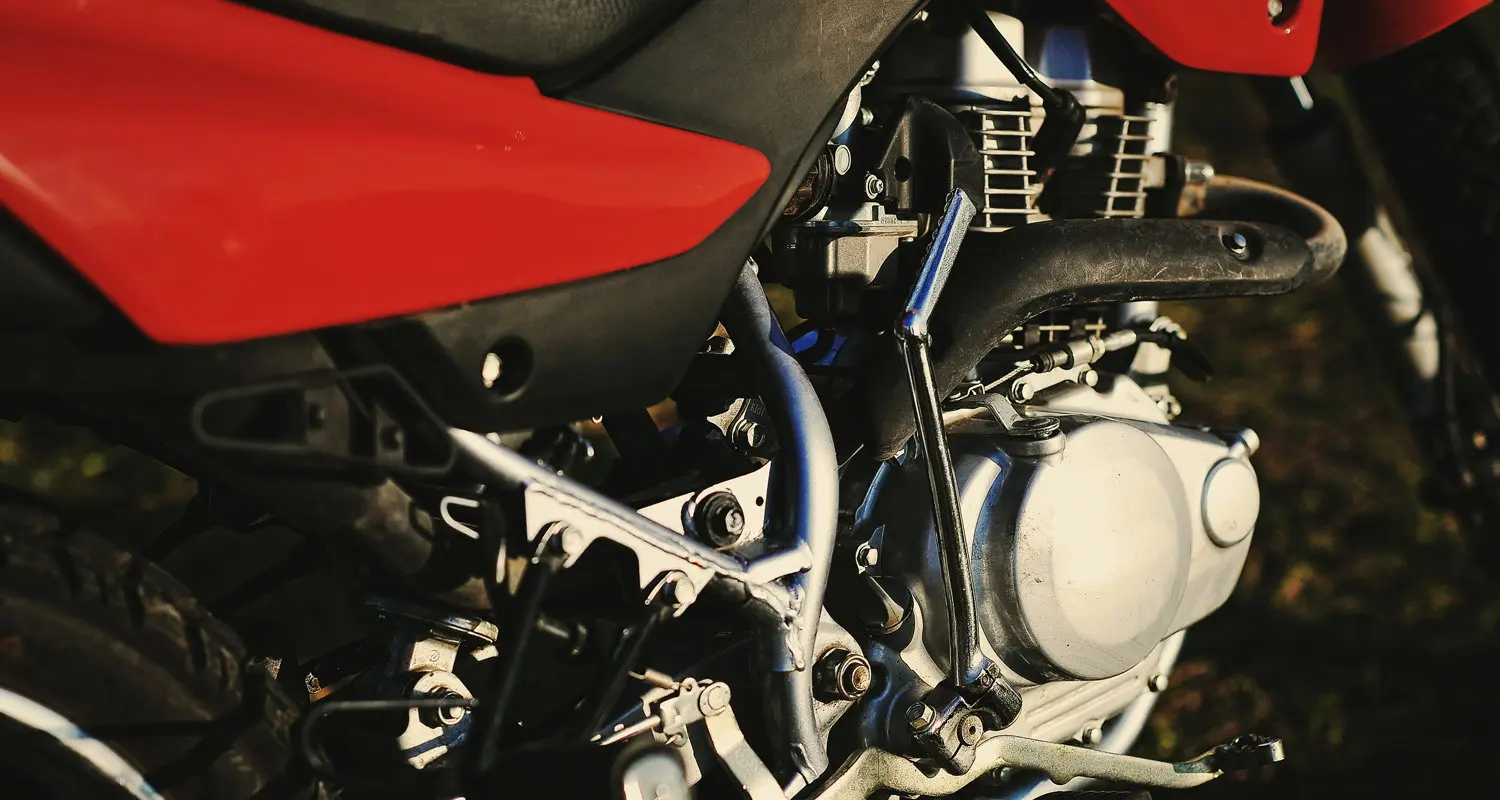
Compact form-factor pump engineered for Austrian motorcycle architectures. Resists severe vibration and continuous high-RPM commutation.
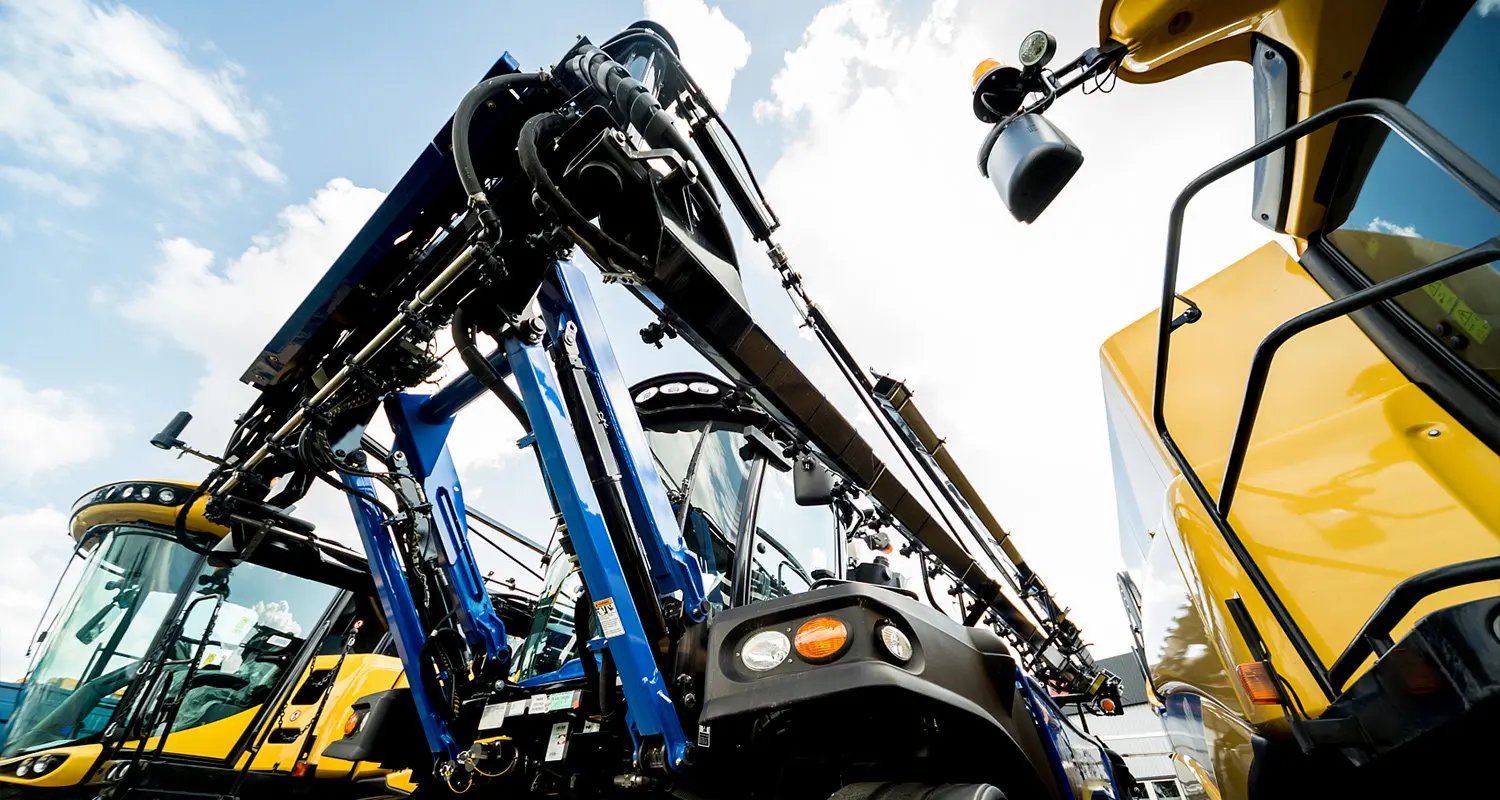
Engineered for high-vibration off-road vehicles, construction excavators, and agricultural tractors operating in dusty Alpine terrain.
Provides catalytic converter efficiency telemetry to OBD-II systems, ensuring passenger and utility vehicles pass Austrian §57a inspections.
Partner directly with Wenzhou Hualeao Automotive Parts Co., Ltd. for drawing evaluation, custom sample fabrication, and full container pricing optimized for the Austrian and Central European markets.
