Primary Fuel System & Electronic Commutator Assemblies
Engineered for direct replacement and OEM line integration across passenger fleets, public transit buses, and industrial machinery across Ethiopia and the Horn of Africa.
EFI fuel pumps and high-torque cores built around dynamic balance verification, providing consistent pressure delivery in high-elevation operating environments.
Upstream and downstream exhaust oxygen sensors that provide precise feedback to the vehicle ECU, optimizing fuel stoichiometry and protecting catalytic convertors.
Top-tier specification commutators requested by global fuel pump remanufacturers, specifically designed for extreme duty cycles and volatile fuel supplies.
Carbon Commutator Engineering Dynamics in Ethiopia & Global Trade
Evaluating the shift from conventional copper-segment commutators to advanced sintered carbon-graphite architectures within demanding transportation, logistics, and power generation corridors.
The Federal Democratic Republic of Ethiopia represents one of Africa's fastest-growing economies, centered around major infrastructural projects like the Hawassa and Bole Lemi Industrial Parks, and the vital trade corridor connecting Addis Ababa to the Port of Djibouti. However, operating internal combustion engines, auxiliary power units (gensets), and electric micro-motors in Ethiopia poses specific mechanical and chemical challenges.
Fuel supplies across East Africa frequently exhibit variances in sulfur concentration, particulate contamination, and alcohol blending (ethanol extracted from domestic sugarcane agro-industries). When submerged electric fuel pumps use standard copper commutators, electrolytic erosion and chemical oxidation rapidly wear down the copper segments, resulting in armature failure, dropped rail pressure, and stalled vehicles. Our high-density carbon-graphite commutators deliver total chemical passivity against ethanol and low-lubricity fuels, extending motor operational life up to 350% compared to traditional metallic surfaces.
High Altitude (2,300m+) Dielectric Reliability
Addis Ababa sits at approximately 2,355 meters above sea level. Thinner air and lower atmospheric pressures alter spark quenching dynamics across motor commutators. Carbon brush-to-commutator contact zones generate micro-arcs that rapidly oxidize standard alloys.
Hualeao's specialized resin-impregnated graphite ensures low electrical contact resistance, reduced electromagnetic interference (EMI), and self-lubricating surface contact films that preserve mechanical integrity in high-altitude environments.
Global Commutator Architecture Shifts
Worldwide, the transition to biofuel blends (such as E10, E20, and E85 flex-fuels) has rendered conventional metallic commutators obsolete in automotive fuel circuits. As Tier-1 powertrain manufacturers adopt higher injection pressures, the fuel pump core must sustain stable armature speeds exceeding 8,000 RPM continuously.
Modern carbon commutators replace single-metal contact faces with a bi-material structure: an internal copper base for maximum electrical conductivity and an outer specialized carbon layer that prevents metal migration, eliminates spark pitting, and withstands organic acids.
Chinese Precision Manufacturing: Cost-to-Performance Advantage
China's Yangtze and Pearl River Delta clusters have consolidated the entire value chain for micro-motor commutation. Based in Ruian, Wenzhou—the automotive component capital of China—Hualeao operates automated CNC grooving, isostatic graphite pressing, and automated visual inspection systems.
By producing over 20 million commutators annually, we provide Ethiopian importers, remanufacturers, and African regional distributors with components that meet German DIN and Japanese JASO automotive standards at a cost structure unachievable by European suppliers. This provides our African partners with healthy margins and predictable replacement part reliability.
Manufacturing Capabilities & Traceability
Closed-Loop Manufacturing from Ingot to Finished Commutator
How our Ruian, Wenzhou production hub implements strict zero-defect quality controls for every commutator shipped overseas.
PHASE 01
Raw Material Isostatic Pressing
Ultra-fine graphite powder is blended with specialized phenolic resins, subjected to cold isostatic pressing (CIP), and heat-treated to ensure uniform grain density and uniform electrical conductivity.
PHASE 02
Copper-Carbon Molecular Bonding
Using proprietary brazing and diffusion bonding processes, the graphite contact ring is bonded to oxygen-free copper substrate hooks without voids, ensuring mechanical shear strength under extreme centrifugal acceleration.
PHASE 03
High-Speed CNC Slotting
Segment isolation slots are diamond-milled to tight tolerances (slot widths controlled within ±0.02mm), preventing carbon dust short-circuiting while optimizing brush commutation timing.
PHASE 04
100% Dielectric & Balance Verification
Every single unit undergoes automated high-voltage surge breakdown tests (inter-segment insulation up to 500V DC) and sub-micron dimensional inspection via automated optical comparator systems.
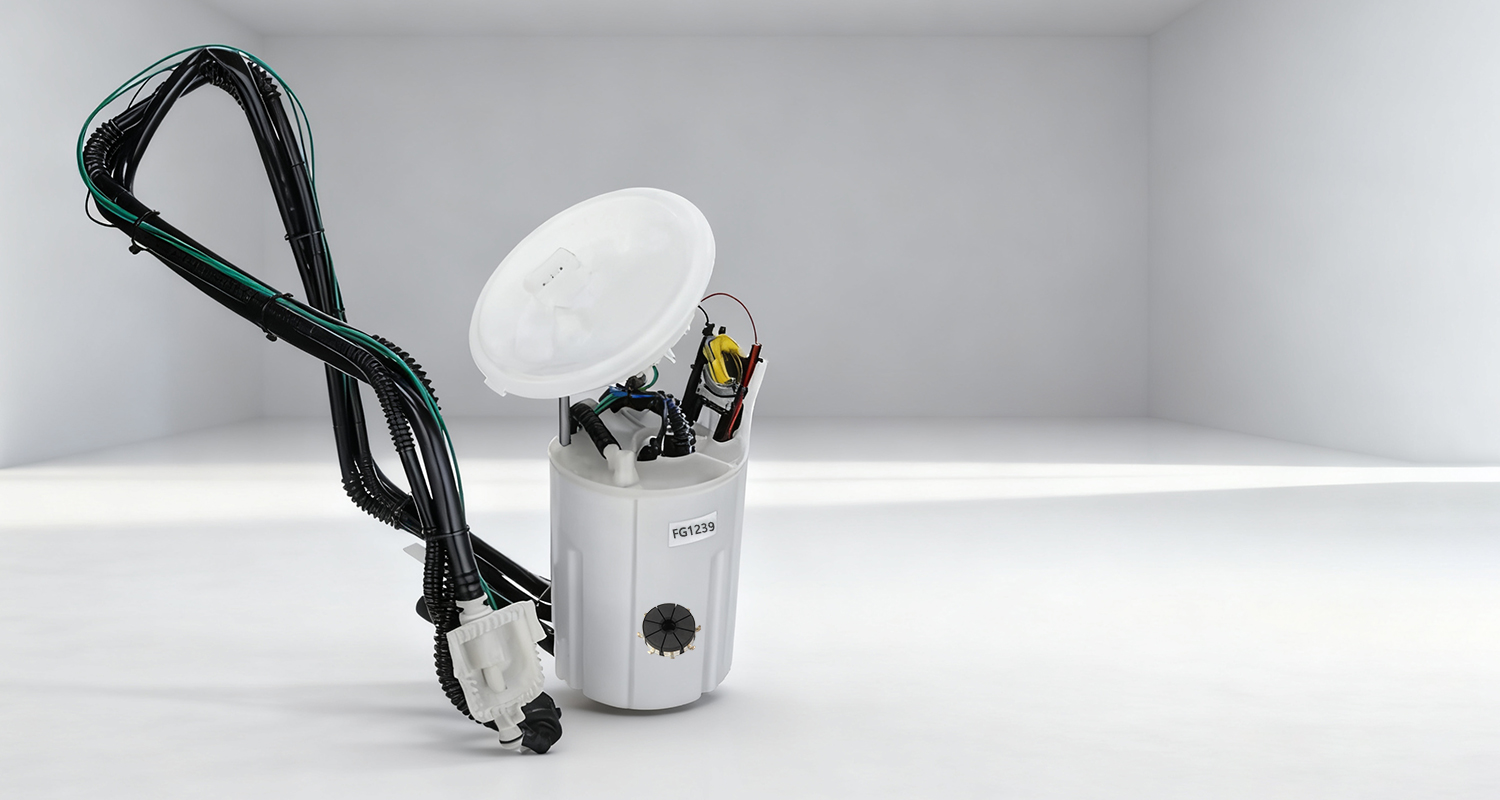
Designed for compact, submerged fuel pump armatures. High thermal resistance eliminates commutator surface glazing during dry tank cranking conditions.
Platinum-coated planar zirconia element providing rapid heater activation times, engineered to maintain accurate air-fuel ratio management on low-grade fuel.
Heavy-duty commuter segments built to endure severe dust, high-vibration off-road terrain, and uninterrupted daily duty cycles in quarry and construction vehicles.
Heavy displacement pump core designed for irrigation pumps, combine harvesters, and diesel fuel transfer assemblies operating under direct solar heat exposure.
Corrosion-resistant copper hooks with special salt-spray protective coatings, ideal for inland lake fishing vessels (Lake Tana) and stationary industrial diesel backup generators.
Meeting Global OEM & Aftermarket Procurement Criteria
Key evaluation points considered by technical buyers, parts distributors, and automotive assembly plants when selecting commutator manufacturers.
Material Homogeneity & Density
In low-cost commutators, micro-voids in sintered graphite cause uneven electrical resistance across segments, leading to localized hotspots and early failure. Hualeao utilizes high-density isostatic moulding that keeps segment resistance variance below 1.5% across production batches.
Drawing & Sample Customization (OEM / ODM)
We work directly with fuel pump motor engineers to optimize hook angles, core reinforcement dimensions, and outer diameter configurations. Provide your physical sample, 2D CAD blueprint, or 3D STEP file, and our engineering team can provide tooling analysis within 48 hours.
Consistent Supply Chain Logistics to Africa
Shipping into East Africa requires seasoned export documentation, maritime packaging that resists moisture-induced oxidation, and prompt lead times. Our location adjacent to Ningbo and Shanghai maritime ports enables rapid dispatch of consolidated containers and air shipments straight to Bole International Airport.
Practical guidance for engineering teams, procurement directors, and regional automotive wholesale managers.
What specific advantage does a carbon commutator provide in the Ethiopian fuel market?
Ethiopia's commercial fuel ecosystem features variable ethanol concentrations and fuel quality differences across regions. Standard copper commutators quickly experience electrochemical corrosion when exposed to alcohol blends, accelerating brush segment wear. Hualeao's carbon-graphite commutators are chemically inert, ensuring stable fuel pump performance, correct line pressure, and extended motor service life.
How does high altitude in cities like Addis Ababa affect electric motor commutation?
At high altitudes (above 2,000 meters), lower atmospheric air density reduces the dielectric breakdown threshold, making commutator brushes more susceptible to micro-arcing. Our resin-reinforced graphite composition maintains a self-healing tribological film on the commutator surface, keeping sparking down and eliminating the surface pitting common in standard copper commutators.
Can Hualeao manufacture customized commutators based on our proprietary samples or blueprints?
Yes. We have in-house tooling, CNC slotting, and mold development facilities. Send us your dimensional drawings (CAD/STEP), OE part numbers, or physical motor samples, and our engineering team will evaluate the copper-to-carbon ratio, hook configurations, and mechanical constraints to design a custom tooling configuration.
What are your typical shipping lead times and logistic arrangements for East Africa?
Standard catalog items are stocked for quick dispatch within 7 to 10 days. Custom production runs typically take 25 to 35 days for mold setup and volume production. We ship via ocean freight (FOB Ningbo or CIF Djibouti) or express air freight directly into Addis Ababa Bole International Airport (ADD), with comprehensive export documentation for customs clearance.
How does Hualeao ensure zero defects across high-volume production orders?
Our quality management system integrates continuous monitoring at every step. Raw materials are checked for graphite density and grain structure; segment isolation slots are monitored by automated optical inspection; and every commutator undergoes high-voltage insulation tests (surge breakdown testing up to 500V DC) before packaging to guarantee electrical separation between segments.
Ready to Strengthen Your Fuel Pump Component Supply Chain?
Get in touch with our engineering team today to request complete CAD drawings, material safety data sheets, and competitive FOB/CIF quotation schedules for the Ethiopian and international markets.